Why Do Global Buyers Choose Pharmaceutical Intermediates?

Why Do Global Buyers Choose Pharmaceutical Intermediates?

Global pharmaceutical manufacturers choose Pharmaceutical Intermediates because they connect scientific development with reliable commercial production. These compounds support the controlled synthesis of active pharmaceutical ingredients, often across several carefully monitored stages. A consistent intermediate can reduce production delays, simplify process validation, and protect final-product quality.

Dr. Janet Woodcock, former Director of the U.S. FDA’s Center for Drug Evaluation and Research, stated, “Quality cannot be tested into products; it has to be built into them.” This principle applies directly to Pharmaceutical Intermediates. Buyers examine purity profiles, impurity controls, analytical methods, batch records, and supplier traceability before signing long-term agreements. They also review manufacturing capacity, change-control procedures, worker safety, and compliance with applicable laws.

Consistency matters greatly.

A shipment may look acceptable while hiding process instability. One unexpected impurity can affect downstream reactions, timelines, and regulatory documentation. For this reason, experienced buyers value suppliers that provide transparent certificates of analysis, validated testing, stable packaging, and clear technical communication. They may also request pilot batches before approving routine supply.

Cost still matters, but the cheapest offer can become expensive after delays or failed testing. That assumption deserves careful review. No supplier is perfect, and global sourcing always carries logistical and quality risks. Strong buyers manage those risks through audits, documented specifications, responsible procurement, and regular performance monitoring. In practice, they choose Pharmaceutical Intermediates for more than price. They choose dependable chemistry, measurable quality, and a supply relationship that can withstand real production pressure.
Why Do Global Buyers Choose Pharmaceutical Intermediates?

What Are Pharmaceutical Intermediates?

Pharmaceutical intermediates are compounds made during pharmaceutical production. They are not finished medicines or active pharmaceutical ingredients. Under ICH Q7, an intermediate requires further molecular change or purification before becoming an API. In practice, this may look like a sealed drum of crystalline material, supported by batch records, test results, and controlled storage. The definition sounds simple, but manufacturing decisions are rarely simple.

Global demand makes these materials strategically important. The IQVIA Institute’s Global Use of Medicines 2024 report projects worldwide medicine spending will approach 2.3 trillion US dollars by 2028. That growth increases pressure on manufacturers to secure consistent, traceable inputs. Buyers examine impurity profiles, residual solvents, assay results, and batch-to-batch stability. A lower price can mislead. Rework, delayed testing, or unstable material may cost much more.

Experienced purchasers also review production capacity and technical documentation before signing supply agreements. They may request samples, audit records, change-control procedures, and transport data. The European Medicines Agency’s guidance on active substances emphasizes robust quality systems and traceability across the supply chain. These expectations explain why pharmaceutical intermediates are often sourced from specialized producers. Still, no supplier is perfect. A strong qualification process should question optimistic specifications, verify real production evidence, and leave room for unexpected results.

Why Do Global Buyers Choose Pharmaceutical Intermediates? - What Are Pharmaceutical Intermediates?

Dimension What It Means Typical Examples or Characteristics Why Global Buyers Value It Important Evaluation Indicators
Definition A pharmaceutical intermediate is a compound produced during the chemical or biological synthesis of an active pharmaceutical ingredient (API). It is not normally the final medicine or finished dosage form; it undergoes one or more additional transformation steps. Intermediates allow manufacturers to divide complex API production into controlled, manageable stages. Chemical identity, structure, purity profile, manufacturing route, and intended process stage.
Role in API Manufacturing Intermediates connect starting materials with the final API through sequential reactions, purification, and analytical testing. A production route may include protected compounds, chiral intermediates, key advanced intermediates, and isolated process intermediates. The buyer can source a defined stage of the route instead of developing every synthesis step internally. Step consistency, impurity control, batch reproducibility, and compatibility with the buyer’s downstream process.
Product Types Intermediates may be classified by their position in the synthesis route and by their chemical function. Common groups include advanced intermediates, chiral intermediates, heterocyclic intermediates, protected intermediates, and building blocks. A broad product range supports different therapeutic areas and synthetic strategies. Functional groups, stereochemical purity, water content, residual solvents, and stability during storage.
Cost Efficiency Purchasing an intermediate can reduce the need for in-house investment in equipment, personnel, process development, and raw-material sourcing. The economic benefit depends on reaction yield, raw-material cost, purification requirements, batch size, and transportation conditions. It may lower total manufacturing cost and improve the utilization of internal production capacity. Total landed cost, yield impact, packaging, shipping requirements, customs classification, and supplier consistency.
Development Speed A qualified intermediate can shorten the time required to begin downstream process development or scale-up. Buyers may evaluate samples, laboratory batches, pilot quantities, and commercial-scale batches before approval. Faster access to a reliable starting point can support development timelines and supply planning. Sample availability, technical response time, documentation completeness, and scale-up history.
Quality Requirements Quality is assessed against agreed specifications rather than appearance alone. Typical tests include identification, assay, related substances, residual solvents, water content, elemental impurities, and optical purity where applicable. A controlled impurity profile helps protect downstream API quality and process performance. Certificate of analysis, validated or qualified analytical methods, reference standards, and batch-to-batch data.
Regulatory Documentation Documentation demonstrates the identity, traceability, control strategy, and handling requirements of the material. Documents may include specifications, certificates of analysis, safety data sheets, impurity information, and change-control statements. Complete records make supplier qualification, audits, import procedures, and internal quality reviews more efficient. Document accuracy, revision control, traceability, audit readiness, and alignment with applicable regulations.
Supply Security Supply security refers to the ability to deliver the required material consistently over time. Relevant factors include manufacturing capacity, raw-material availability, lead time, inventory policy, and contingency planning. Reliable intermediate supply reduces the risk of interruptions to API production. On-time delivery record, capacity information, forecast flexibility, business continuity planning, and geographic logistics.
Customization Potential Some intermediates can be produced to agreed specifications for a particular downstream process. Customization may involve particle characteristics, impurity limits, packaging configuration, batch size, or production route development. Material properties can be matched more closely to process, equipment, and formulation requirements. Technical capability, confidentiality controls, development support, scale-up feasibility, and change-management procedures.
International Logistics Pharmaceutical intermediates are shipped according to their physical, chemical, and regulatory characteristics. Packaging, labeling, temperature control, hazardous-goods classification, shelf life, and moisture sensitivity may affect transportation. Professional logistics management supports product integrity and predictable delivery across borders. Packaging validation, transport conditions, customs documents, shelf-life data, and shipment traceability.
Buyer Selection Priorities Global buyers generally assess commercial, technical, quality, regulatory, and supply-chain factors together. The lowest quoted price is not necessarily the lowest overall cost if quality failures, delays, or process changes occur. A balanced supplier assessment supports long-term production continuity and compliance. Quality consistency, technical support, regulatory readiness, delivery reliability, scalability, and total cost of ownership.

How Do Intermediates Support Pharmaceutical Manufacturing?

Pharmaceutical intermediates support manufacturing by connecting raw materials with the active pharmaceutical ingredient. They are processed through controlled chemical steps, purification, and analytical testing. In a typical facility, technicians may track reaction temperature, mixing speed, moisture, and batch color. These details help maintain consistent quality before the final ingredient enters formulation.

Reliable intermediates also improve production planning. Manufacturers can select suitable materials for scale-up, reduce process interruptions, and manage inventory more accurately. A well-documented intermediate includes specifications, impurity profiles, storage conditions, and test methods. Certificates of analysis provide useful evidence, but buyers should still review testing procedures and supplier records. Documentation is not decoration.

Tips: Check identity, purity, residual solvents, stability data, and packaging before purchase. Ask how the material performed in pilot or commercial-scale batches. Small differences in particle size or moisture can affect later processing. Supplier audits and sample evaluation add practical confidence. Yet no system is perfect. Unexpected impurities may appear after process changes, and transport conditions can be overlooked. Careful communication between quality, procurement, and manufacturing teams remains essential.

Why Do Global Buyers Choose Pharmaceutical Intermediates?

How intermediates support pharmaceutical manufacturing

Pharmaceutical intermediates help manufacturers build reliable supply chains by enabling specialized synthesis, flexible sourcing, production scaling, and better control of active pharmaceutical ingredient manufacturing.

Selected published supply-chain indicators. The percentages use different published denominators and are shown for context rather than as directly comparable market shares. Sources: U.S. FDA, “Drug Shortages: Root Causes and Potential Solutions” (2019); European Commission, “Pharmaceutical Strategy for Europe”; WHO and industry supply-chain publications.

Why Do Global Buyers Prefer Specialized Suppliers?

Global buyers choose pharmaceutical intermediates for more than competitive pricing. They need dependable quality at every production stage. Specialized suppliers understand this pressure because they work with narrow product categories daily. Their teams can discuss purity profiles, impurity risks, analytical methods, and storage conditions with practical detail.

A specialized supplier usually provides stronger batch traceability. Each drum may carry a batch number, manufacturing date, test status, and storage instruction. Buyers can review certificates of analysis, technical data, and controlled documentation before shipment. Clear communication also matters. A responsive technical contact can explain a deviation instead of sending a vague email. Small details often protect large production schedules.

Experience still has limits. A supplier may have excellent laboratory data but weak export coordination. That gap can delay customs clearance or damage temperature-sensitive materials. Responsible buyers therefore review manufacturing controls, quality agreements, audit records, and applicable regulatory requirements. Independent testing may also be appropriate for higher-risk materials. It costs more time, but assumptions cost more later. Not every supplier will fit every project. Some communication may be imperfect, and specifications can change during development. Honest discussion makes those problems visible early, while disciplined documentation keeps decisions reliable.

Which Quality and Regulatory Factors Influence Purchasing?

Global buyers choose pharmaceutical intermediates when quality evidence supports consistent production. Price matters, but one failed batch can delay a finished product for weeks. Buyers examine the certificate of analysis, assay results, impurity profiles, and residual solvent data. They also check whether testing methods are validated and suitable for the material. A clean document is useful, but it is not complete proof. Sampling errors and outdated specifications can still create risk.

Tips: Request recent batch records and clear traceability. Compare supplier specifications with your target market’s requirements. Ask how deviations, complaints, and changes are documented. Review packaging details, storage conditions, and transport controls. Small gaps often appear there.

Regulatory readiness strongly influences purchasing decisions. Reliable suppliers should explain their quality system, manufacturing controls, and change-notification process. Evidence of good manufacturing practice can support confidence, but buyers should review its scope and validity carefully. Some markets may require additional technical files, impurity assessments, or registration support. A supplier that responds quickly with precise records is easier to qualify. However, speed should not replace verification. I have seen procurement teams trust familiar paperwork too quickly. That assumption deserves review. Clear audit trails, stable production data, and transparent communication usually matter more than polished presentations. In practice, buyers often prefer a supplier willing to discuss an unexpected result honestly.

How Do Cost, Supply, and Customization Shape Buyer Decisions?

Global buyers choose pharmaceutical intermediates when cost, supply, and customization work together.

IQVIA Institute’s Global Use of Medicines 2024 projects worldwide medicine spending will reach about $2.3 trillion by 2028. That growth increases pressure on intermediate suppliers. Buyers compare more than price. They examine batch consistency, documentation, lead times, and technical support.

Supply reliability often decides the contract. The U.S. FDA’s Drug Shortages Task Force reported that 62% of shortages involved manufacturing or product-quality problems. Therefore, buyers increasingly request dual sourcing, stability data, and clear change-control procedures.

A 25-kilogram drum is not useful if its certificate of analysis arrives late. Customization also matters. Suppliers may adjust particle size, impurity limits, packaging, or synthesis routes. These changes can reduce downstream rework and improve process yield.

However, customization can increase validation time and cost. It is not always the faster option.

Tips:

Compare total landed cost, not only the quoted kilogram price. Review audit records, analytical methods, and deviation histories. Ask for realistic lead times under peak demand. Confirm whether a custom specification is scientifically necessary. A cheaper intermediate may create hidden testing costs. Buyers should also challenge their own assumptions. Forecasts can be wrong, and “secure” supply may still depend on one production site. Clear quality agreements and documented communication remain practical safeguards.

Article Source:

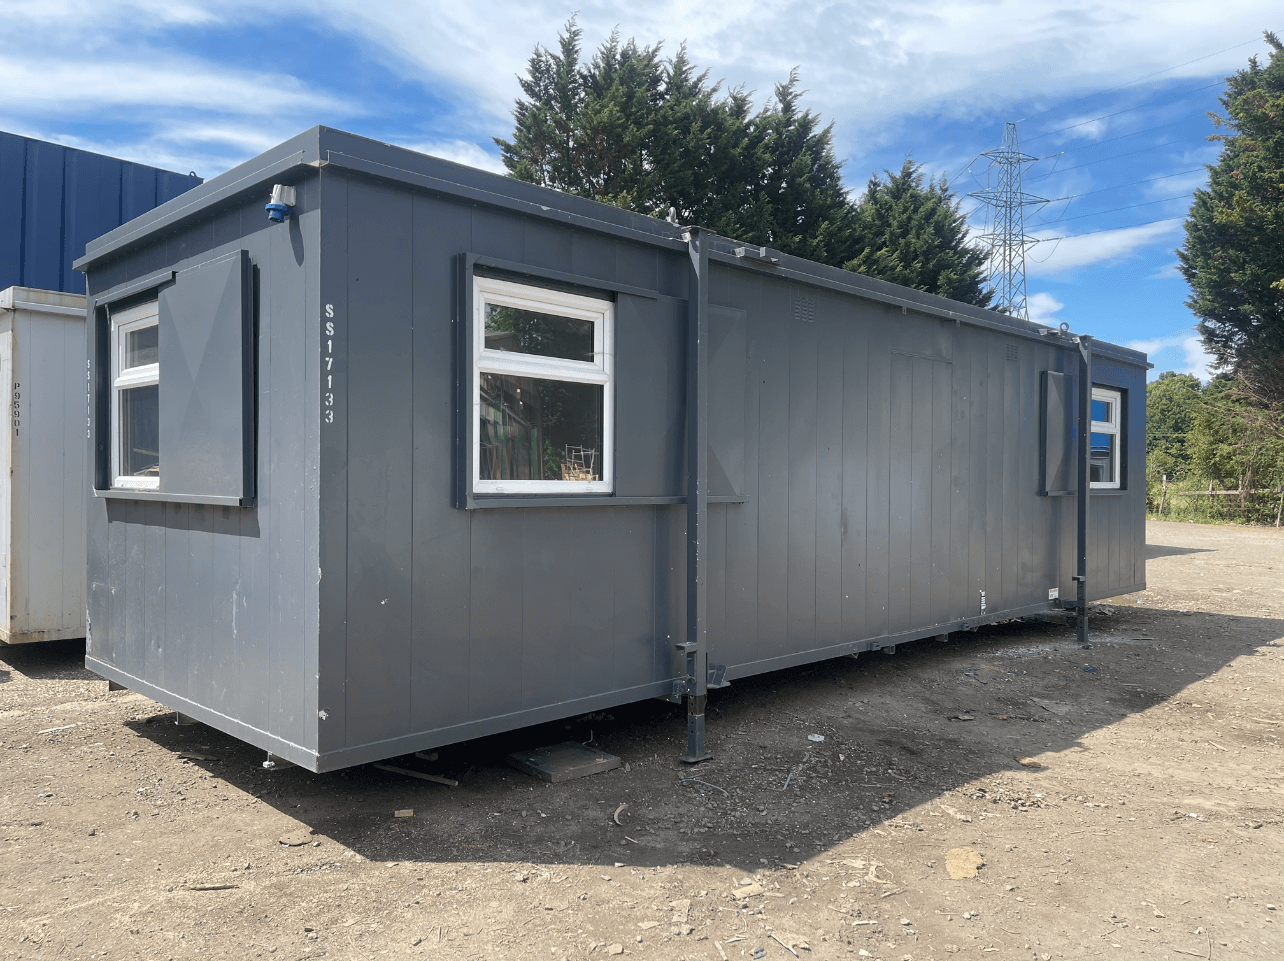
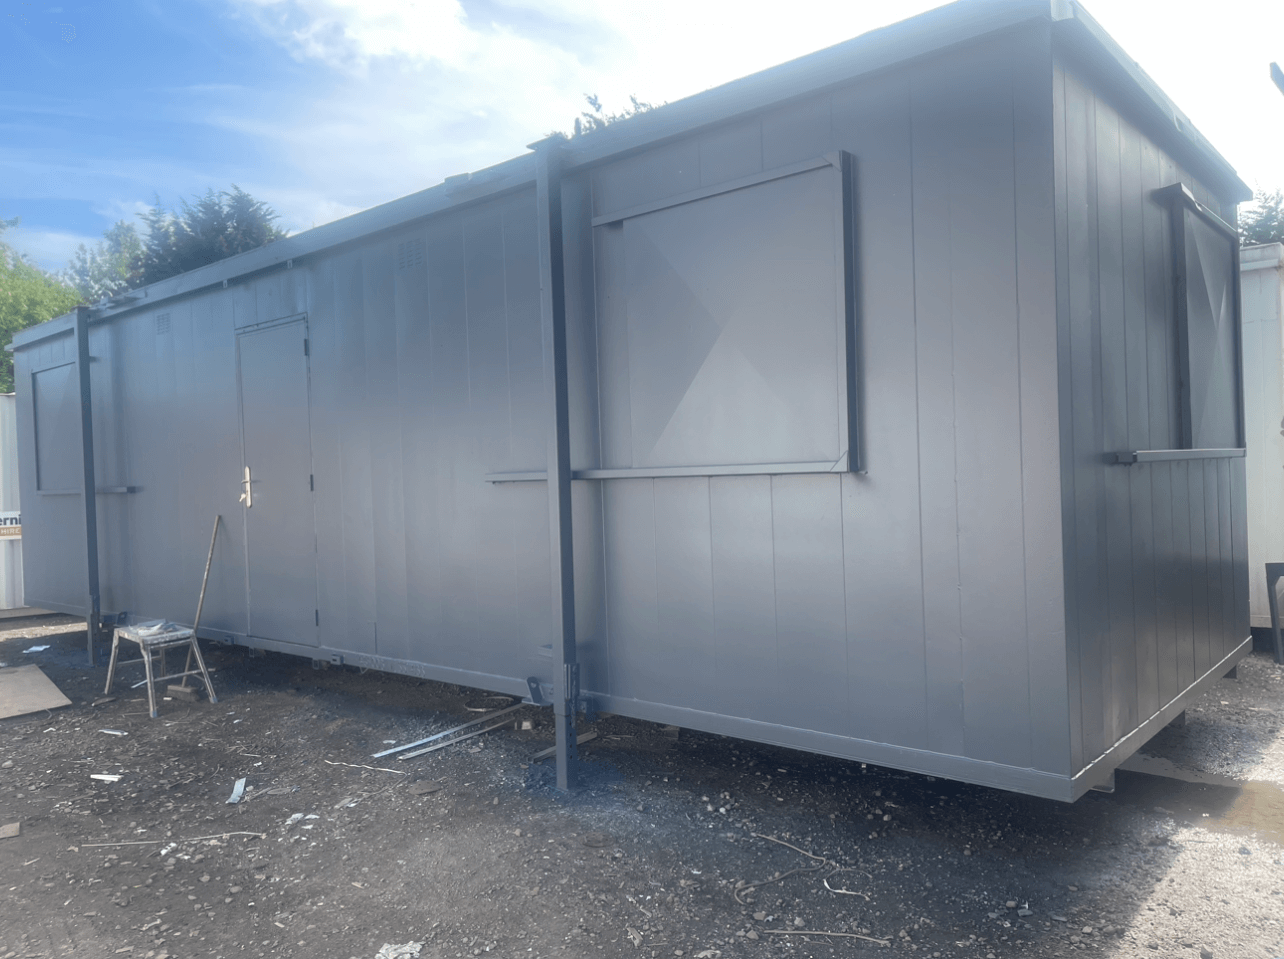
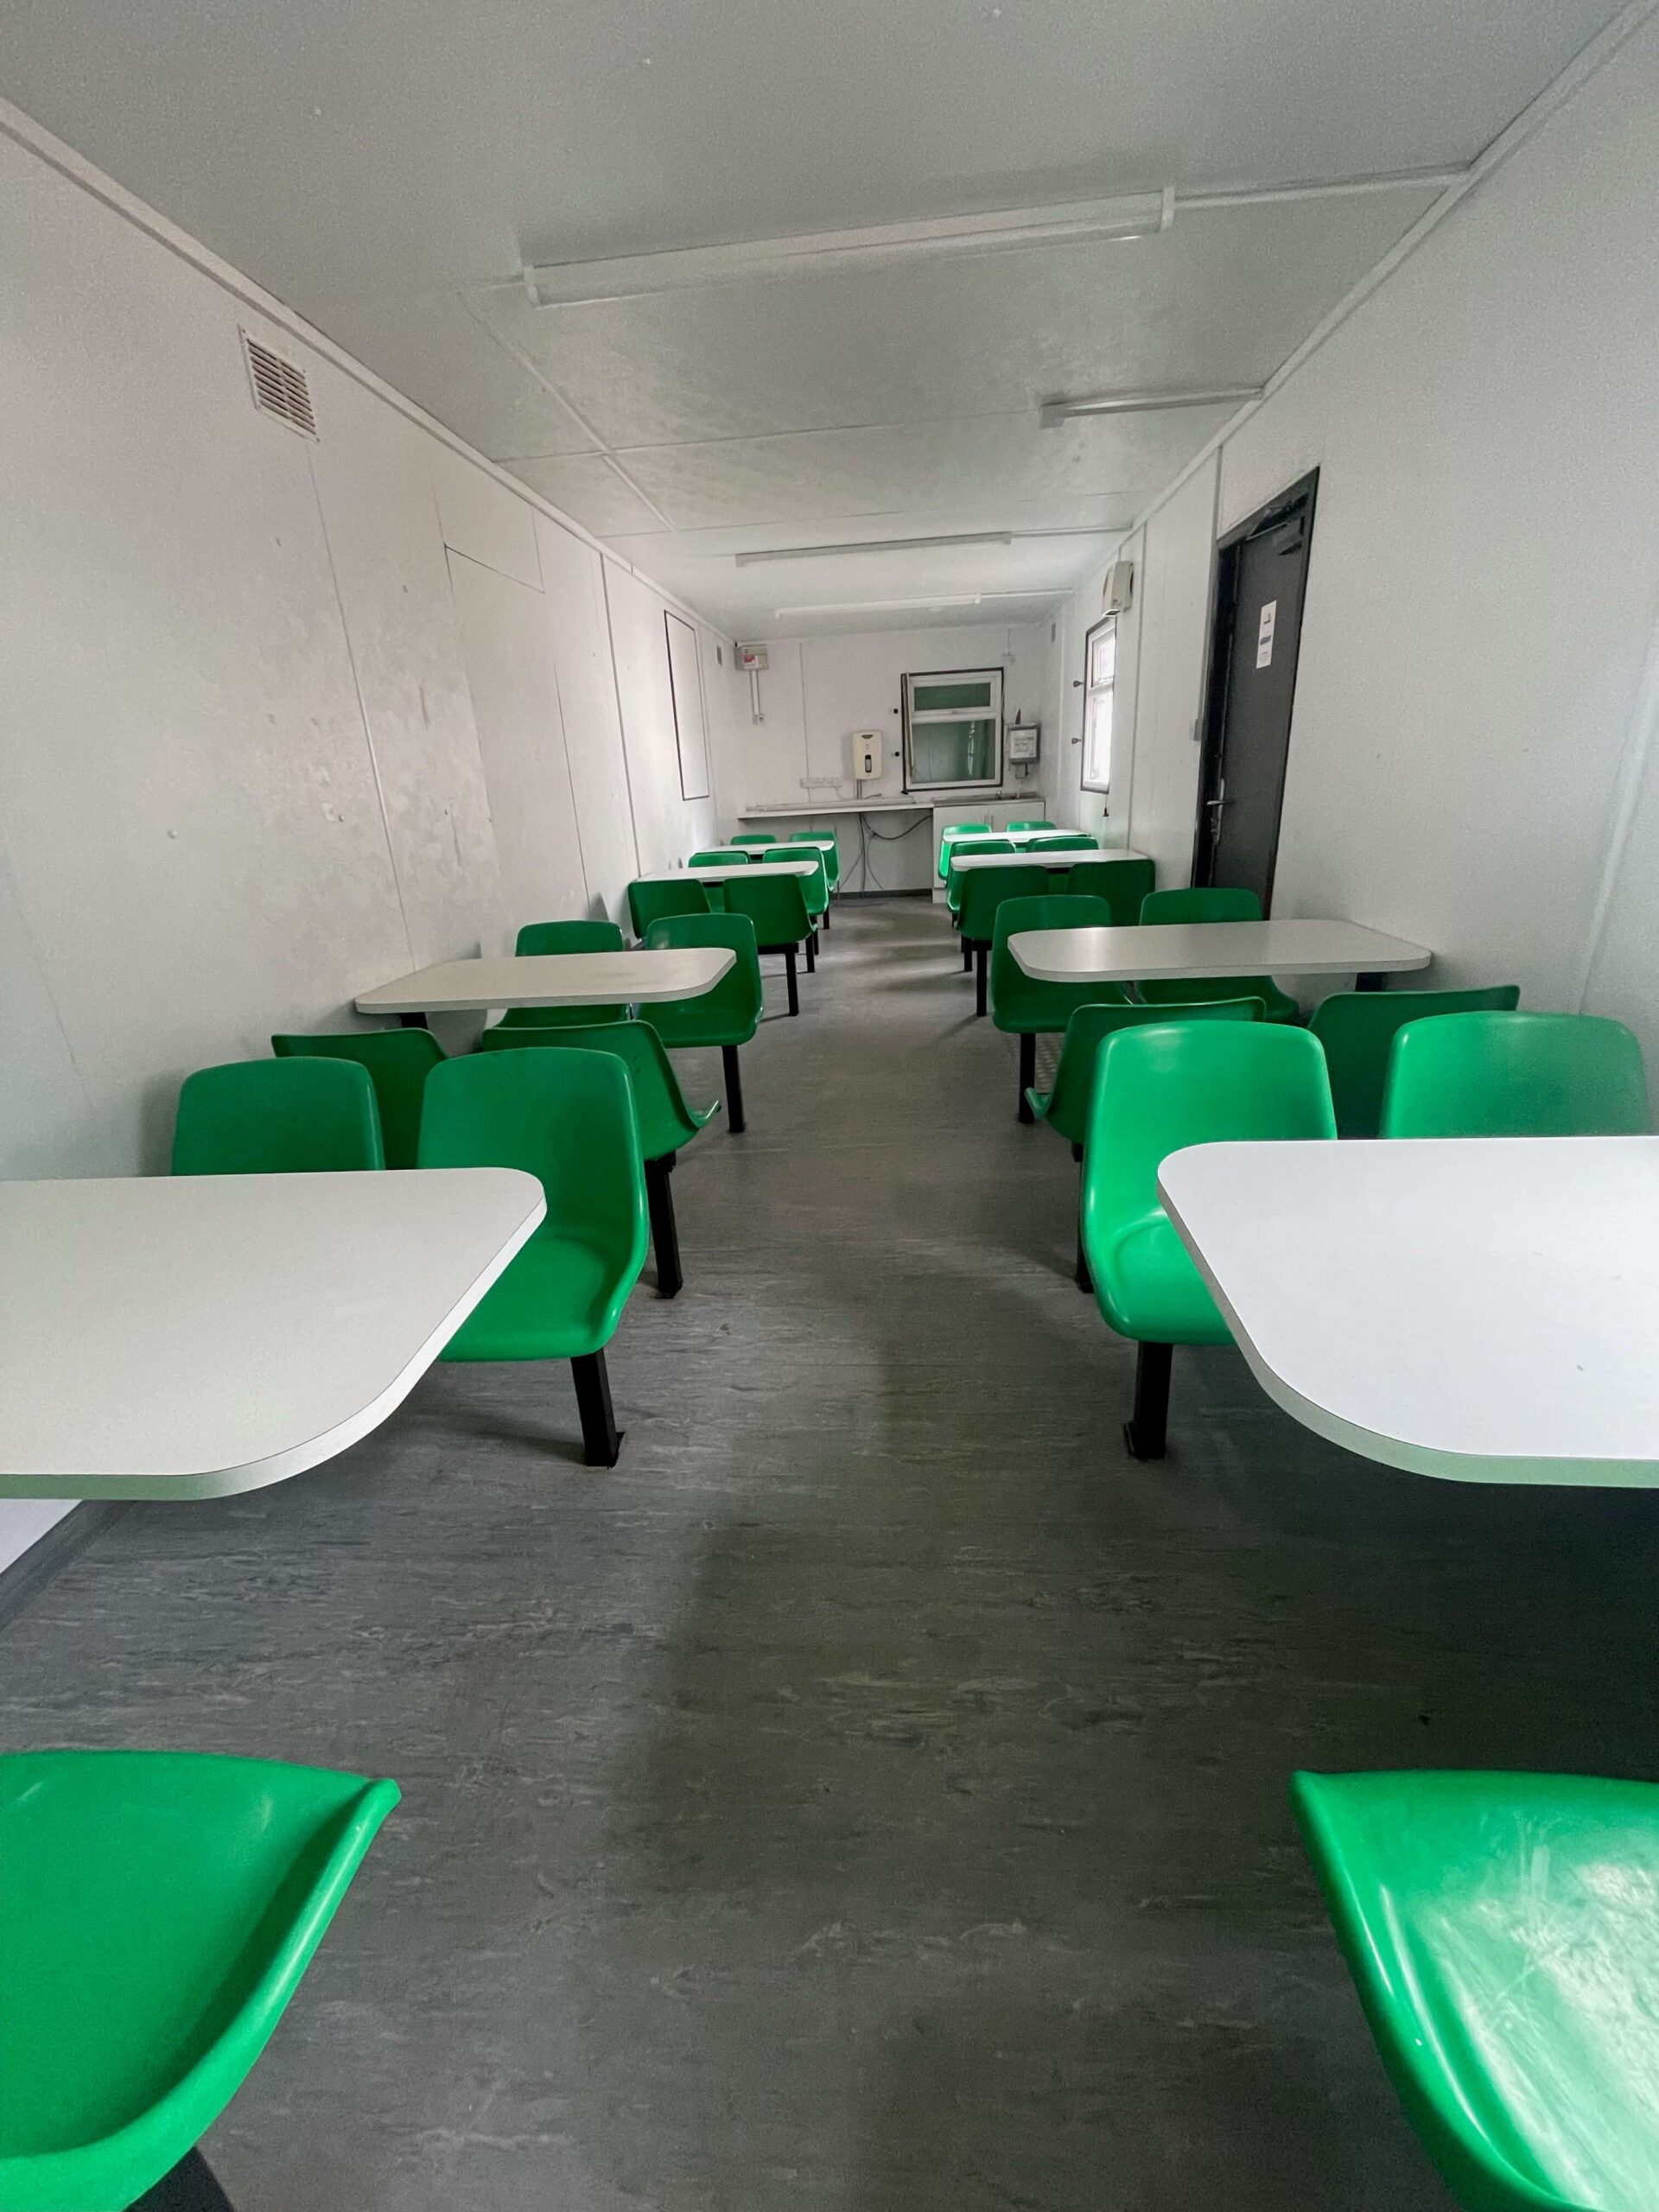
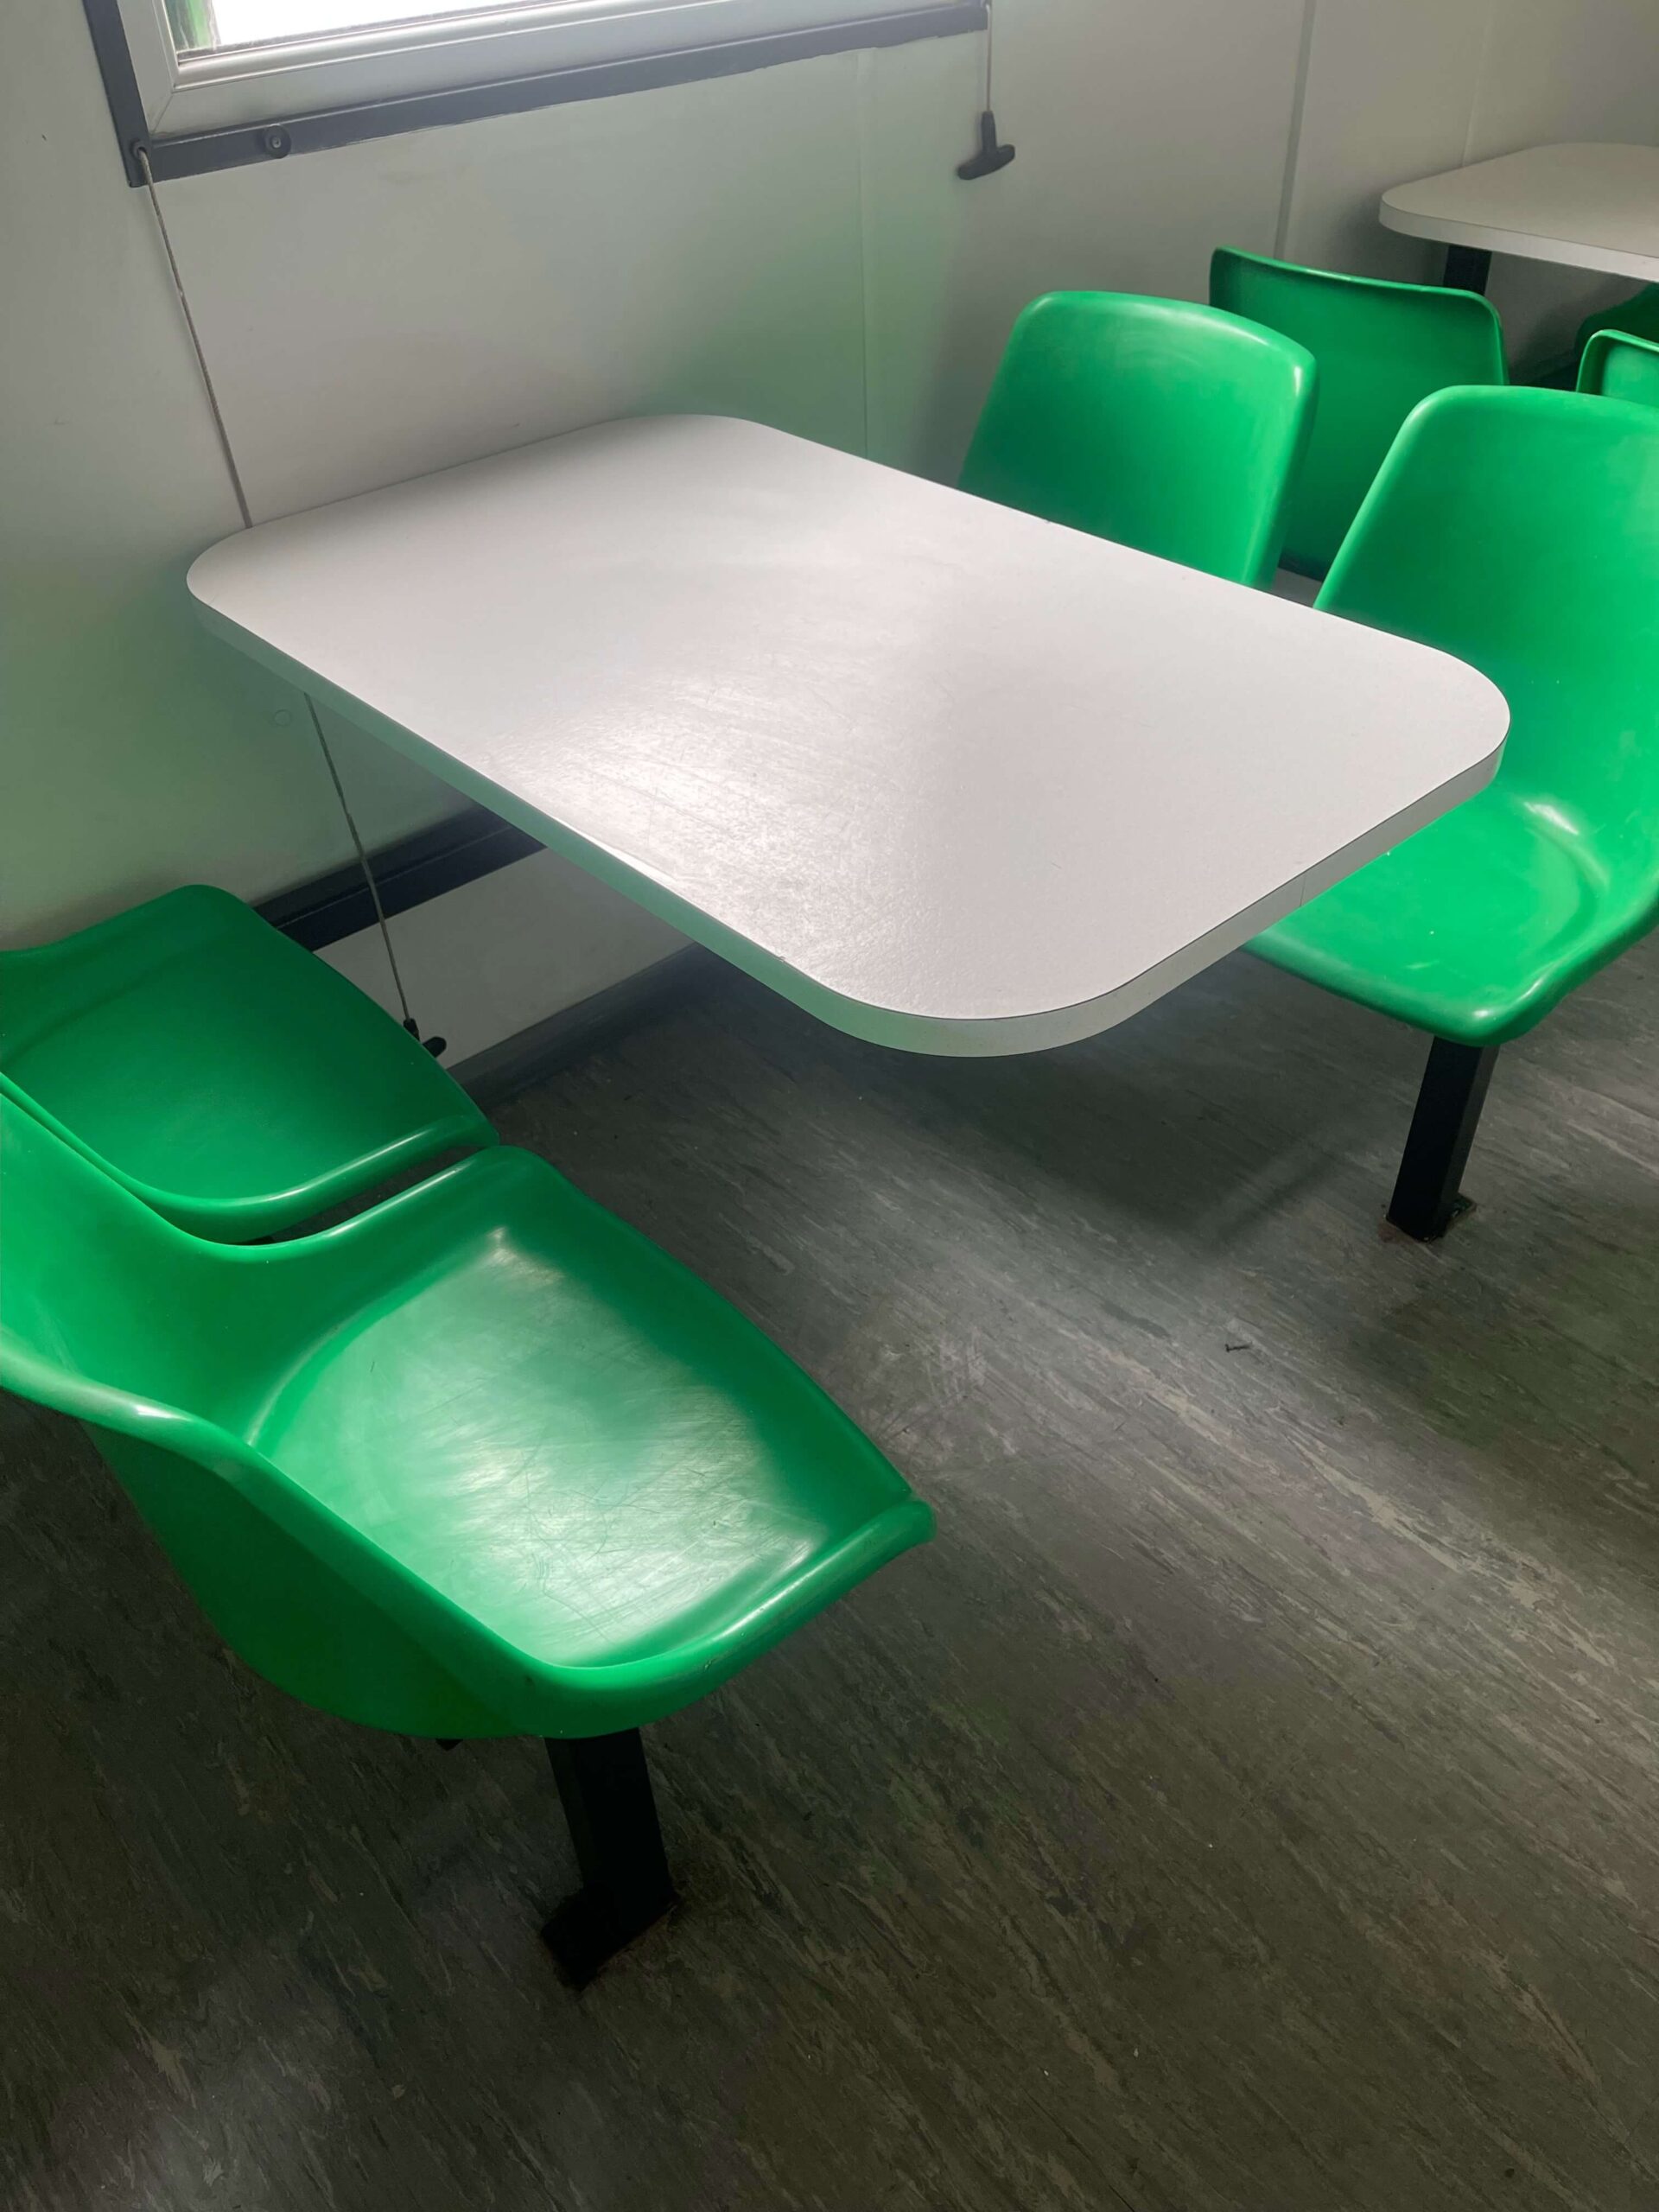
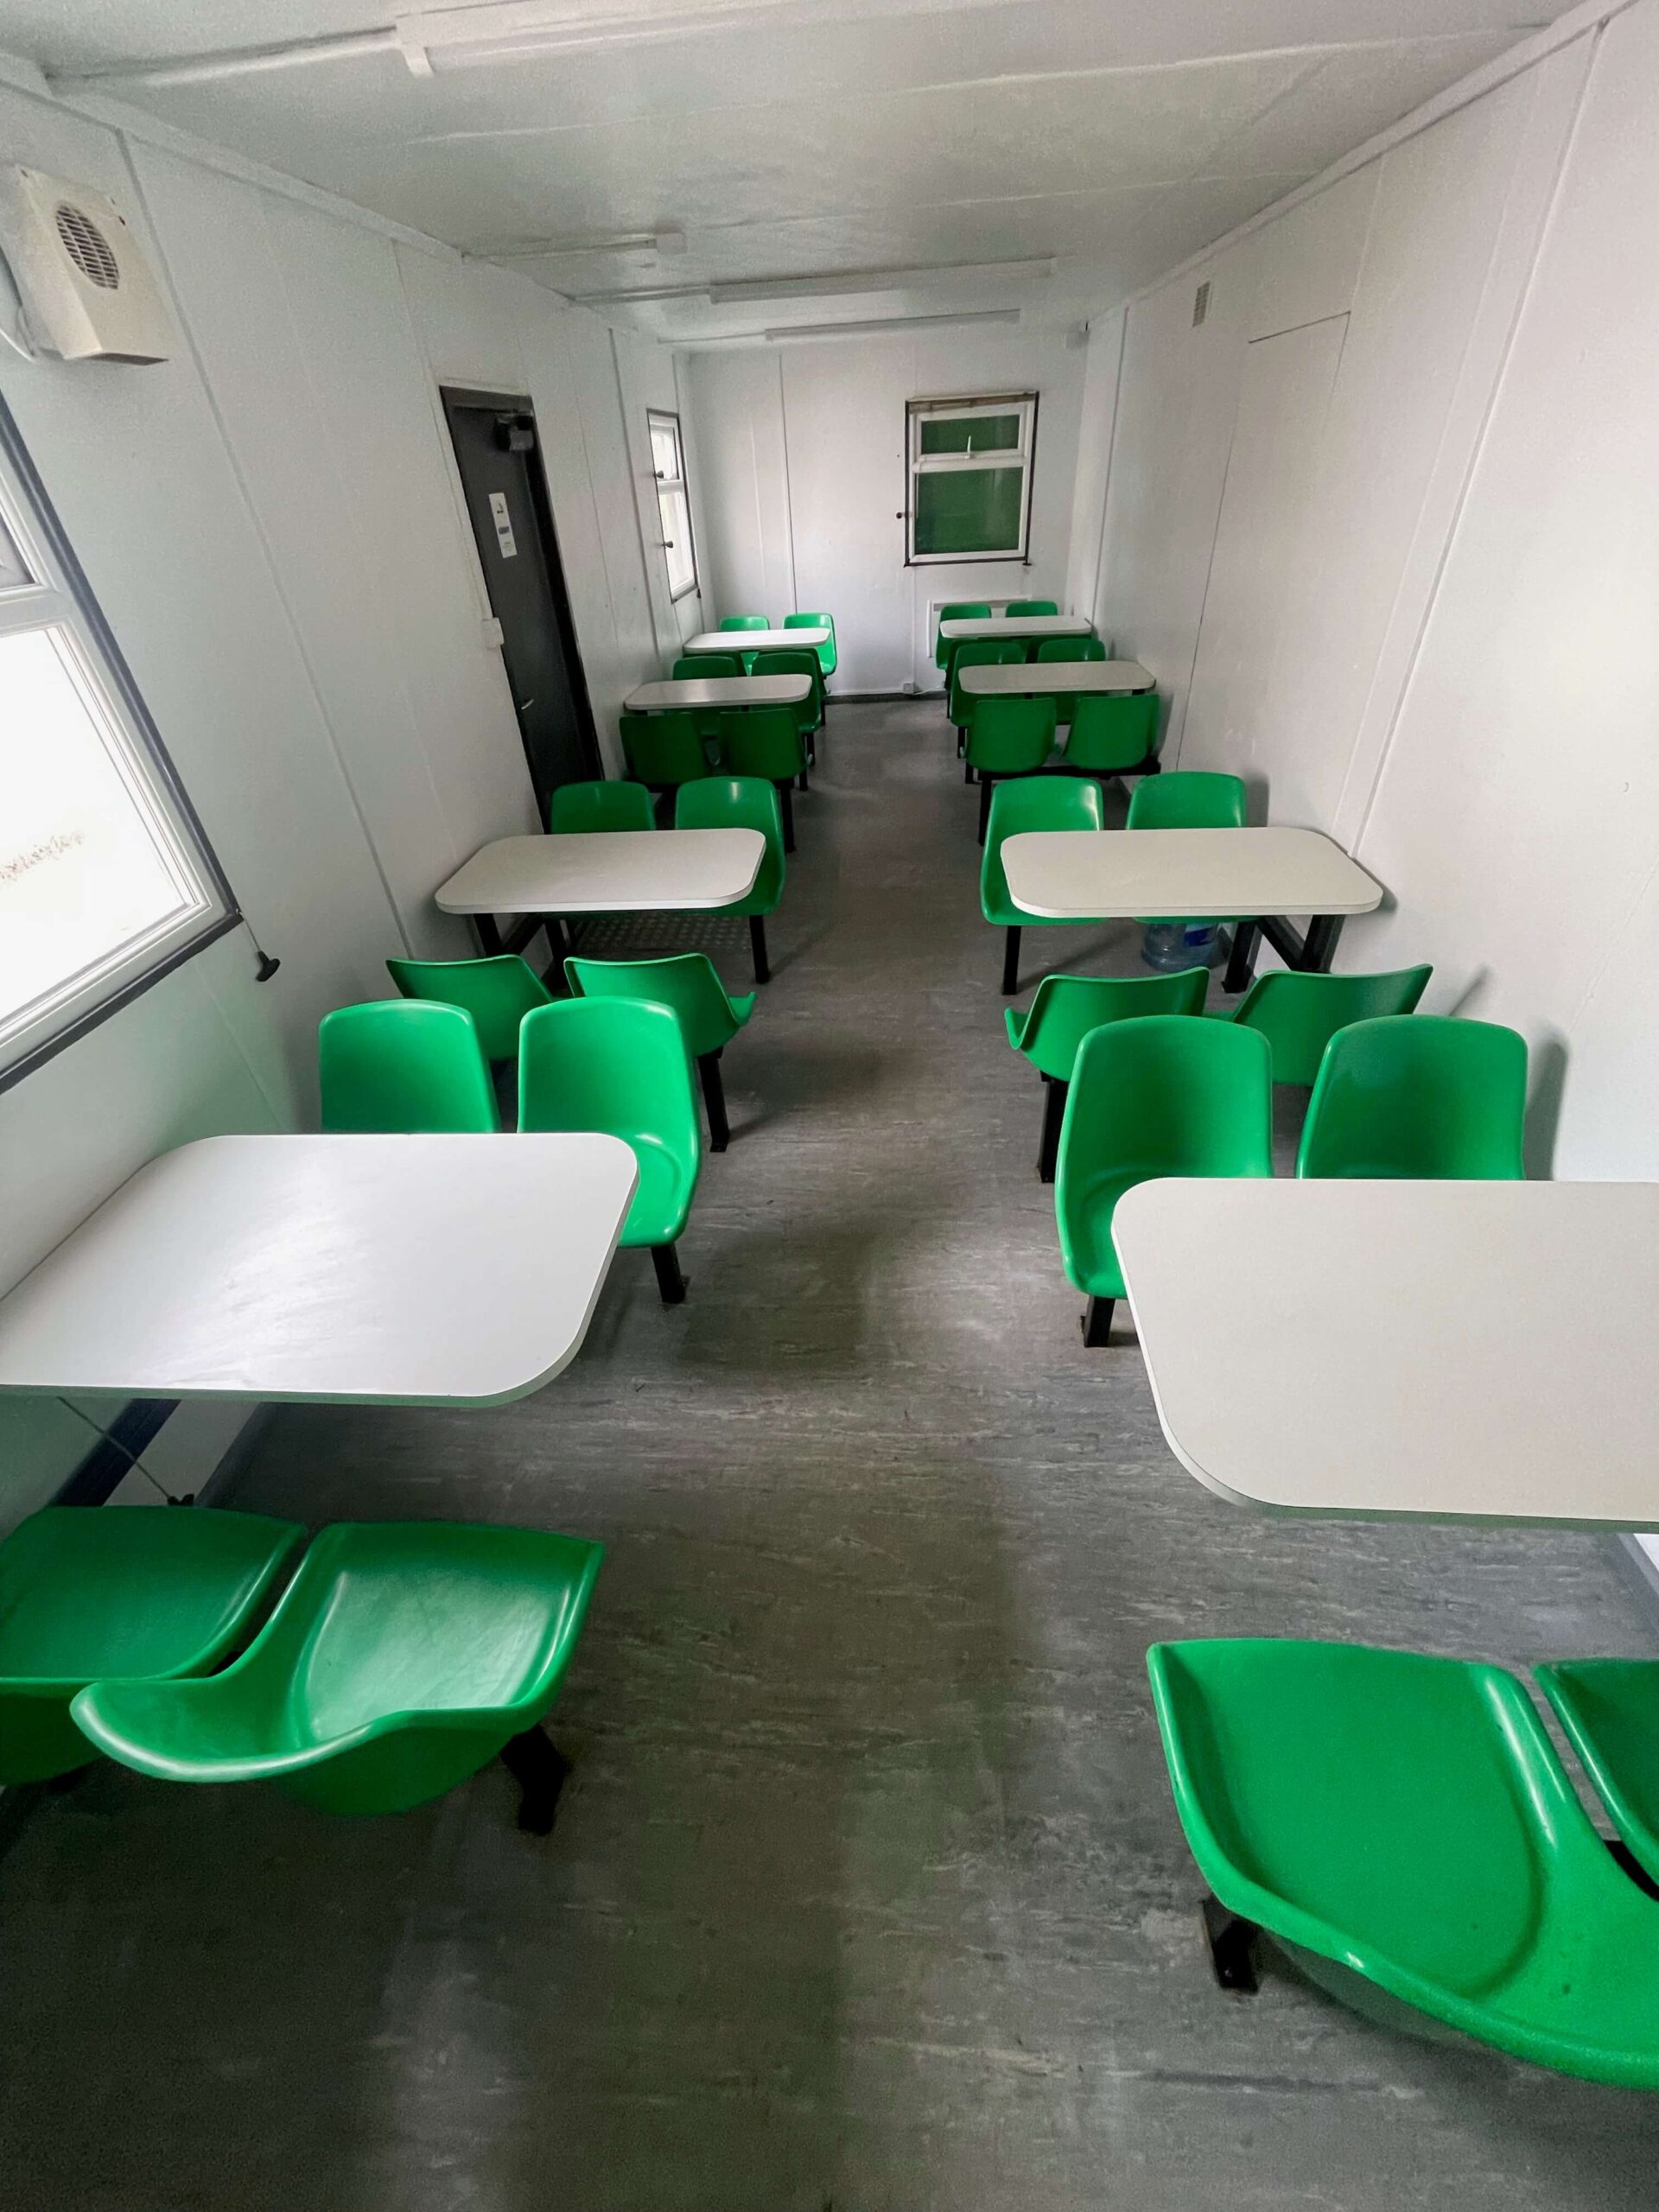
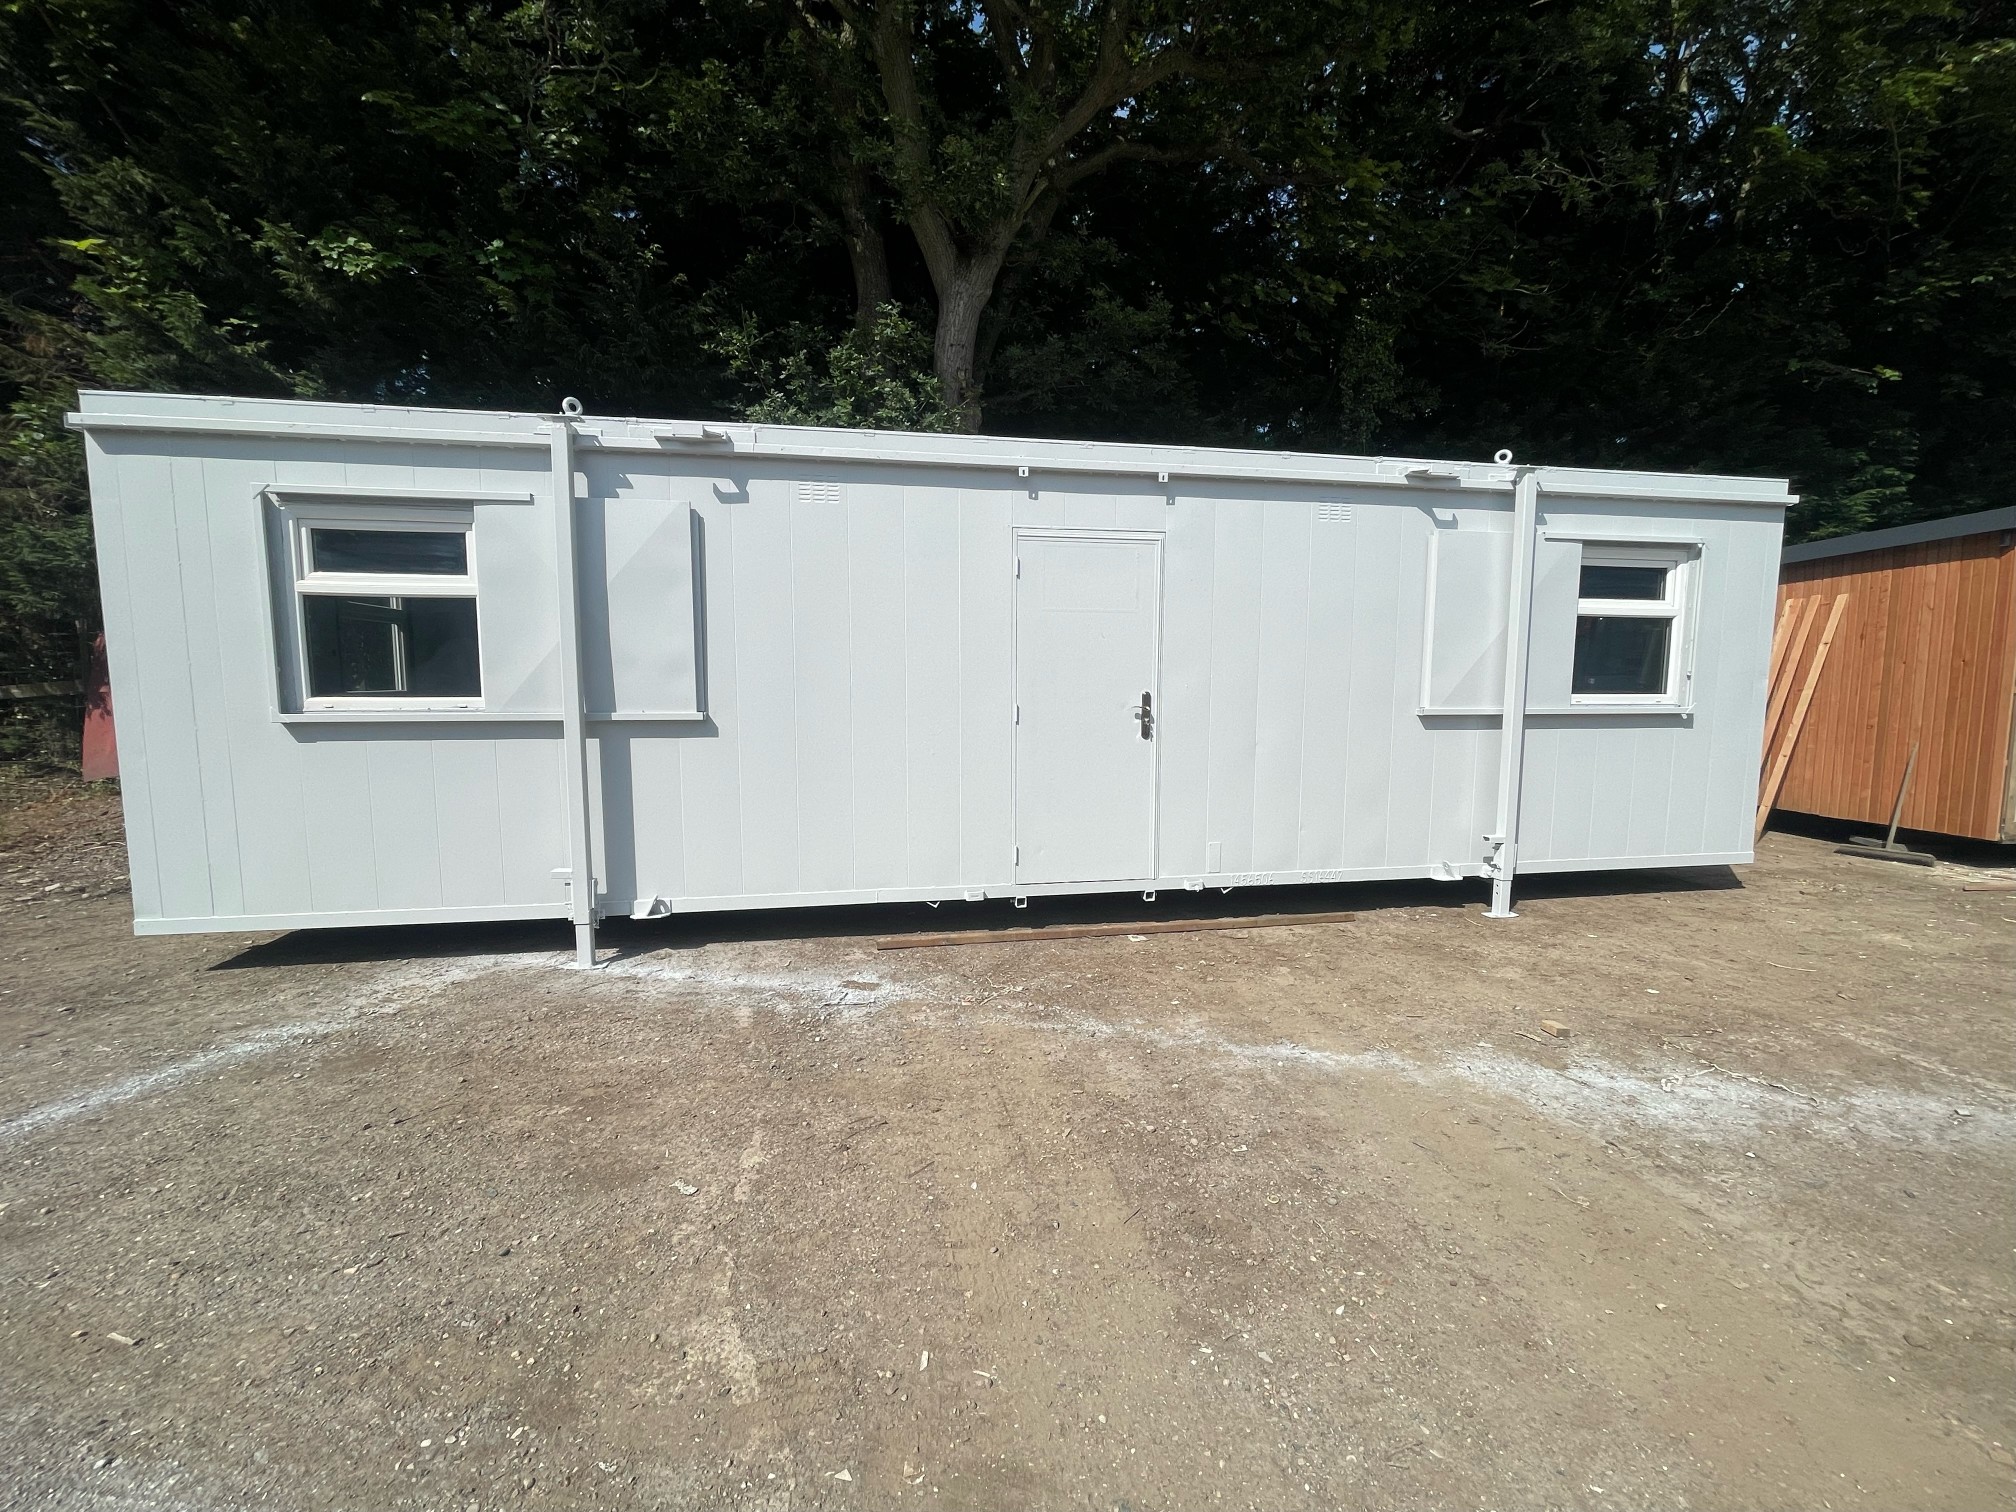
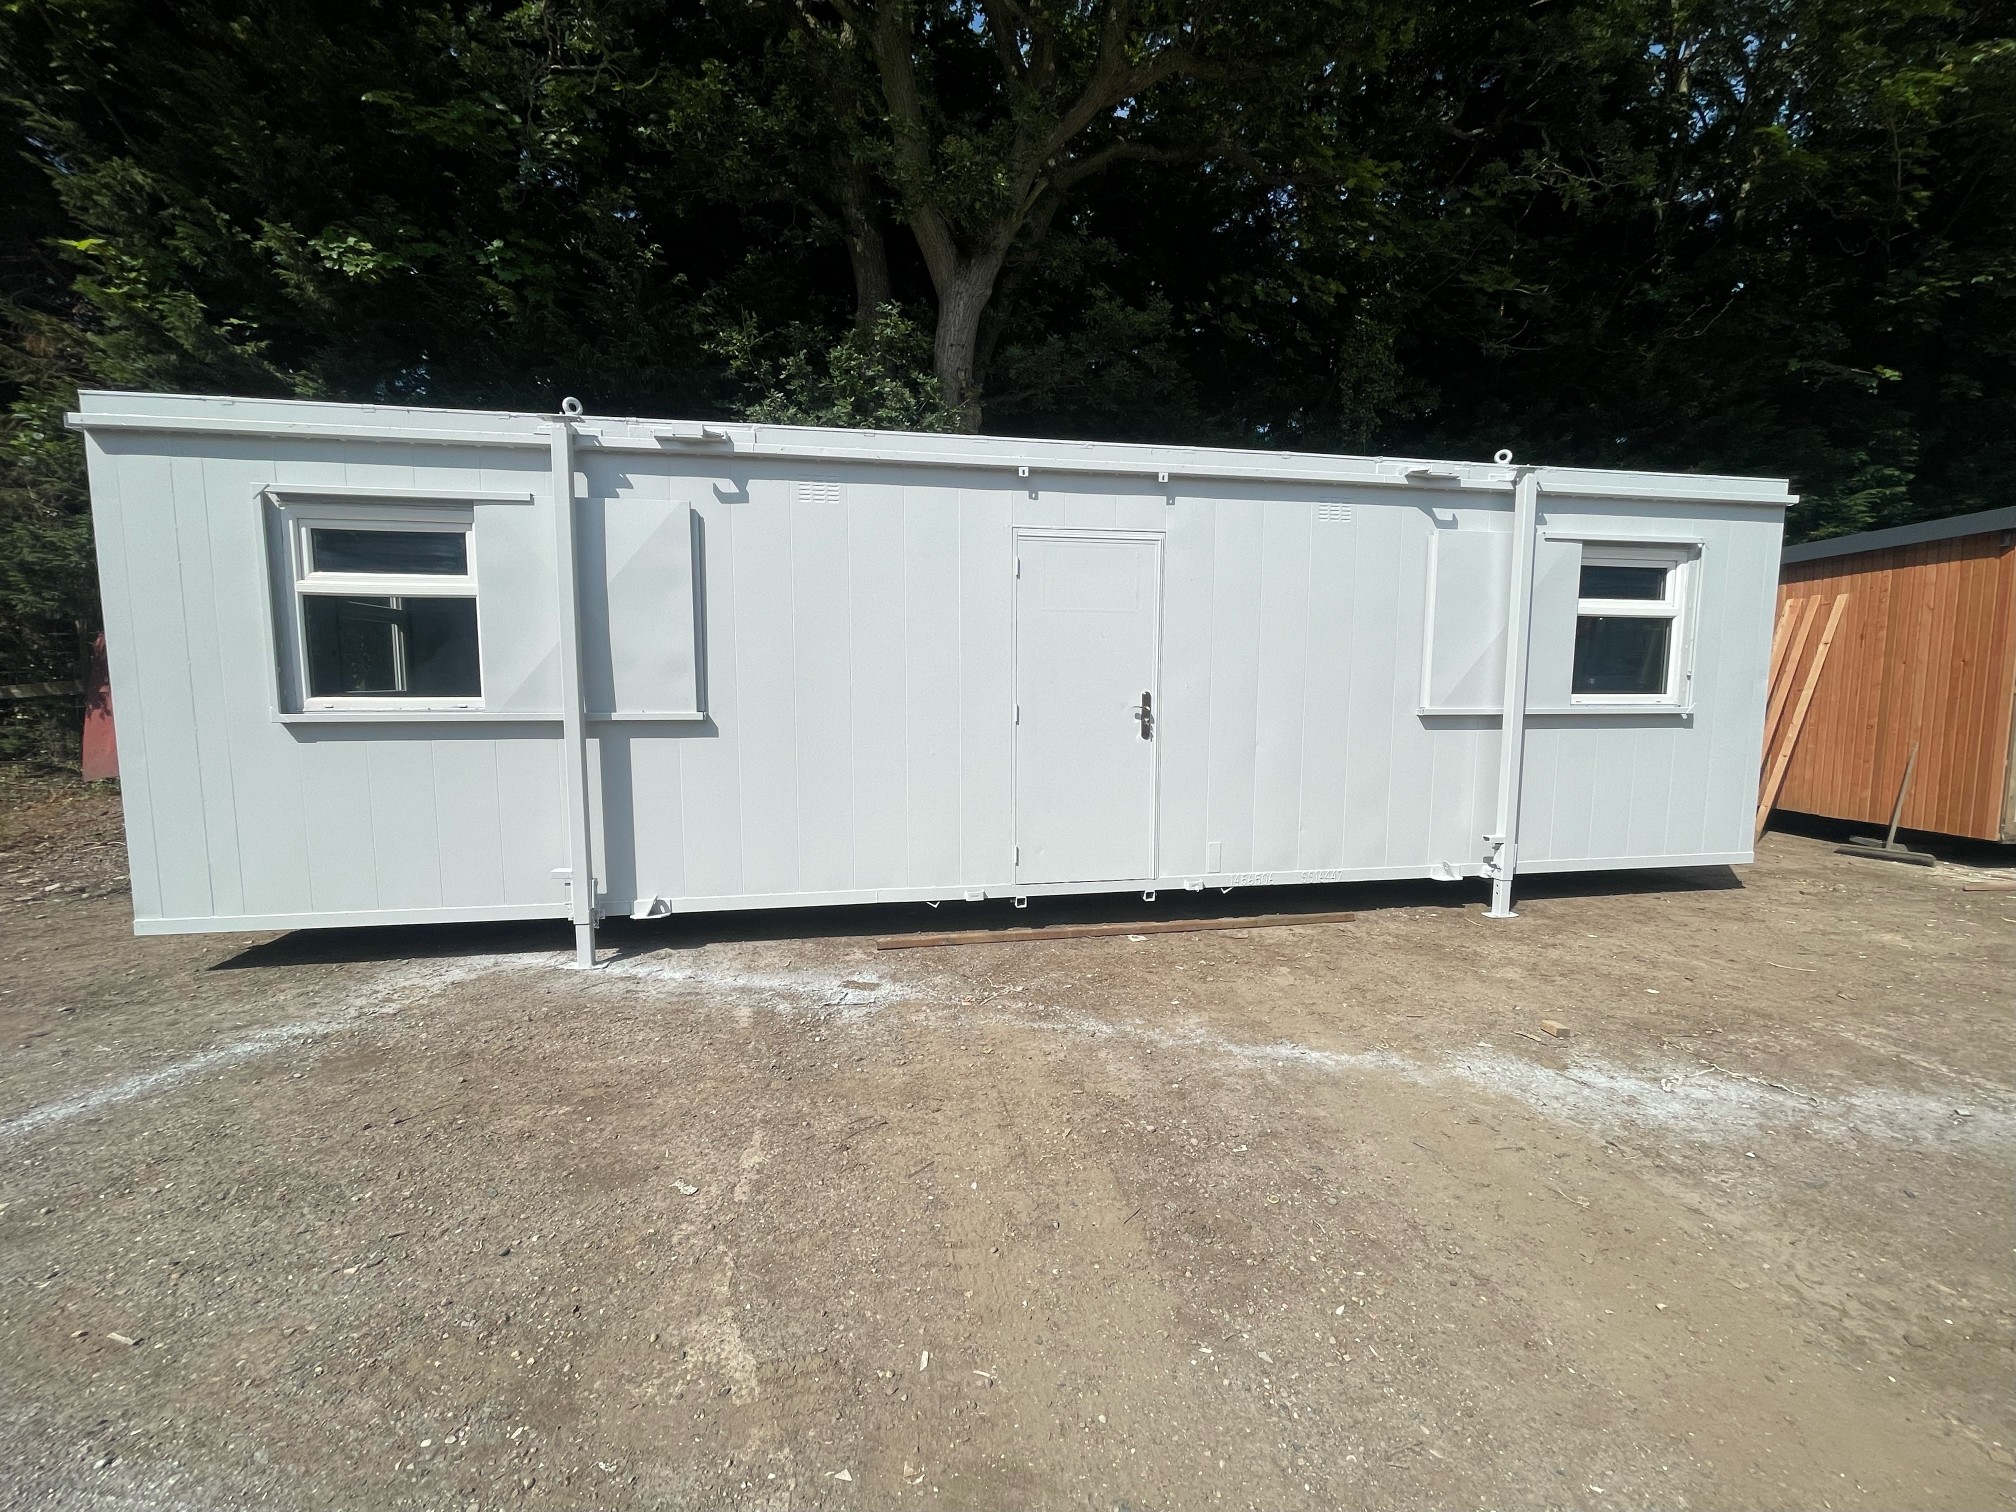
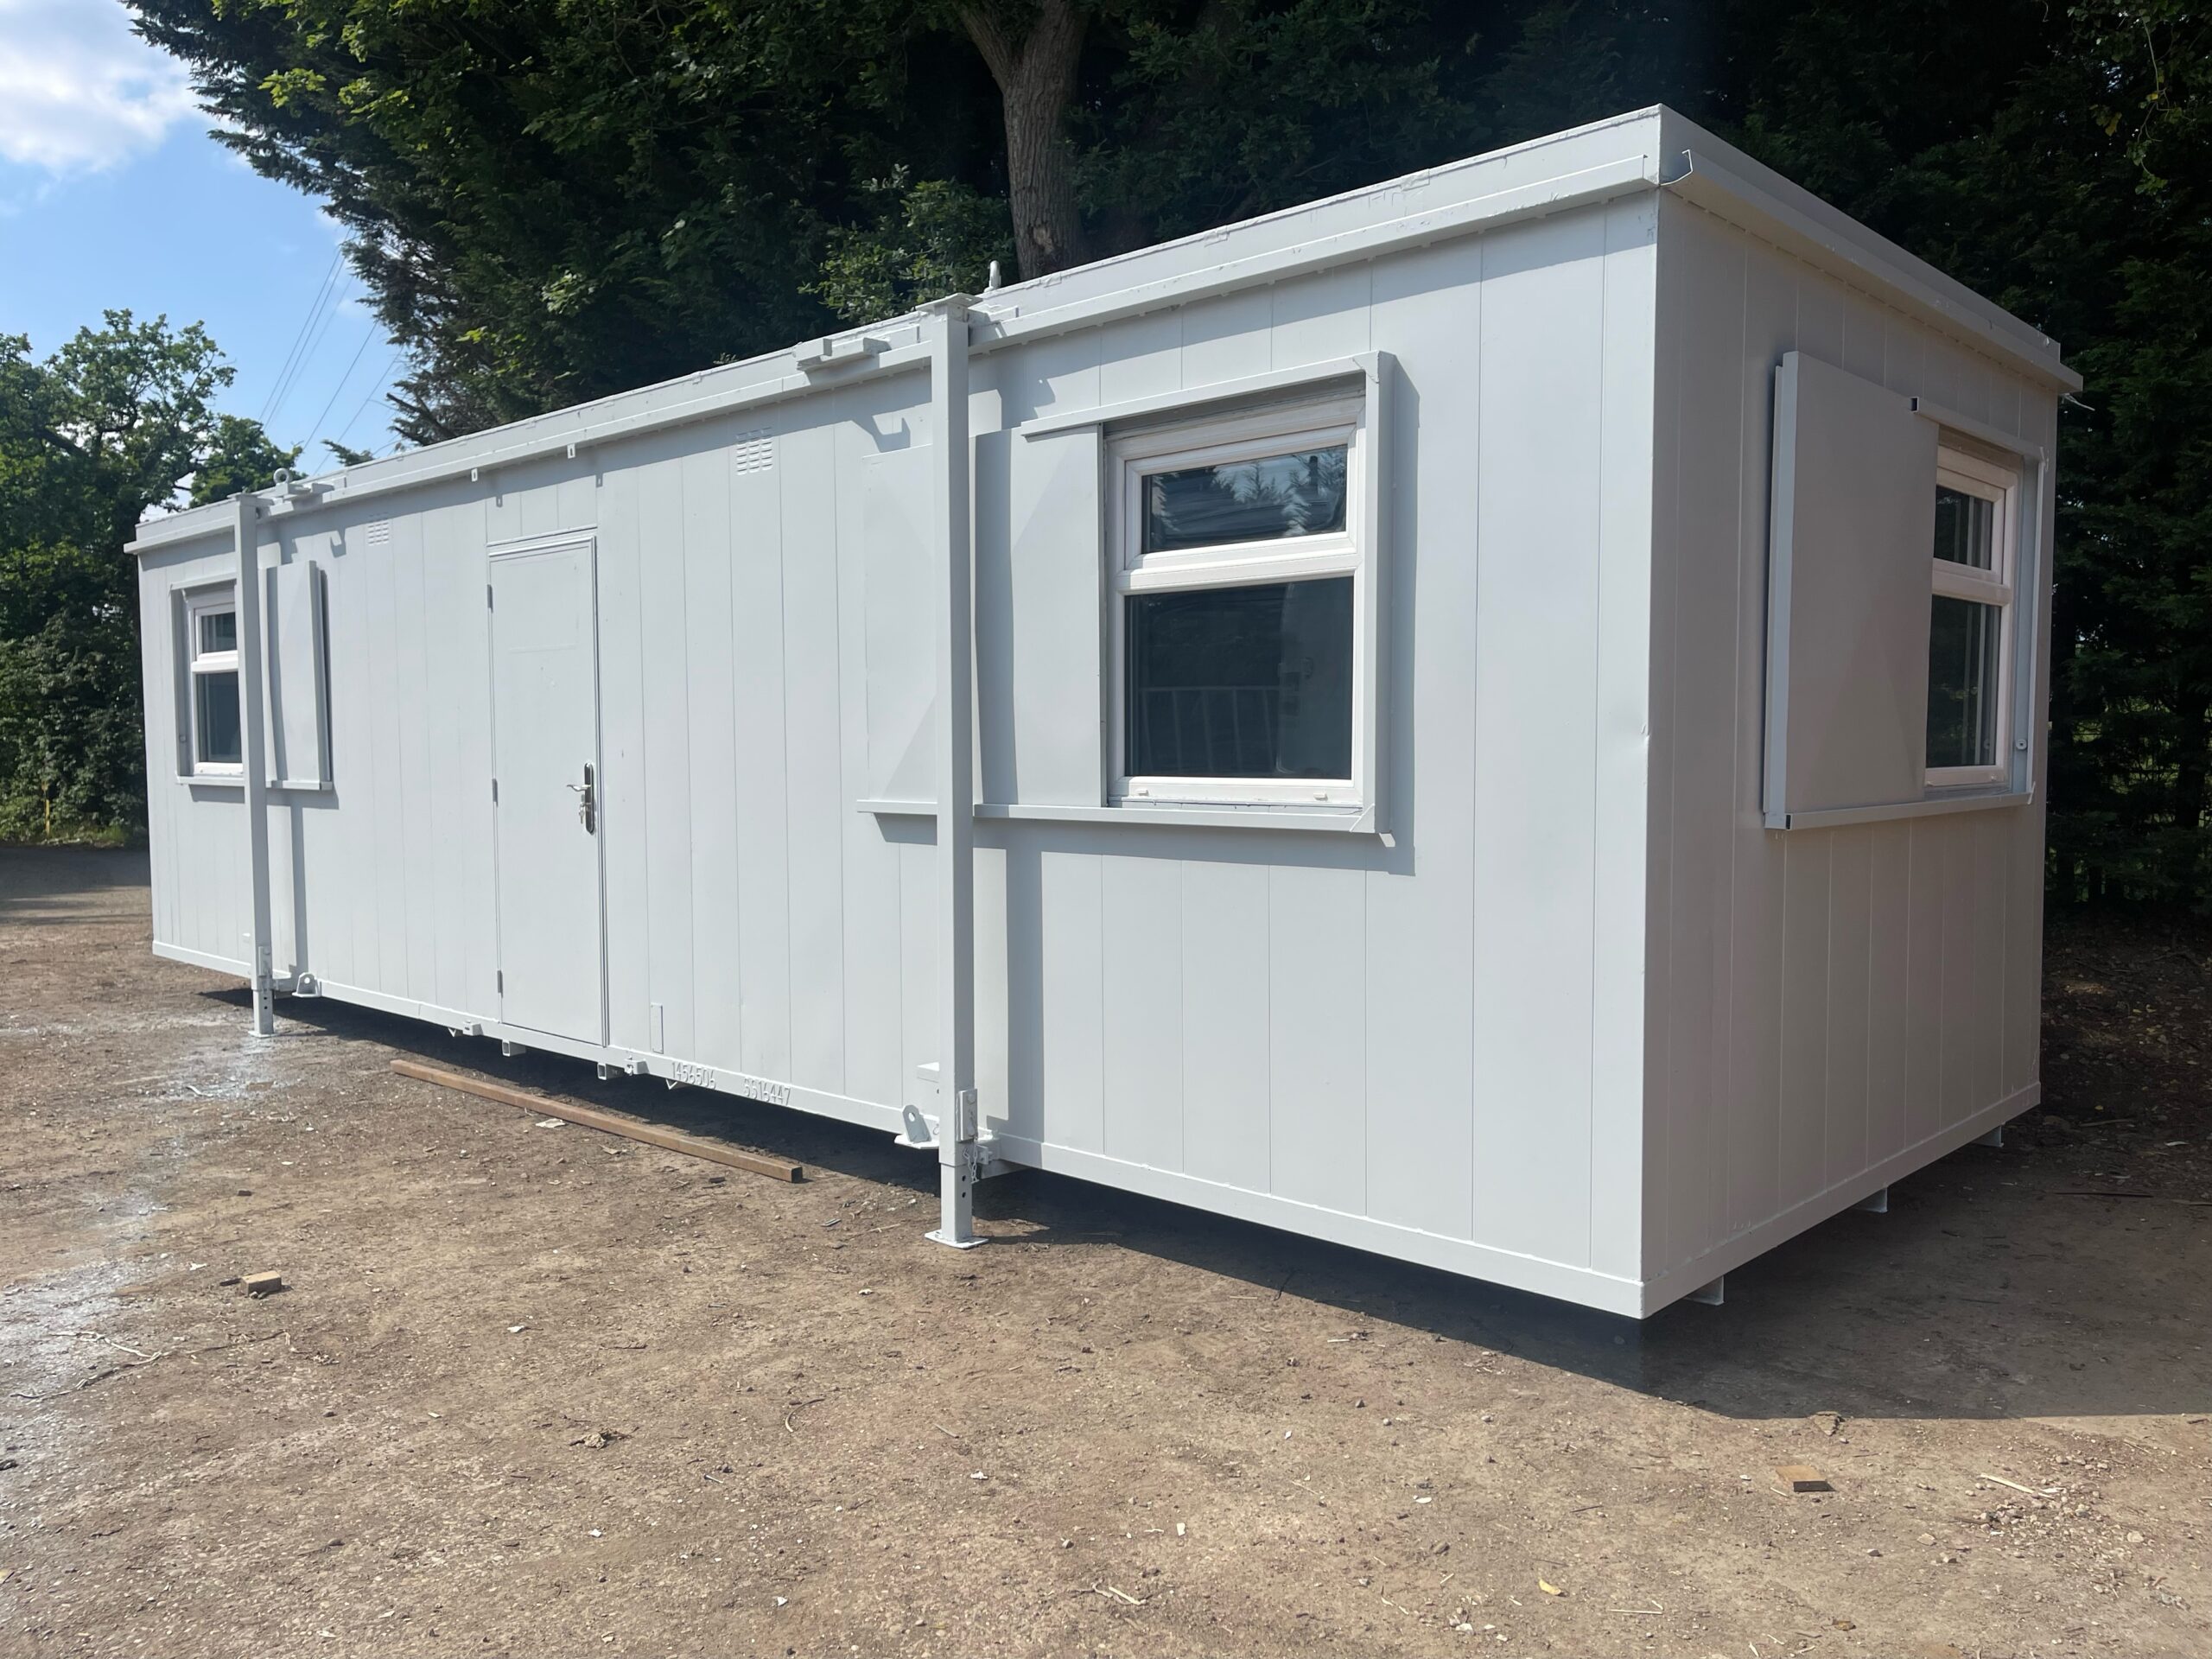
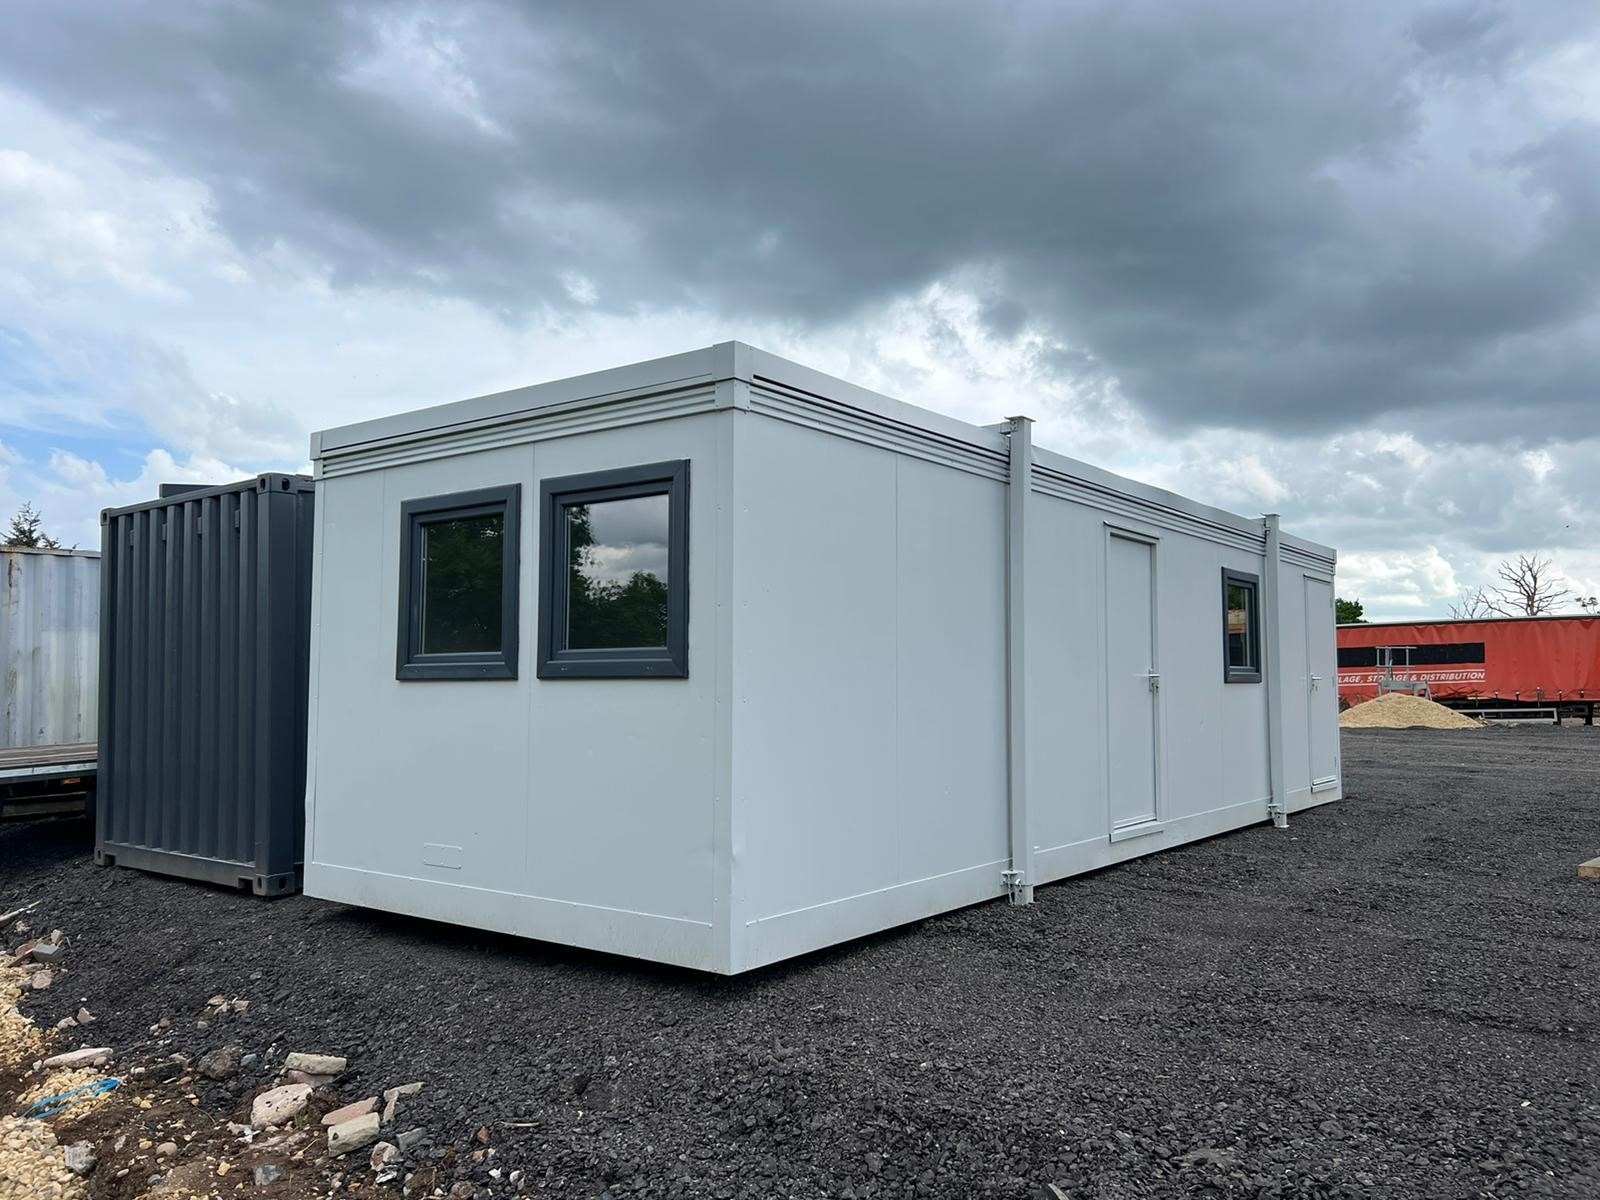
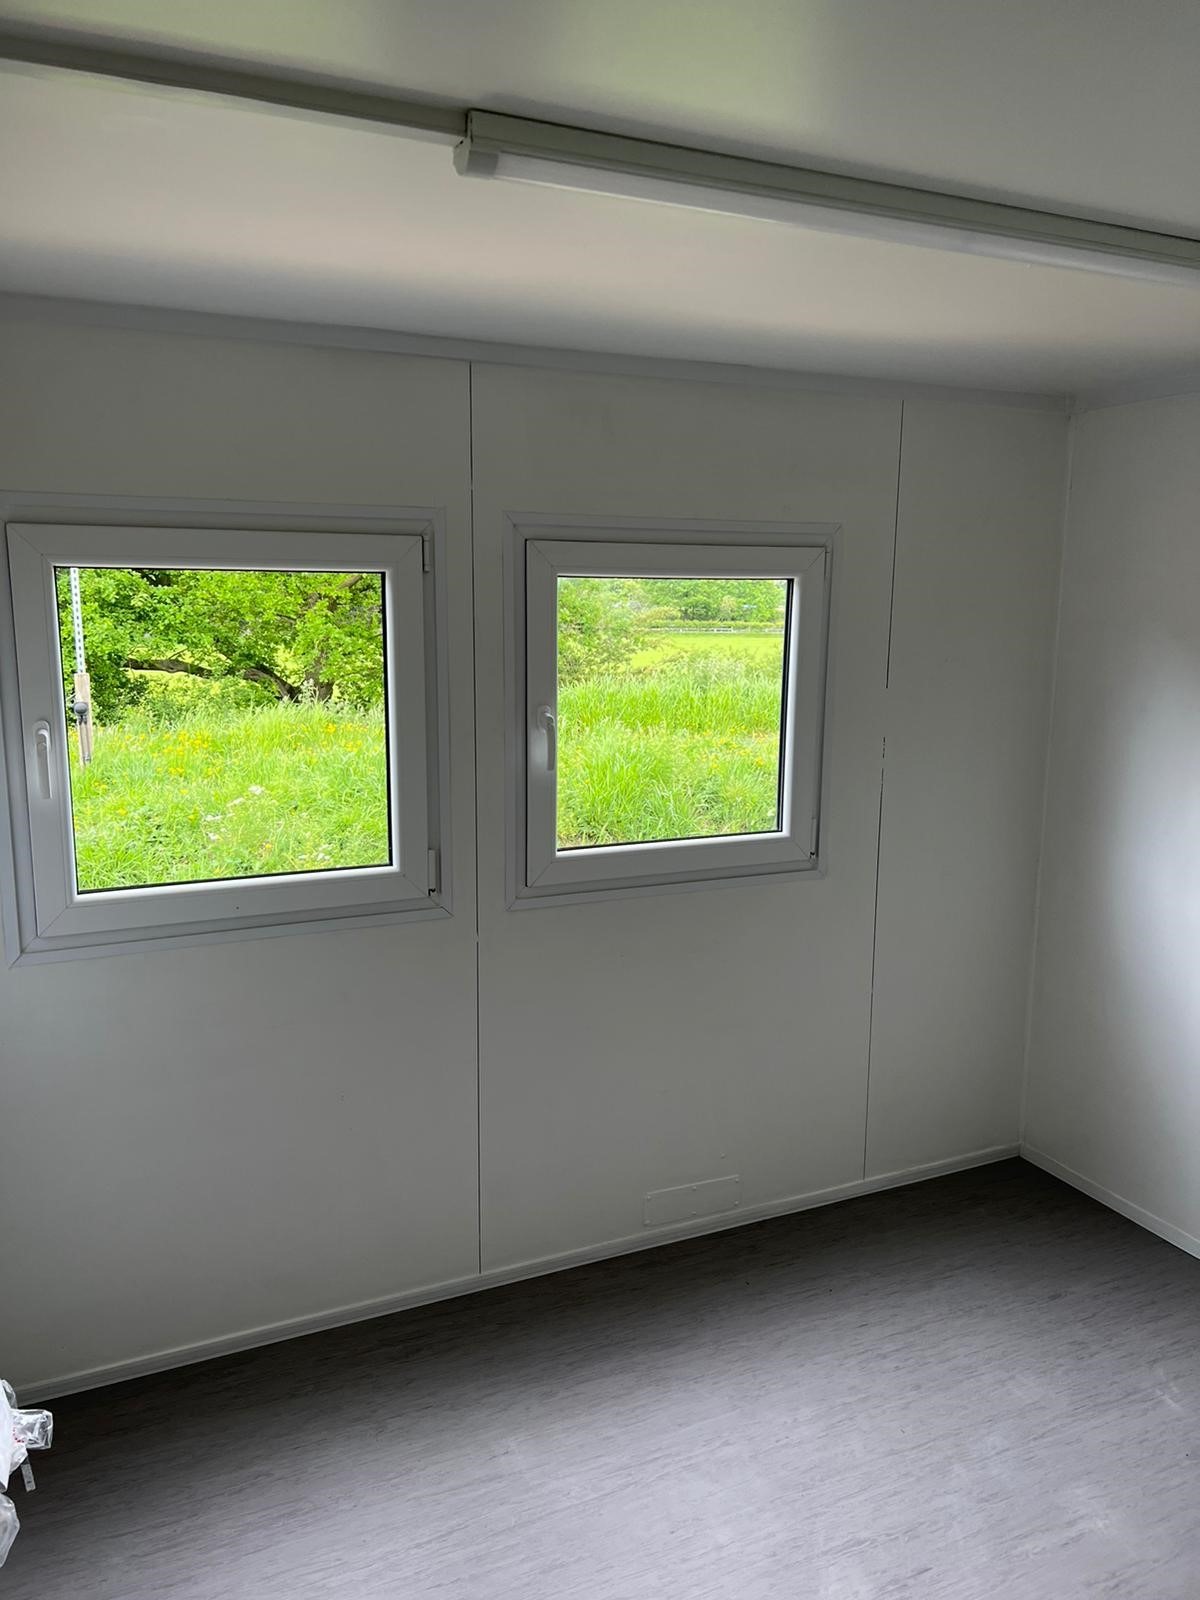
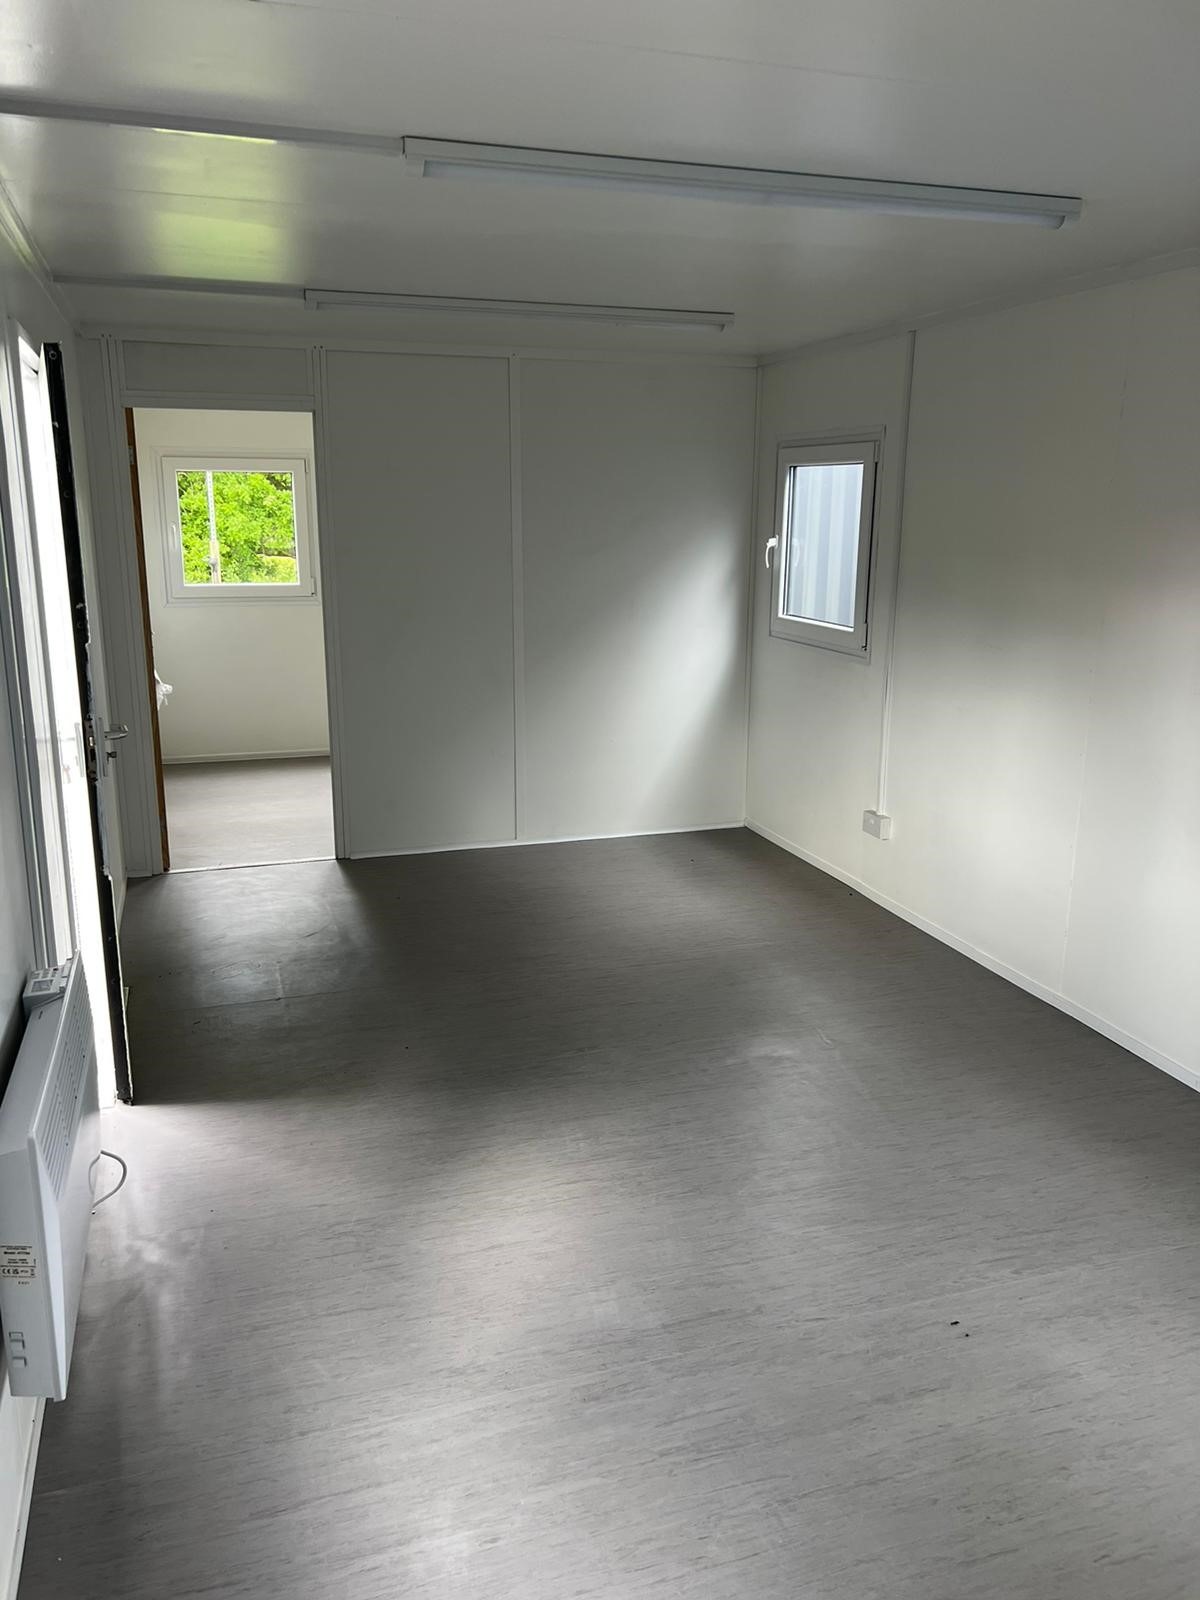
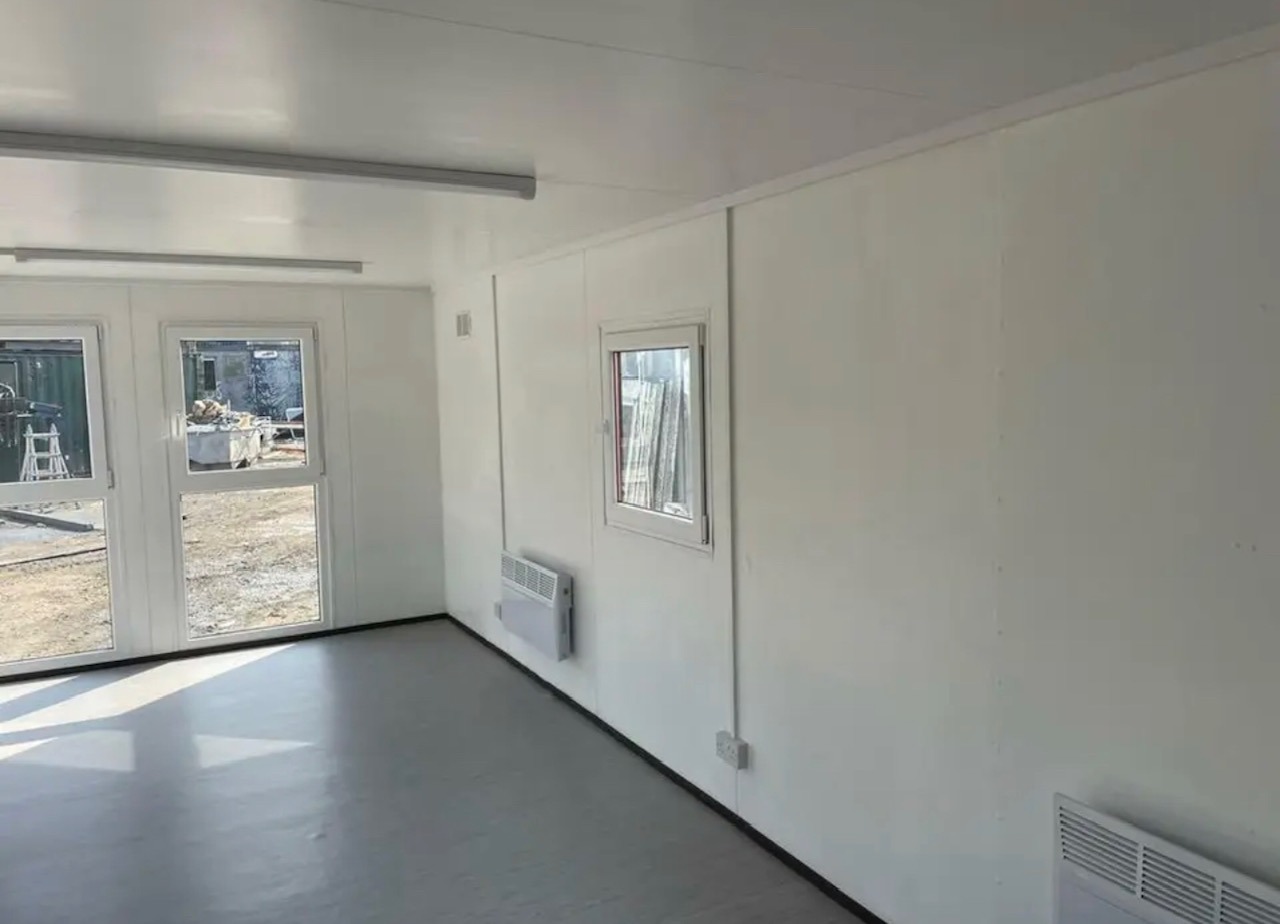
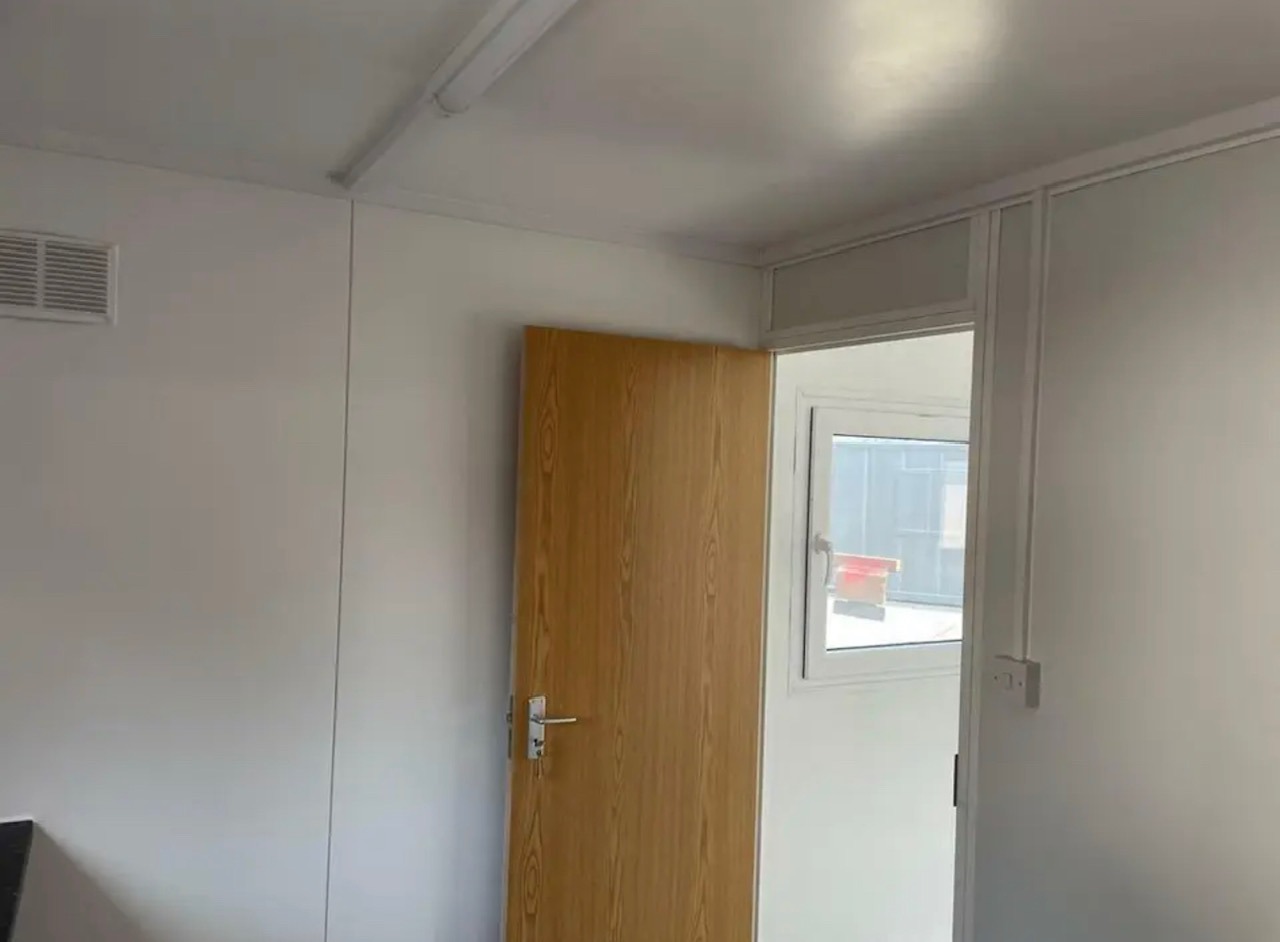
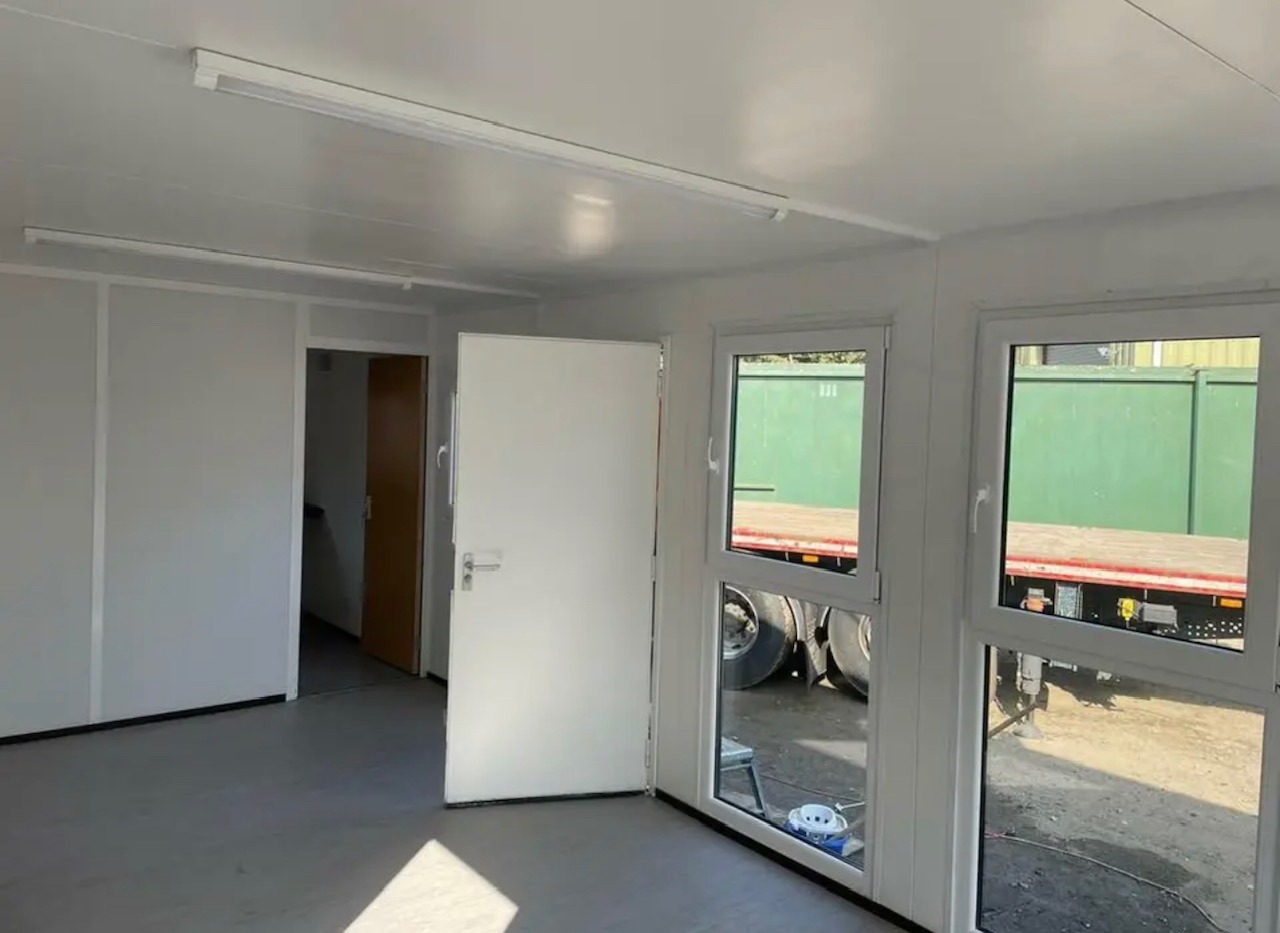
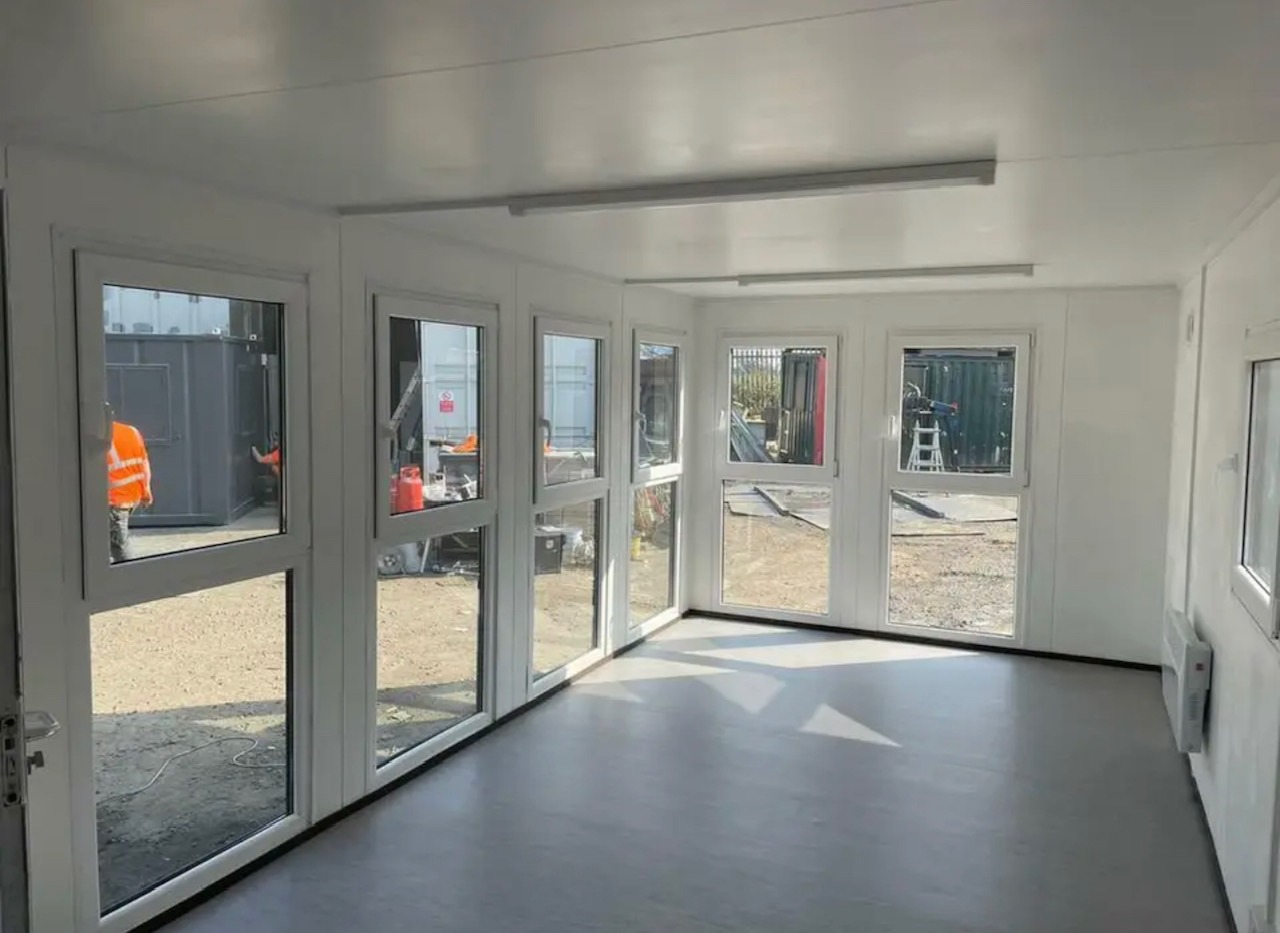
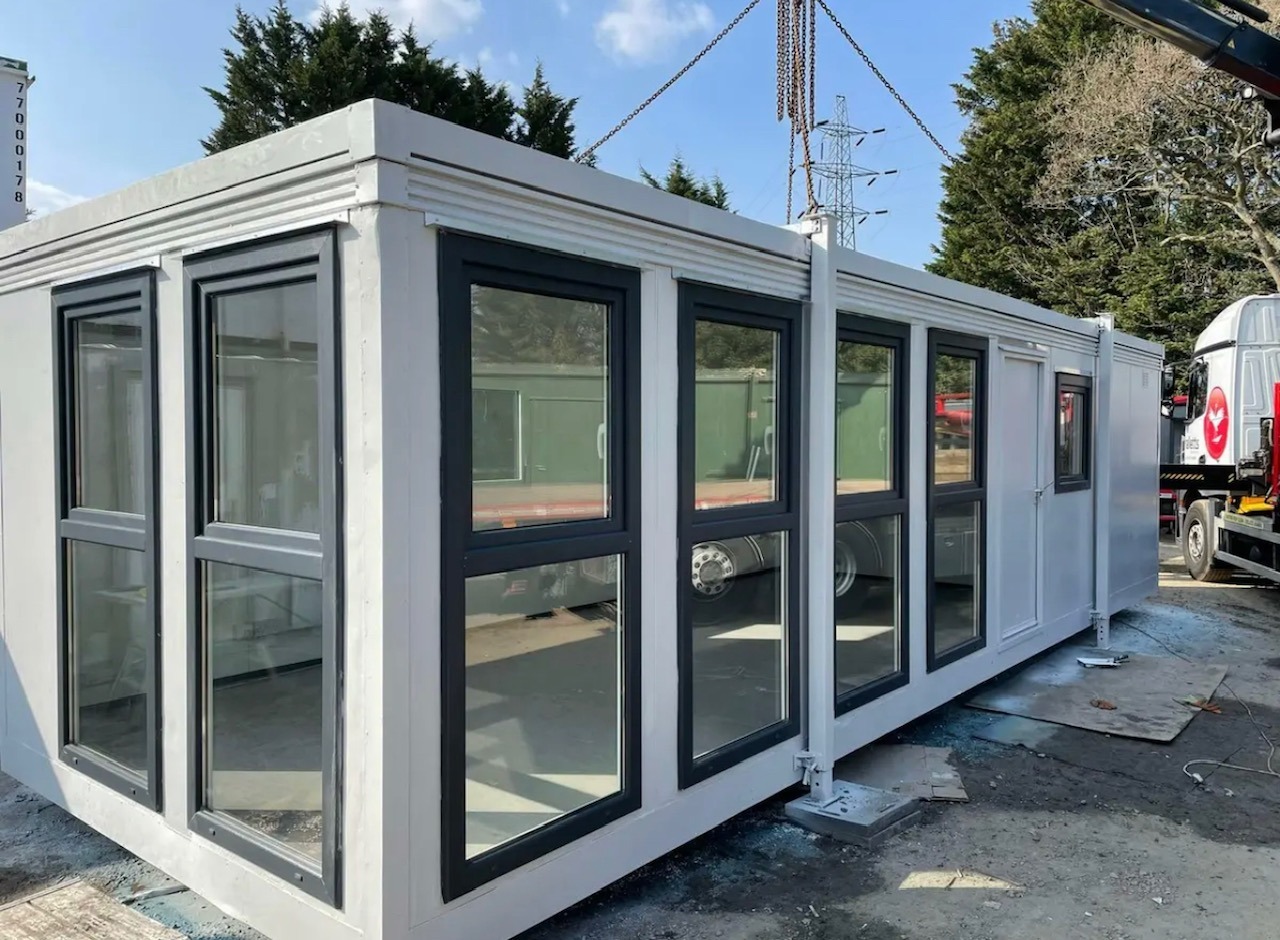
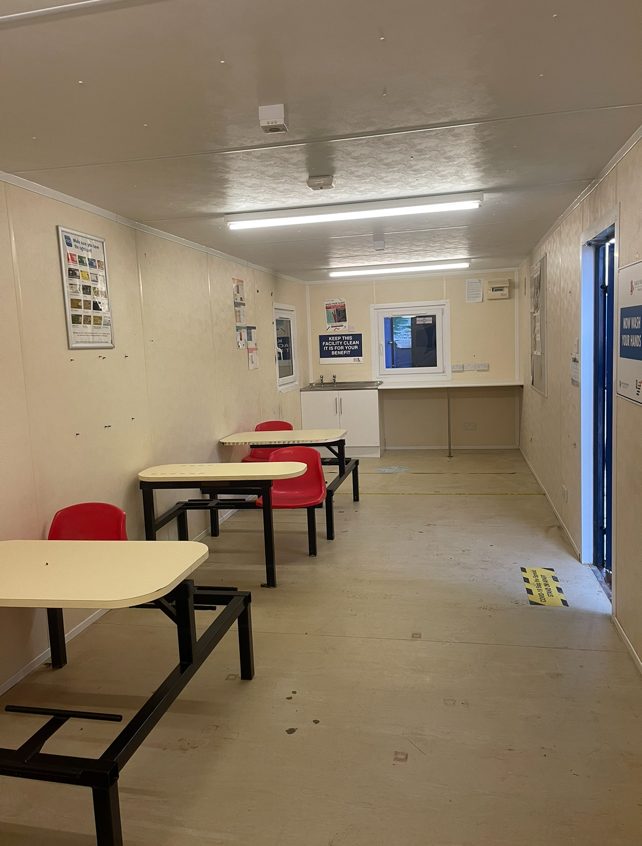
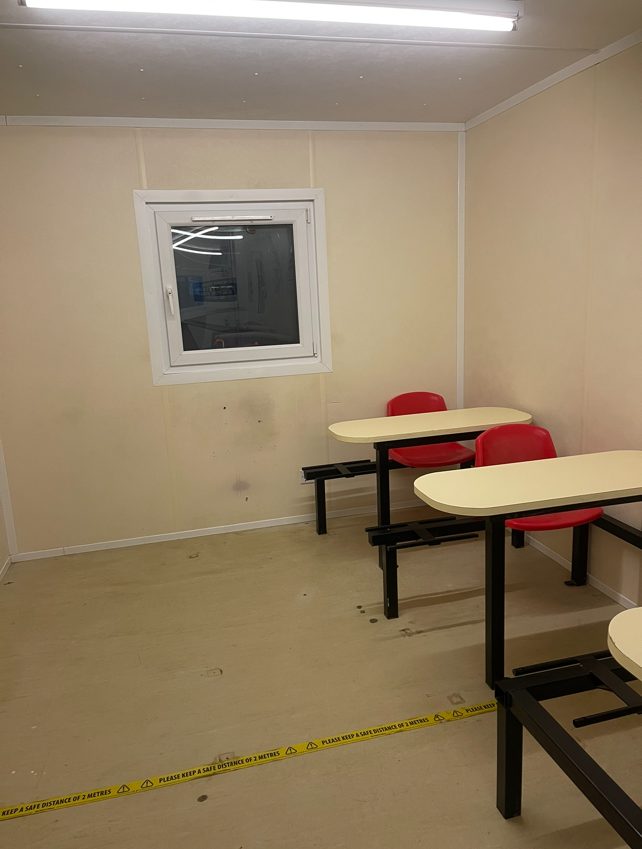
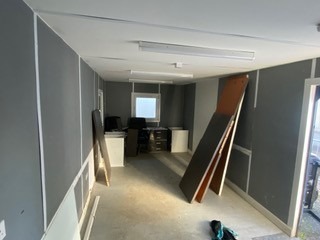
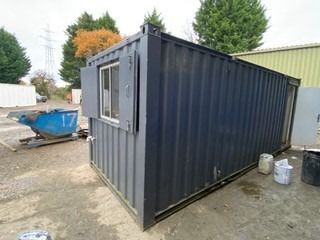
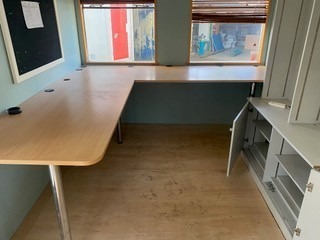
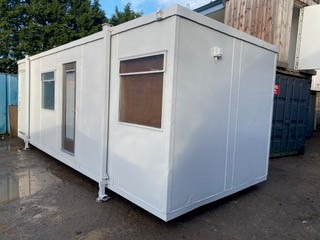
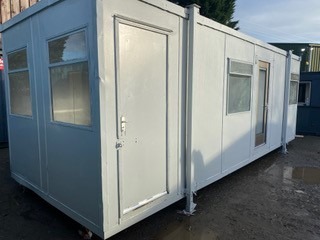
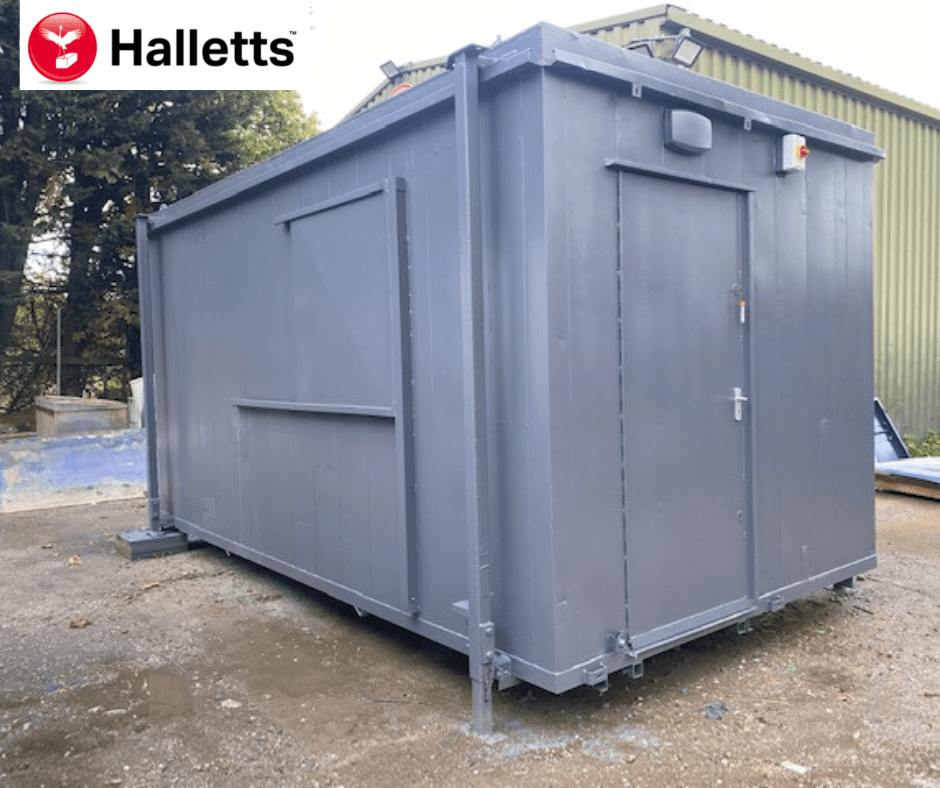
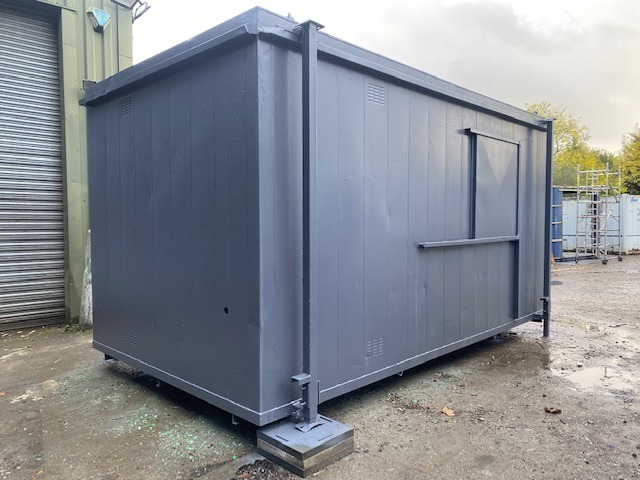
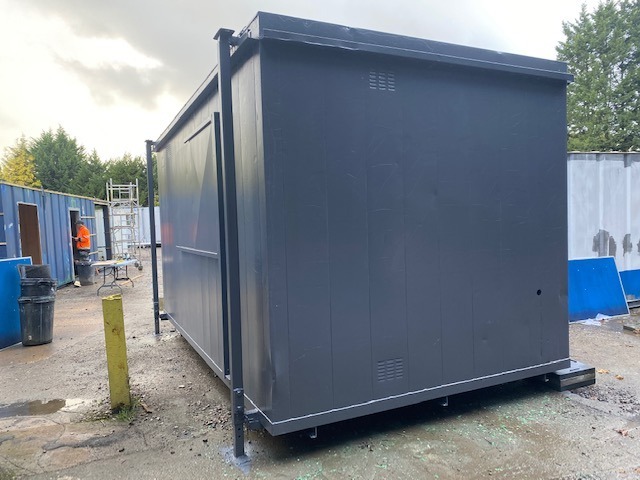
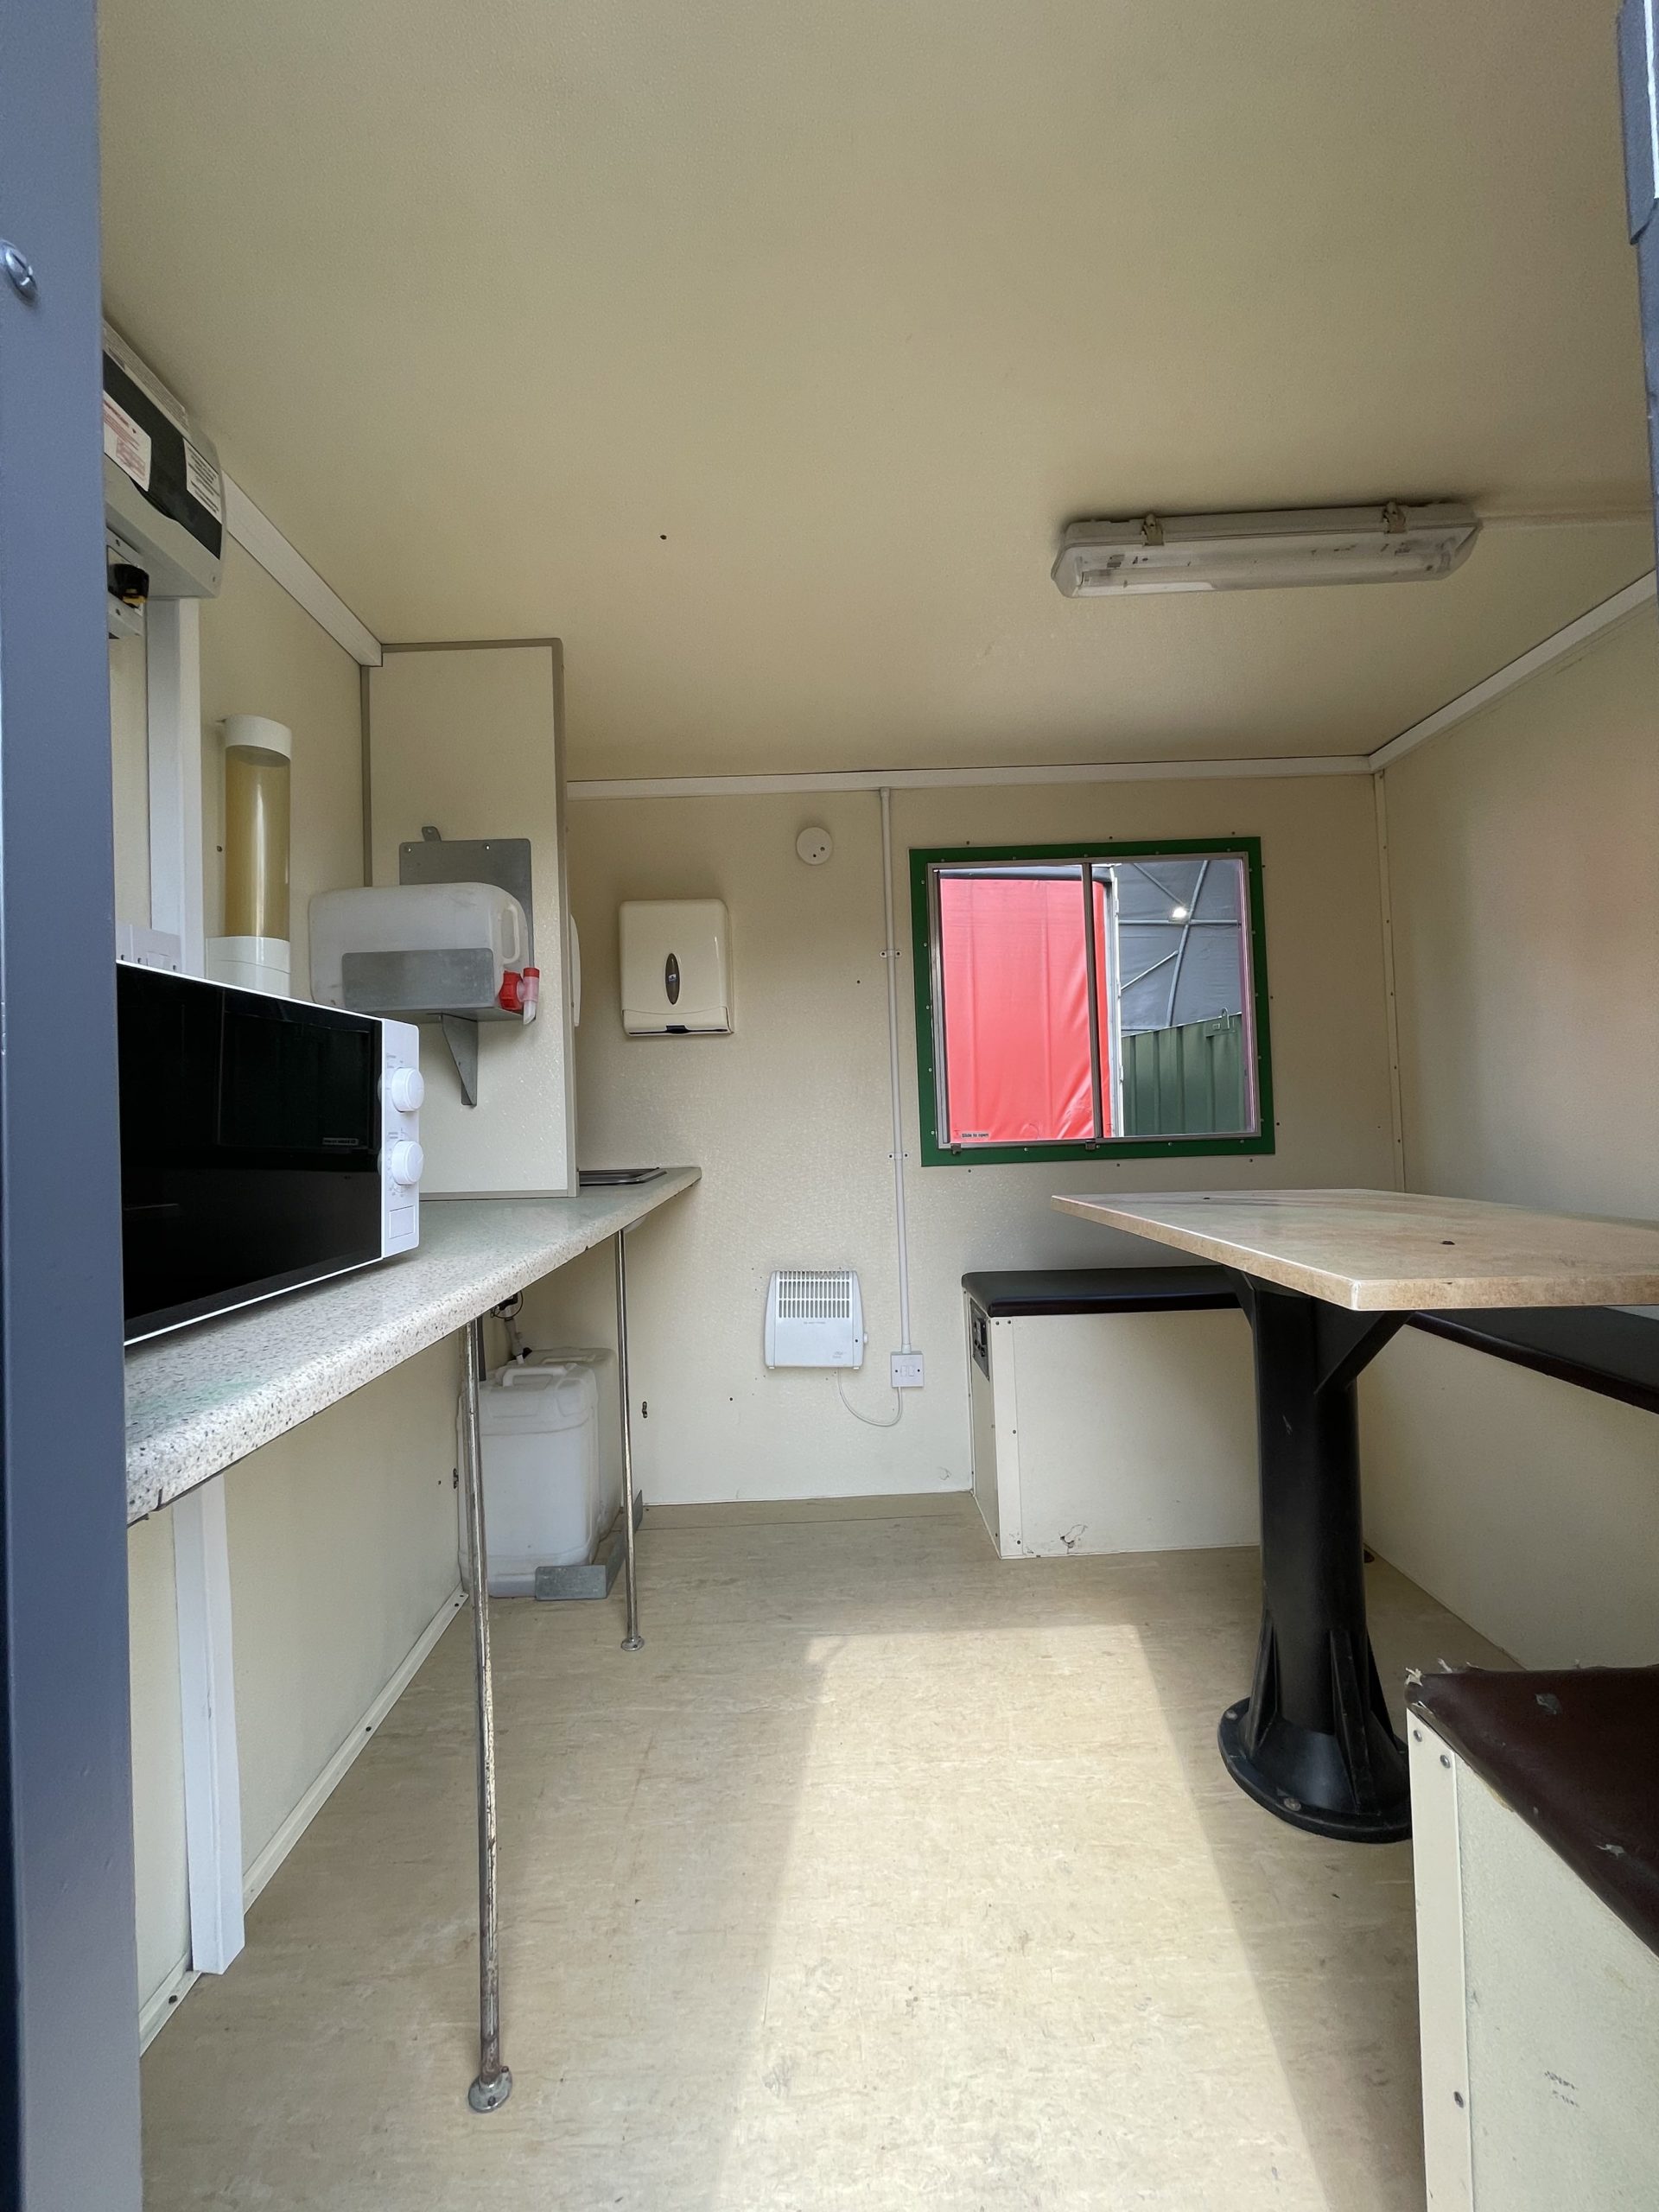
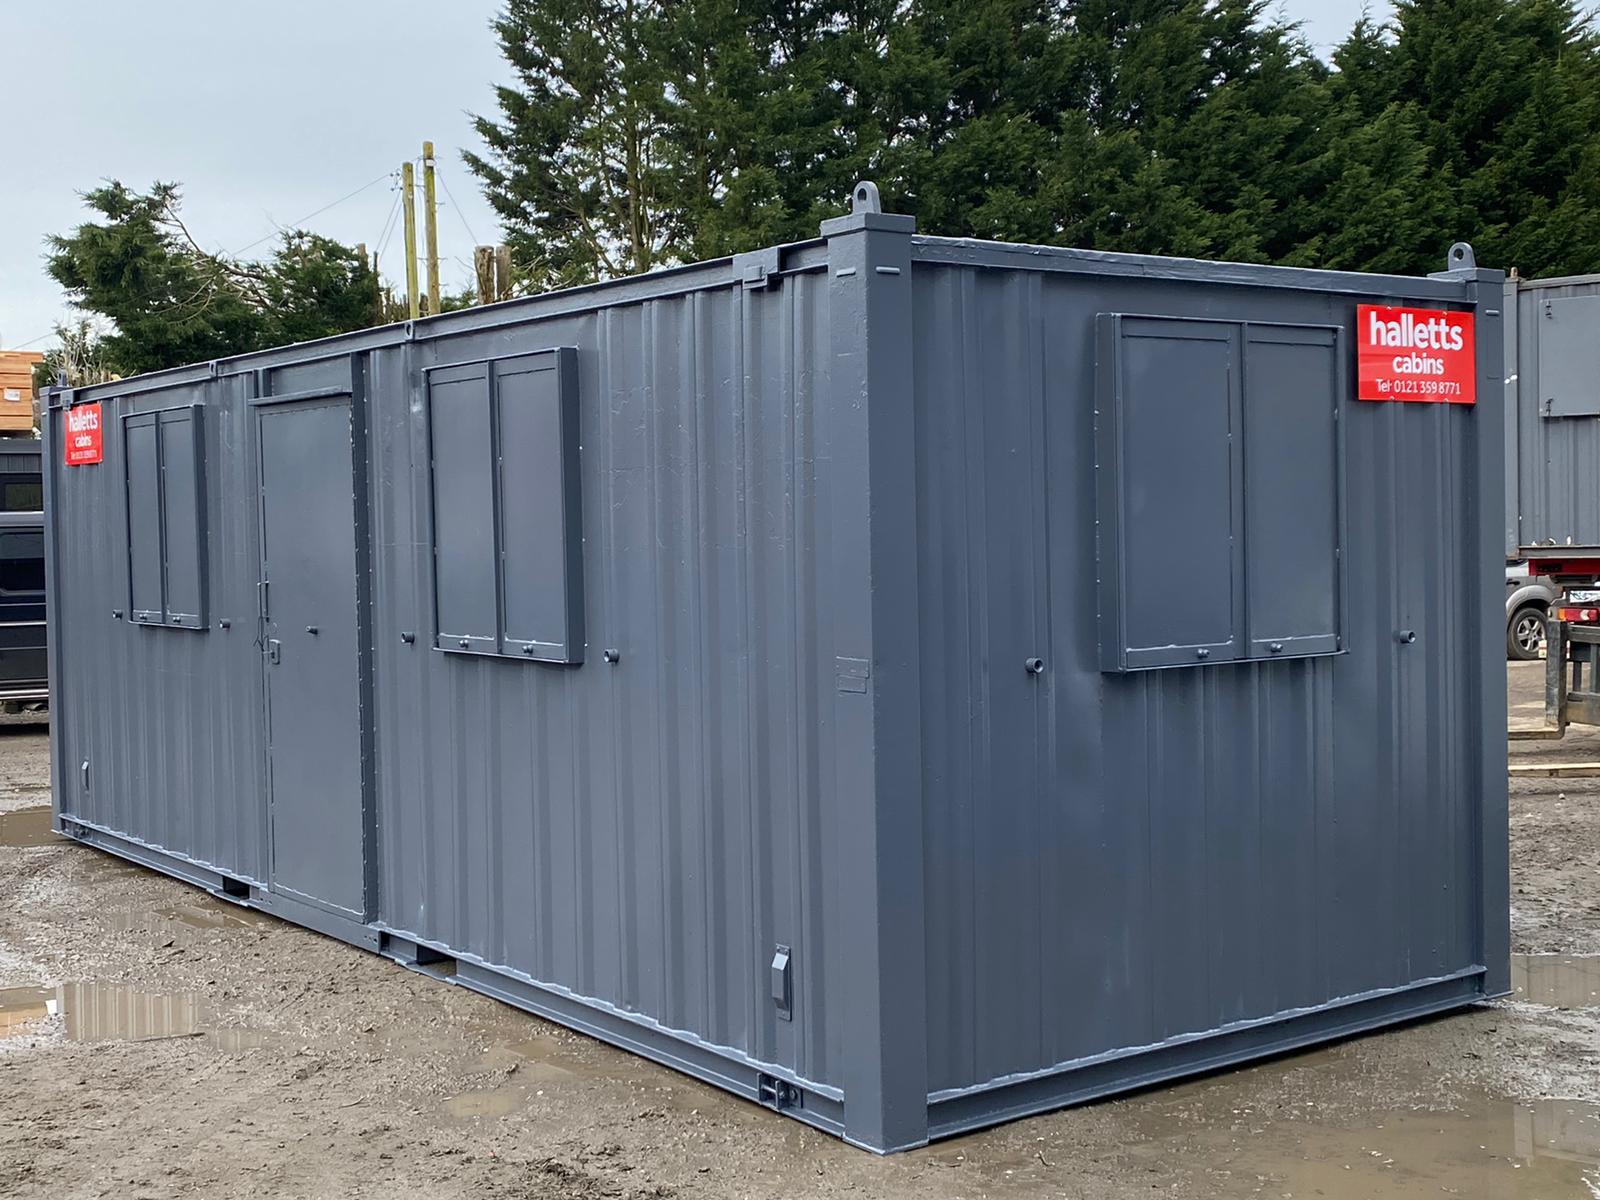
32ft x 10ft Anti Vandal Canteen/Office

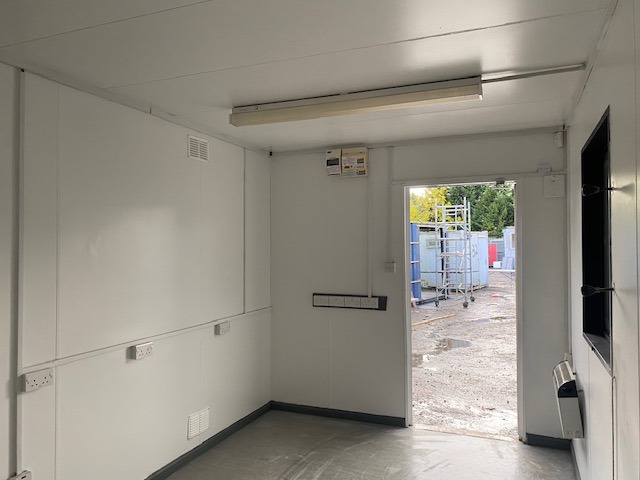
  • Complete with tables and chairs
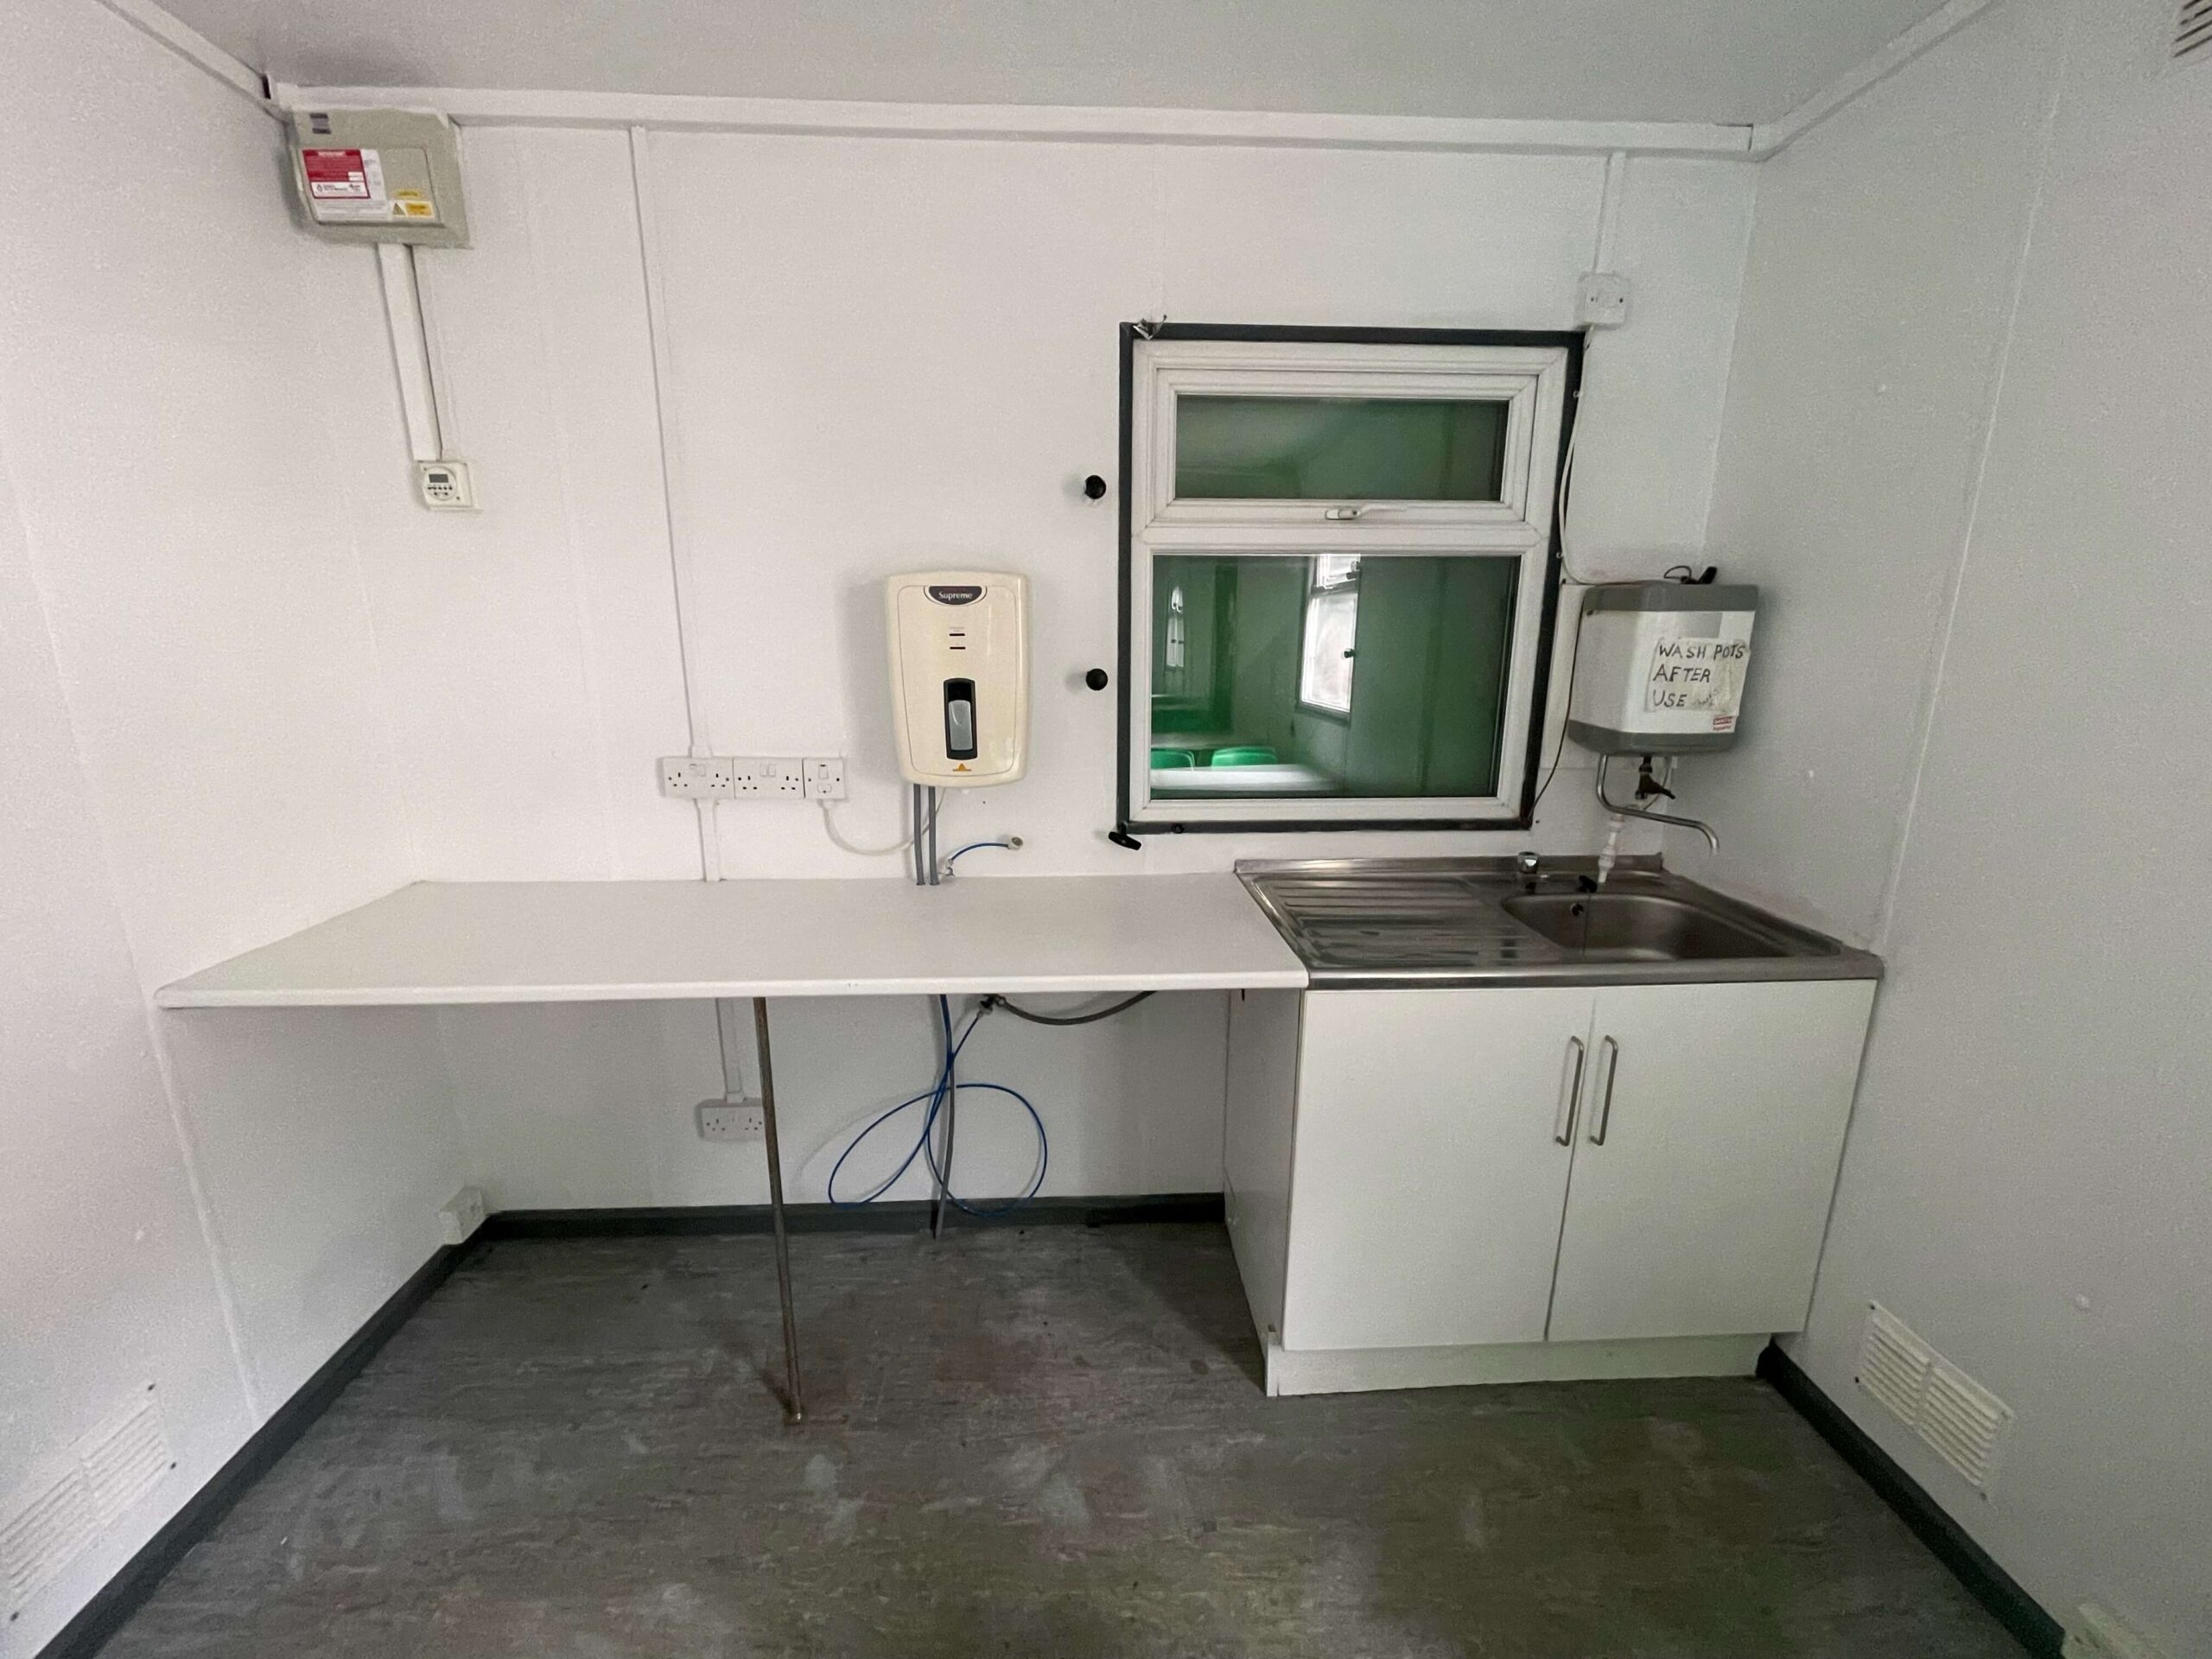
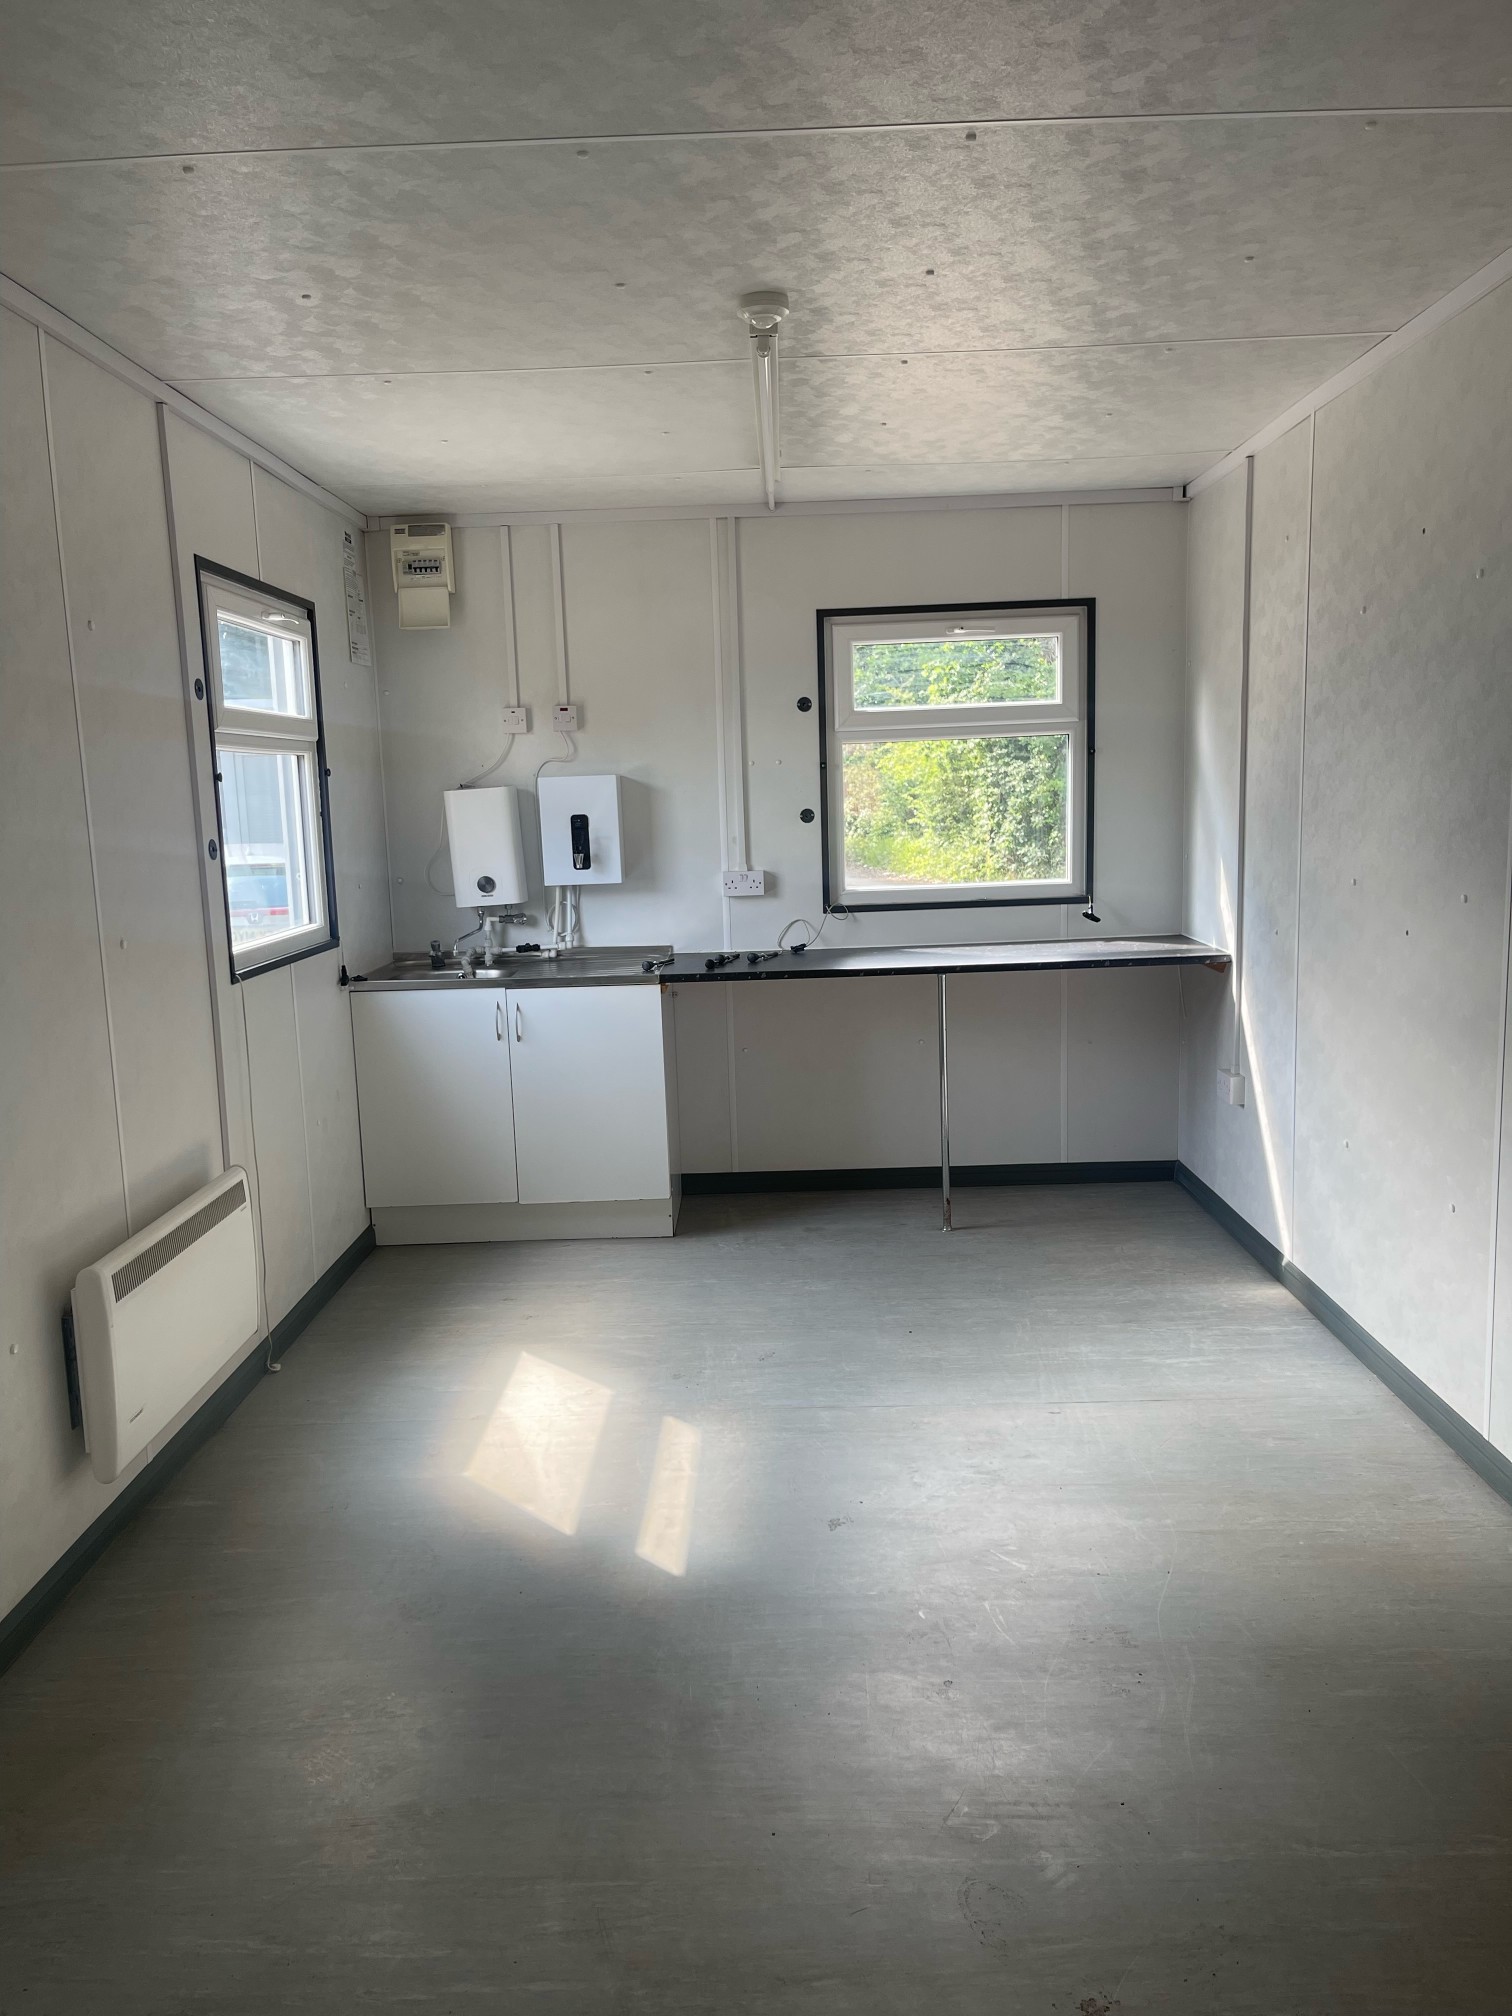
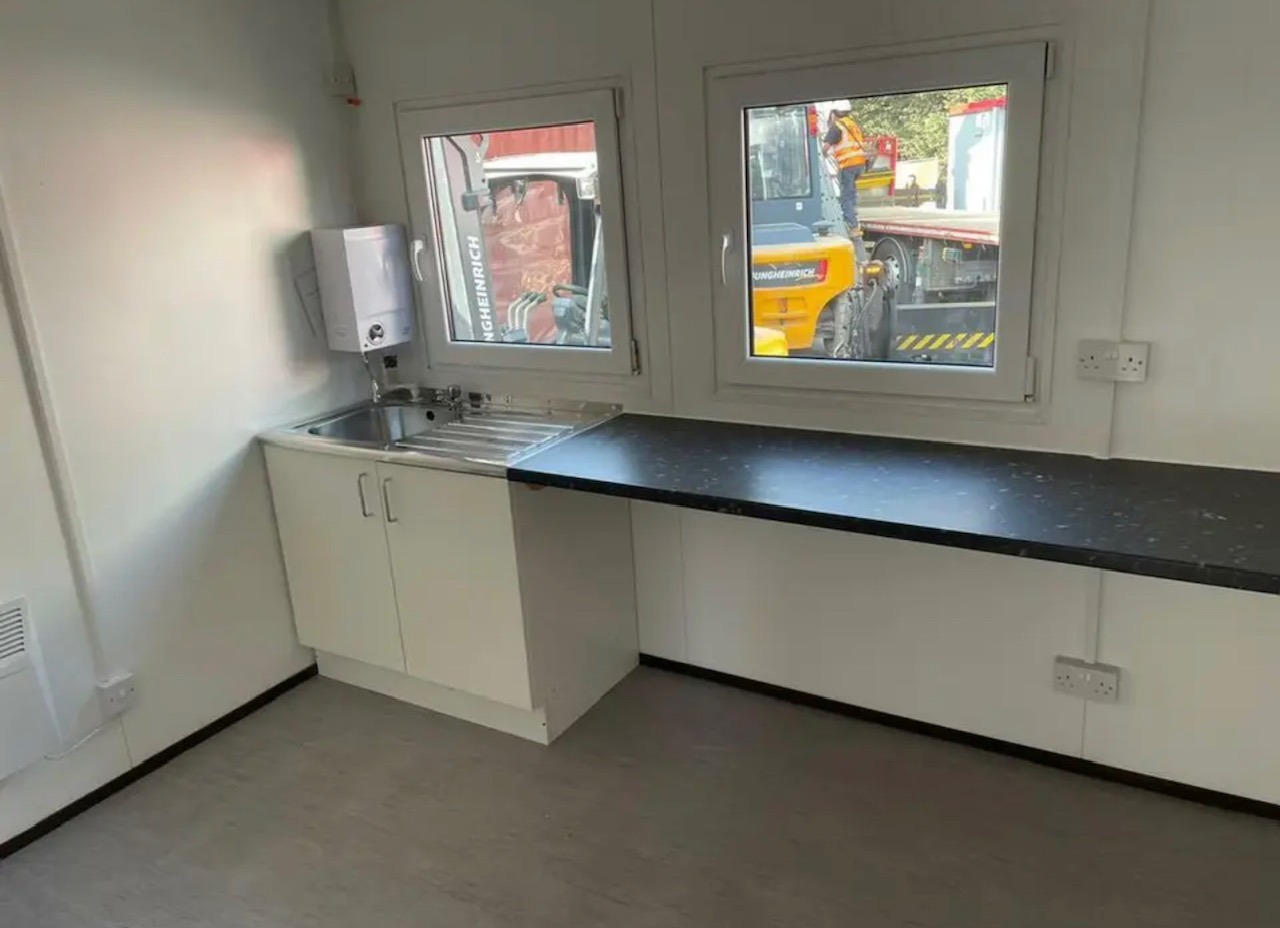
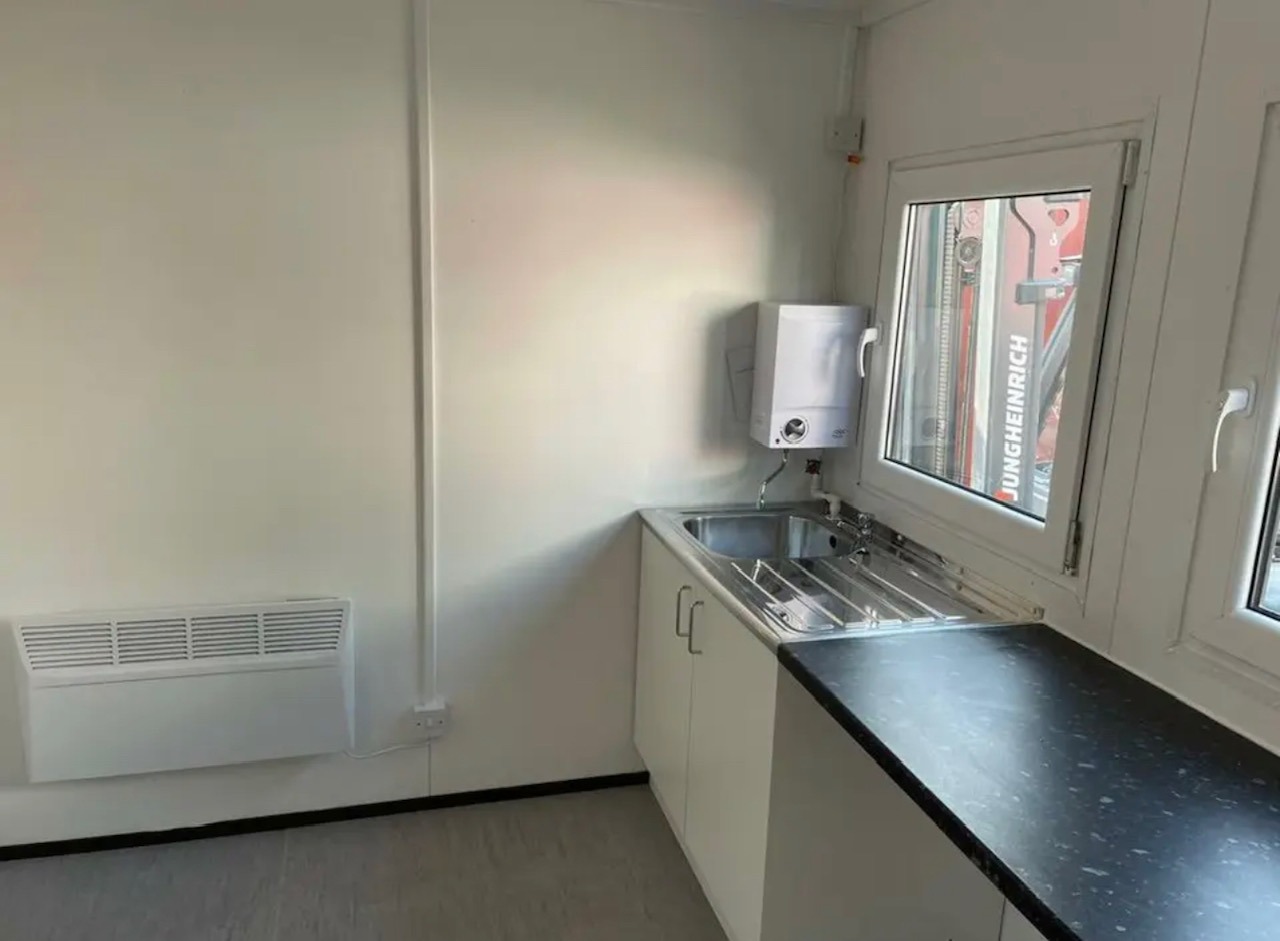
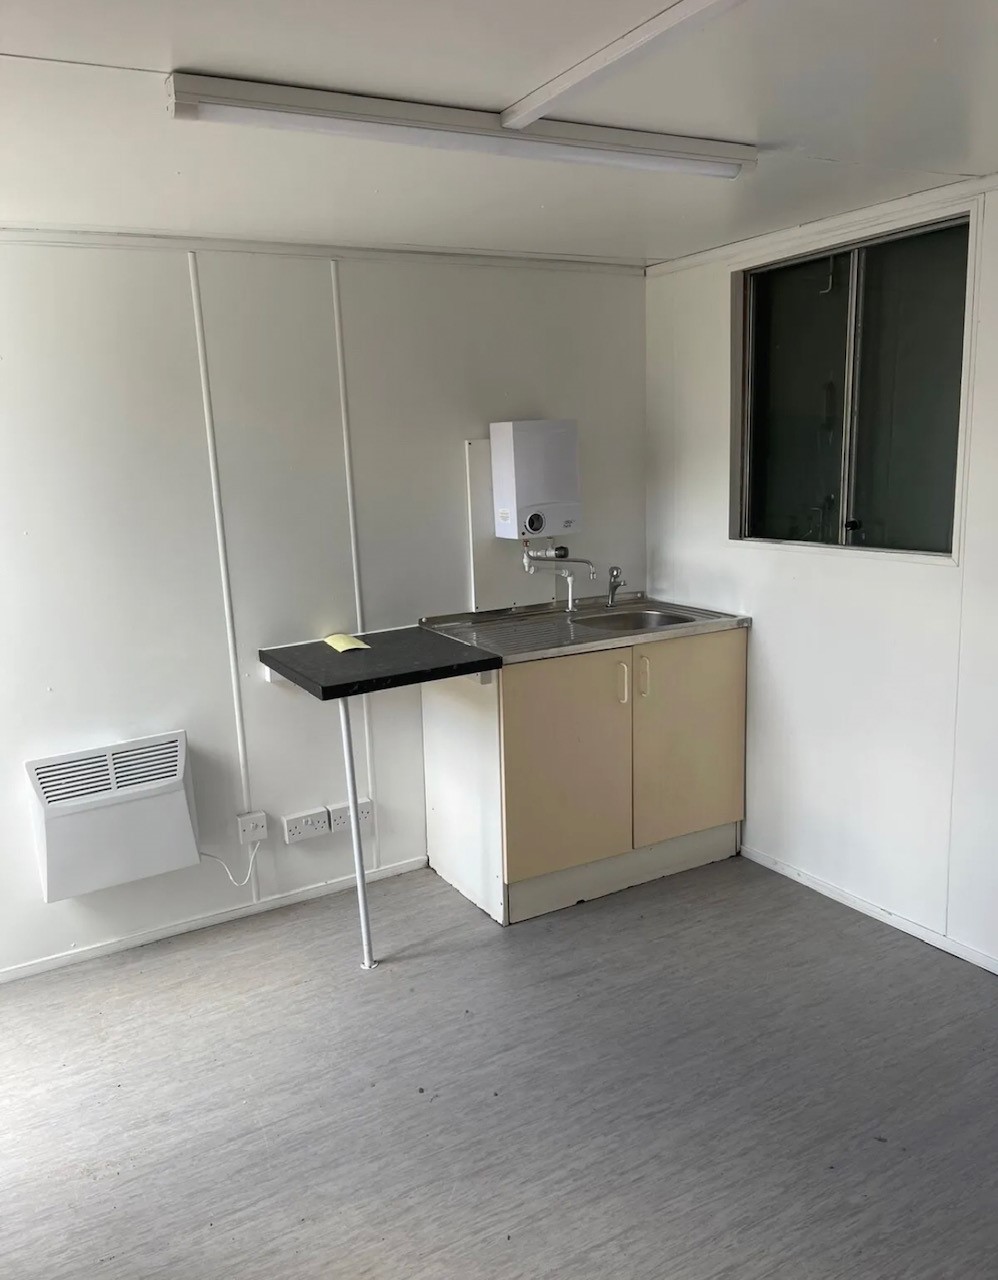
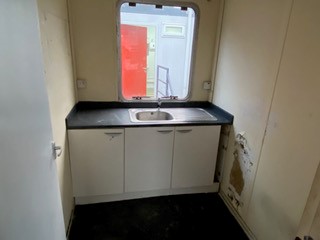
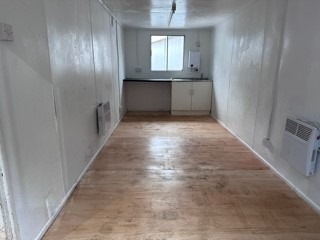
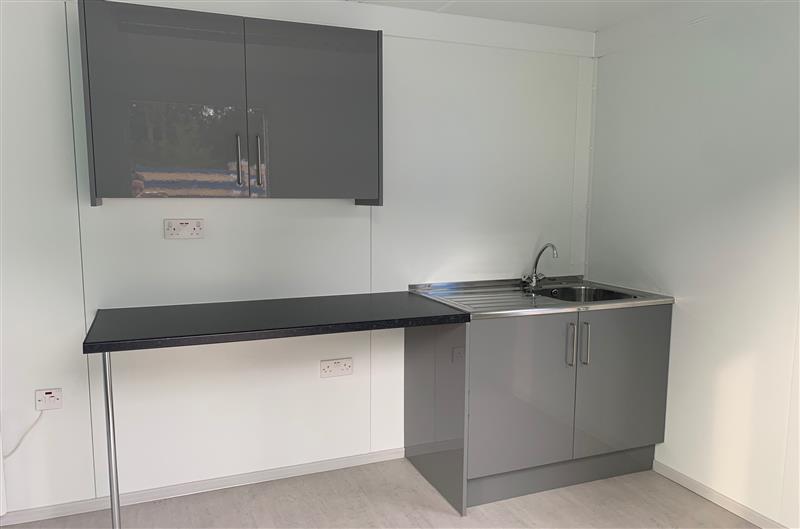
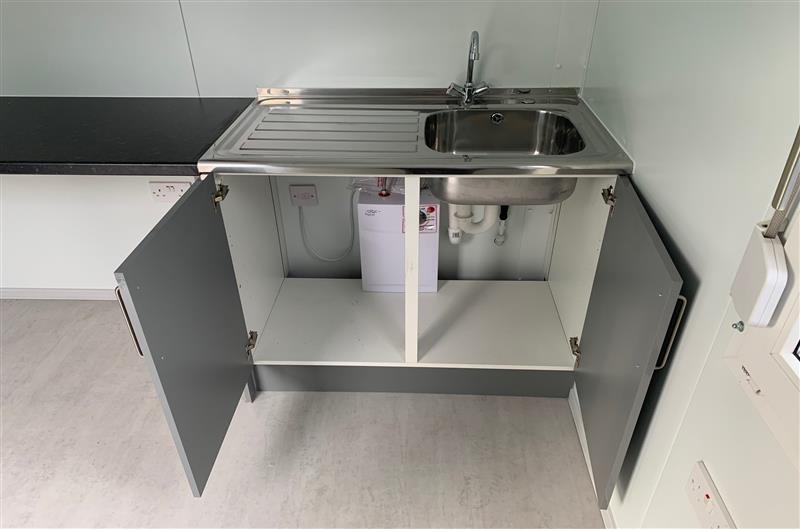
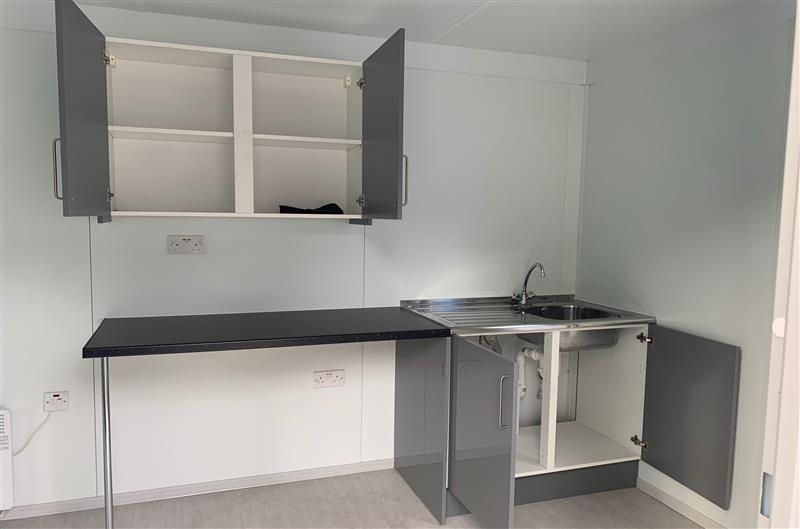
  • Kitchen with sink worktop, cupboard and water heater
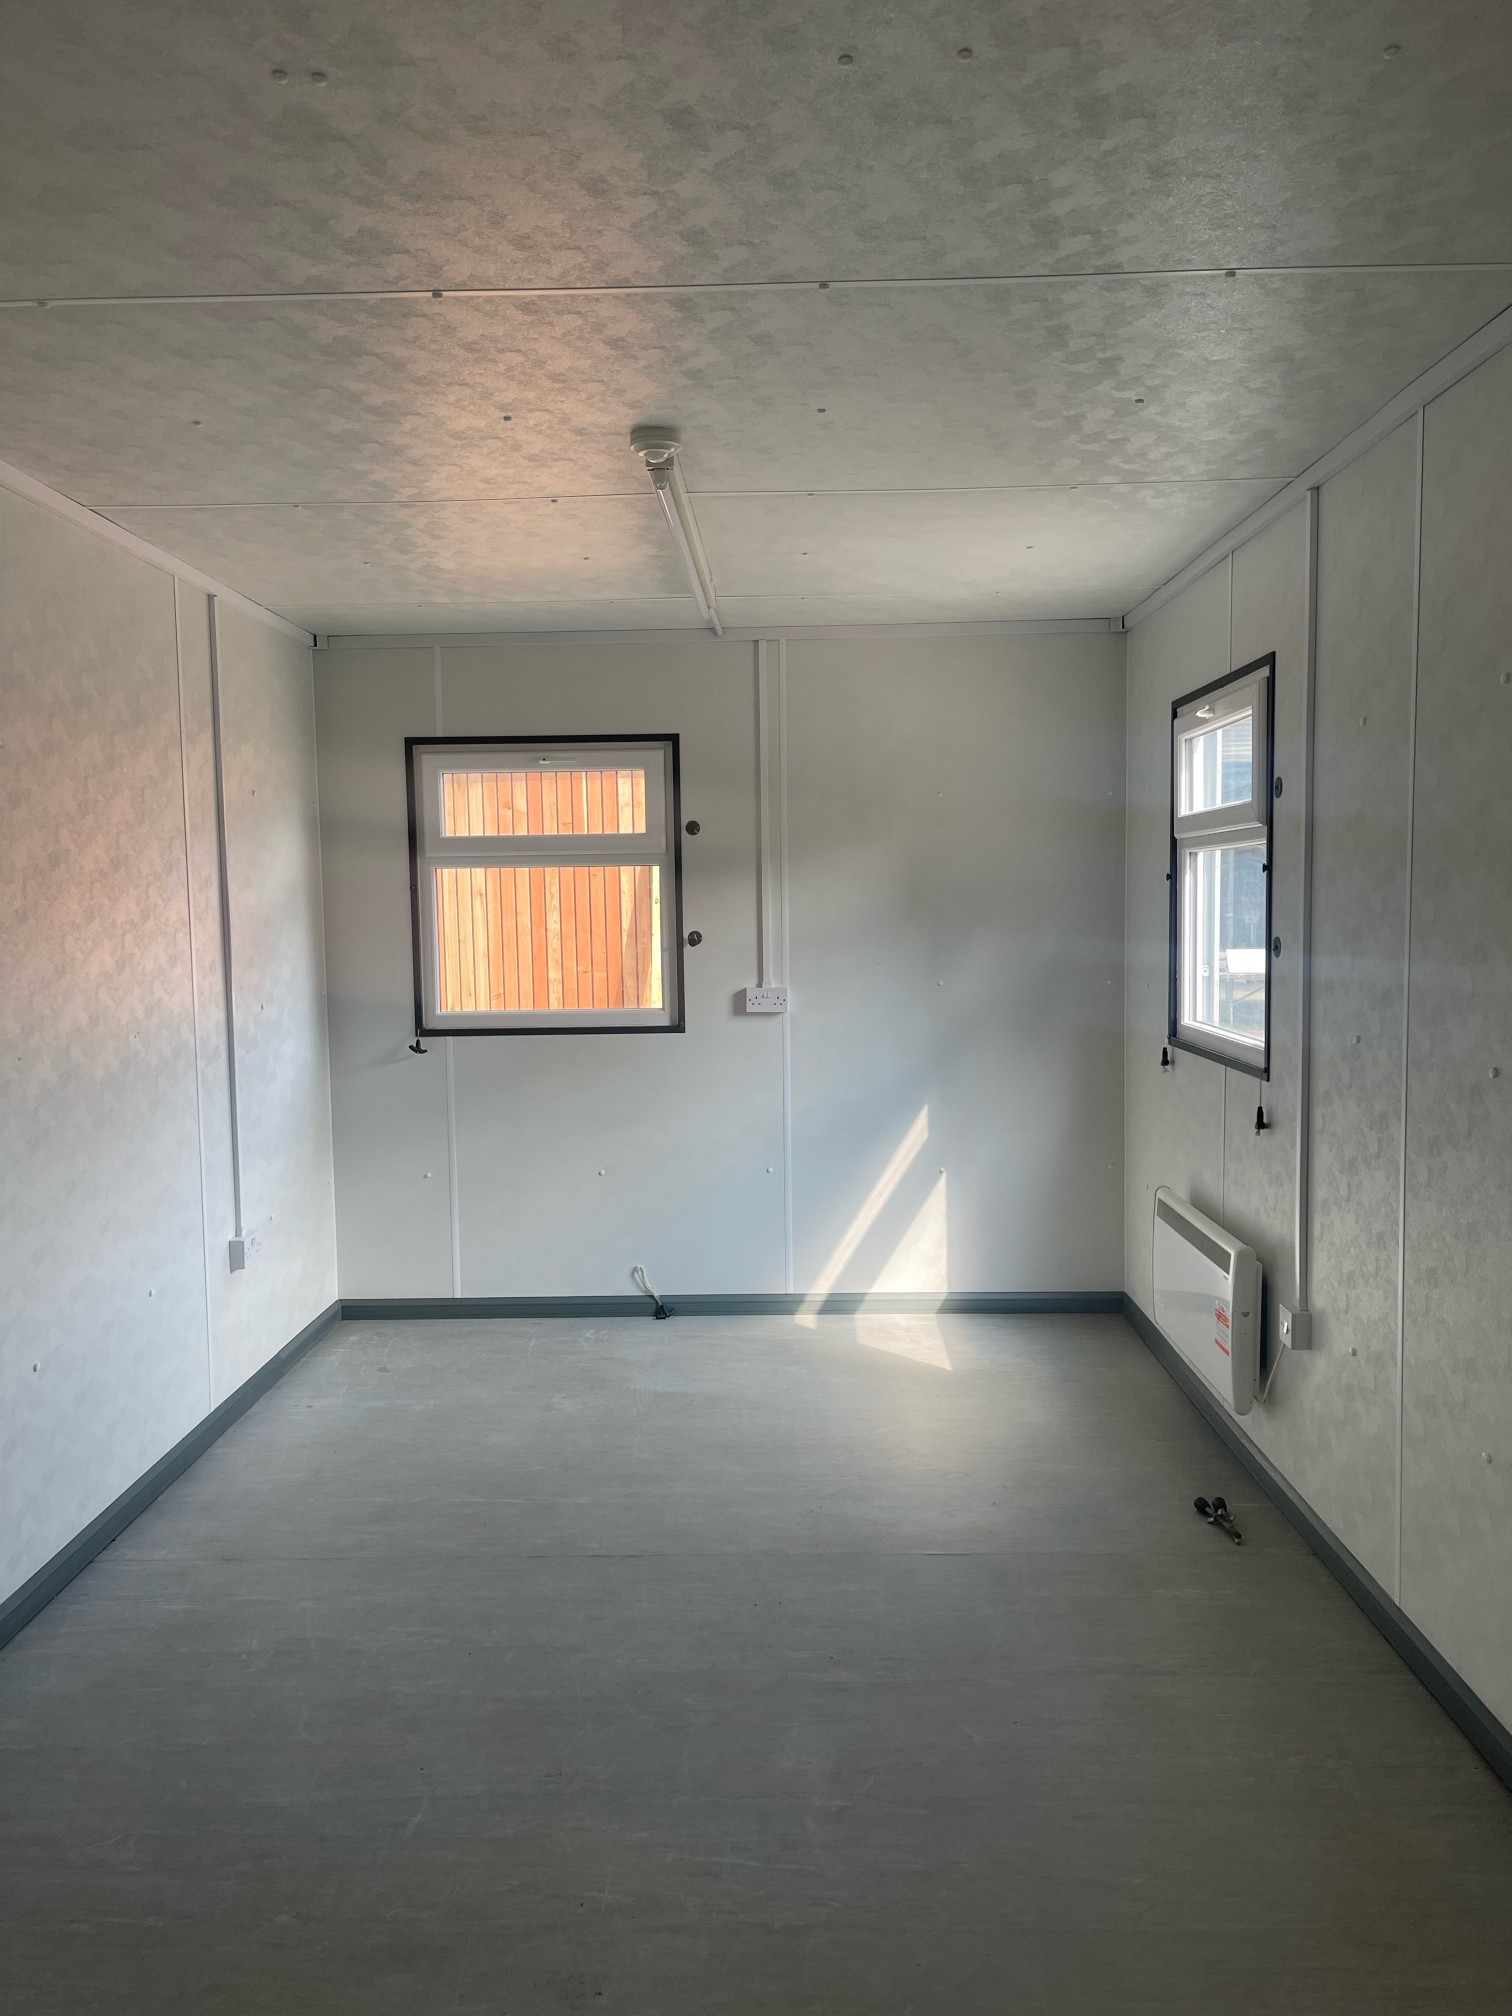
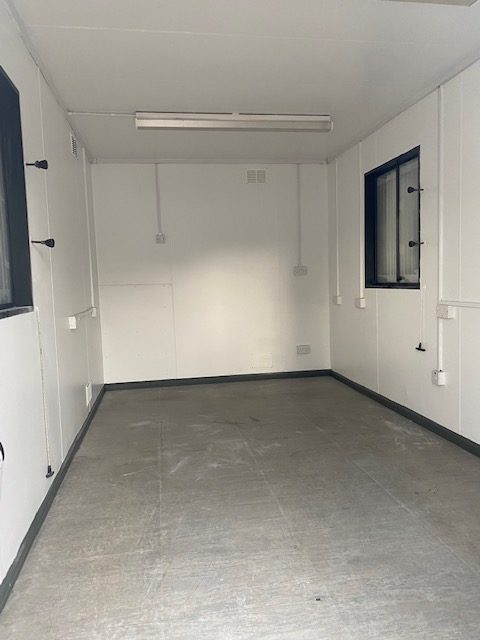
  • Insulated with electric sockets, lighting and heating
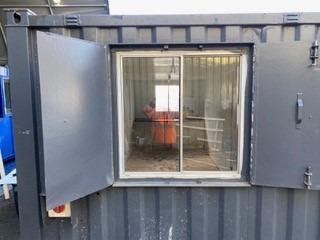
  • White upvc double glazing
  • External re spray in dark grey

Location: Nationwide

£6,500 + vat

Not Available for Hire

We can deliver for a cost please ask and send us post code.

Call for an instant quote!

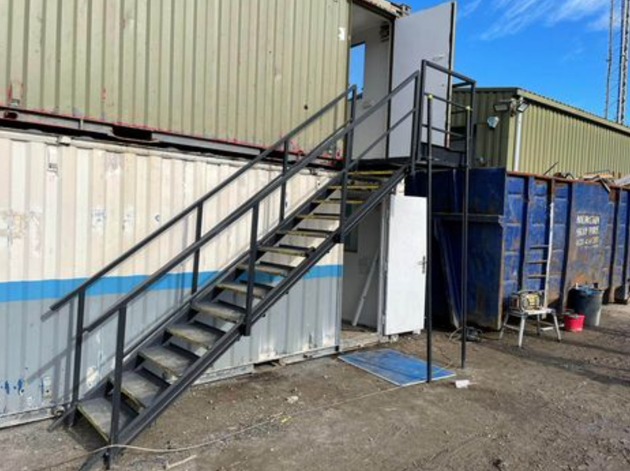
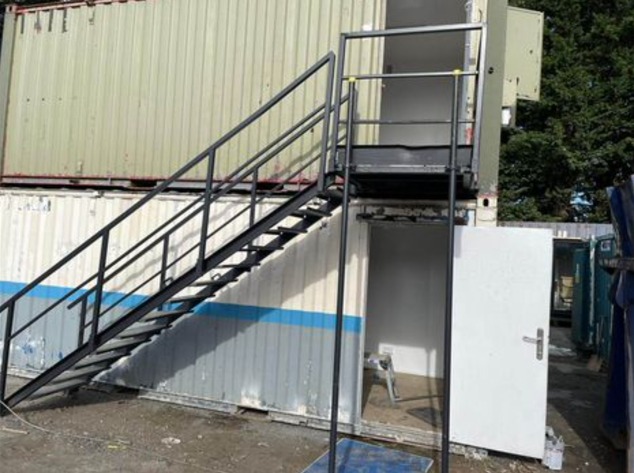
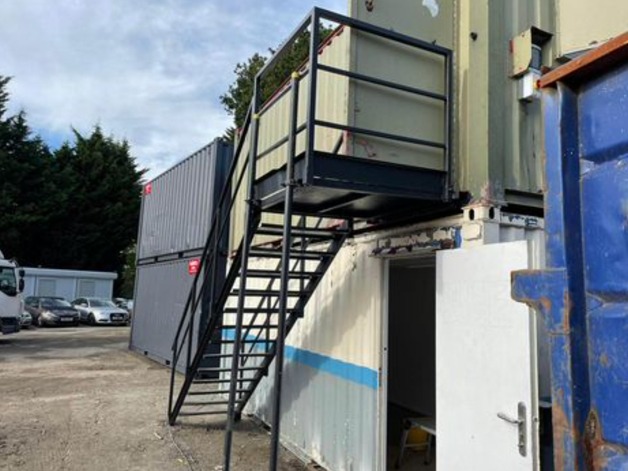
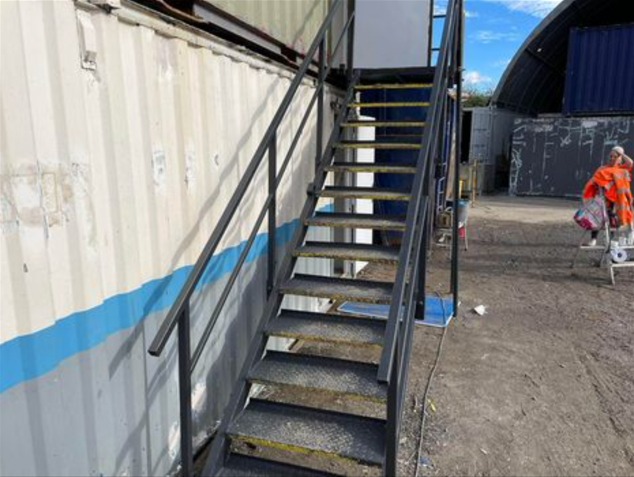
Steel Cabin Staircases, in various sizes

  • 13 tread

  • 14 tread

  • 15 tread

Location: Nationwide

£1,200.00 + vat

Not Available for Hire

Call for an instant quote!

32ft x 10ft Anti Vandal Canteen/Office

    • Price: £5,995 + VAT
    • Description: 32ft x 10ft Anti Vandal Canteen/Office
  Part refurbished including:
  • Electric sockets, lighting and heating
  • White upvc double glazing
  • Canteen
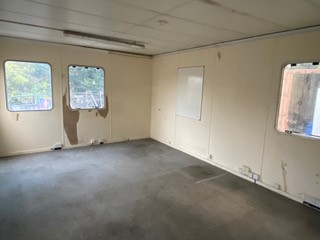
  • Open plan
  • External light grey re spray

Location: Nationwide

£5,995 + vat

Not Available for Hire

We can deliver for a cost please ask and send us post code.

Call for an instant quote!

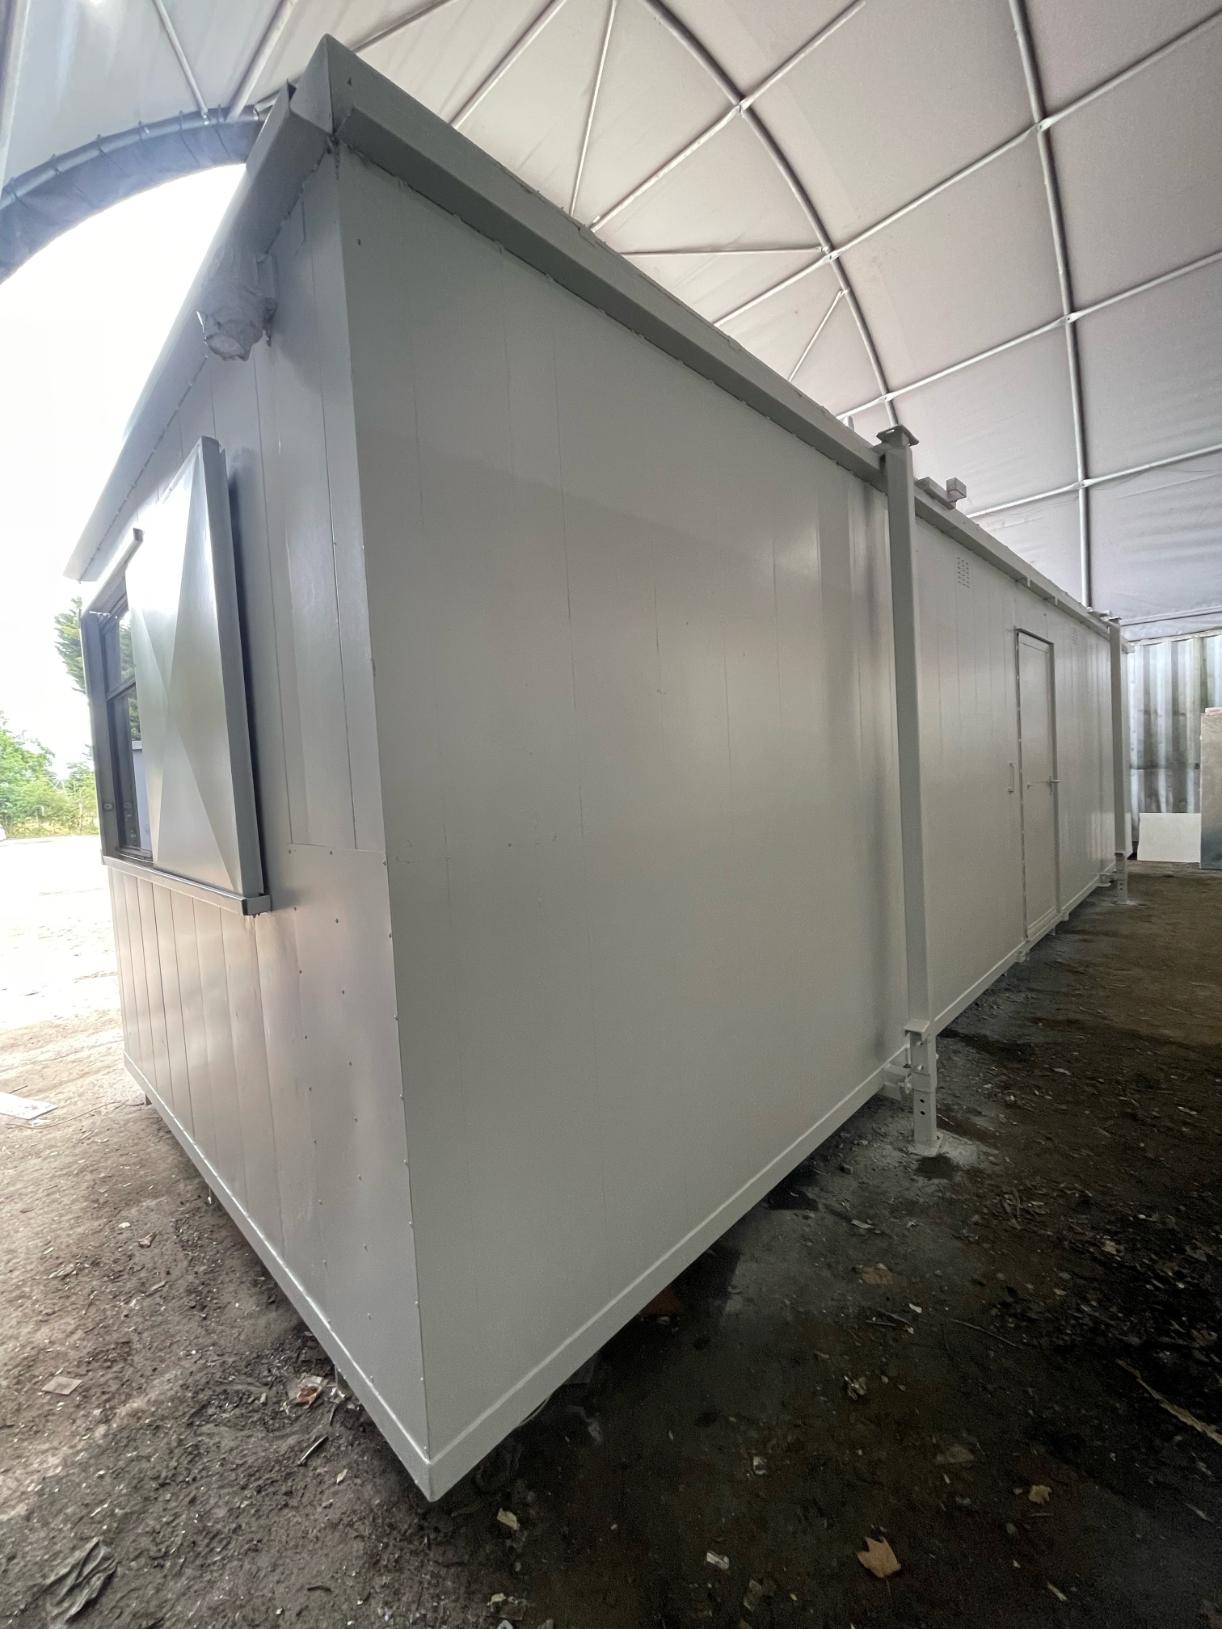
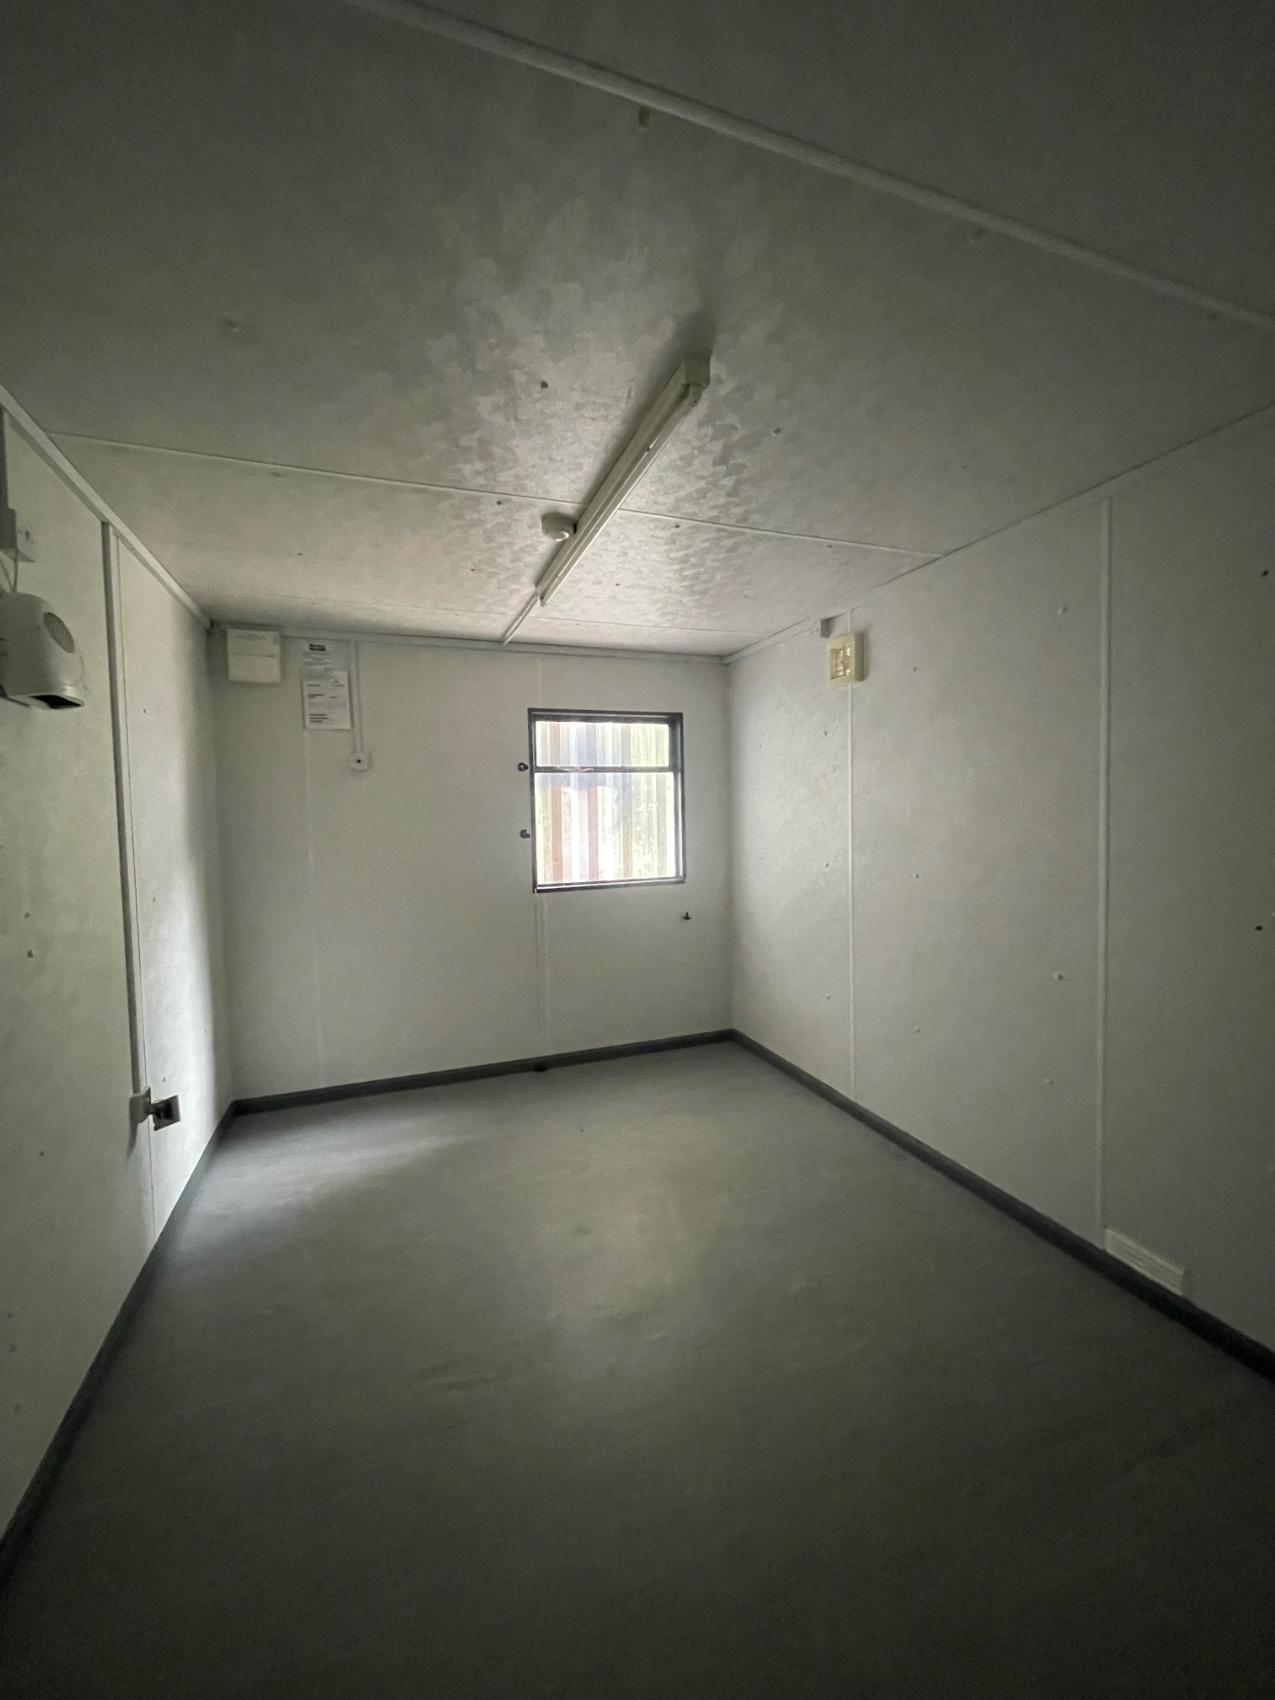
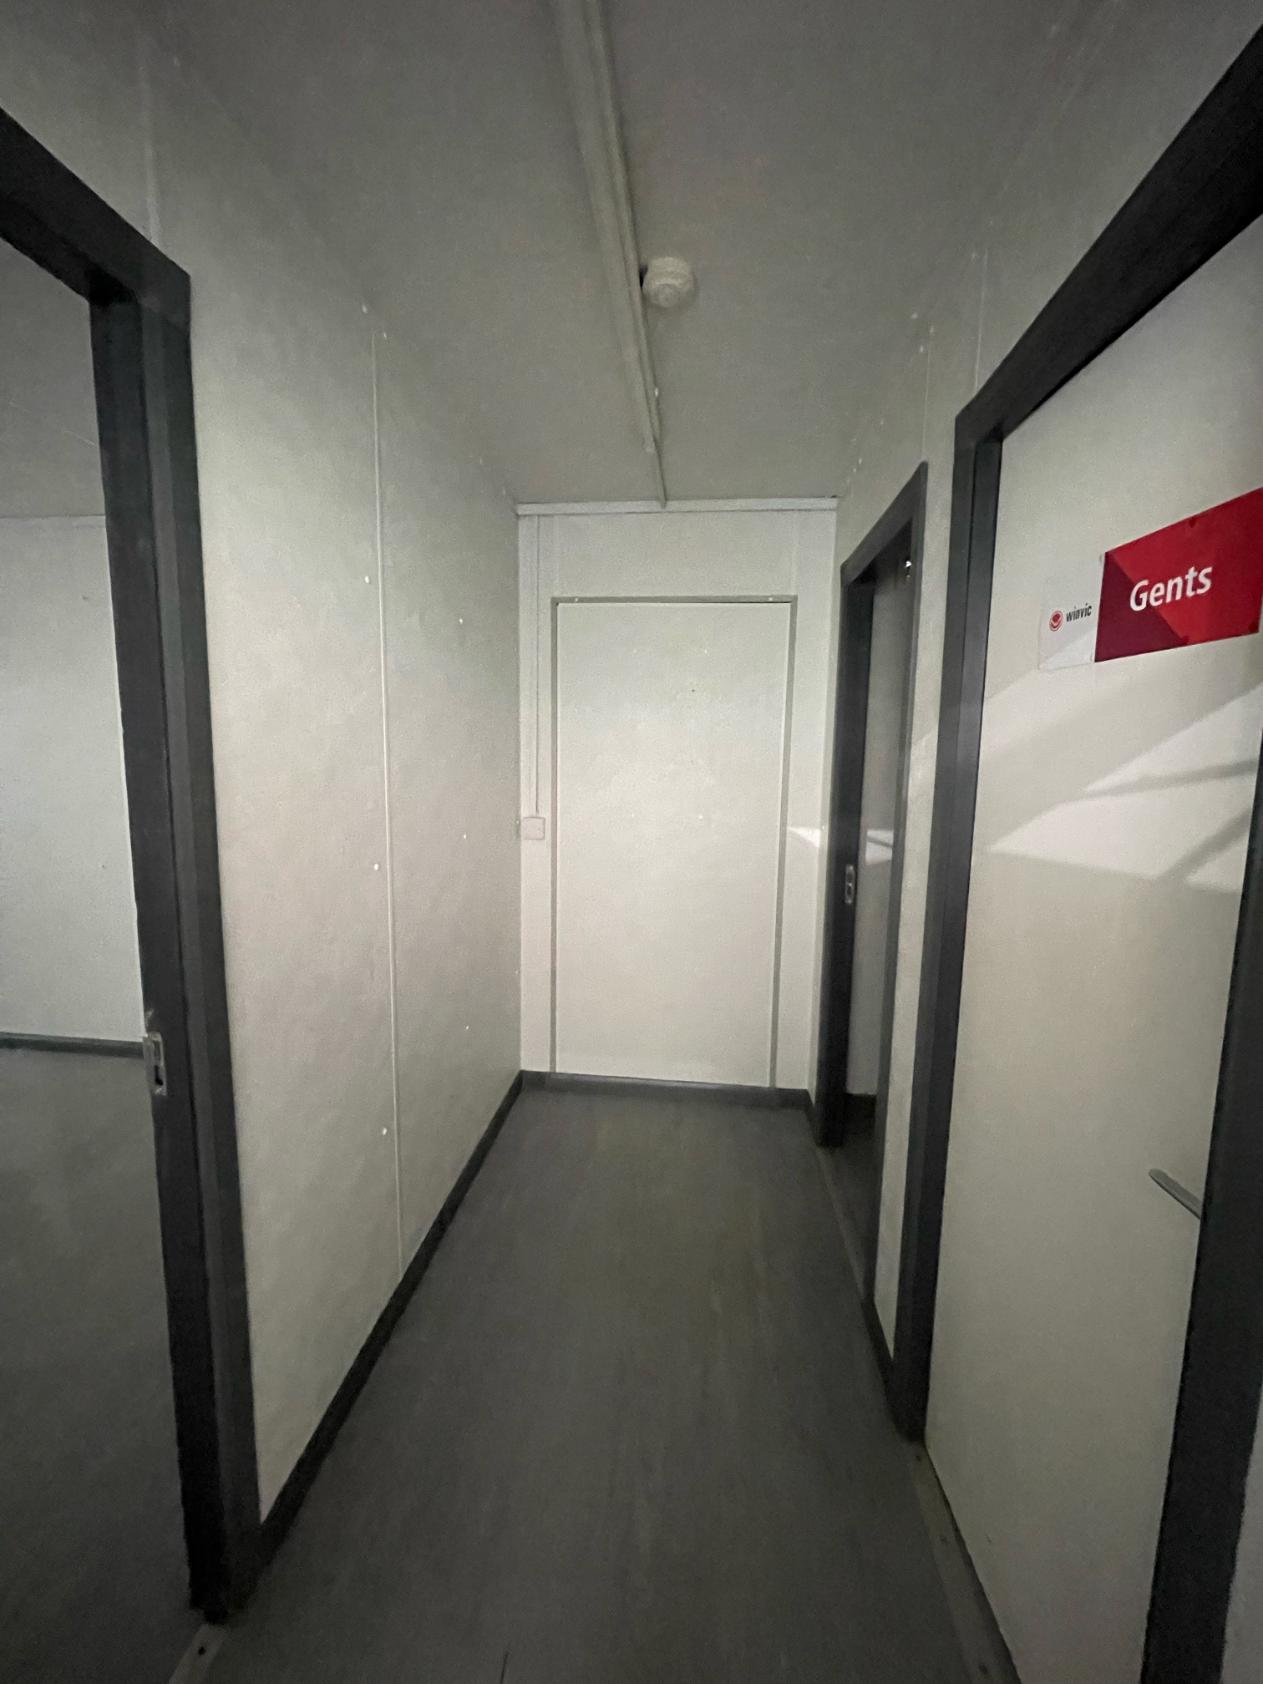
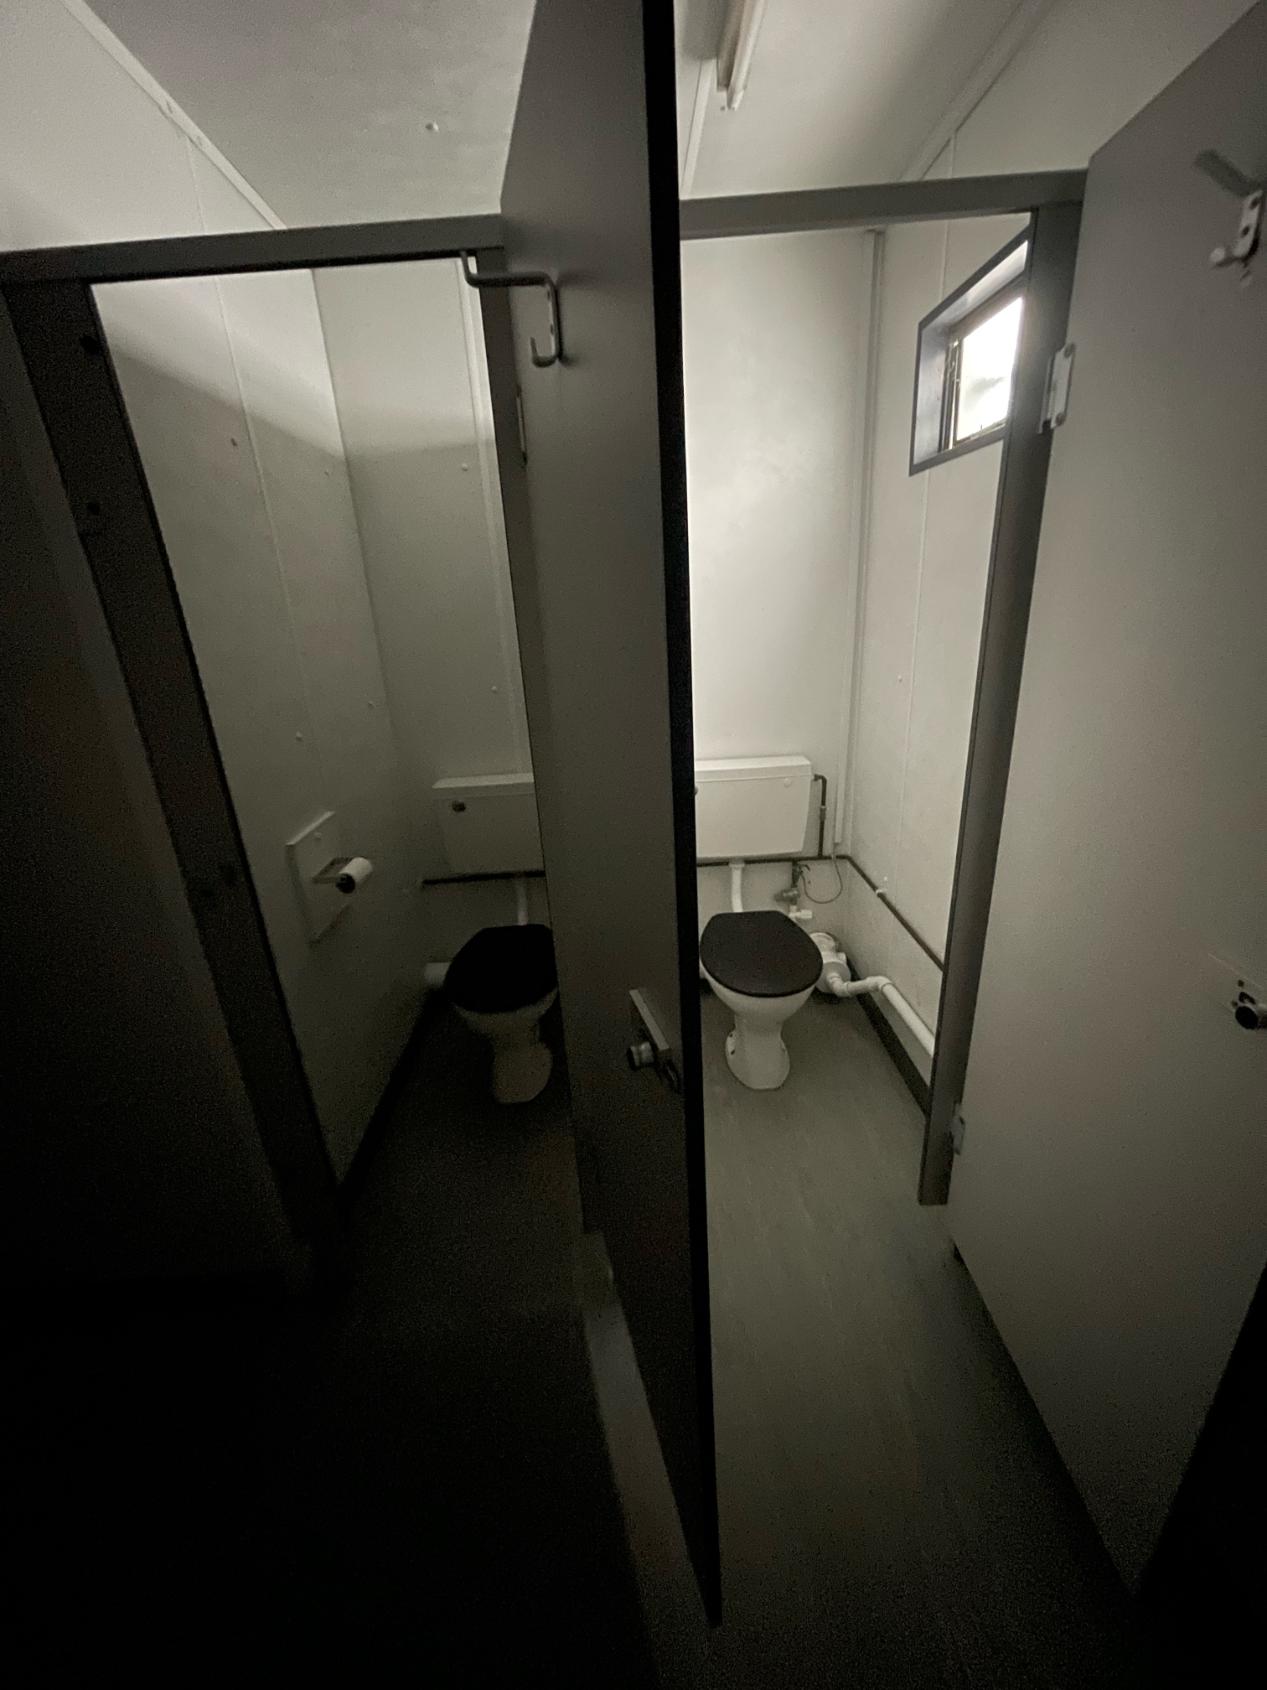
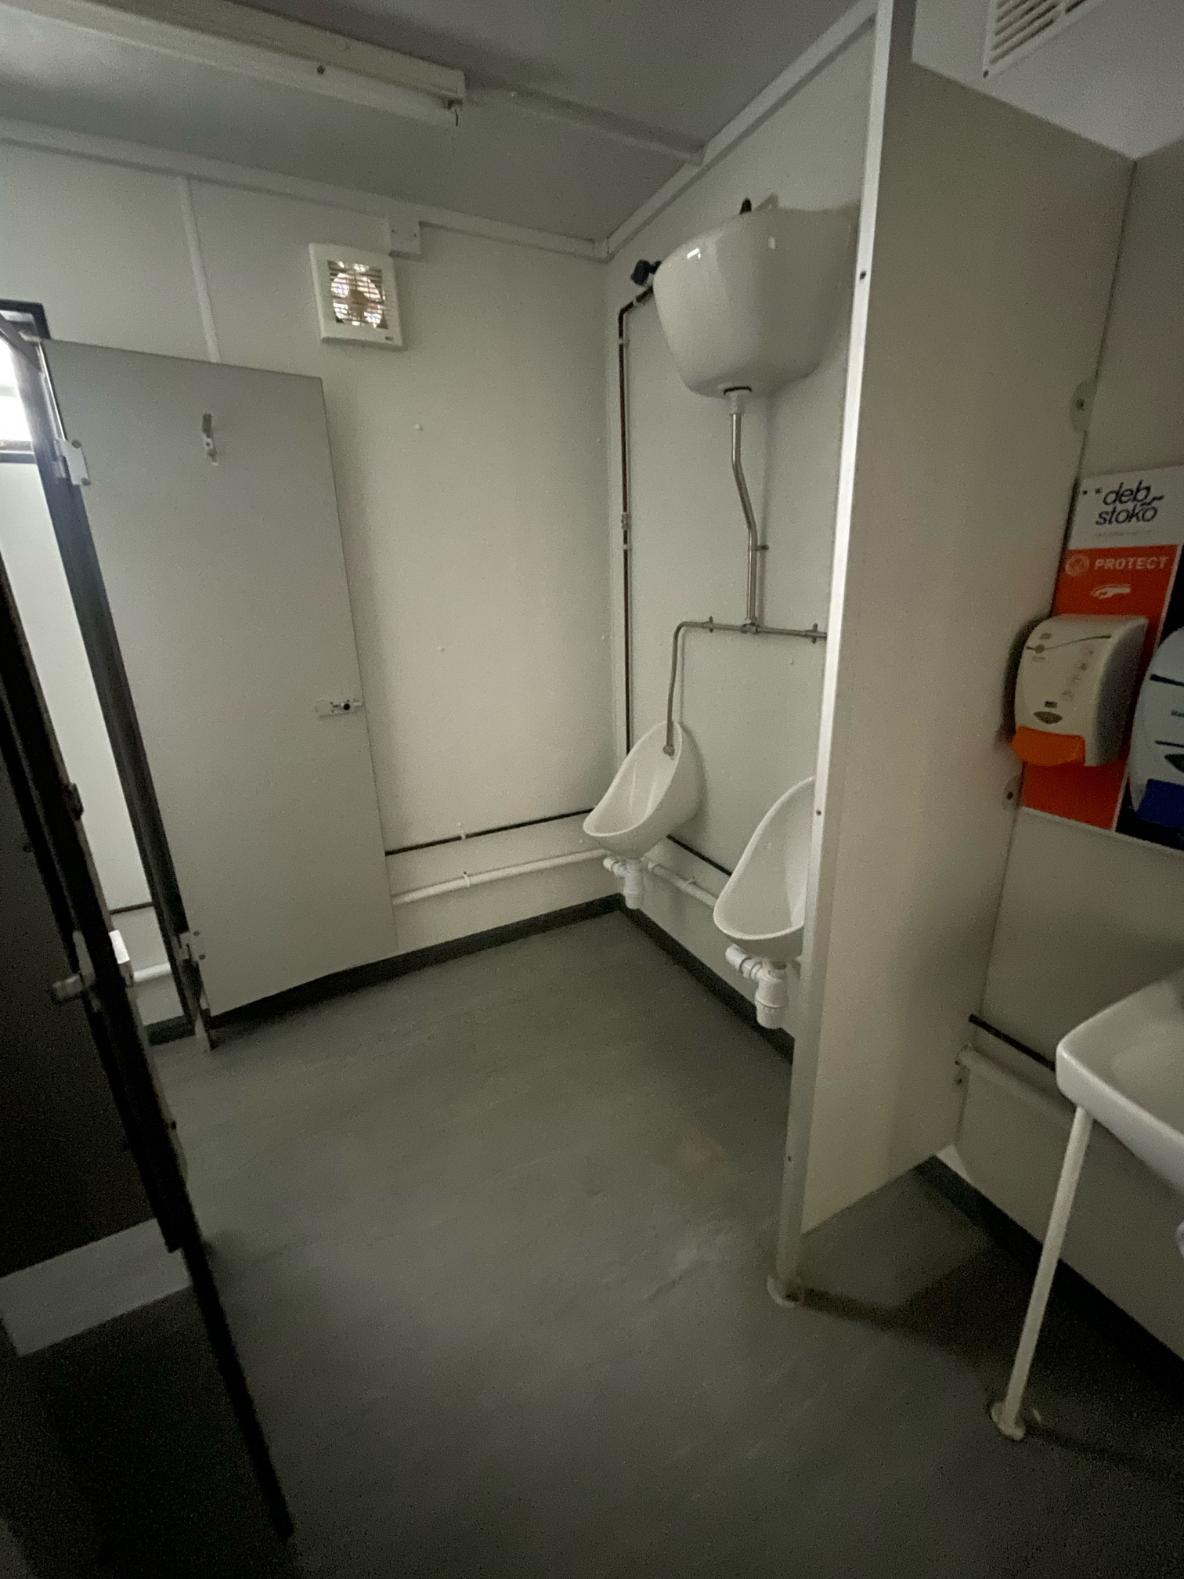
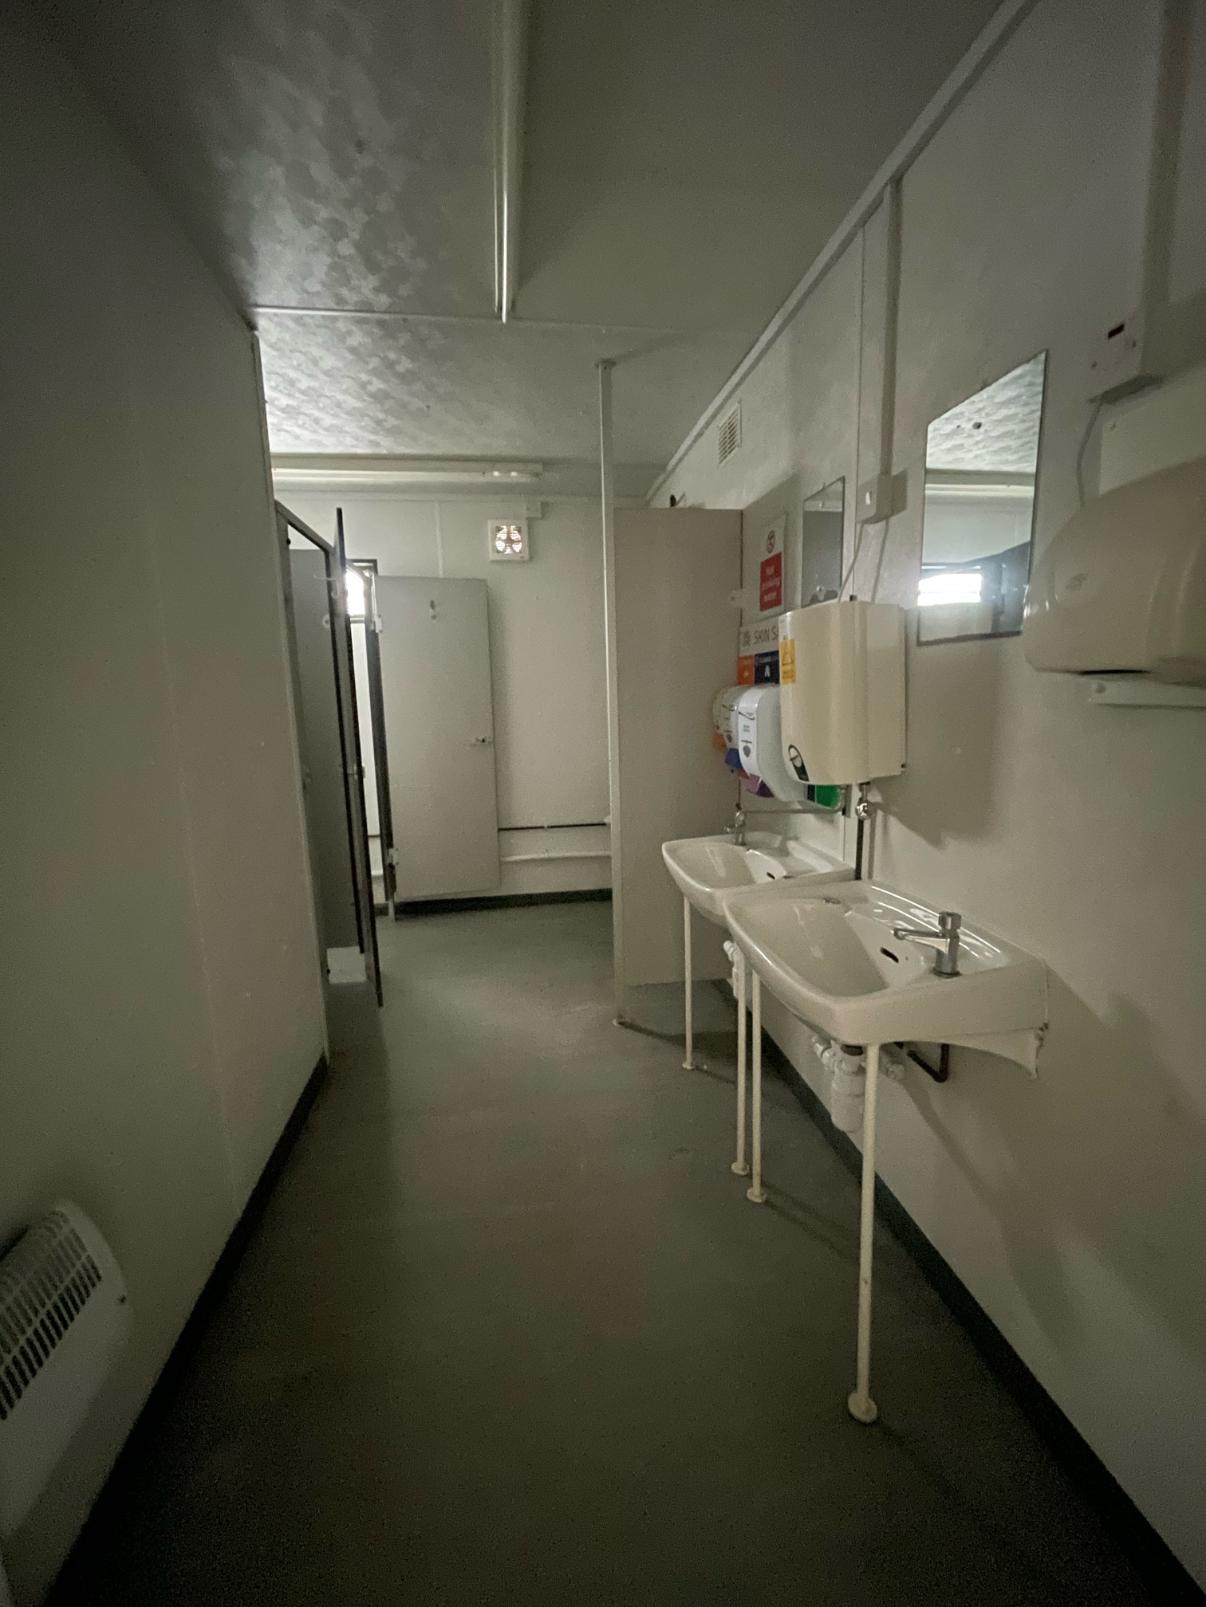
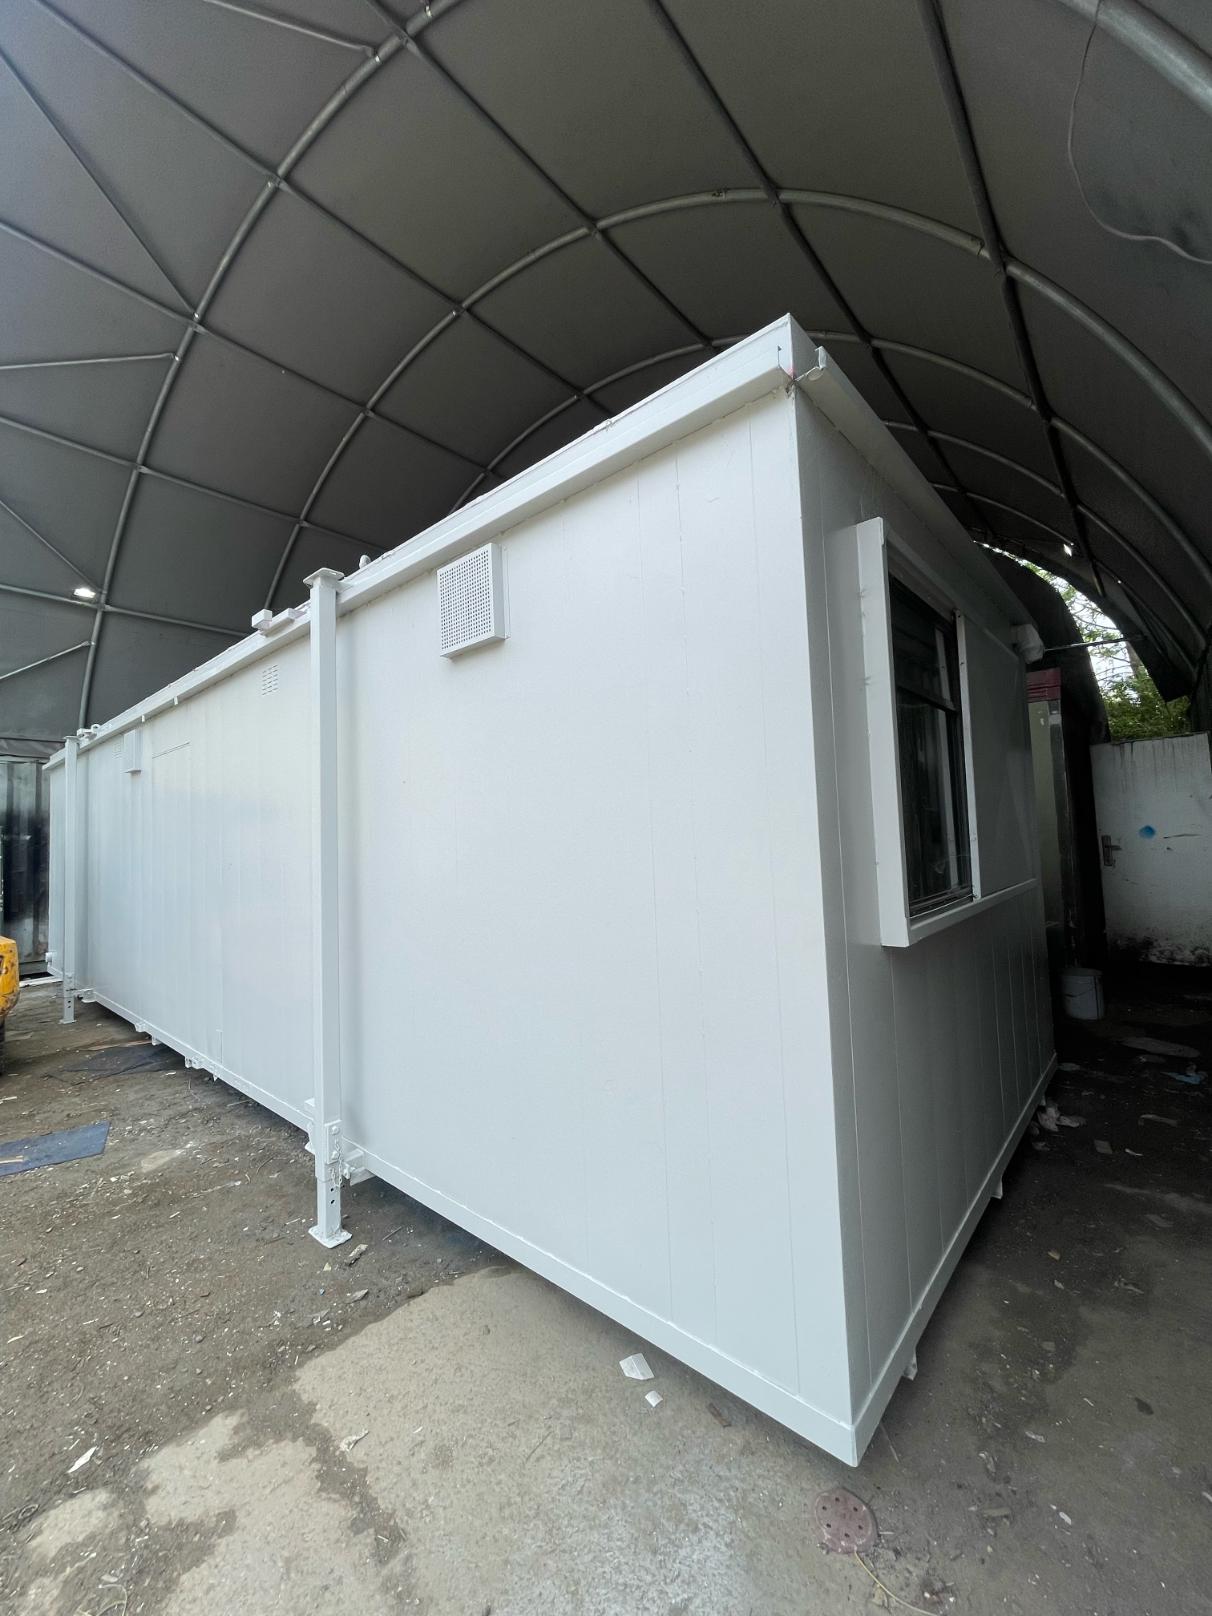
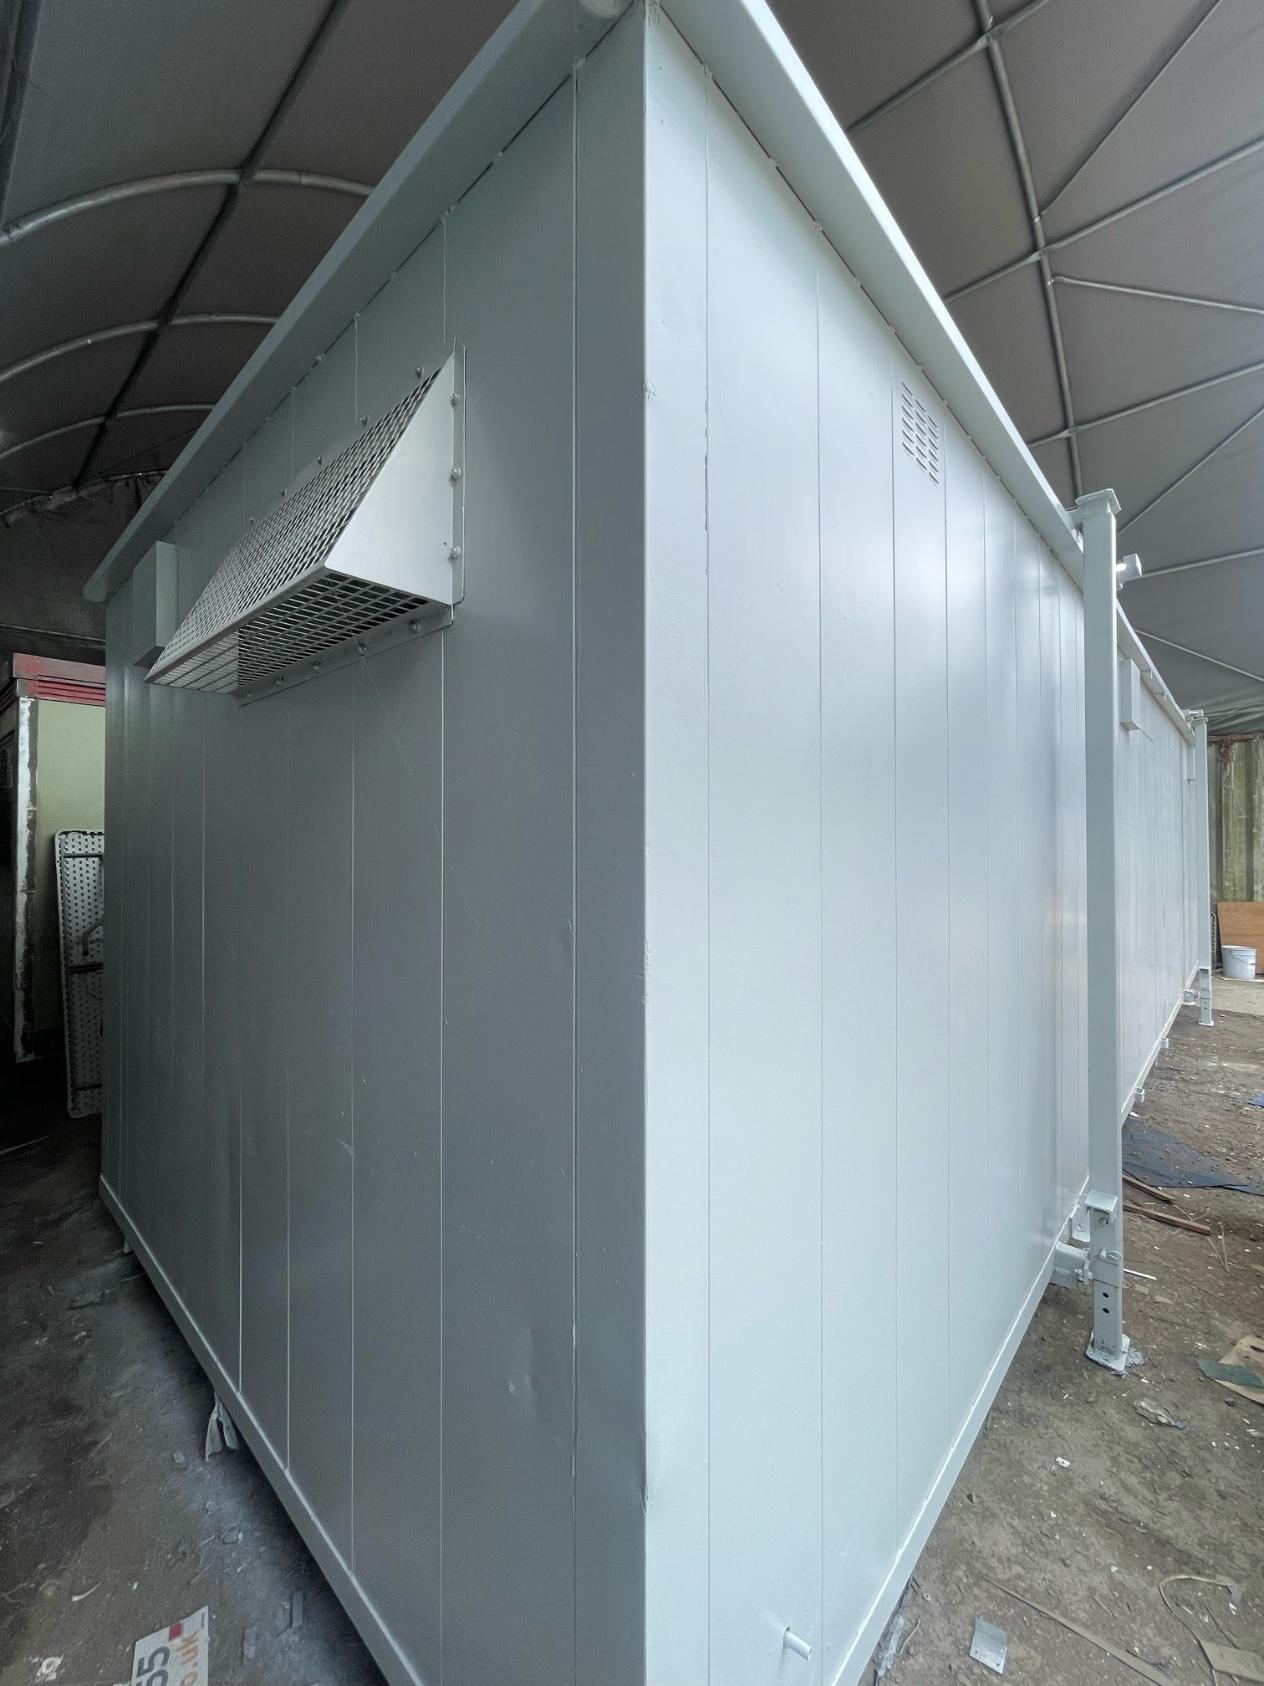
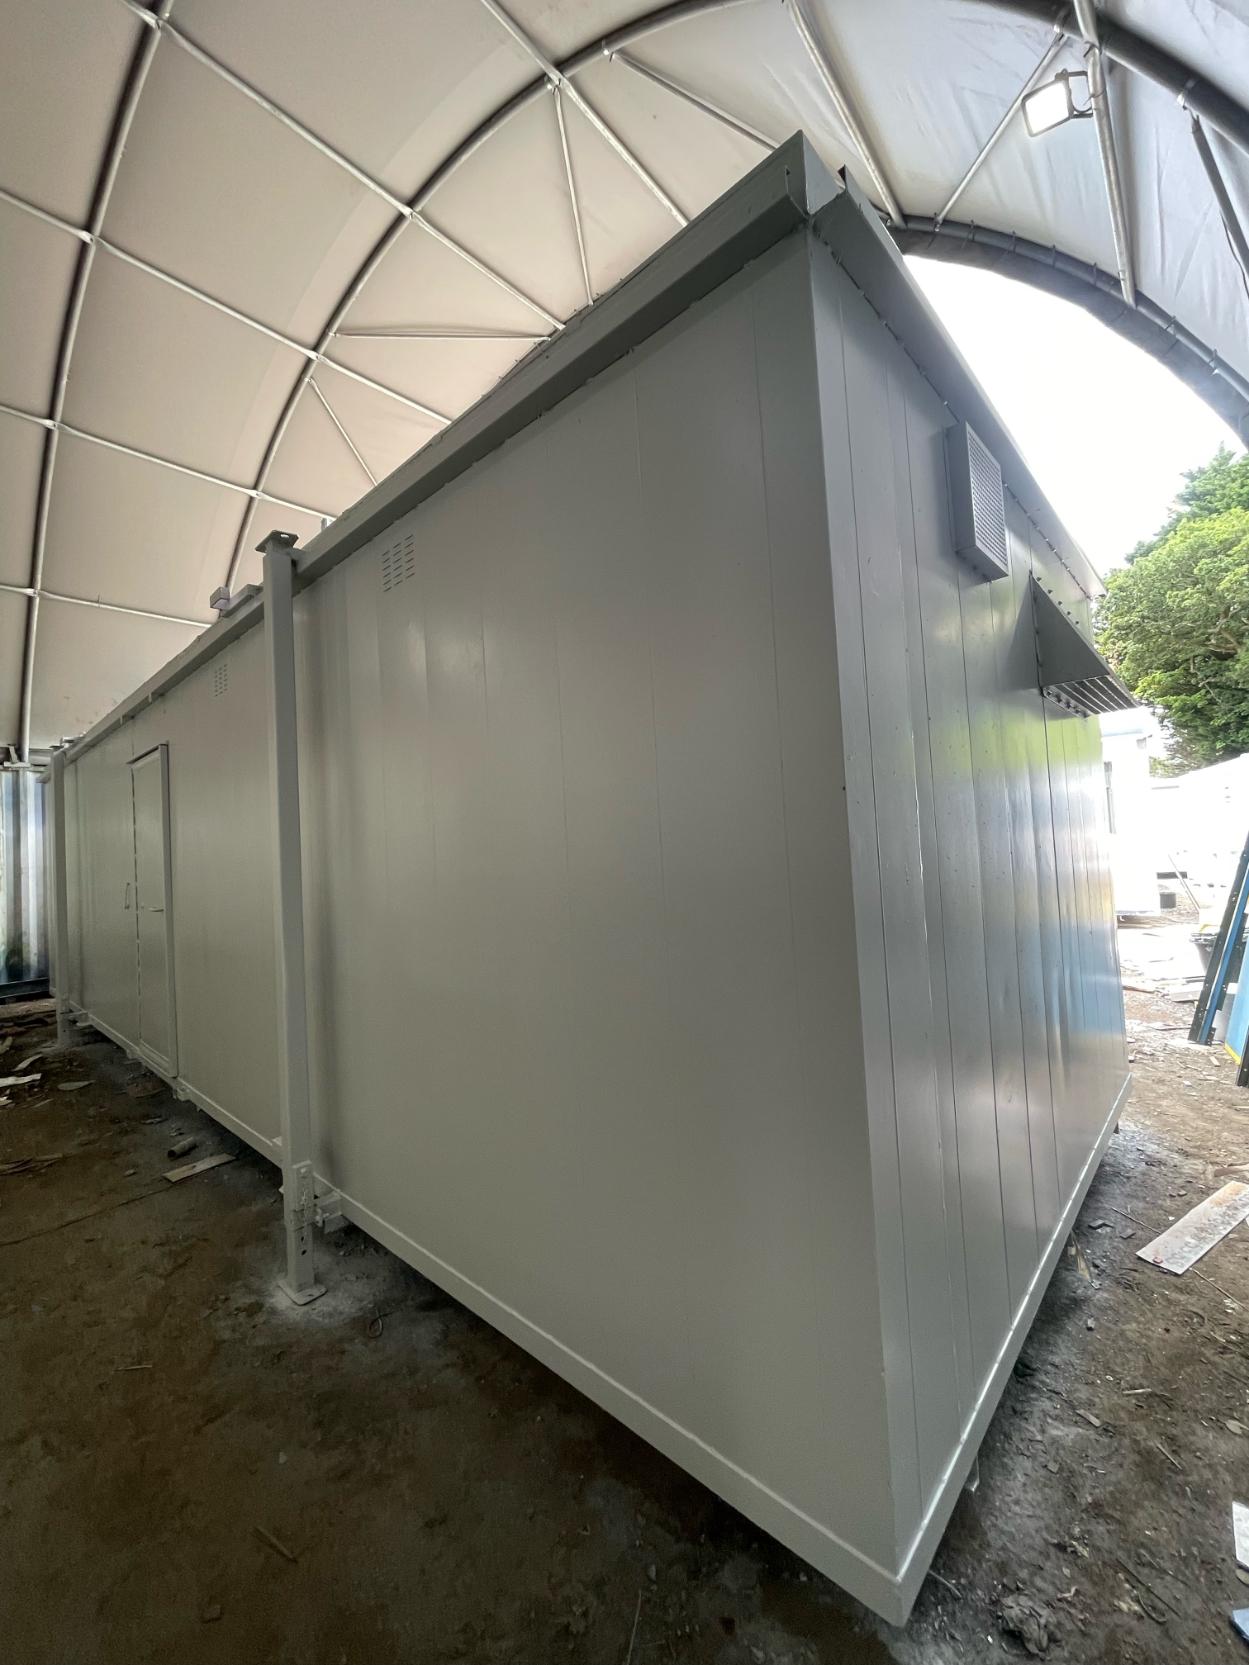
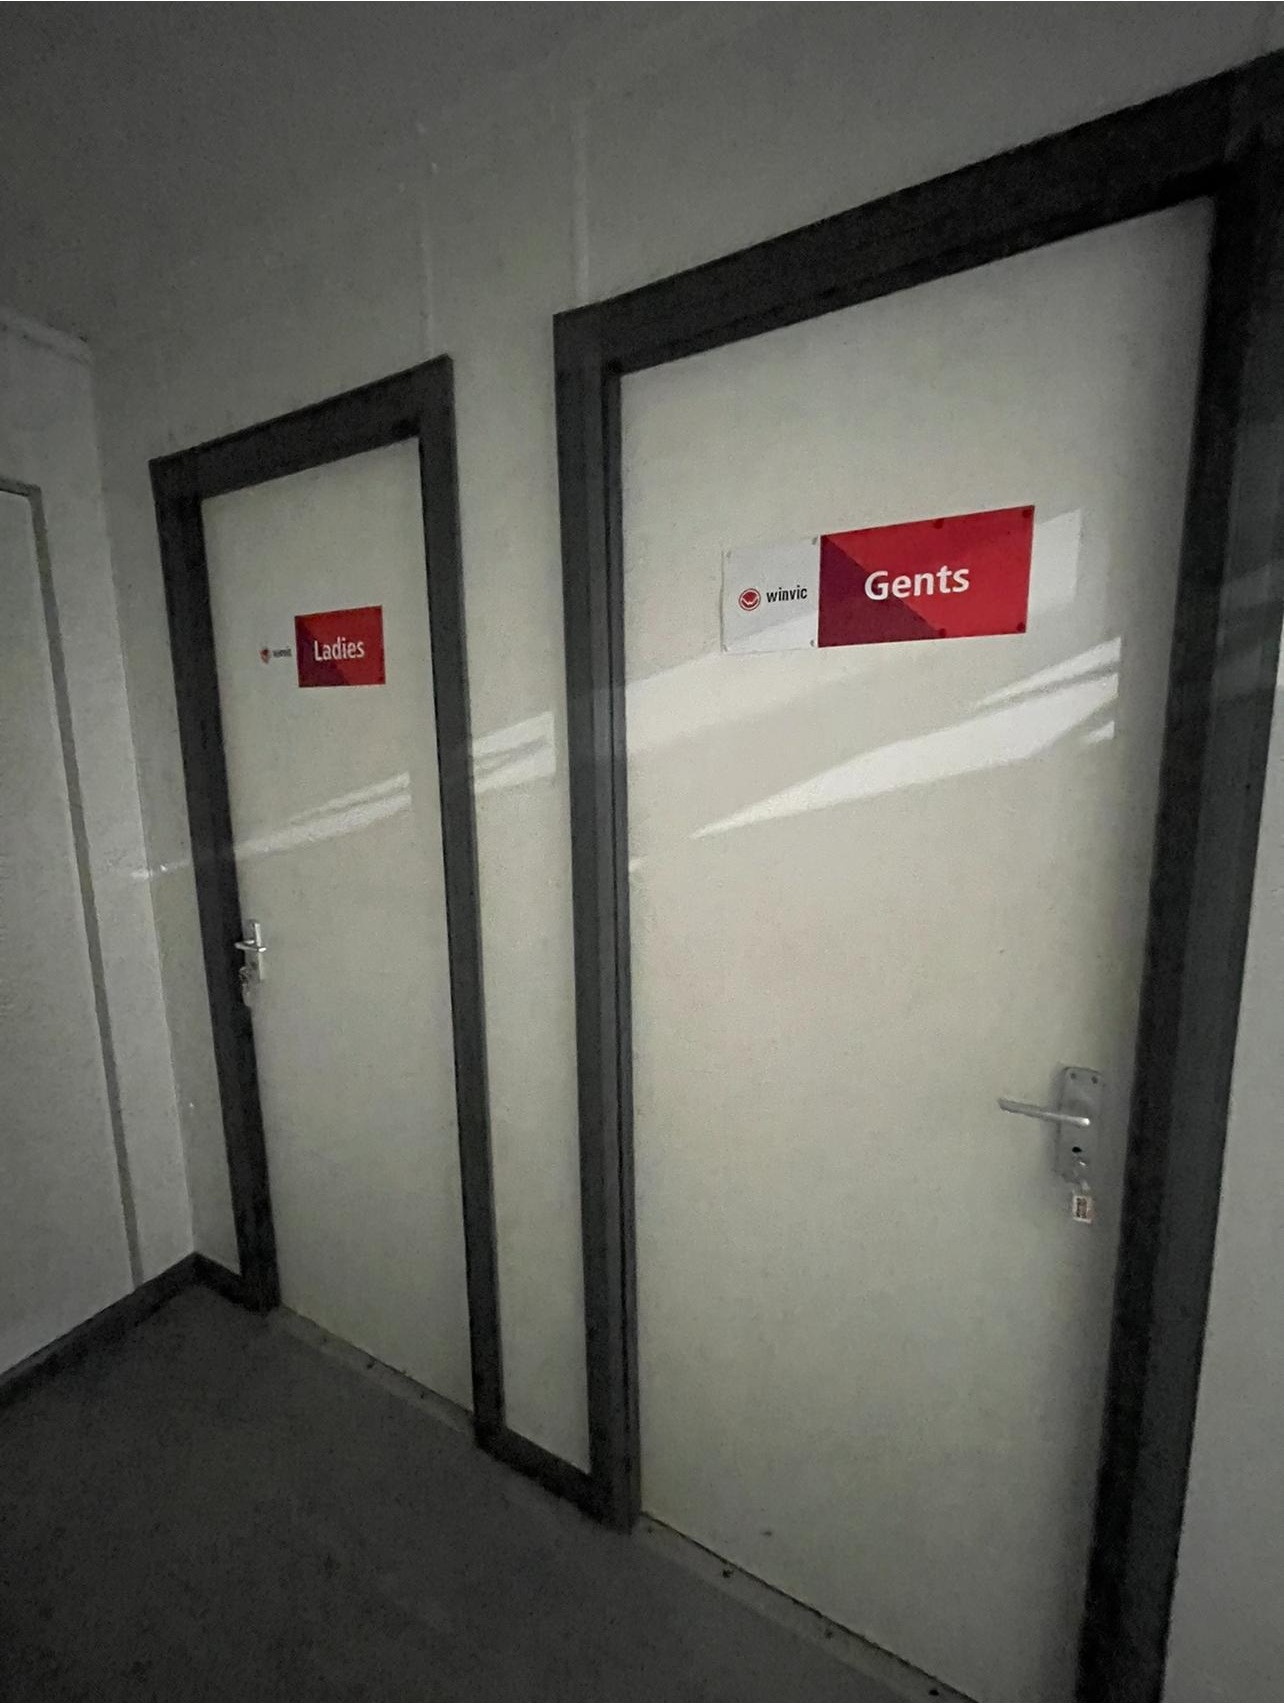
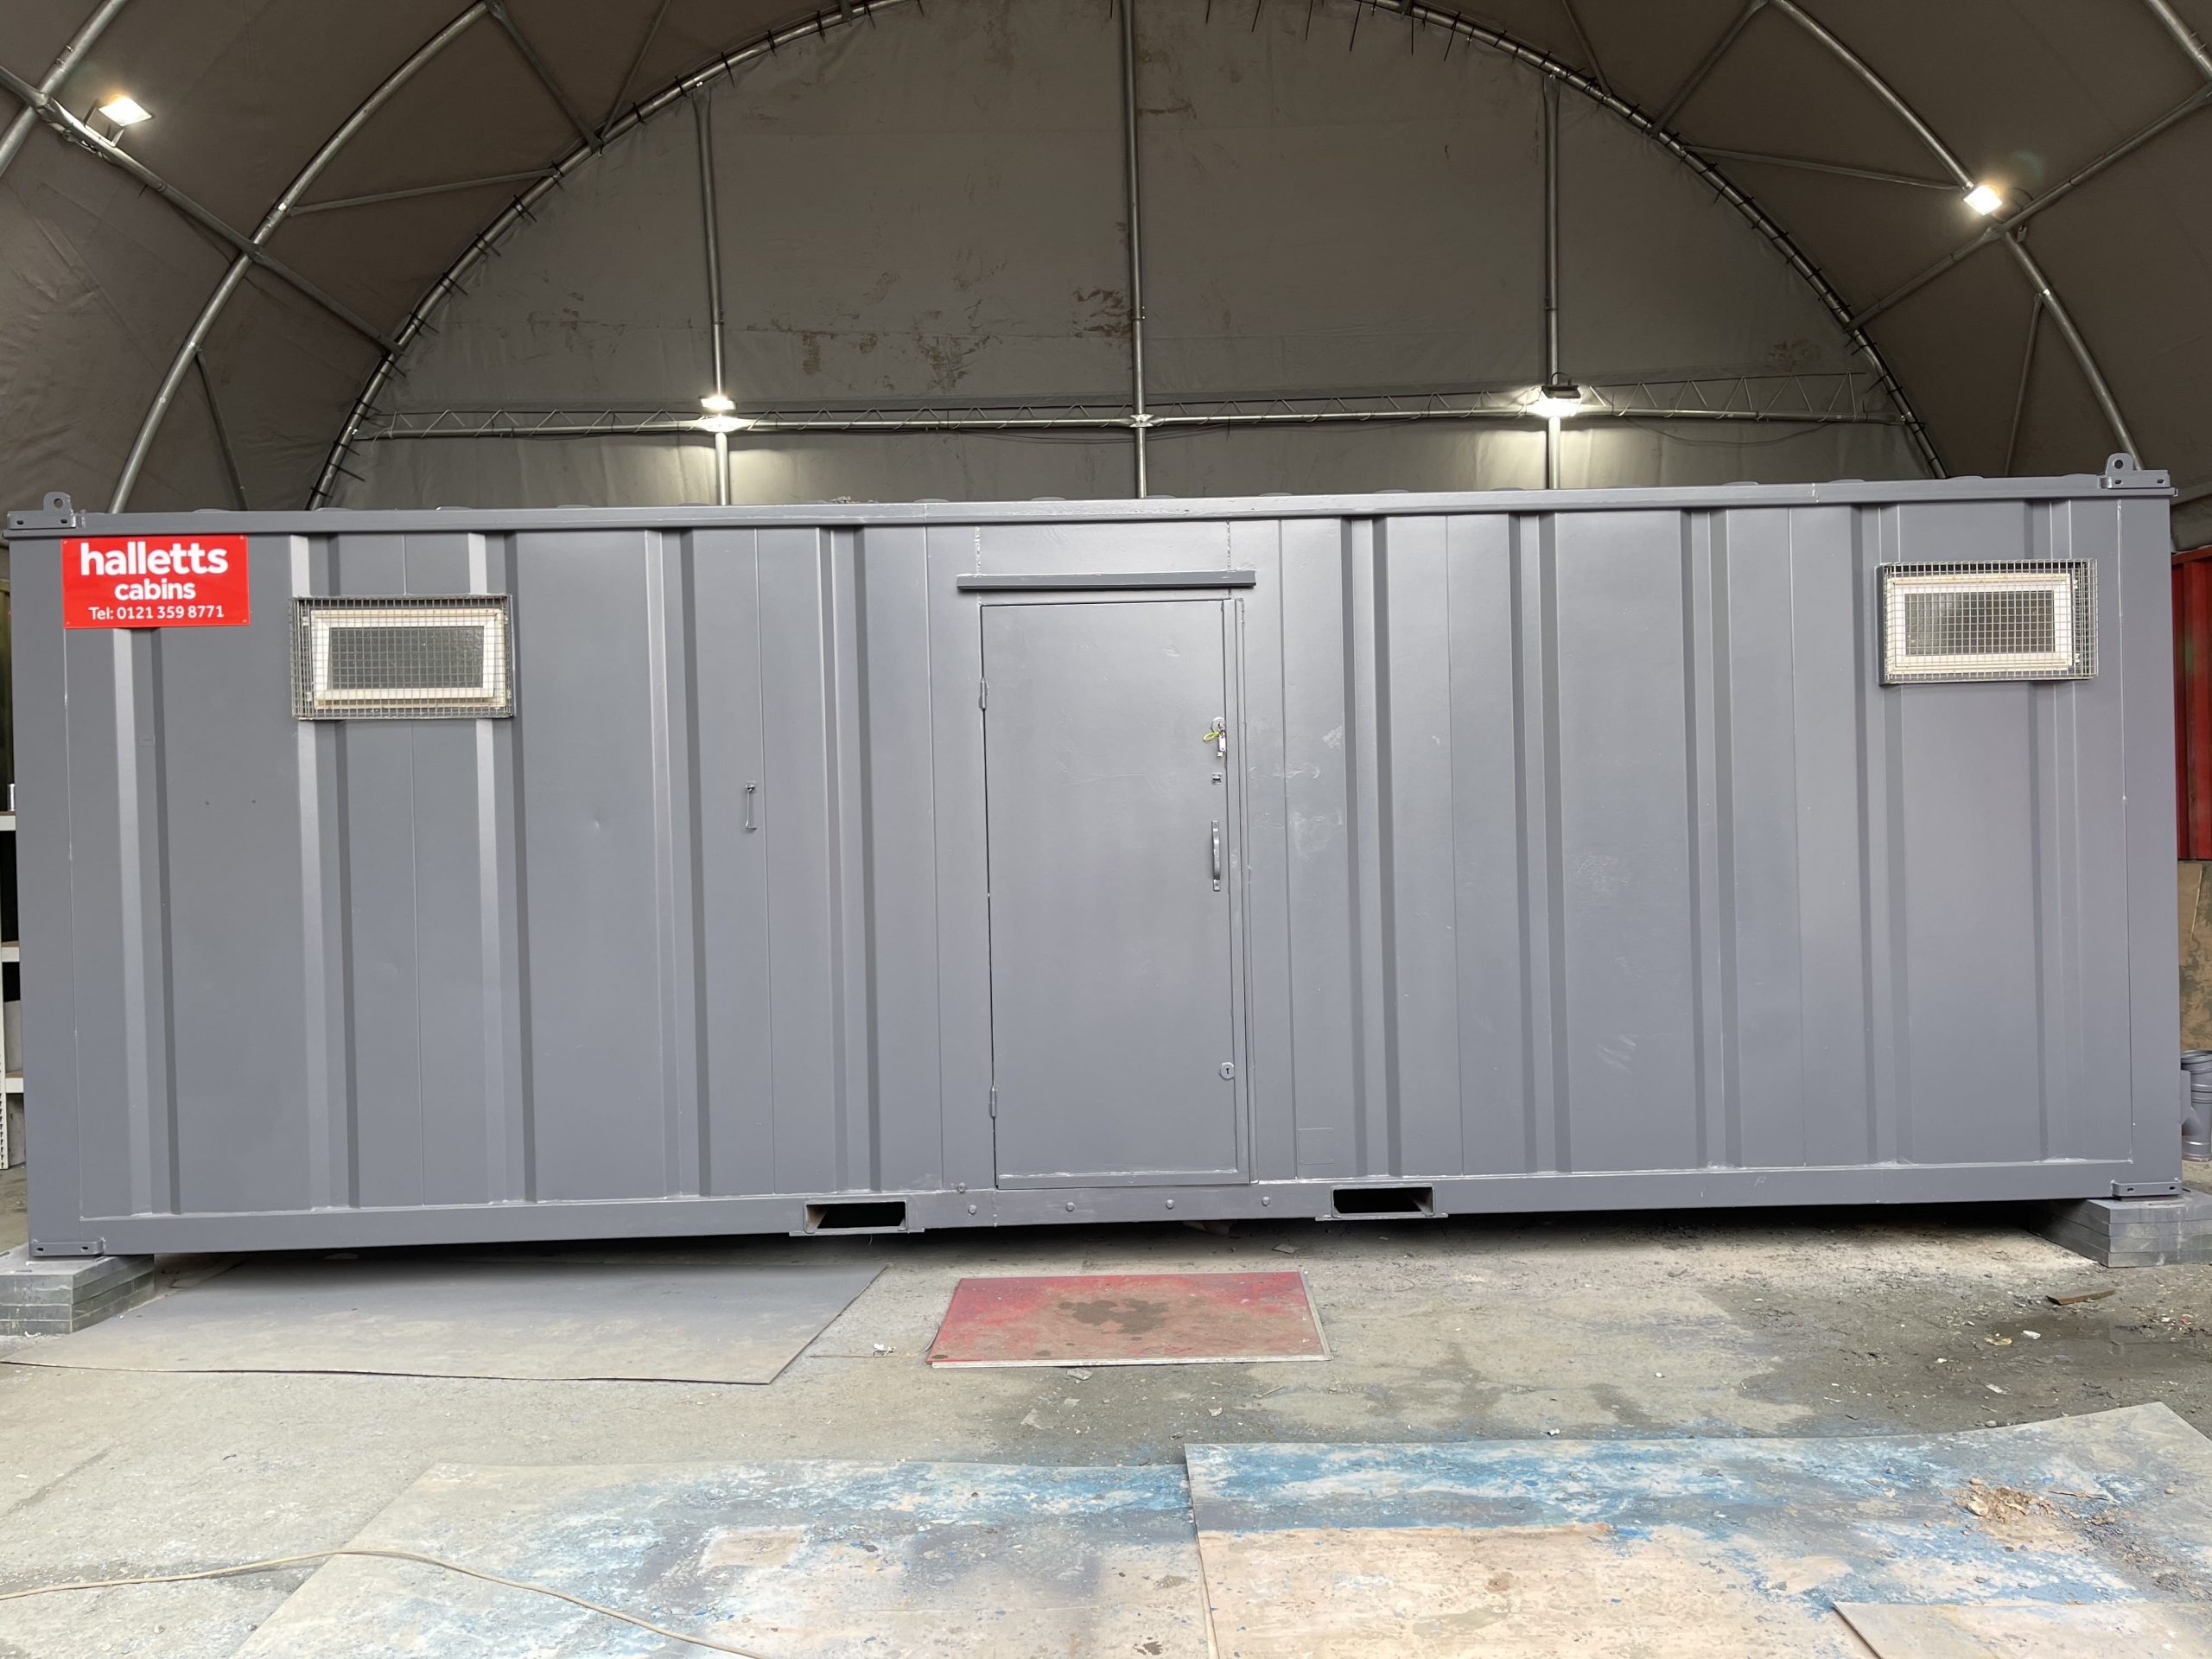
32ft x 10ft Drying Room, Toilet Block

Hallway leading into:

  • Price: £6,500 + VAT
  • Half open plan drying room, or we could add in a canteen. (additional cost)
  • Female Single toilet
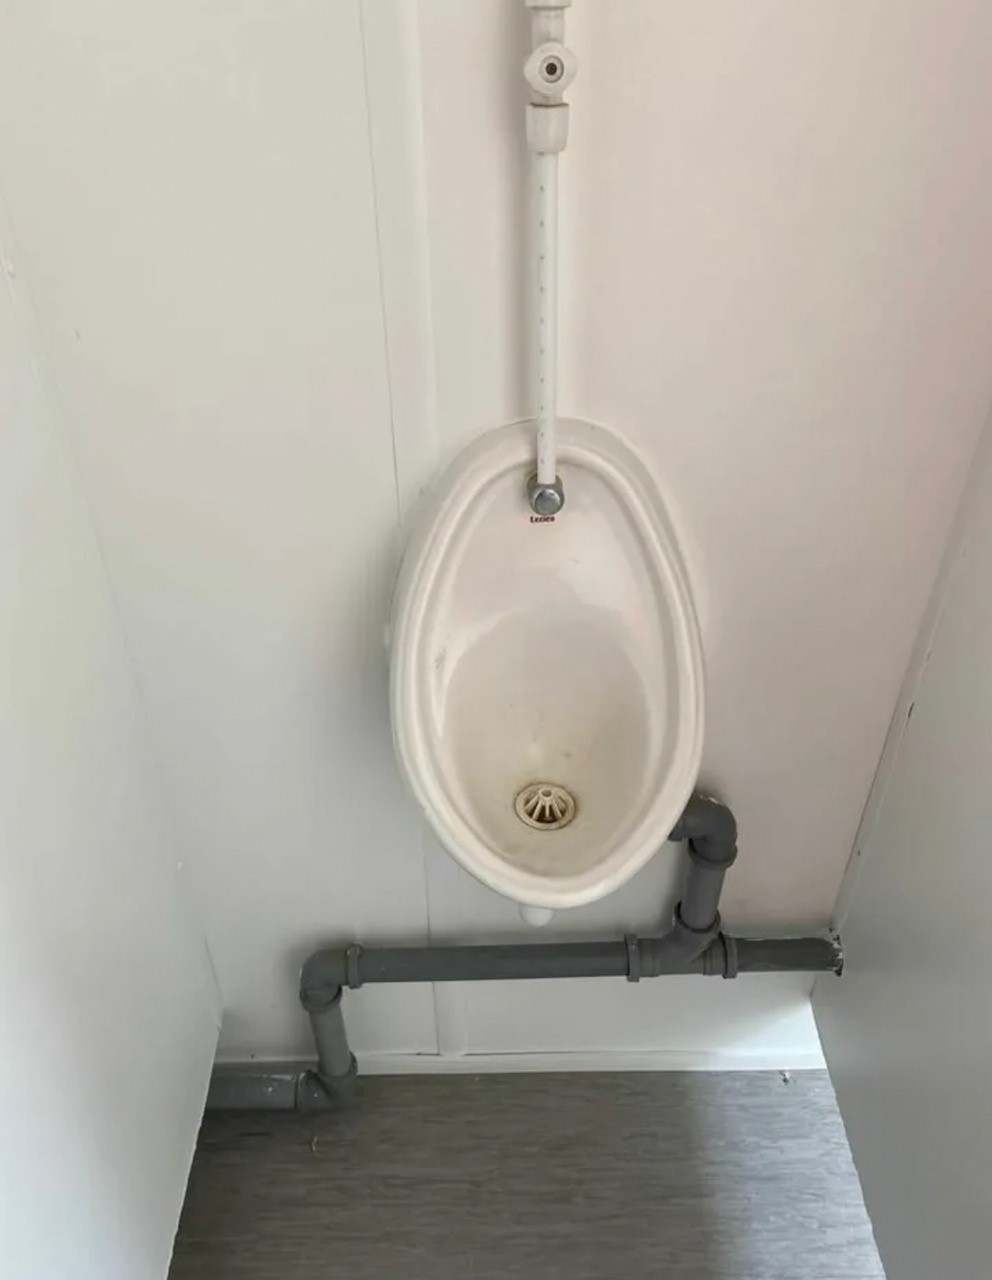
  • Male toilets including 2 x cubicles, 2 x urinals and 2 x sinks
  • External light grey spray
  • Deep cleaned
  • Ready to use
  • Excellent overall condition

Transport can be arranged please ask.

Location: Nationwide

£6,500.00 + vat

Not Available for Hire

Call for an instant quote!

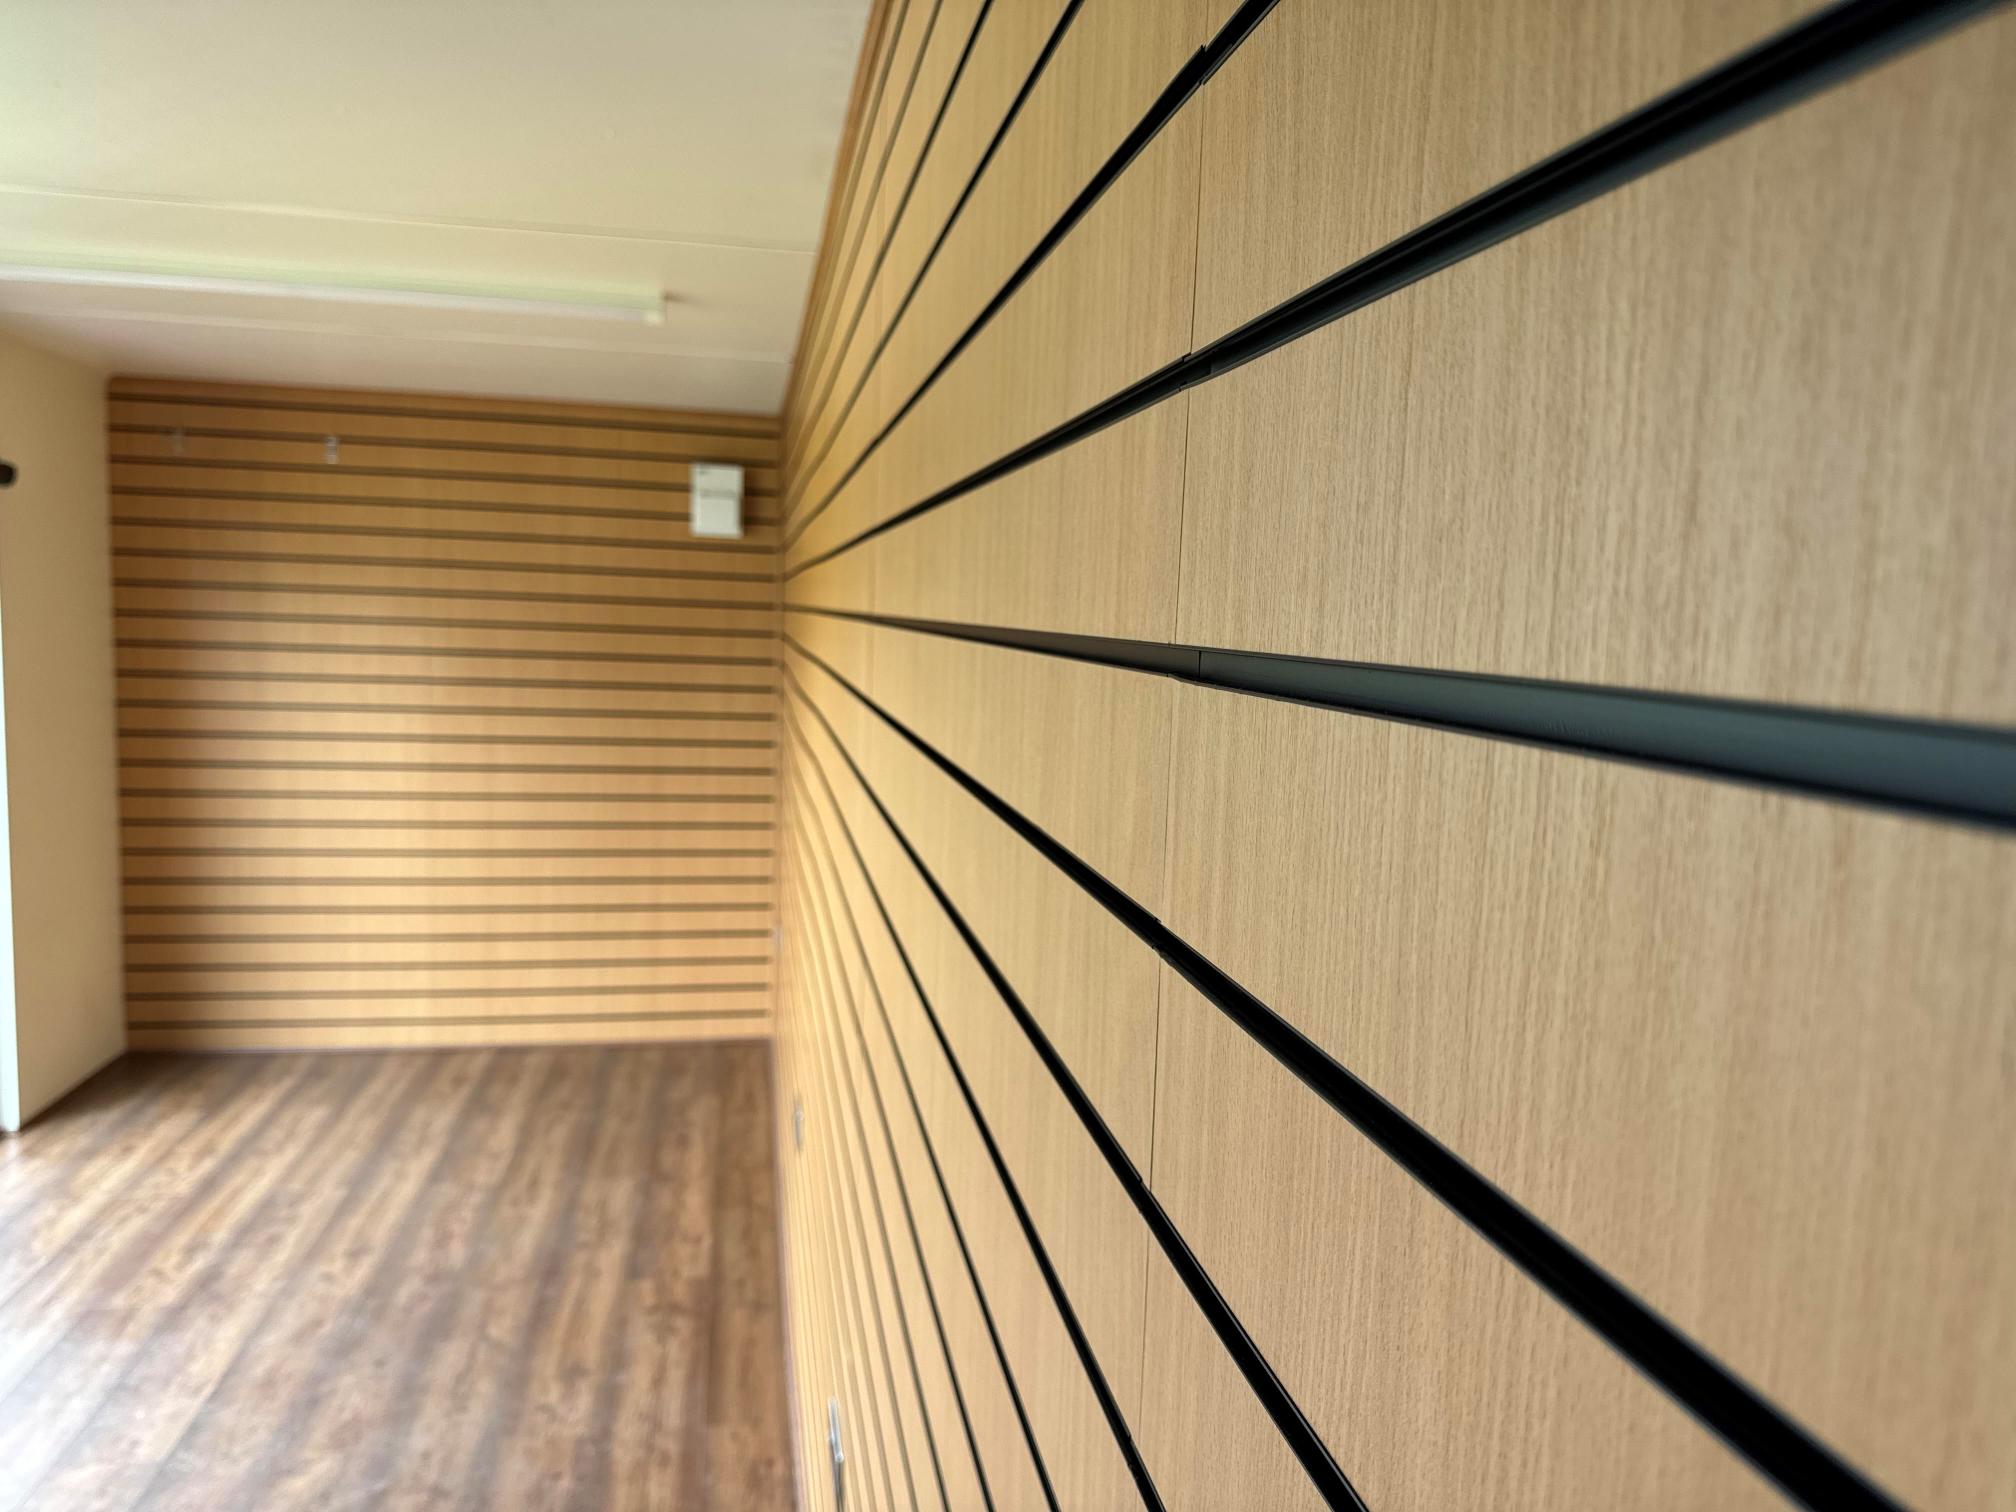
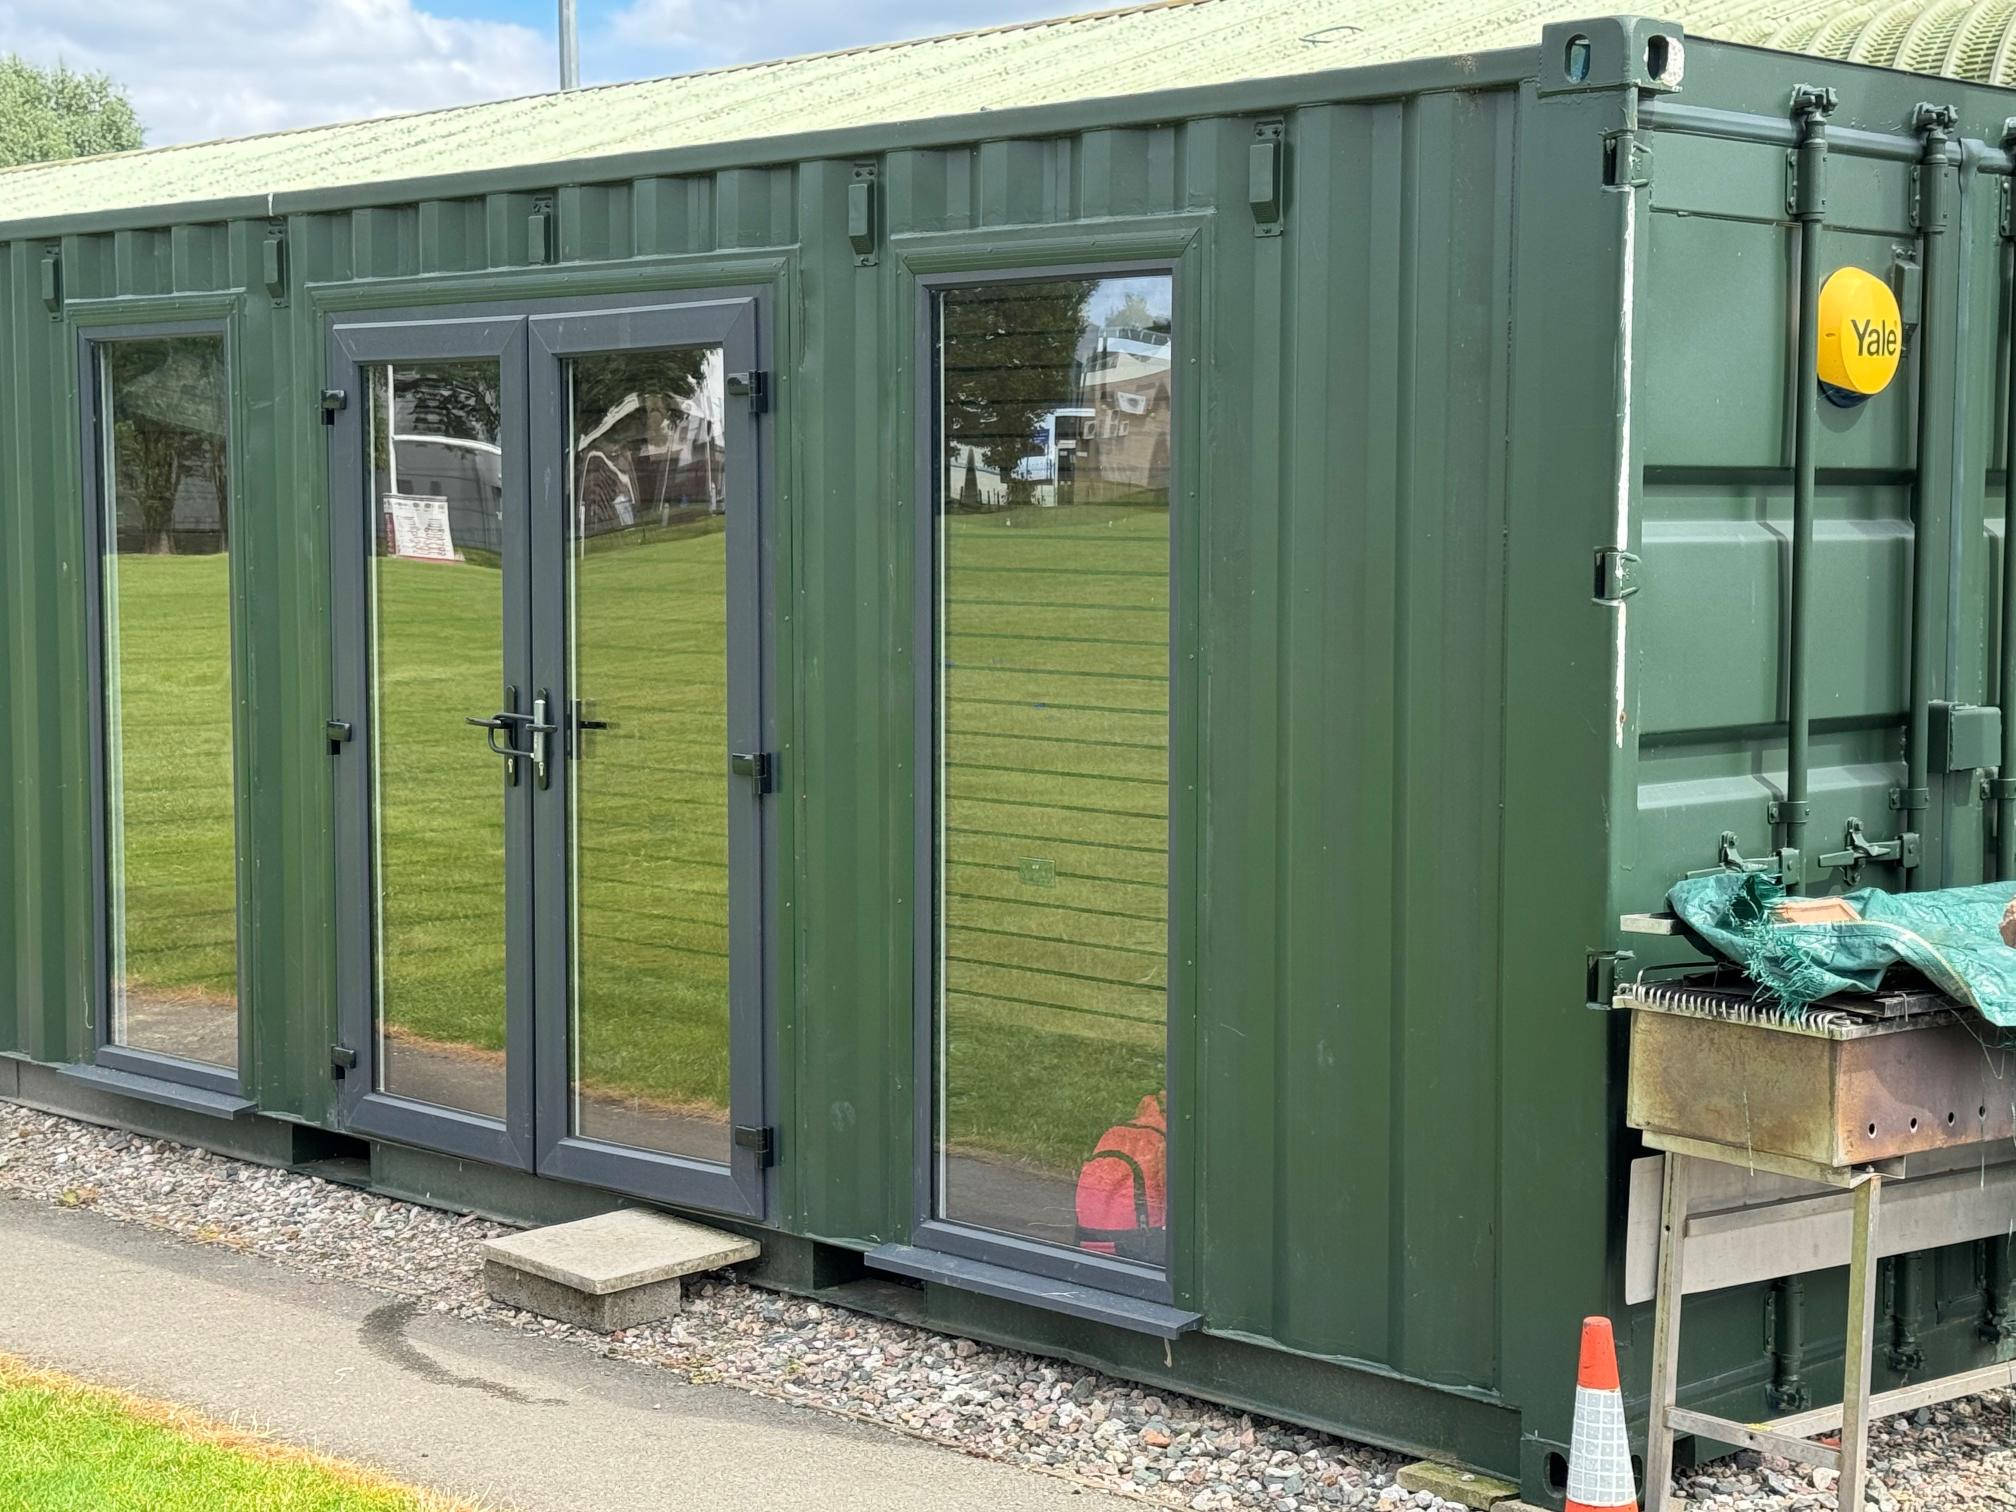
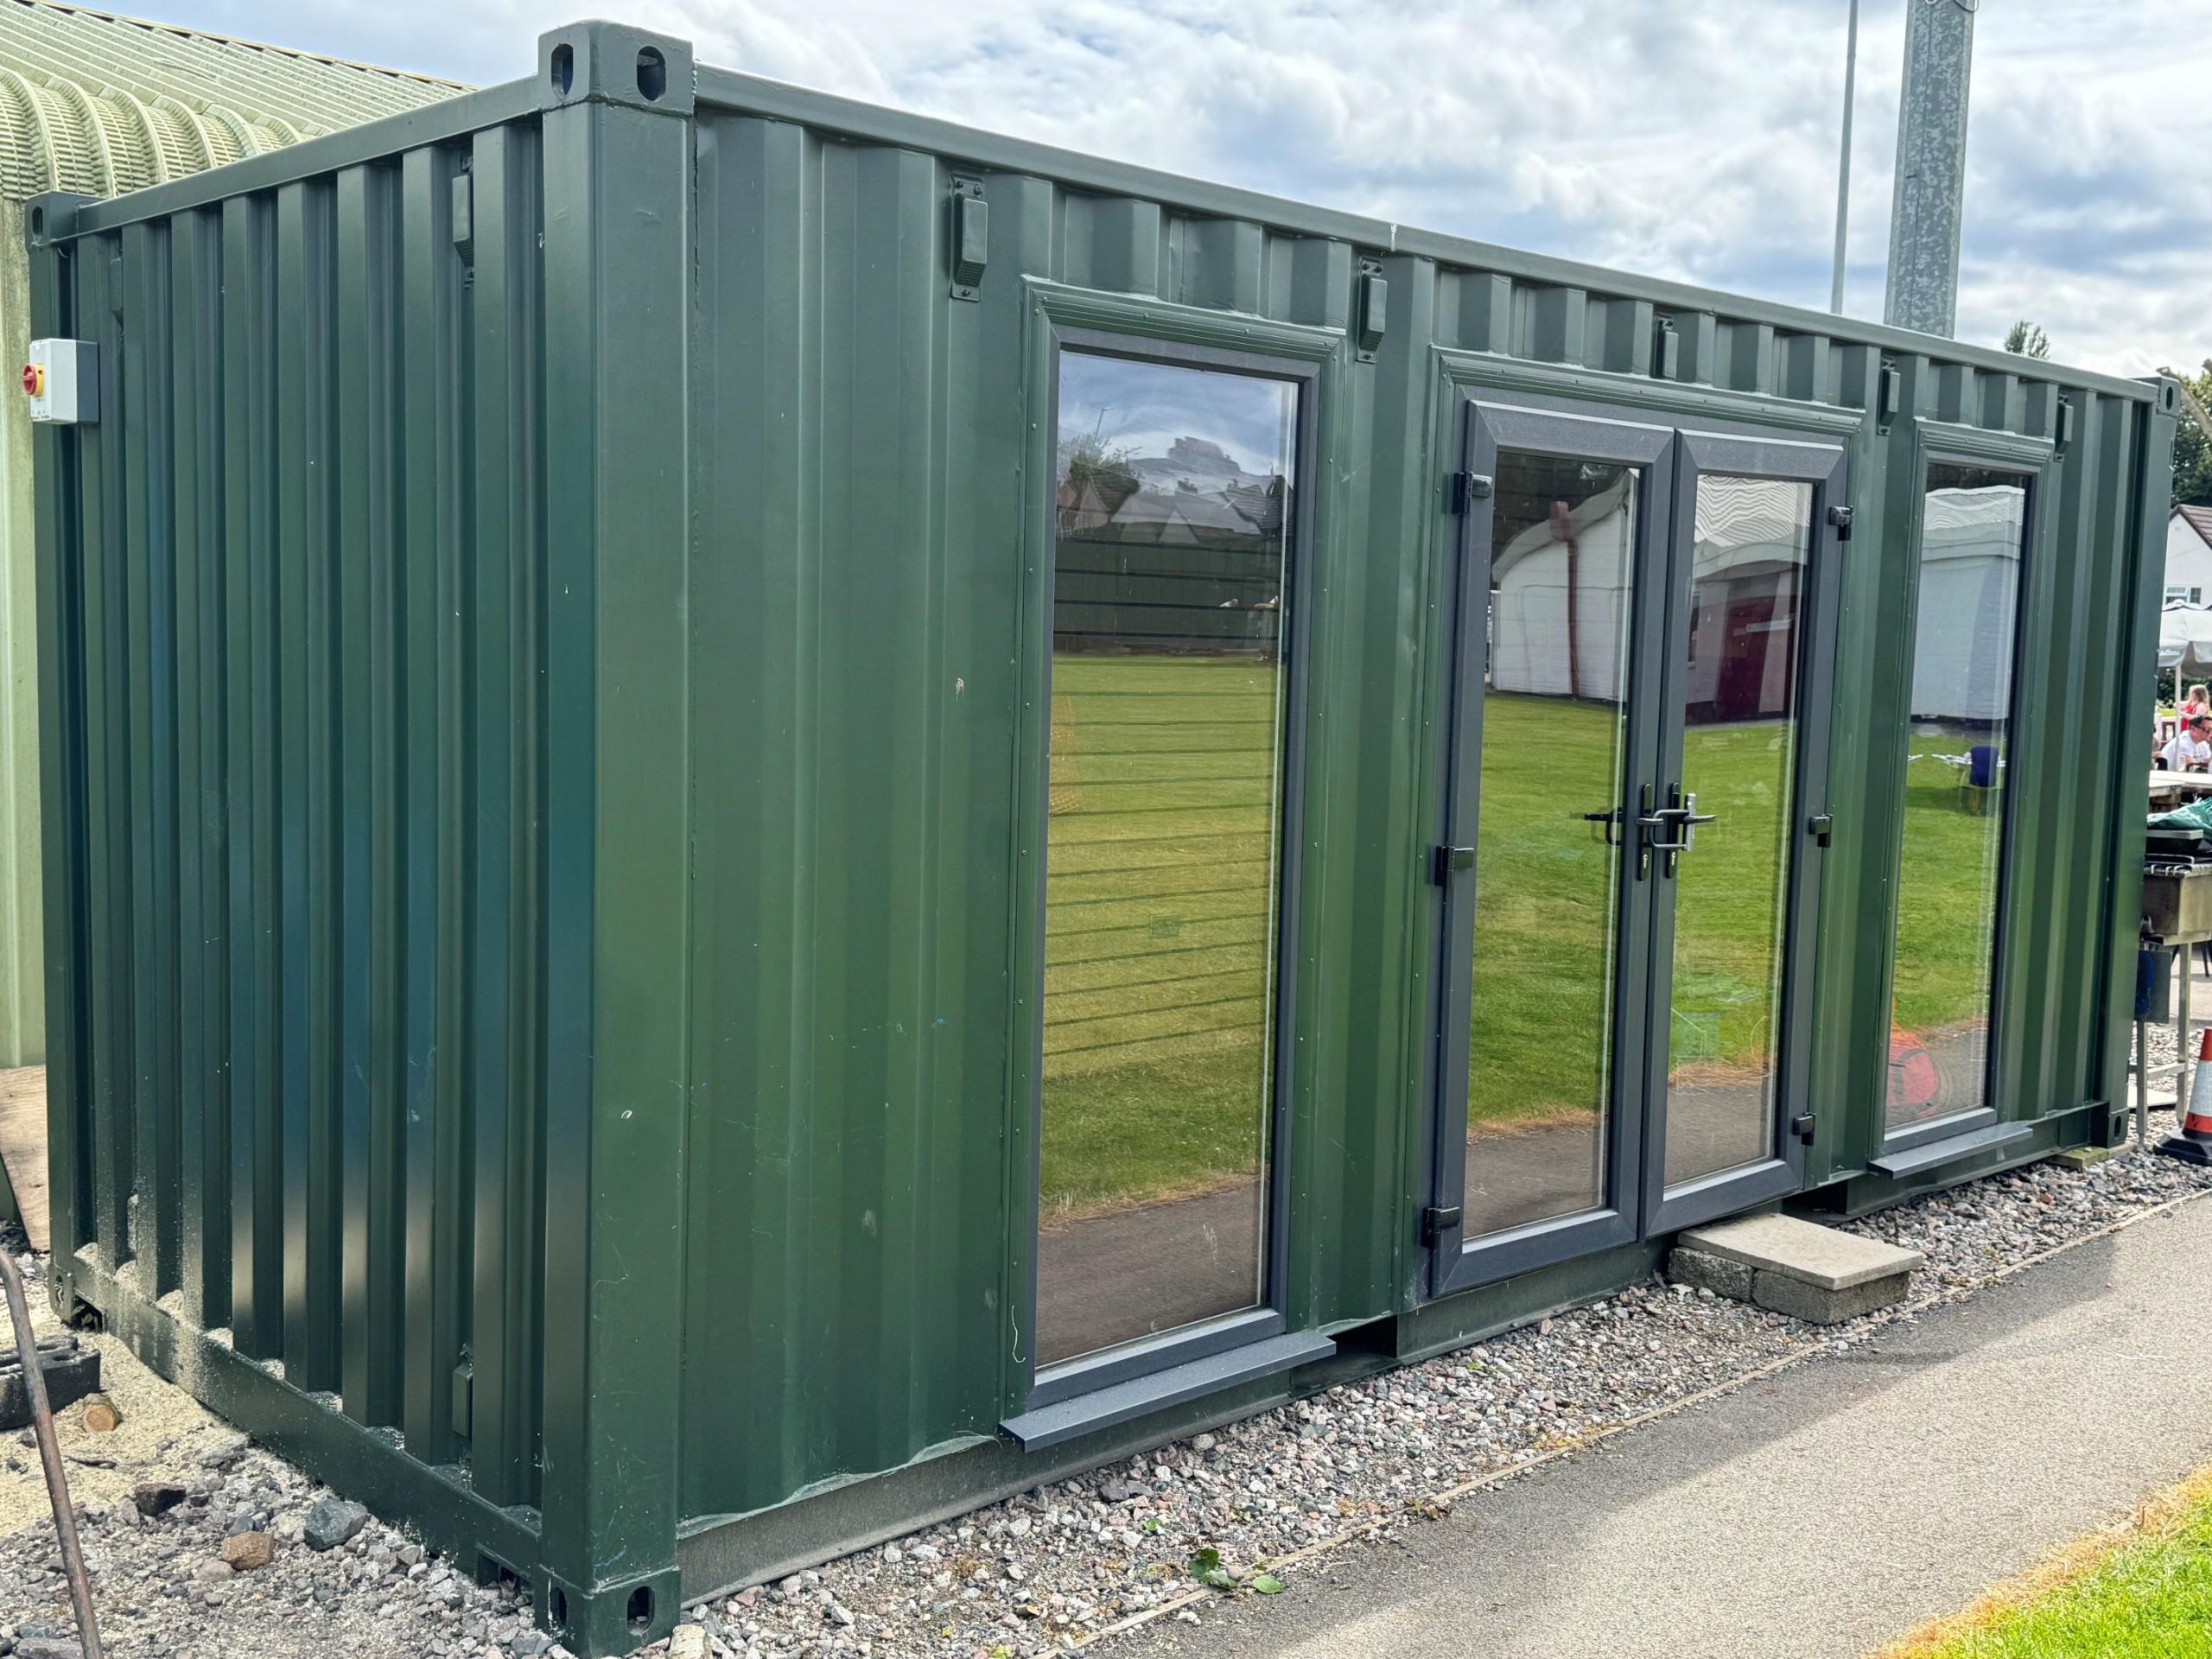
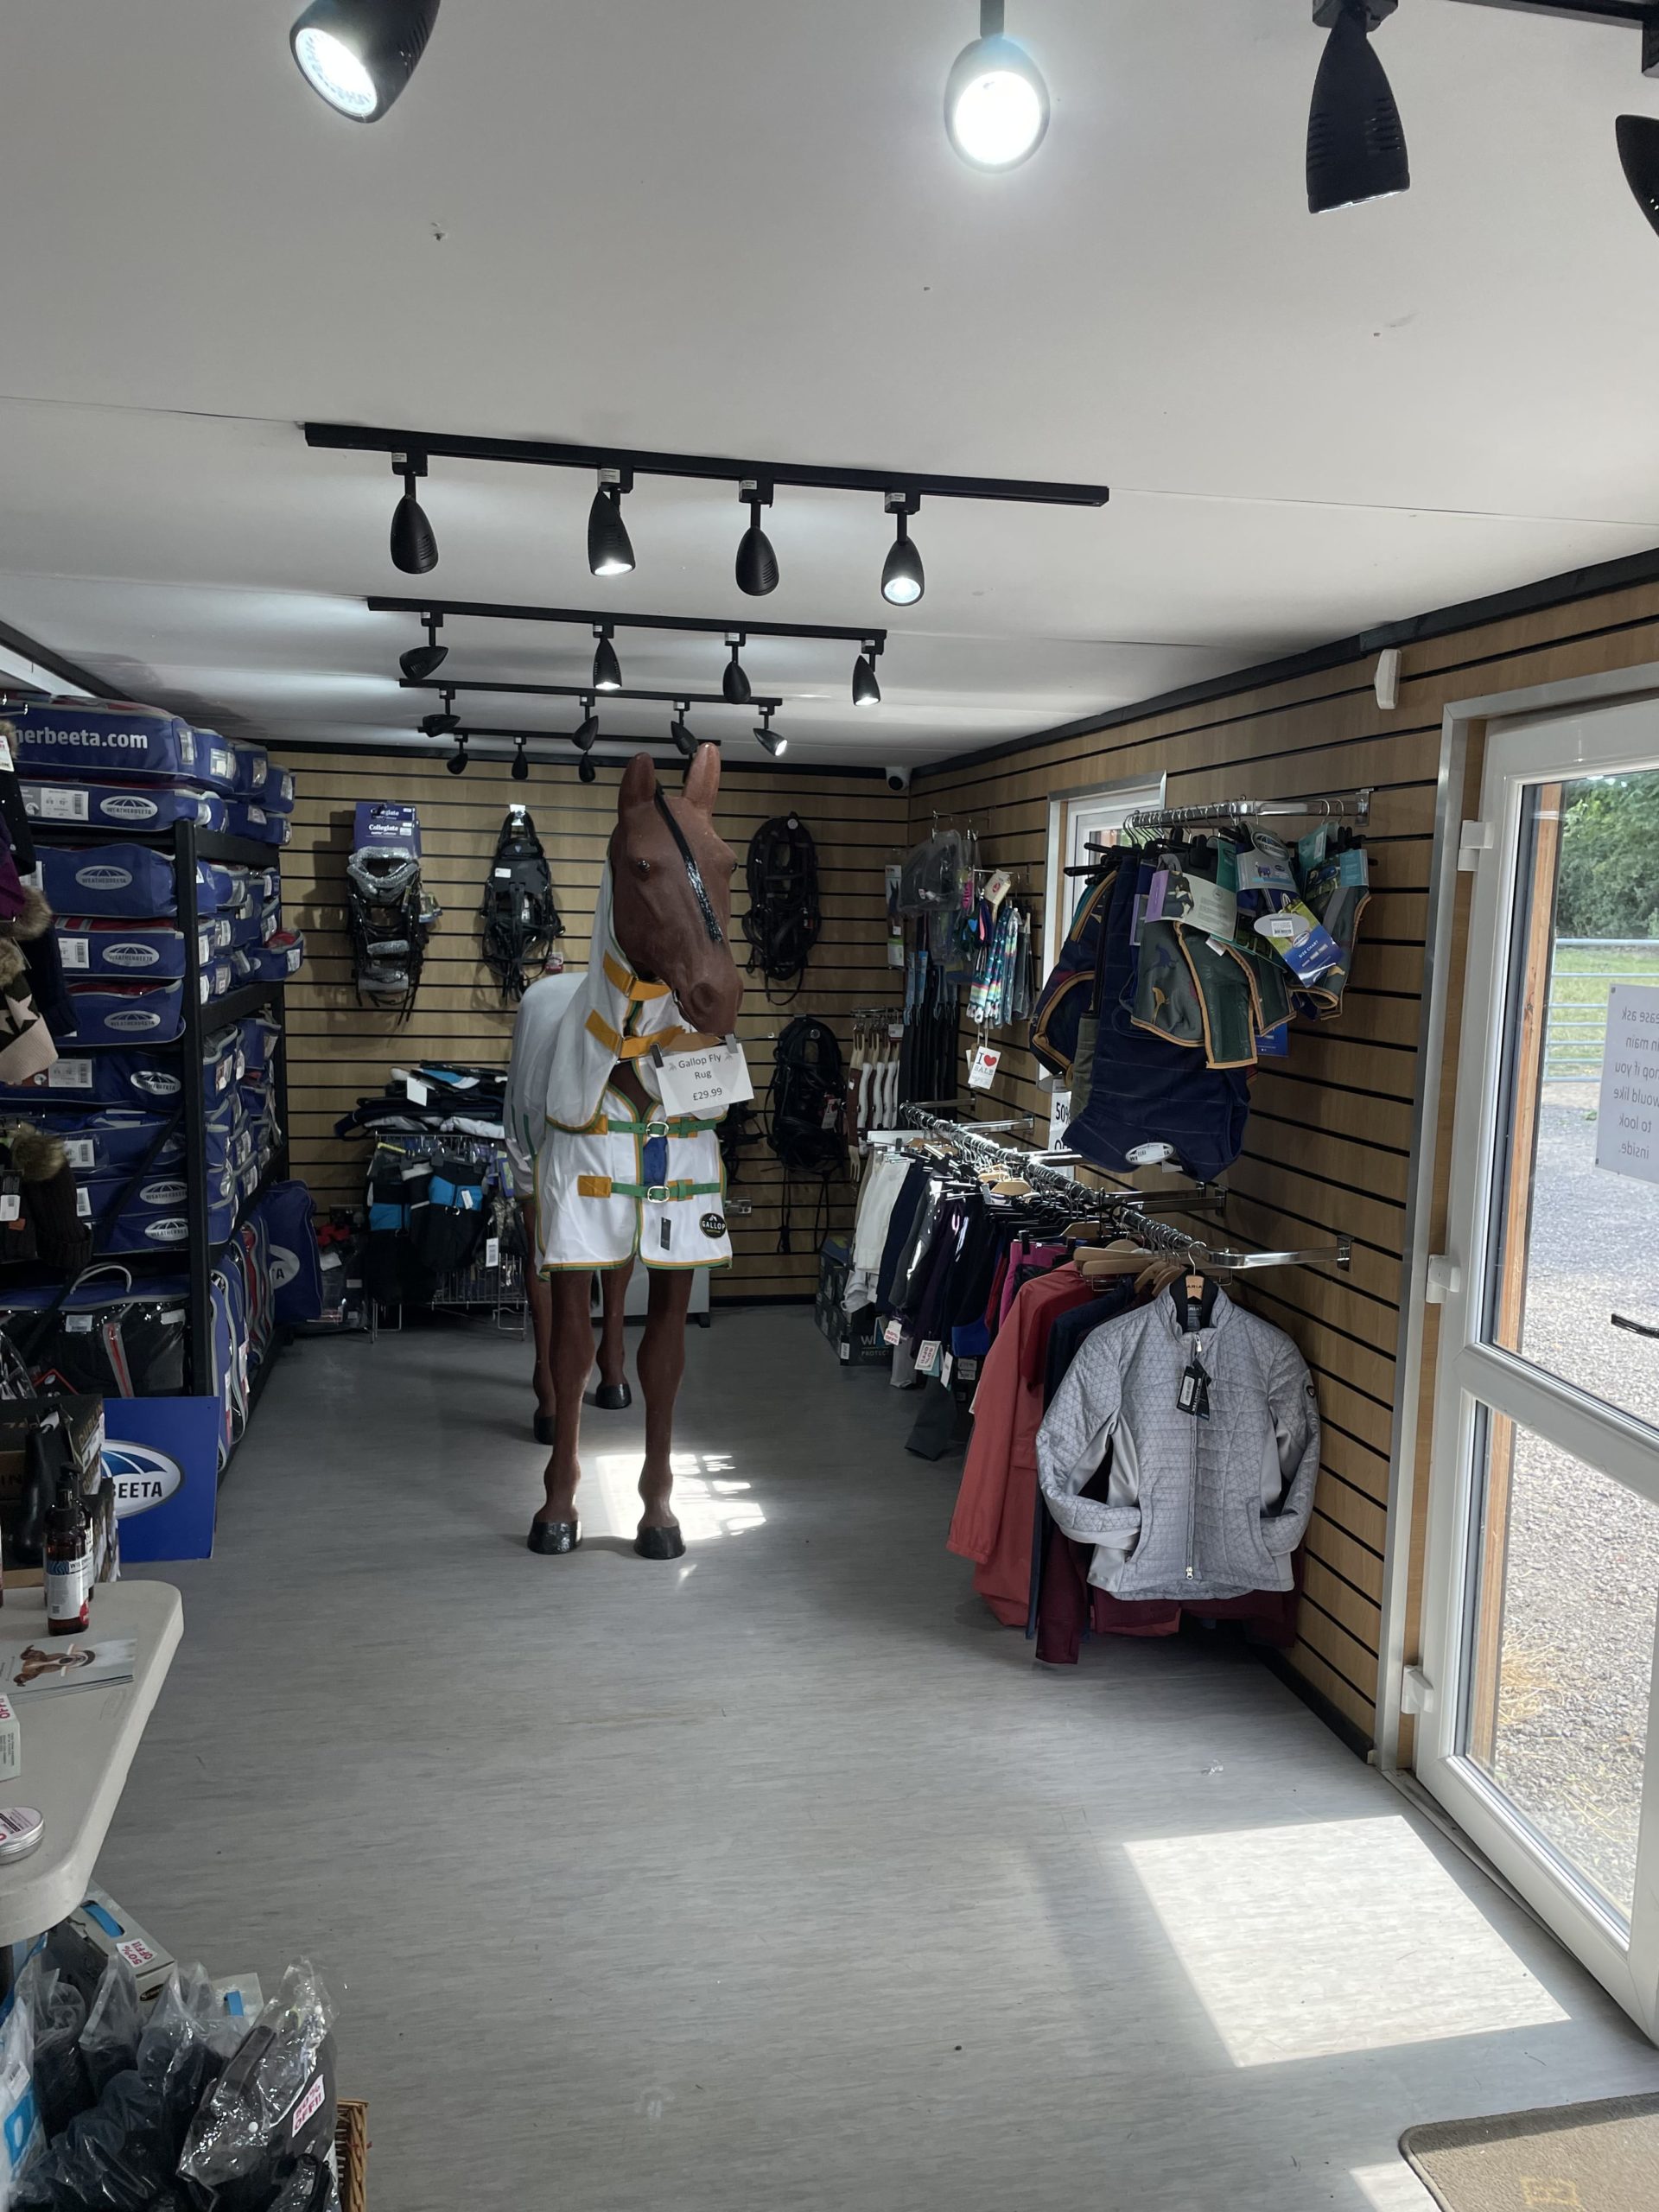
  • 20ft x 8ft Container Conversion Retail Shop

  • UPVC Double glazed Windows + French Doors

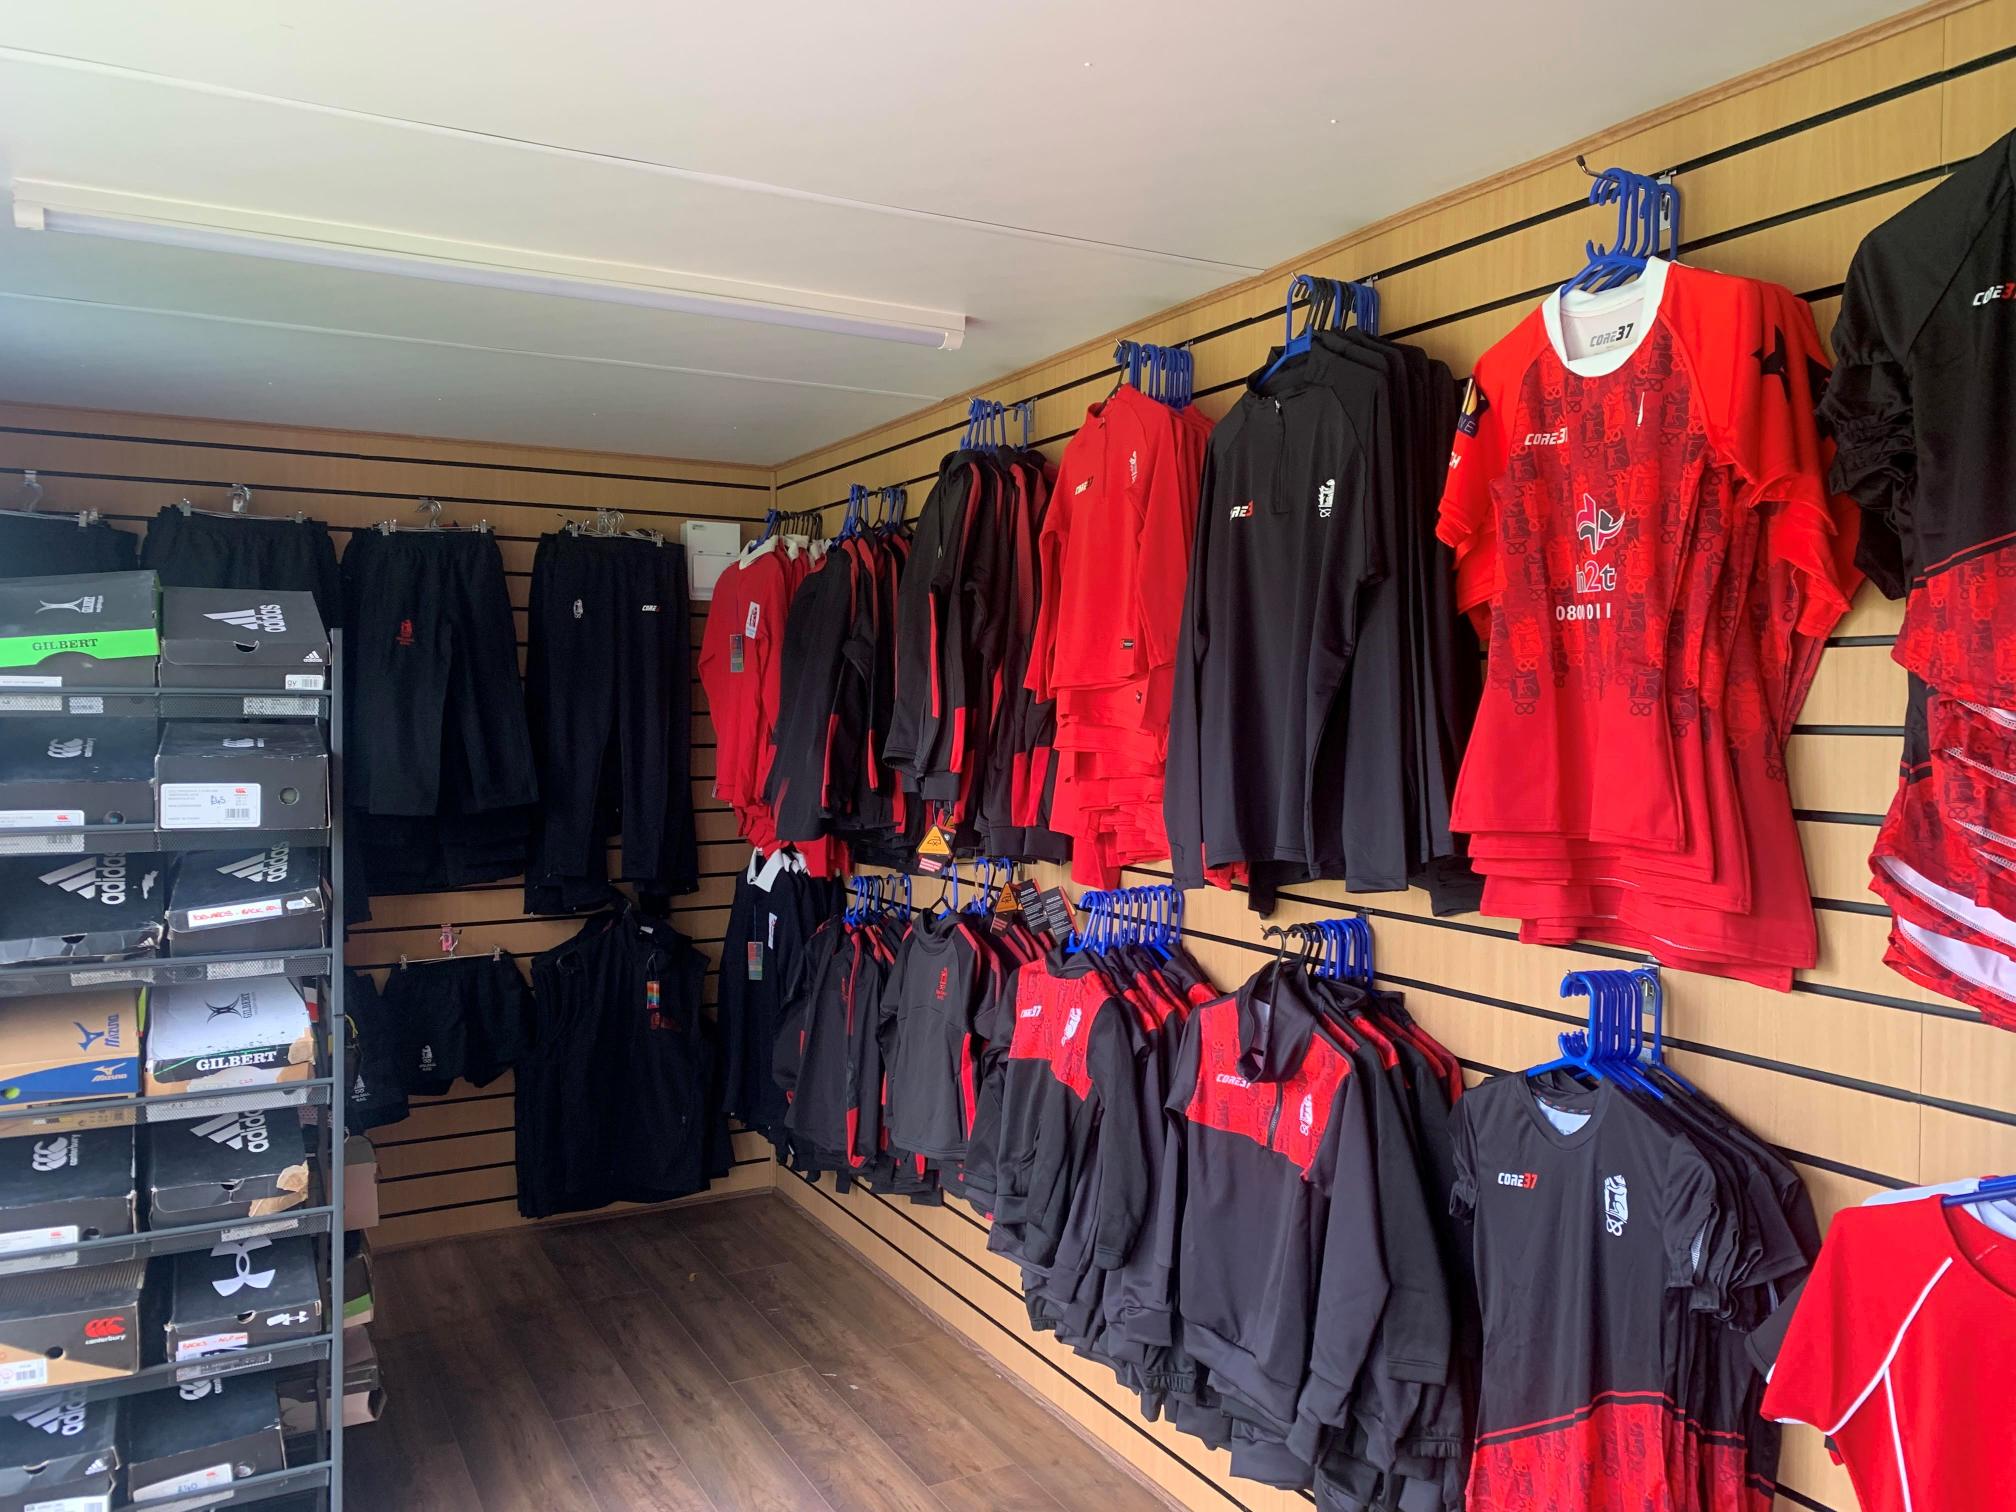
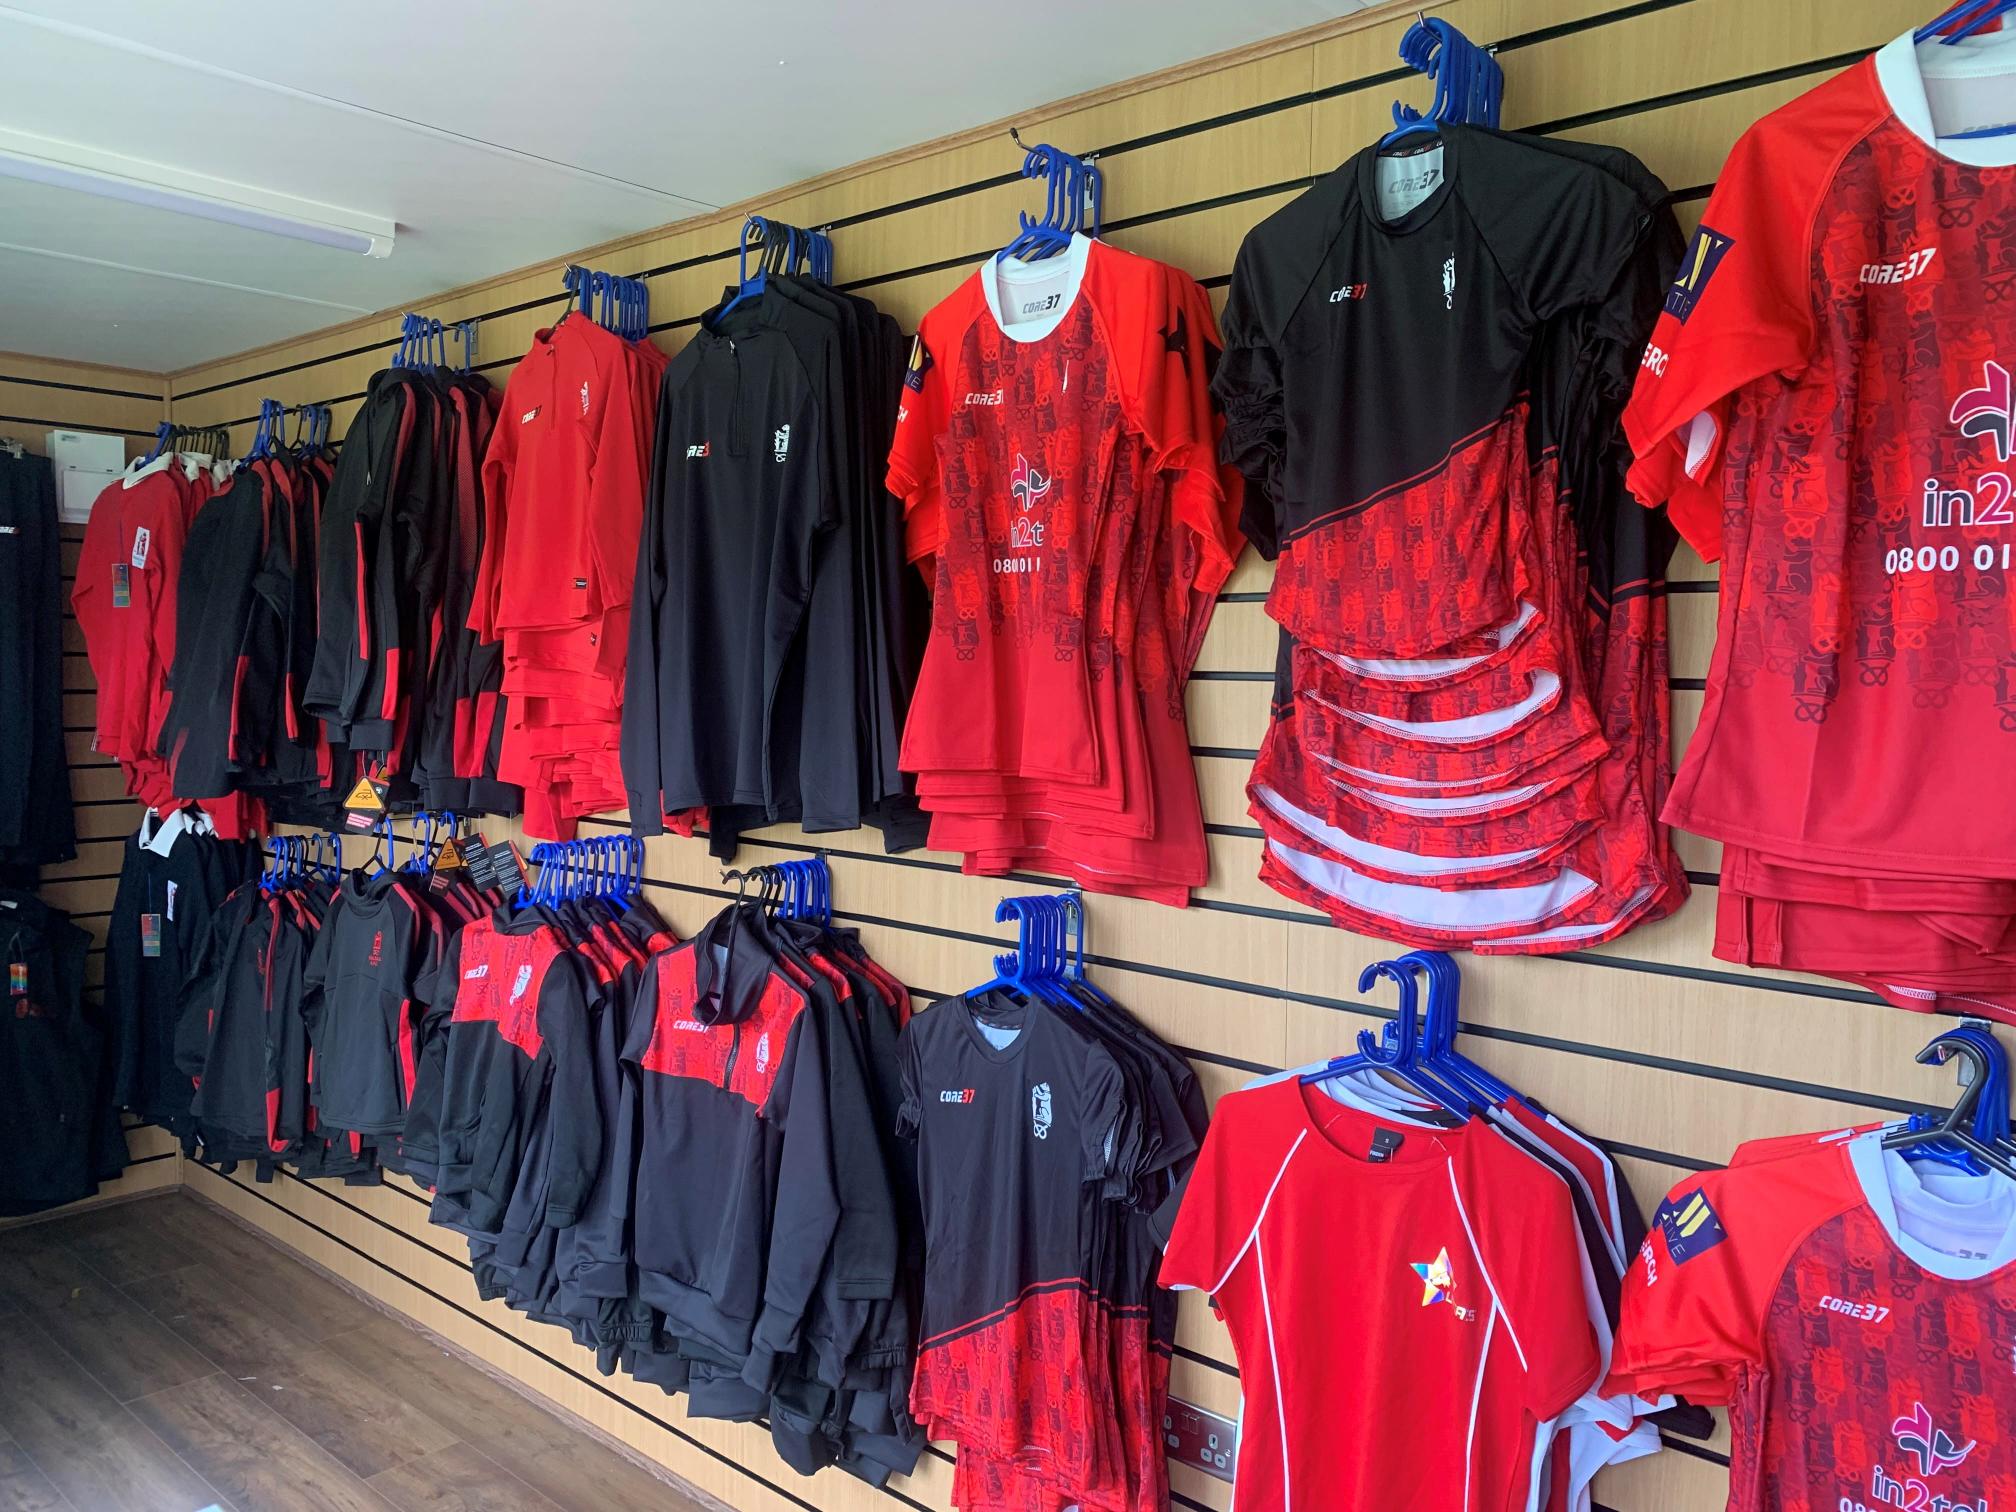
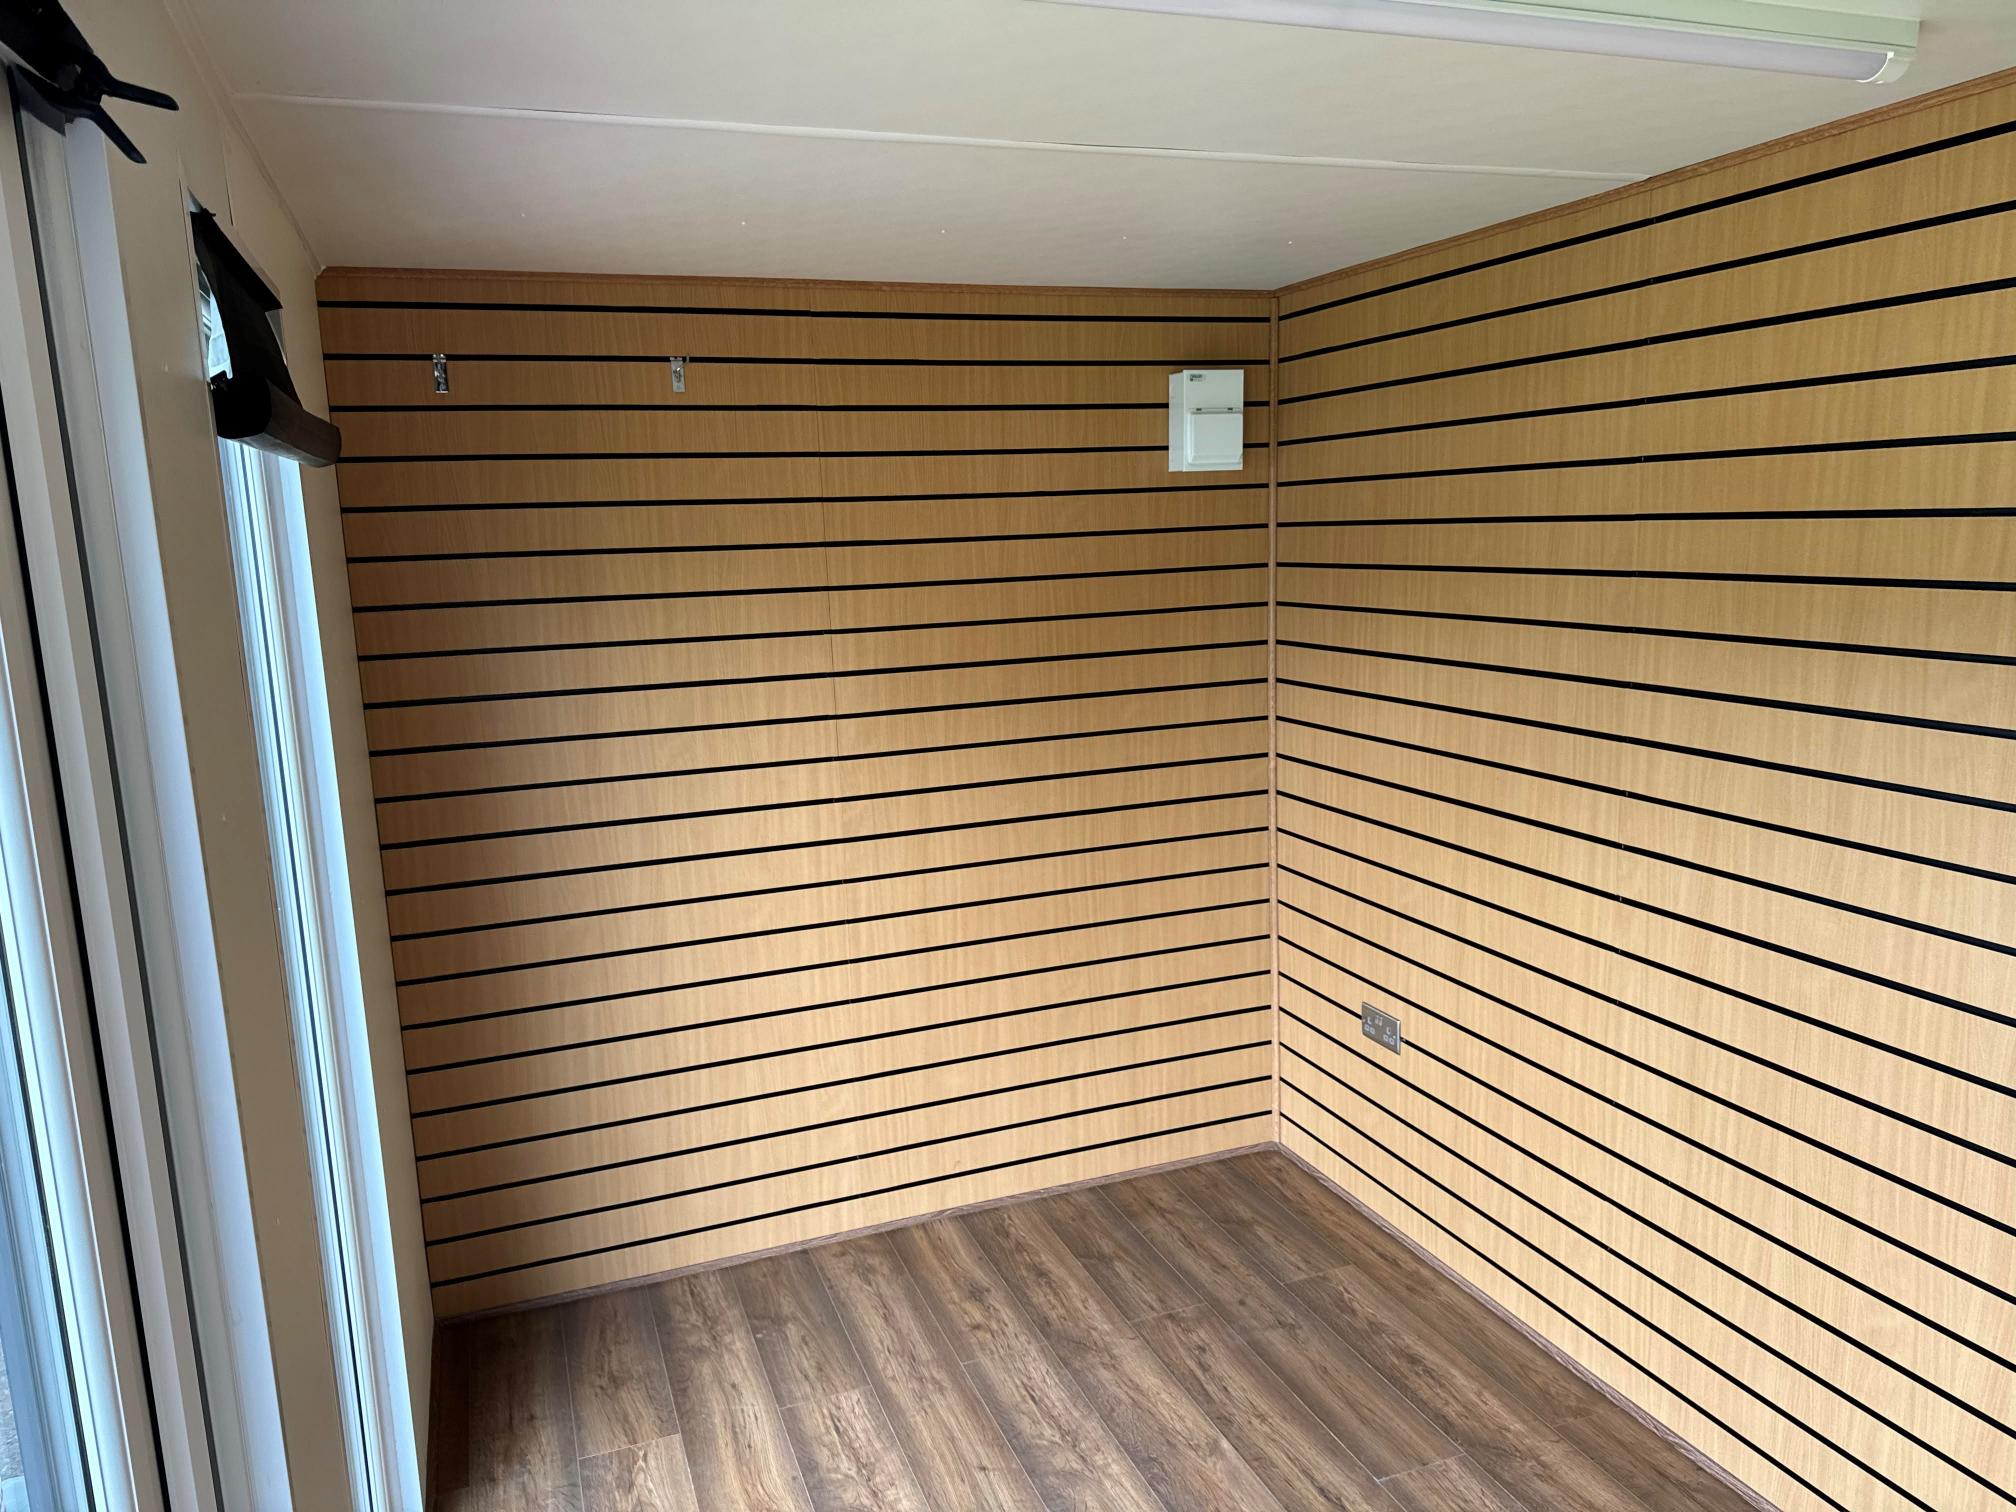
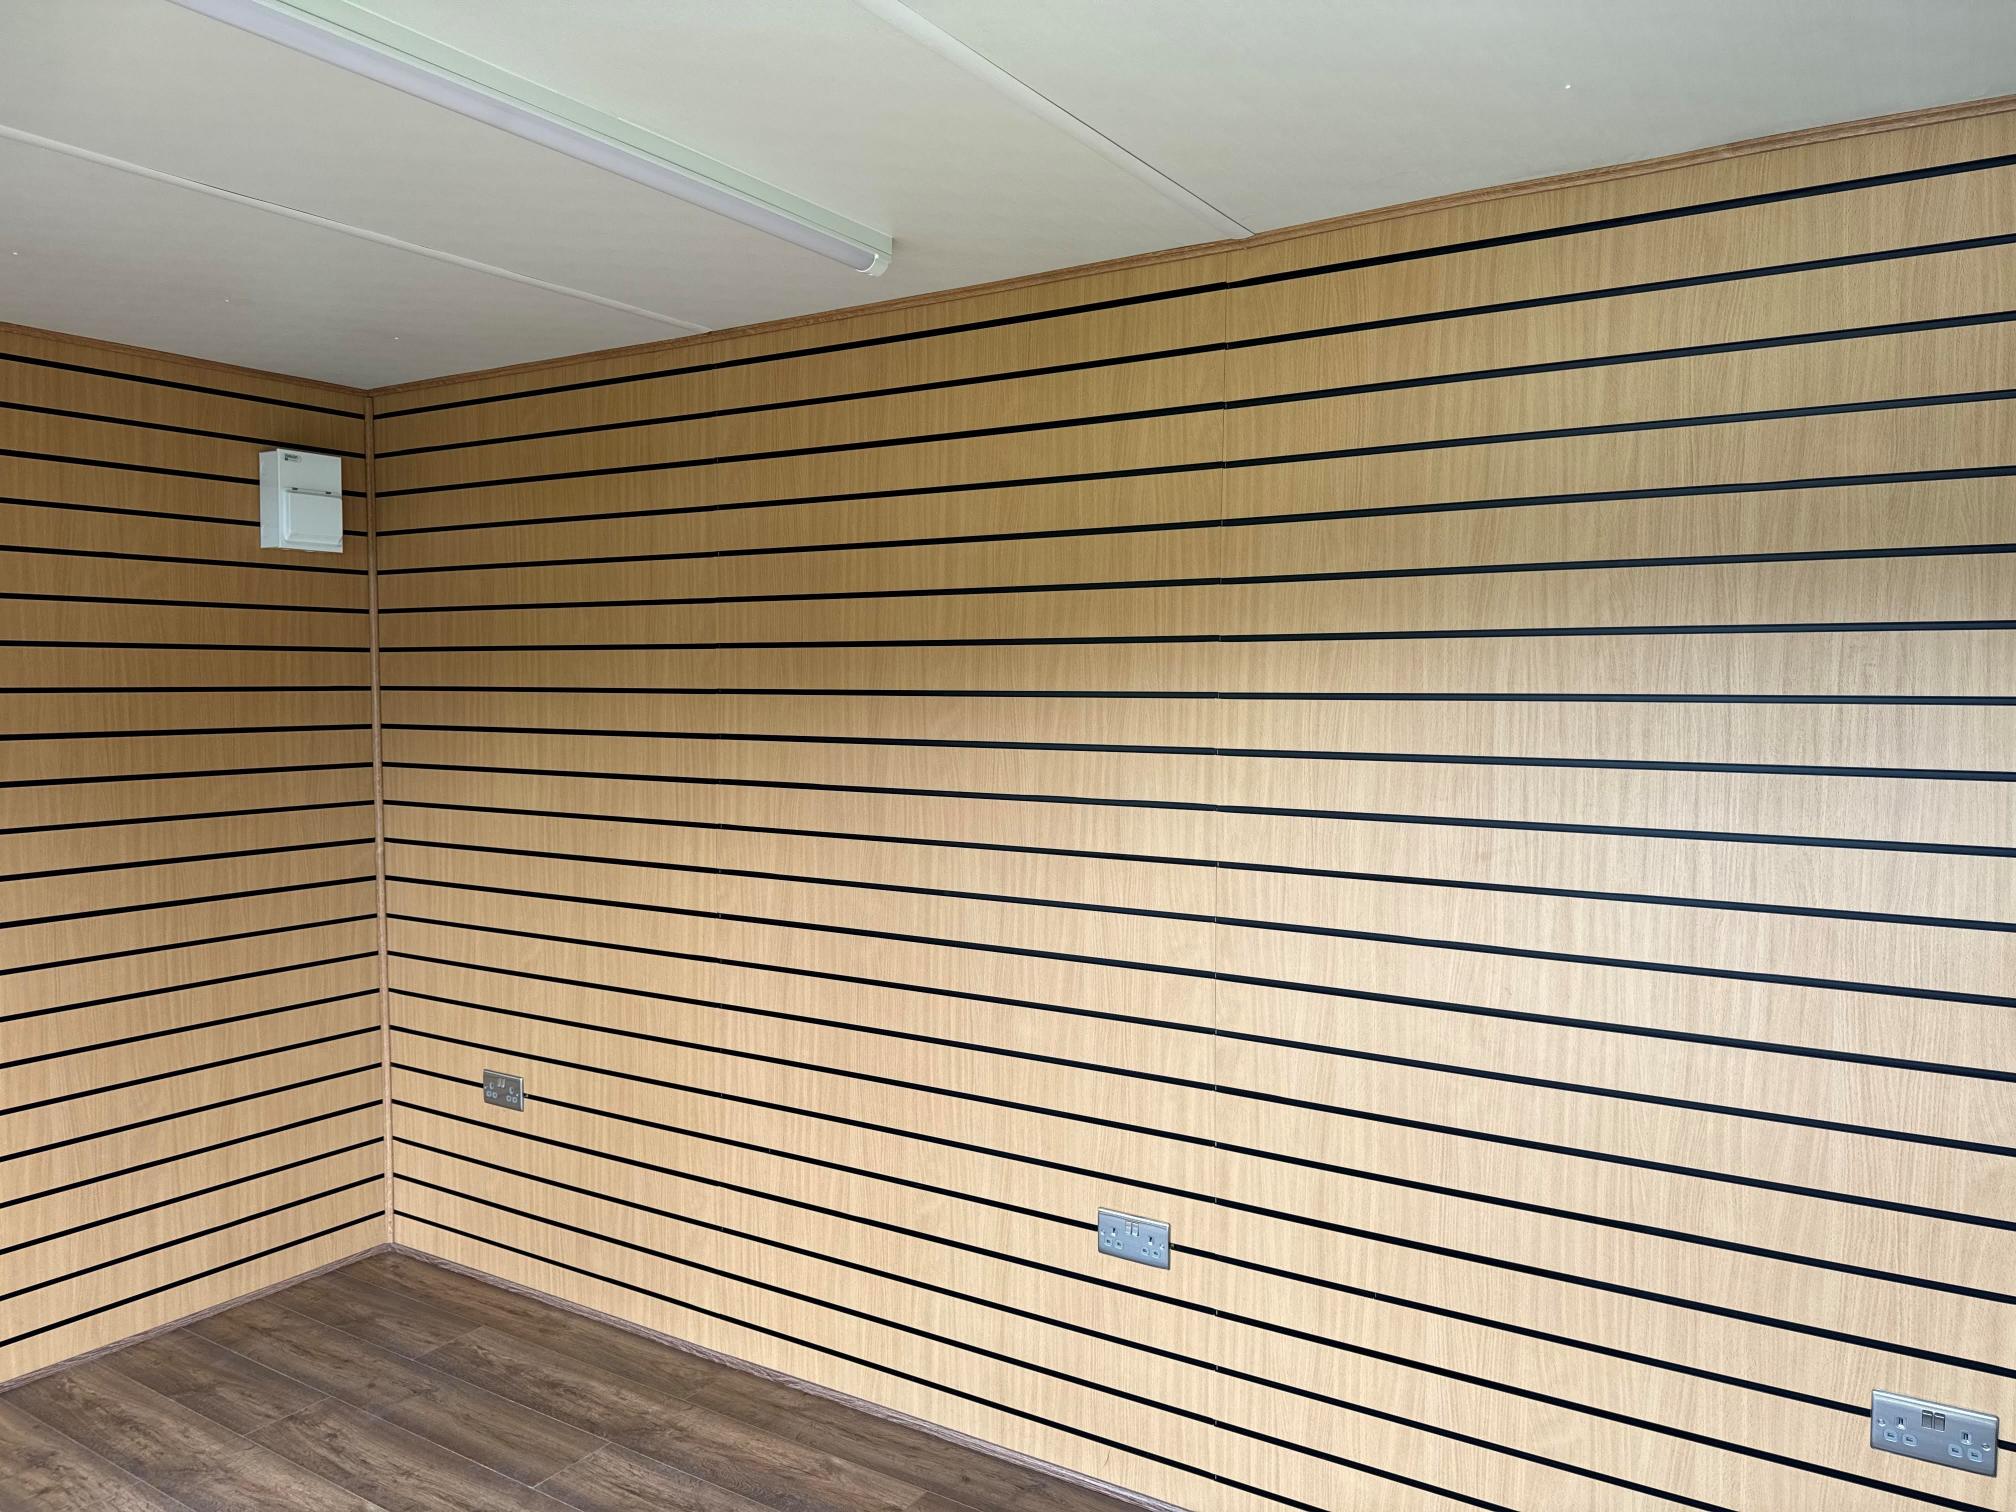
  • Slat Wall for retail fixings and Merchandise

  • Electric Chrome Sockets, led lighting and heating.

  • Laminate Flooring

  • 12 months Warranty

  • Maintenance call out package included

  • Less than 2 years old

  • Still in Brand New Condition

Location: Nationwide

POA

Not Available for Hire

Call for an instant quote!

32ft x 10ft Jack Leg Cabin

  • Fully refurbished

  • Colour light grey

  • Slate grey anthracite upvc double glazed windows

Location: Nationwide


£15,000

+ VAT

Not Available for Hire

Call for an instant quote!

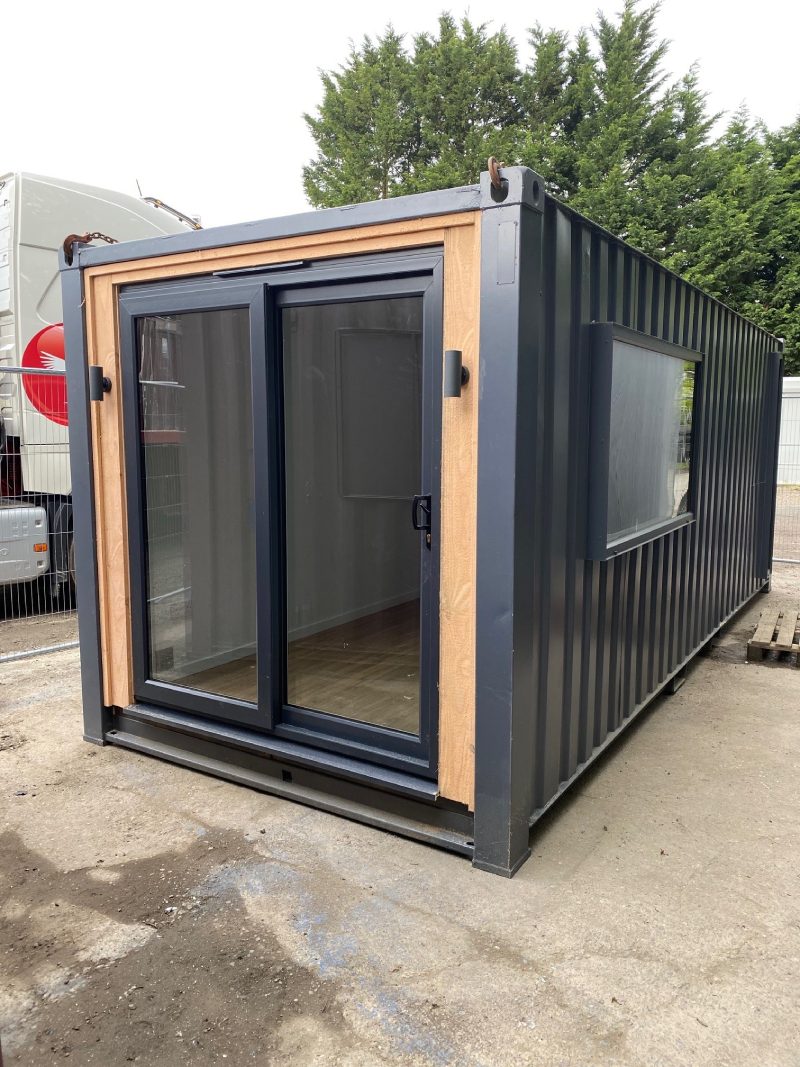
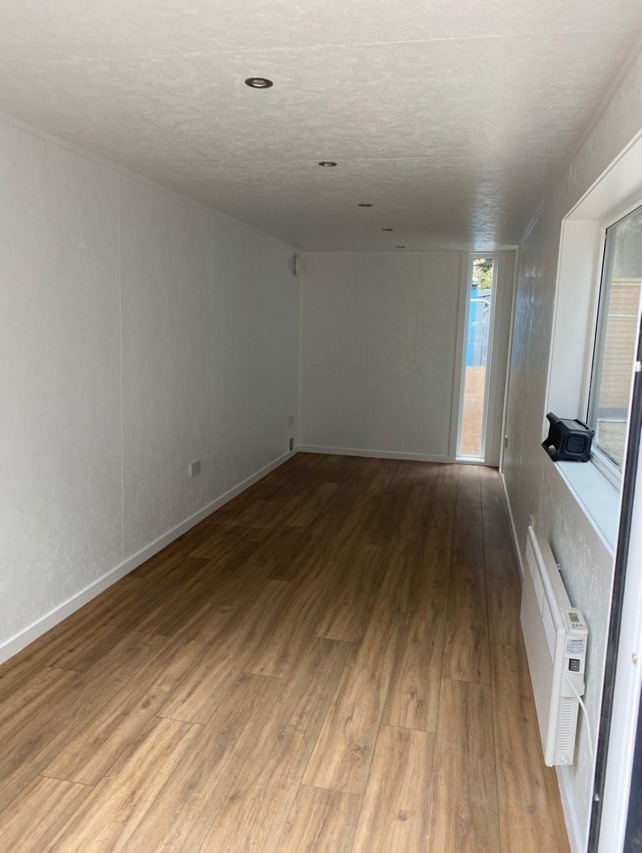
20ft x 8ft Container Office

  • Fully Insulated with electric sockets, spot lighting, and heating

  • Wood Flooring

  • UPVC Sliding Door + Windows

  • Lead Time for build 6-8 weeks

Location: Nationwide


£12,995.00

+ VAT

Not Available for Hire

Call for an instant quote!

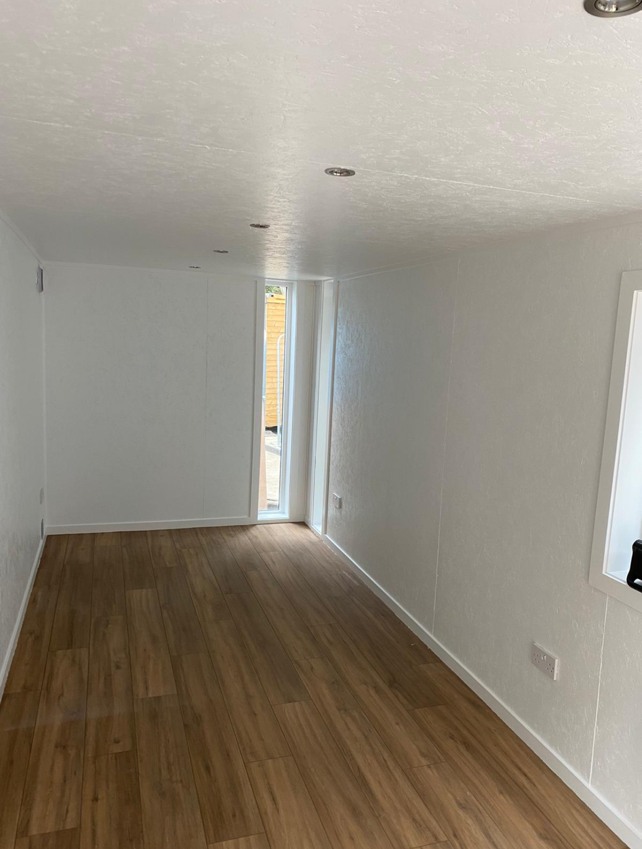
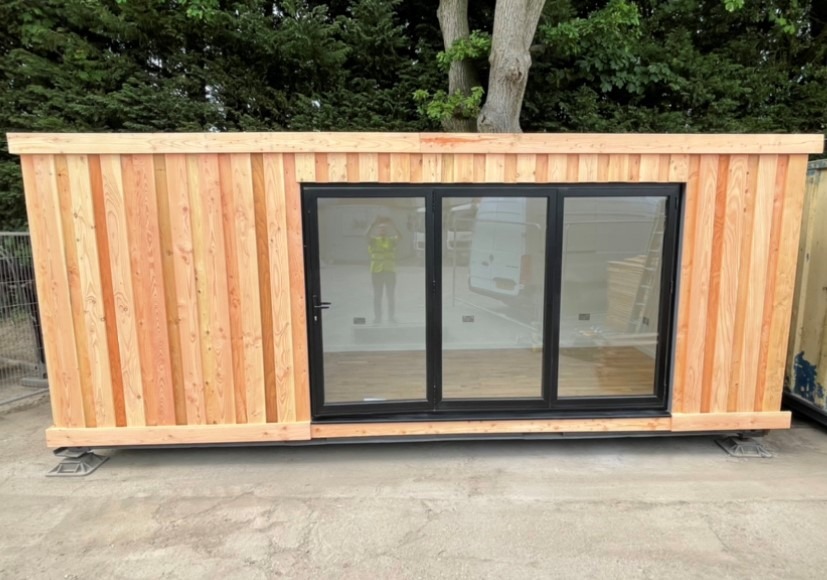
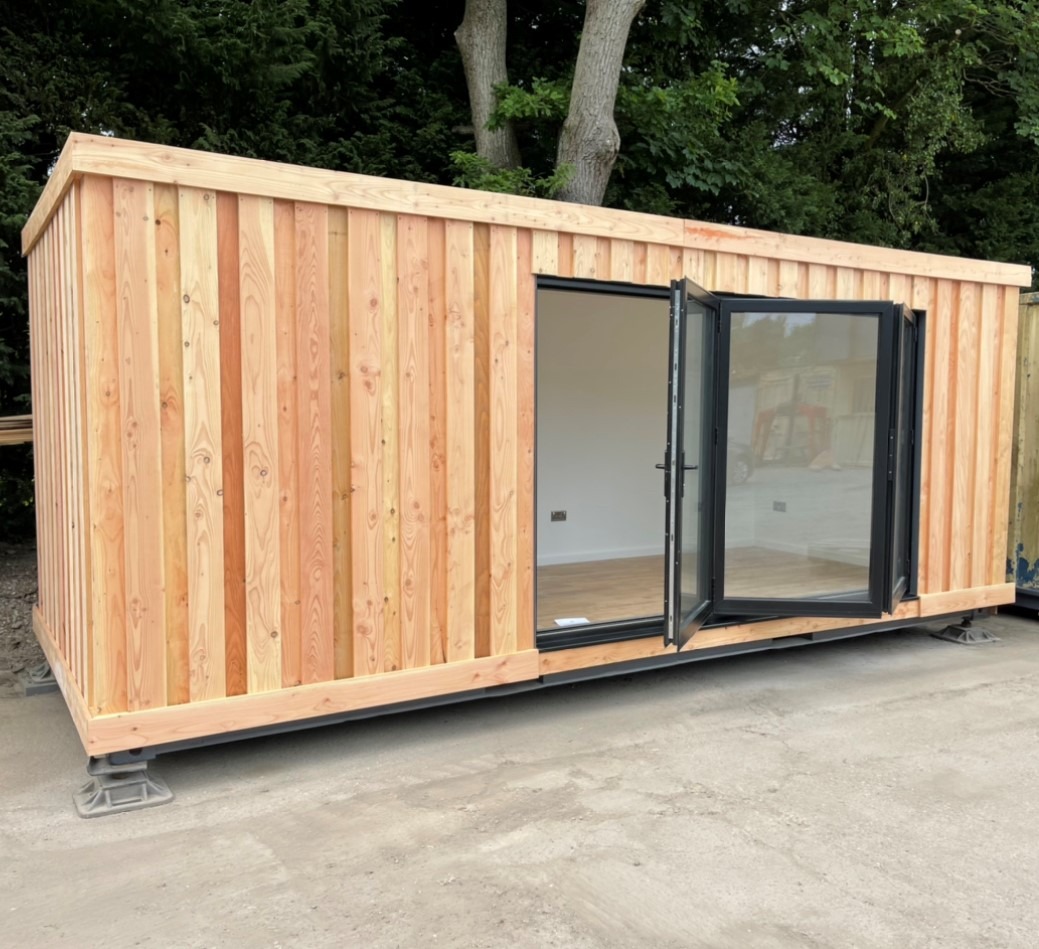
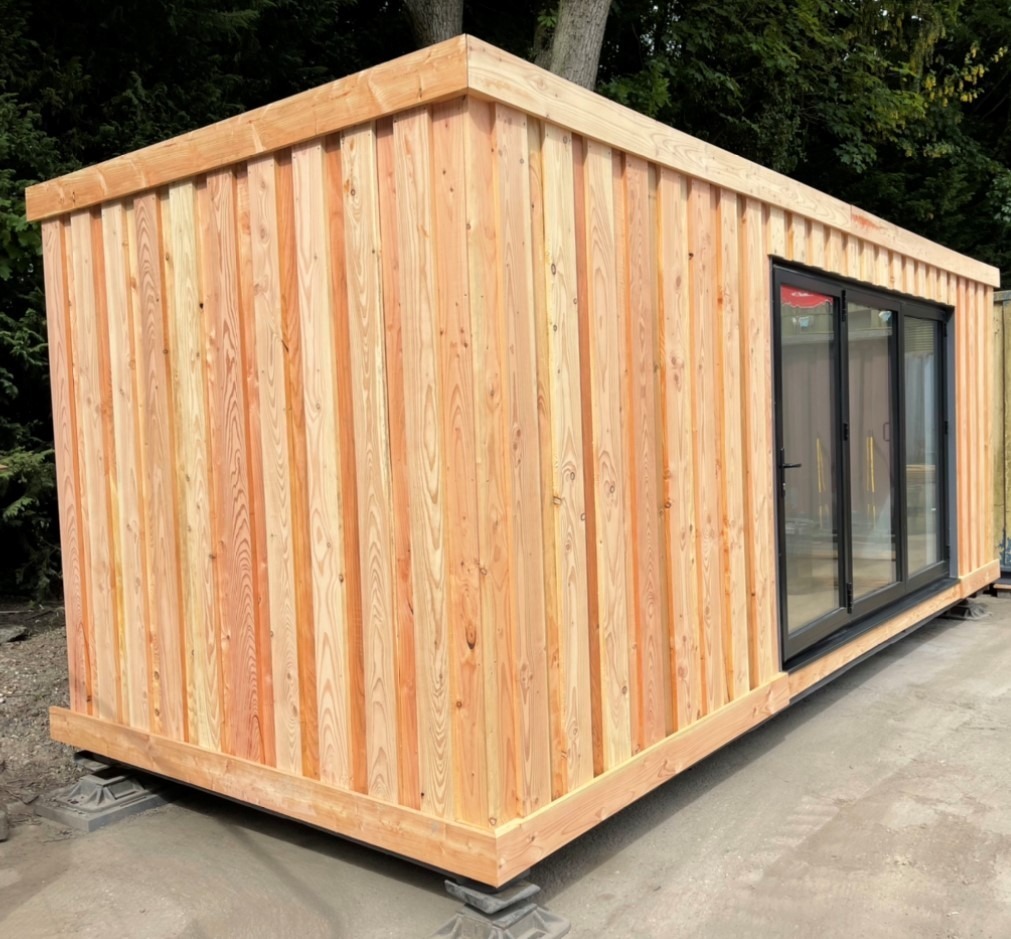
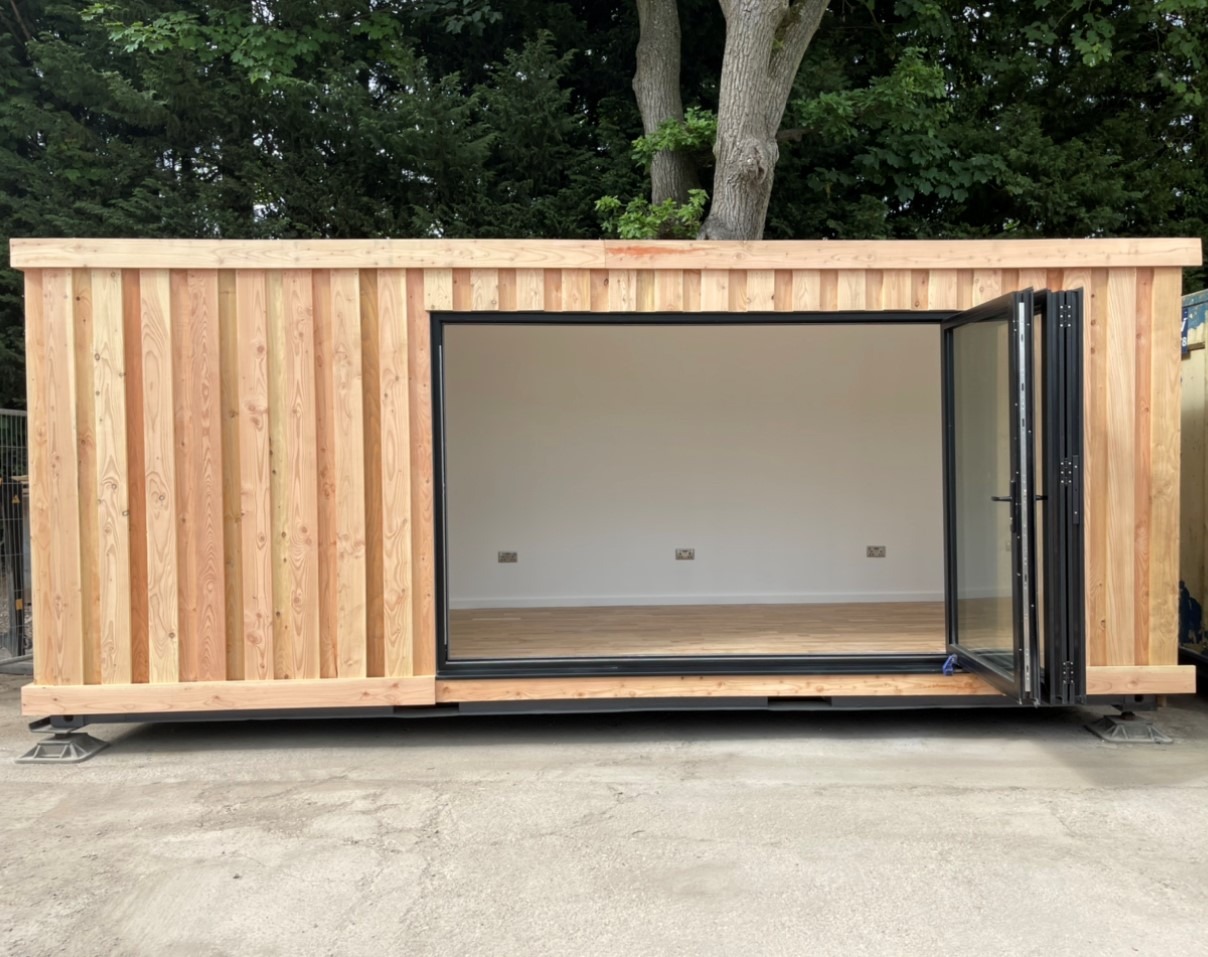
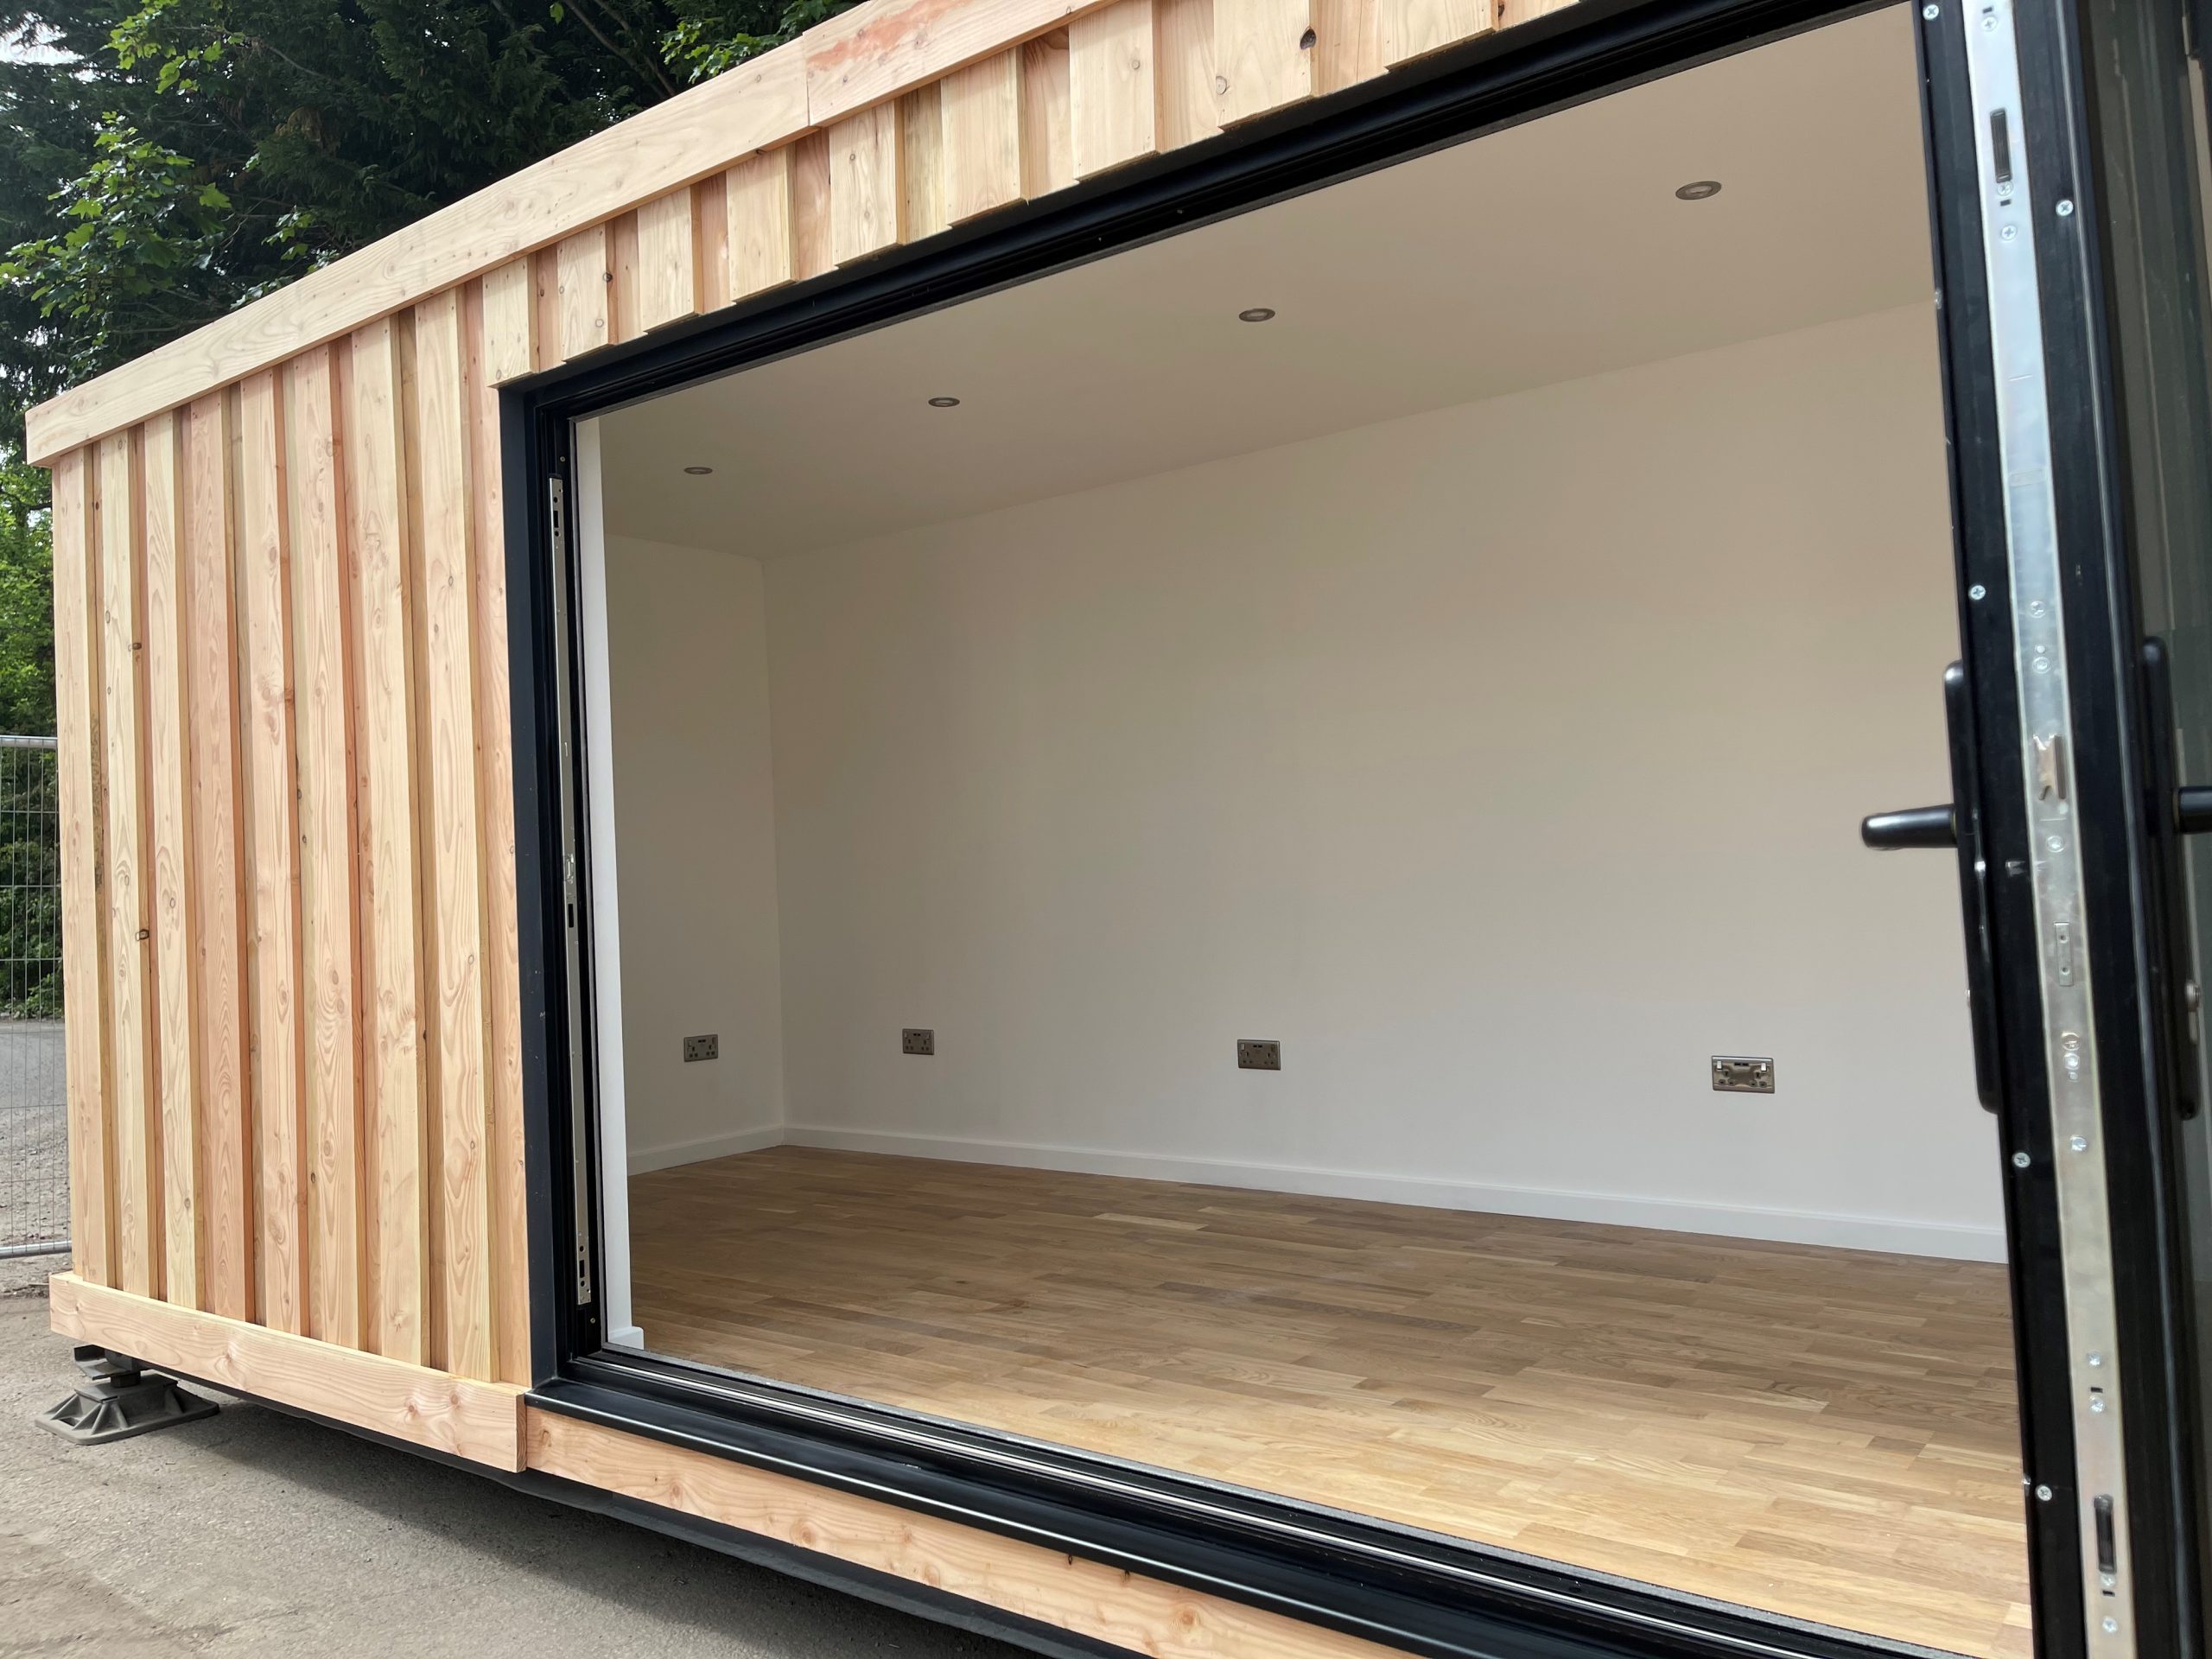
20ft x 8ft Container Office

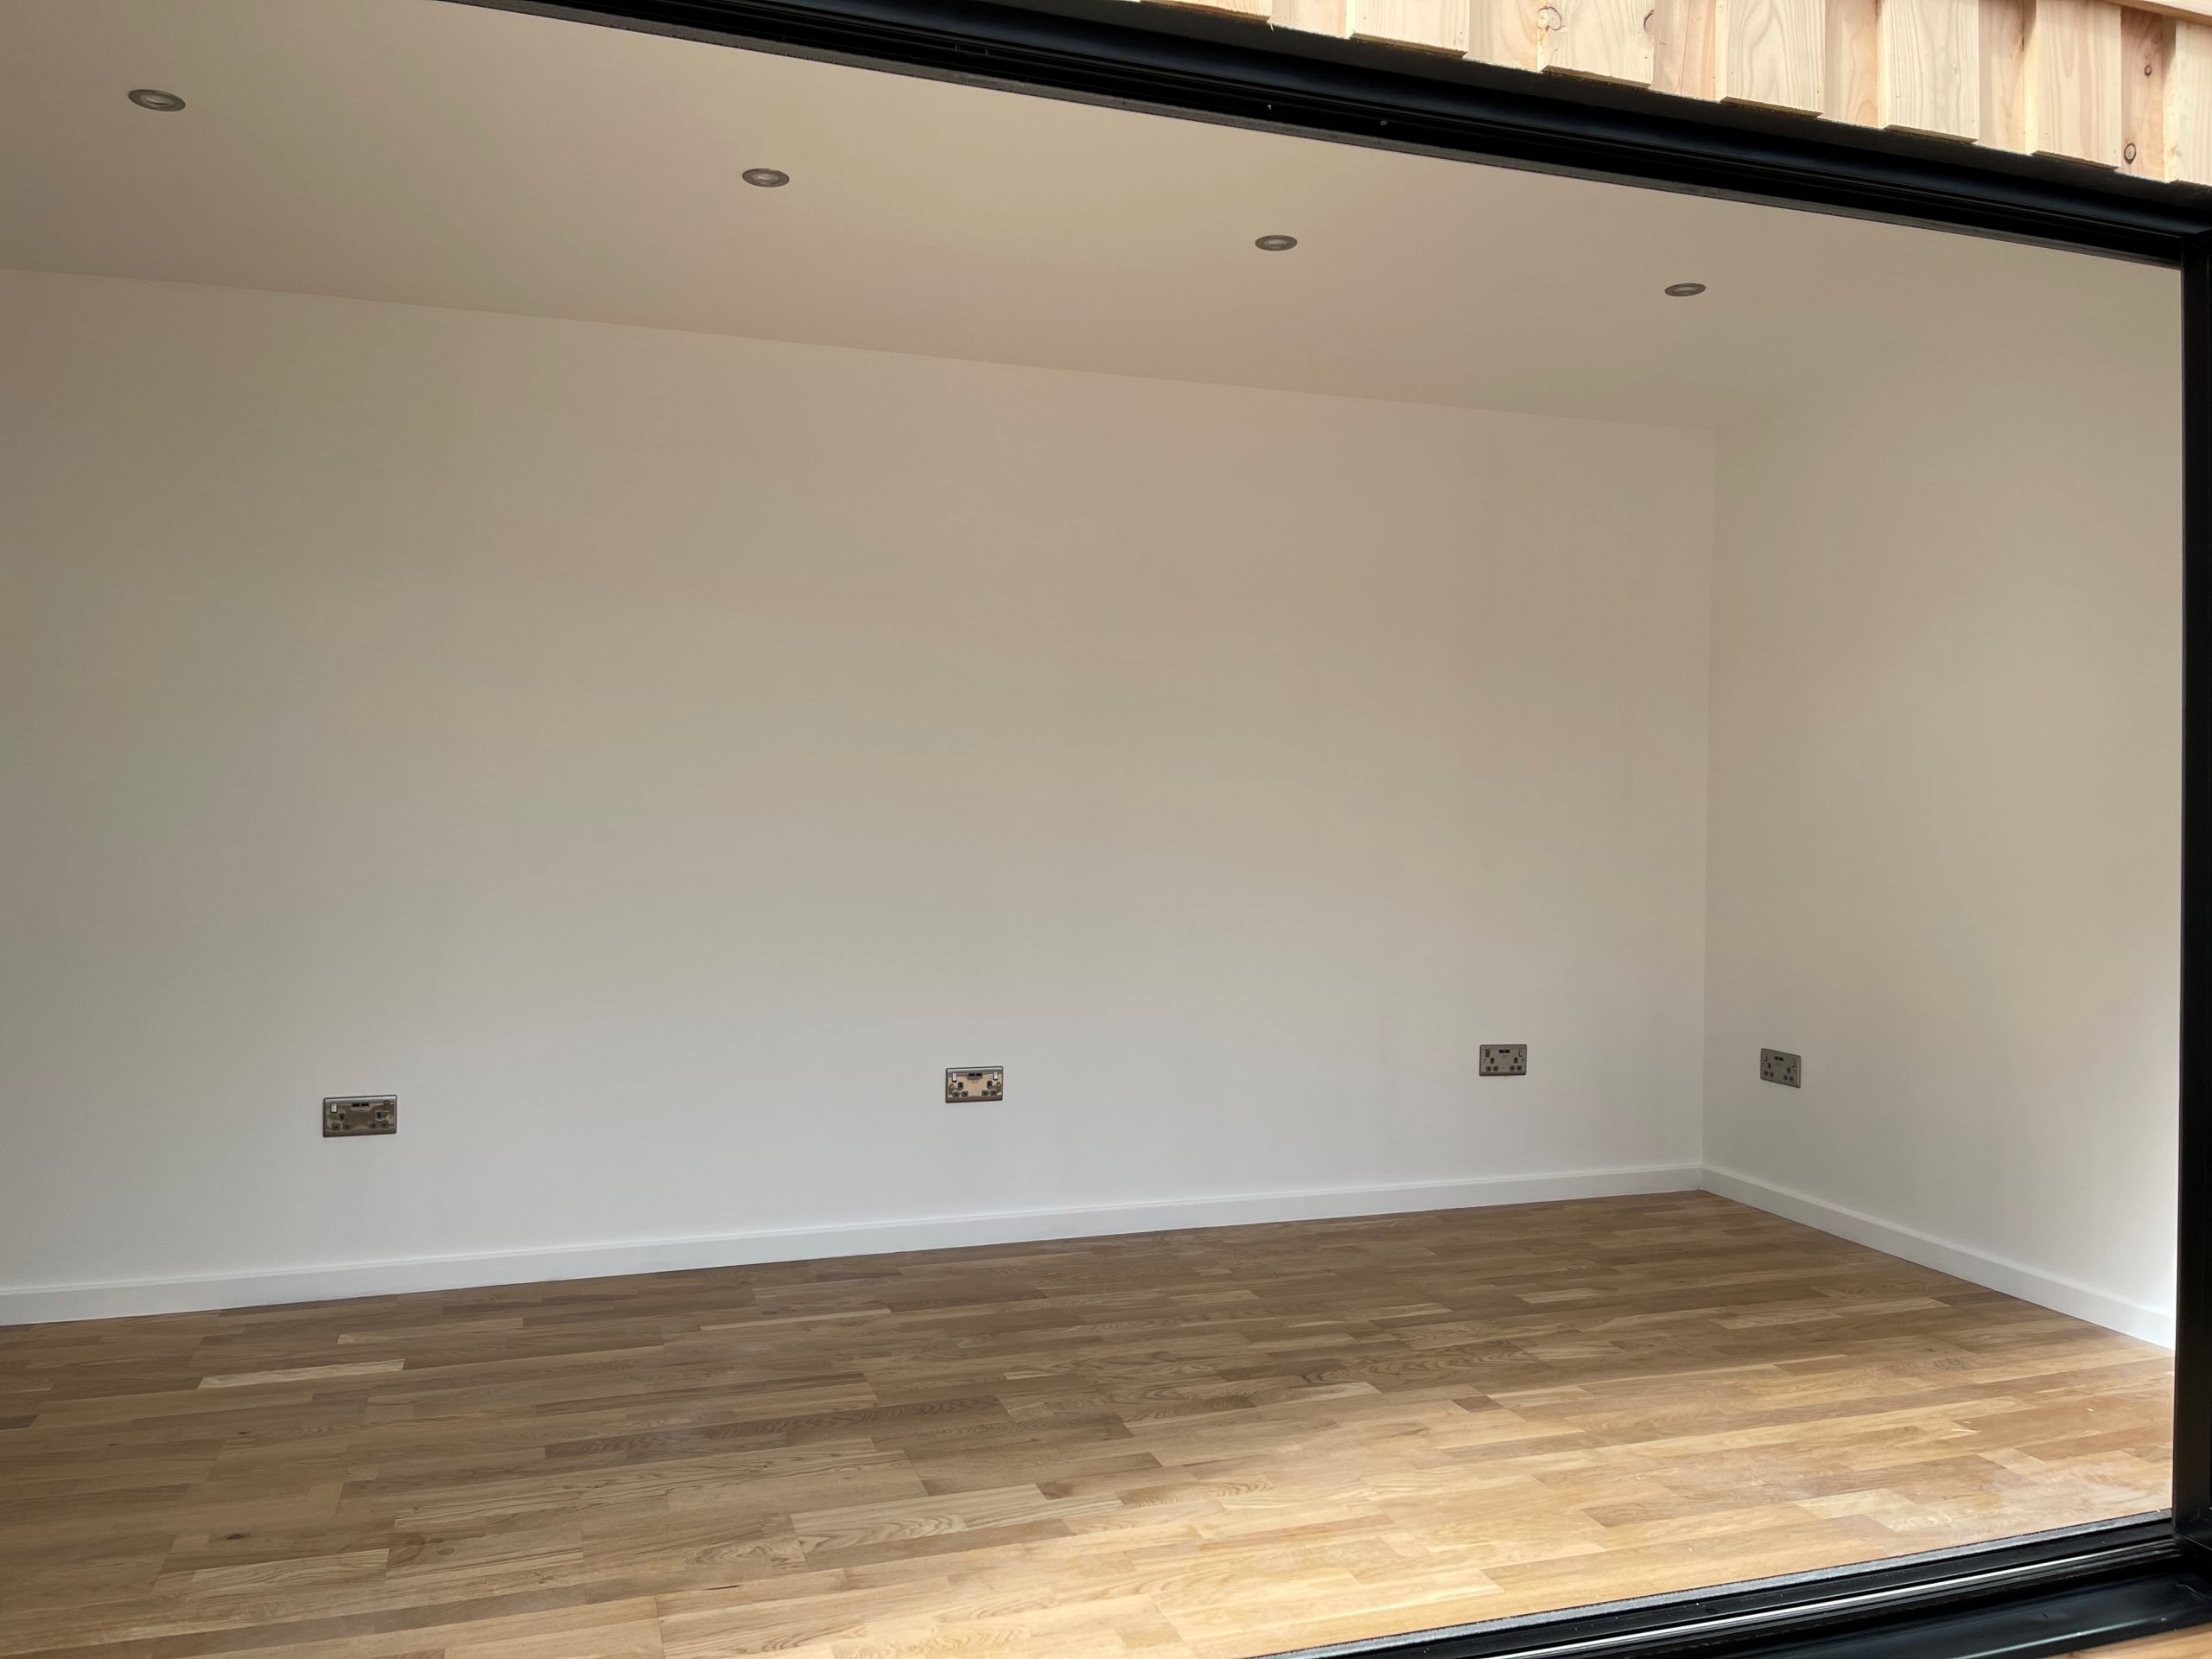
  • Fully Insulated with electric sockets, spot lighting, and heating

  • Wood Flooring

  • Aluminium Bi Fold Doors

  • Fully wrapped in larch cladding

  • Lead Time for build 6-8 weeks

Location: Nationwide


£16,500.00

+ VAT

Not Available for Hire

Call for an instant quote!

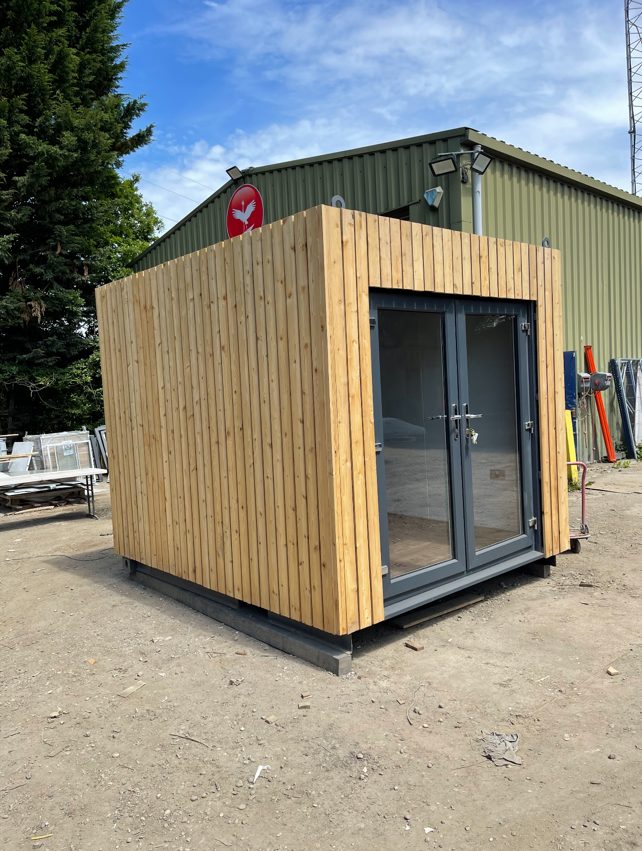
10ft x 8ft Container Conversion

  • Fully Insulated with electric sockets, spot lighting, and heating

  • Wood Flooring

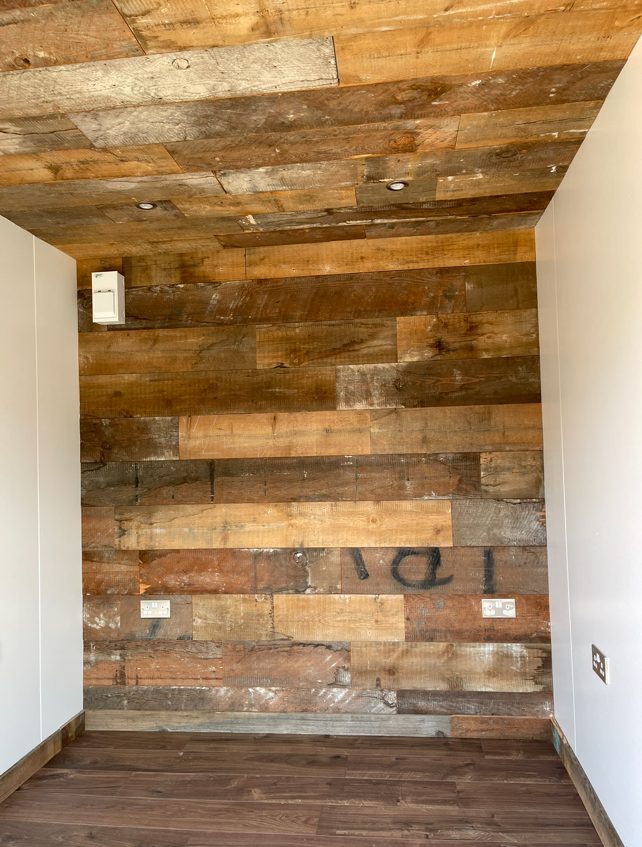
  • Feature Clad Wall and Ceiling

  • UPVC Double glazed French Doors

  • Fully wrapped in larch cladding

  • Lead Time for build 6-8 weeks

Location: Nationwide


£12,500.00

EX VAT

Not Available for Hire

Call for an instant quote!

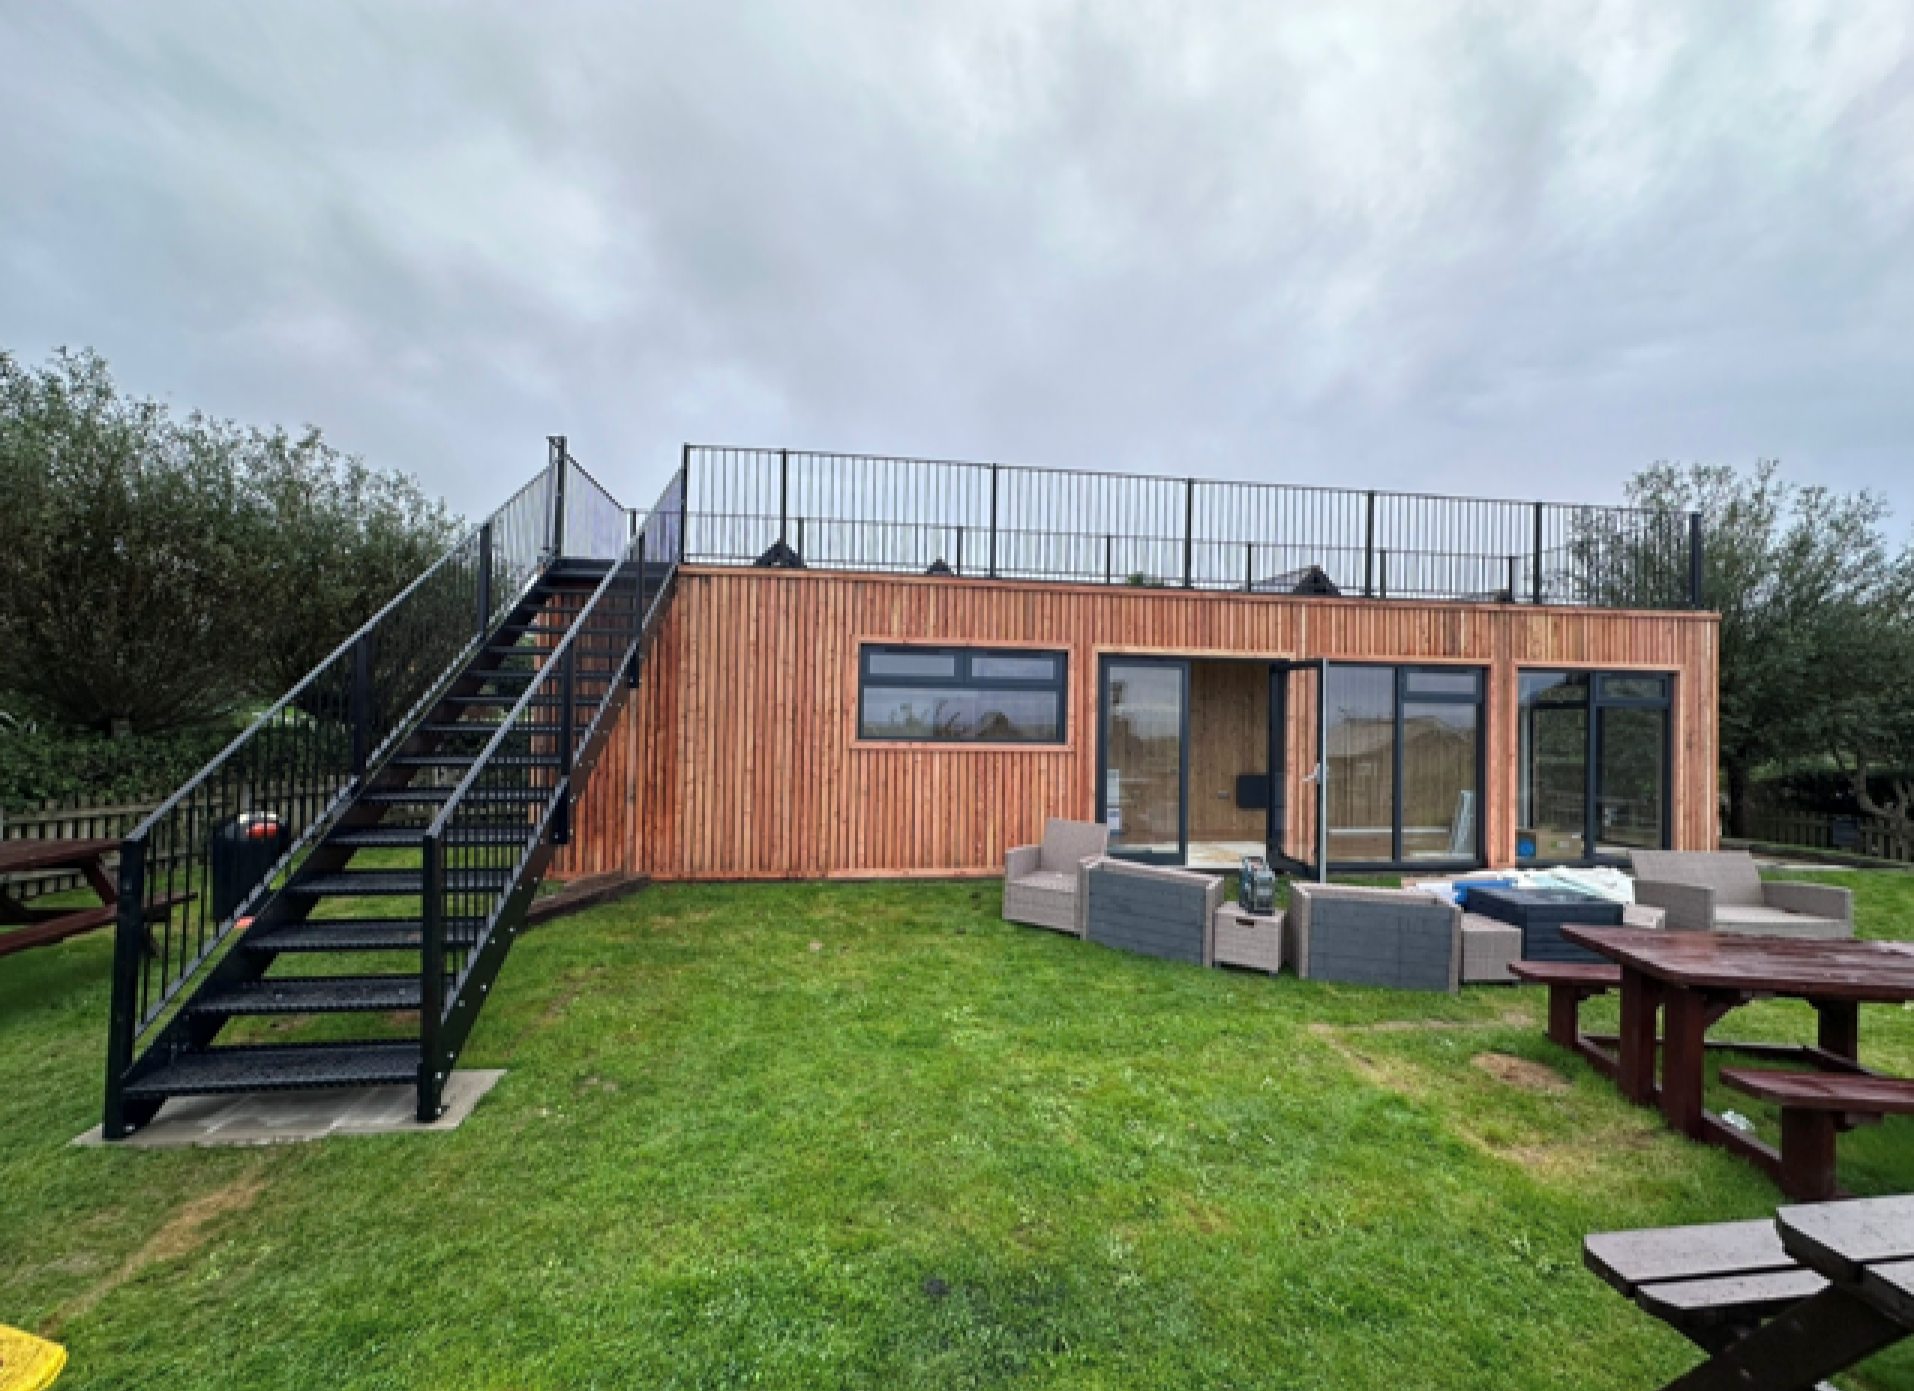
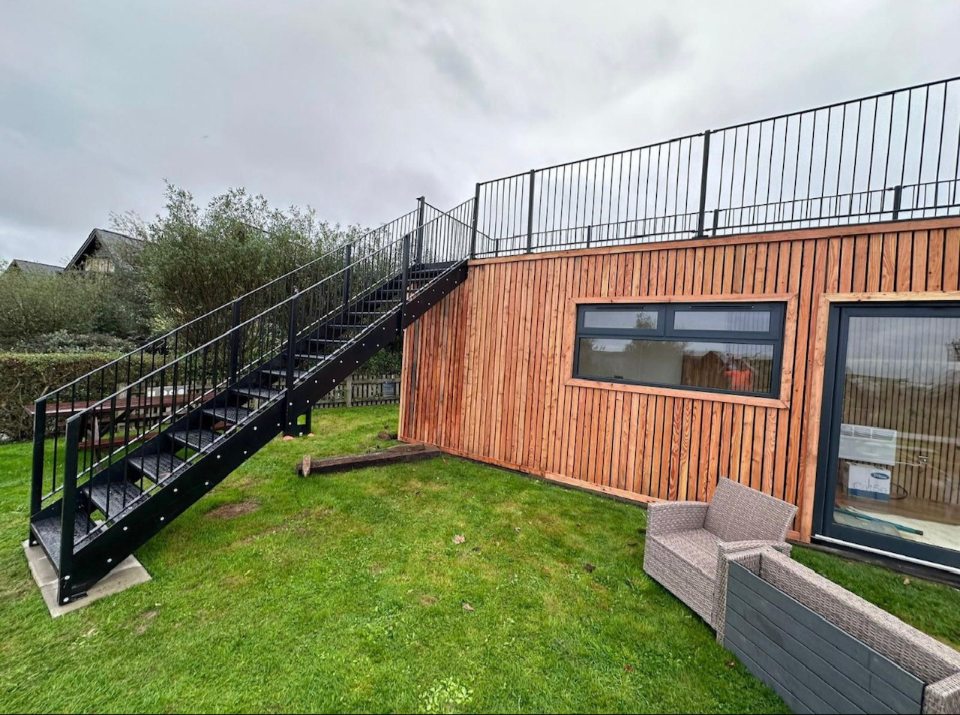
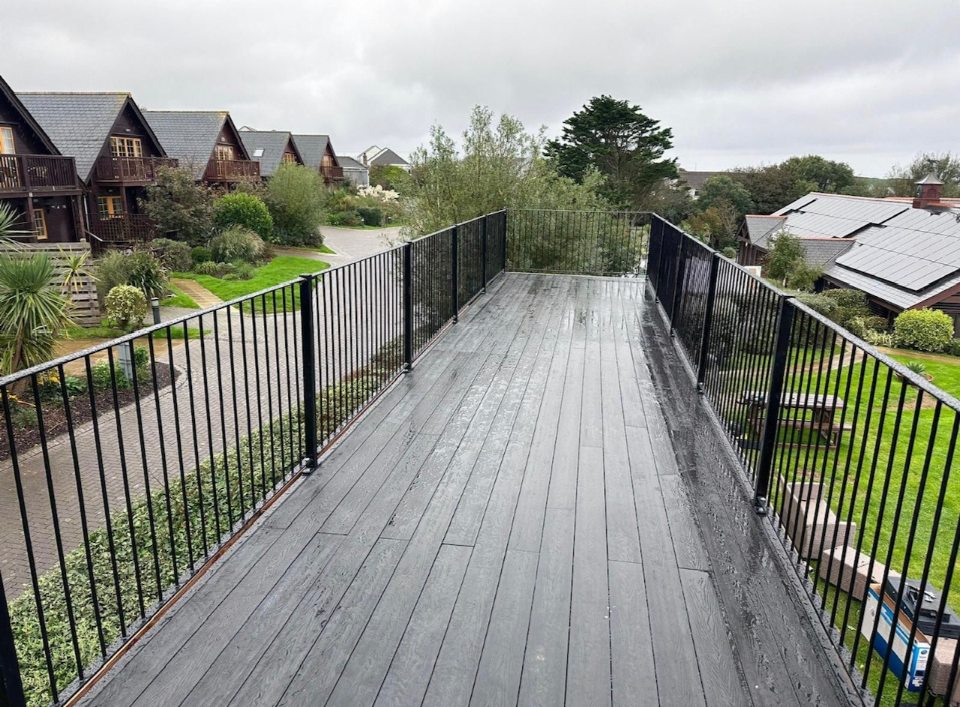
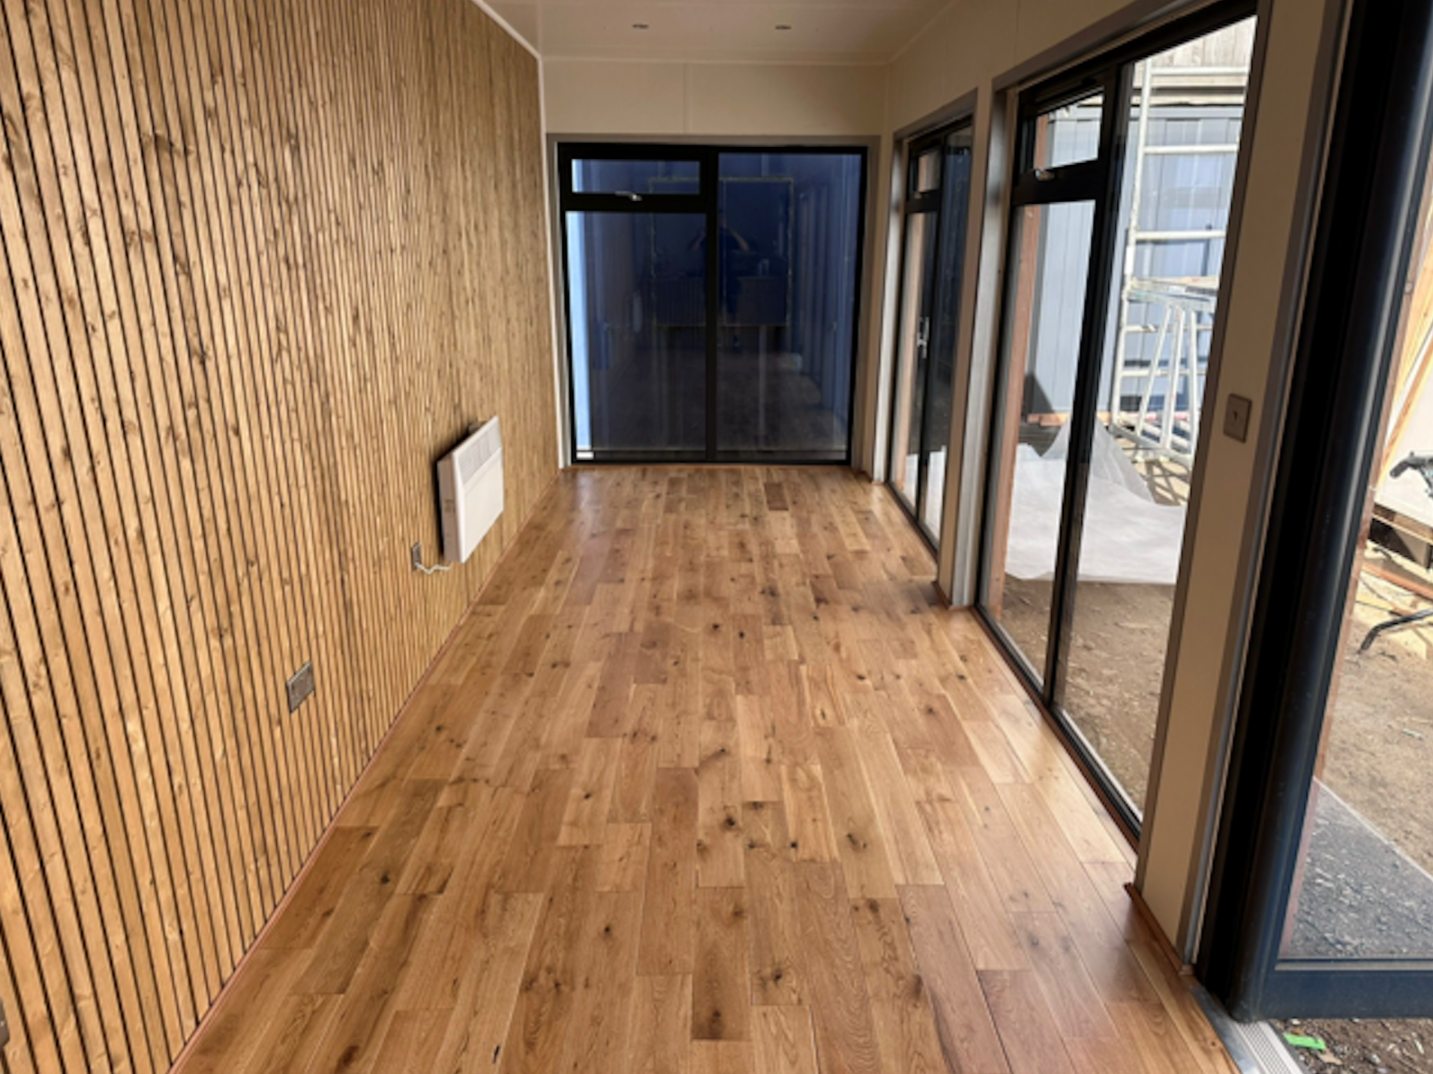
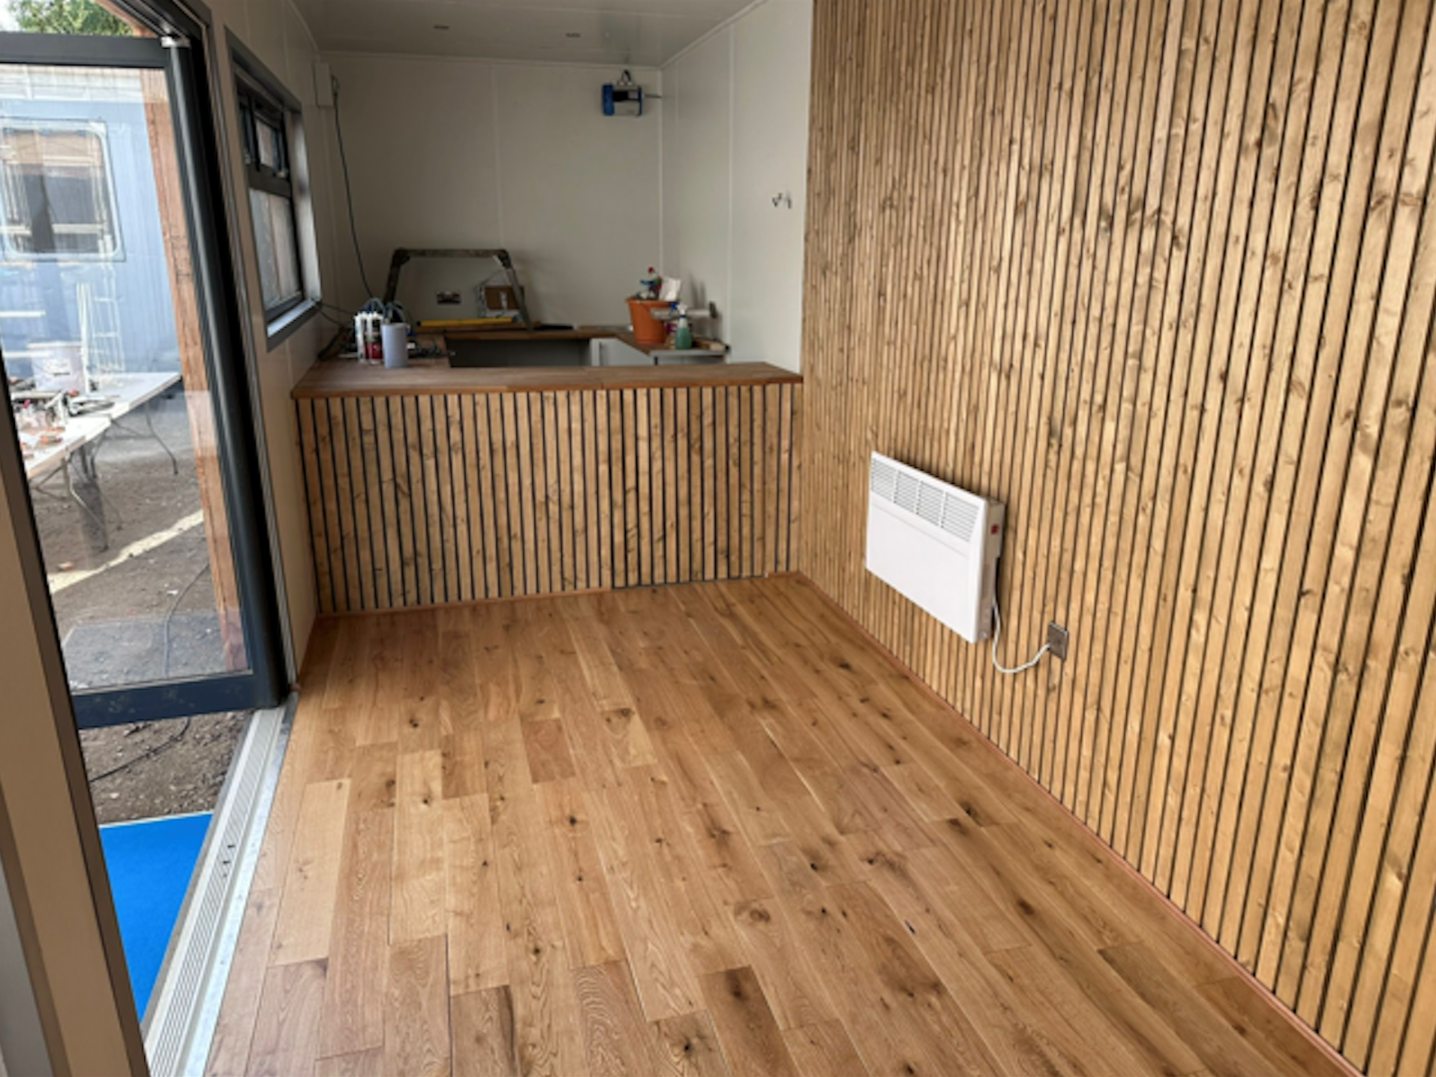
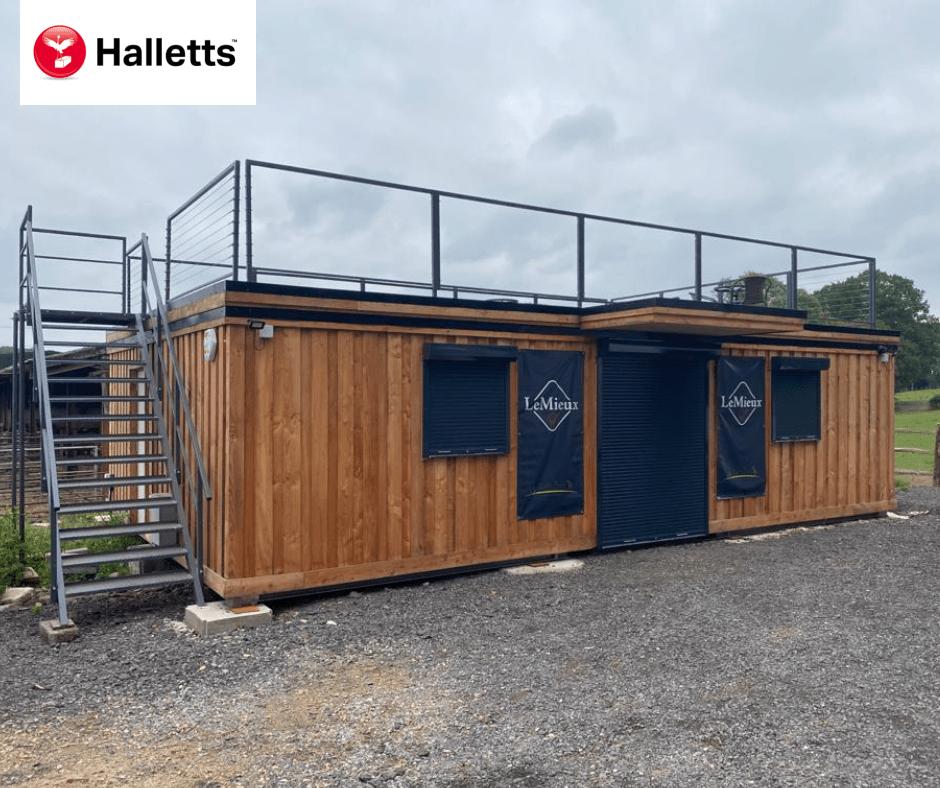
40ft x 8ft Rooftop Container Bar

  • 40ft x 8ft Rooftop Container Bar
  • Fully Insulated with electric sockets, spot lighting, and heating
  • Built in Bar
  • Wood Flooring
  • Feature Larch Clad Wall
  • Aluminium double glazed premium windows and double French doors
  • Fully wrapped in larch cladding
  • Steel staircase up to Rooftop terrace with full surrounding steel balustrade
  • Double container doors leading to cool room with Air Conditioning unit.
  • Lead Time for build 6-8 weeks

Location: Nationwide


£85,000.00

EX VAT

Not Available for Hire

Call for an instant quote!

  • Fully Refurbished
  • Zinc Roof
  • Colour Light Grey (Other Colour Options Available)
  • New Flooring
  • New Electric Sockets, Lighting and Heating
  • New UPVC Large and Small Windows
  • New Kitchenette with Partition
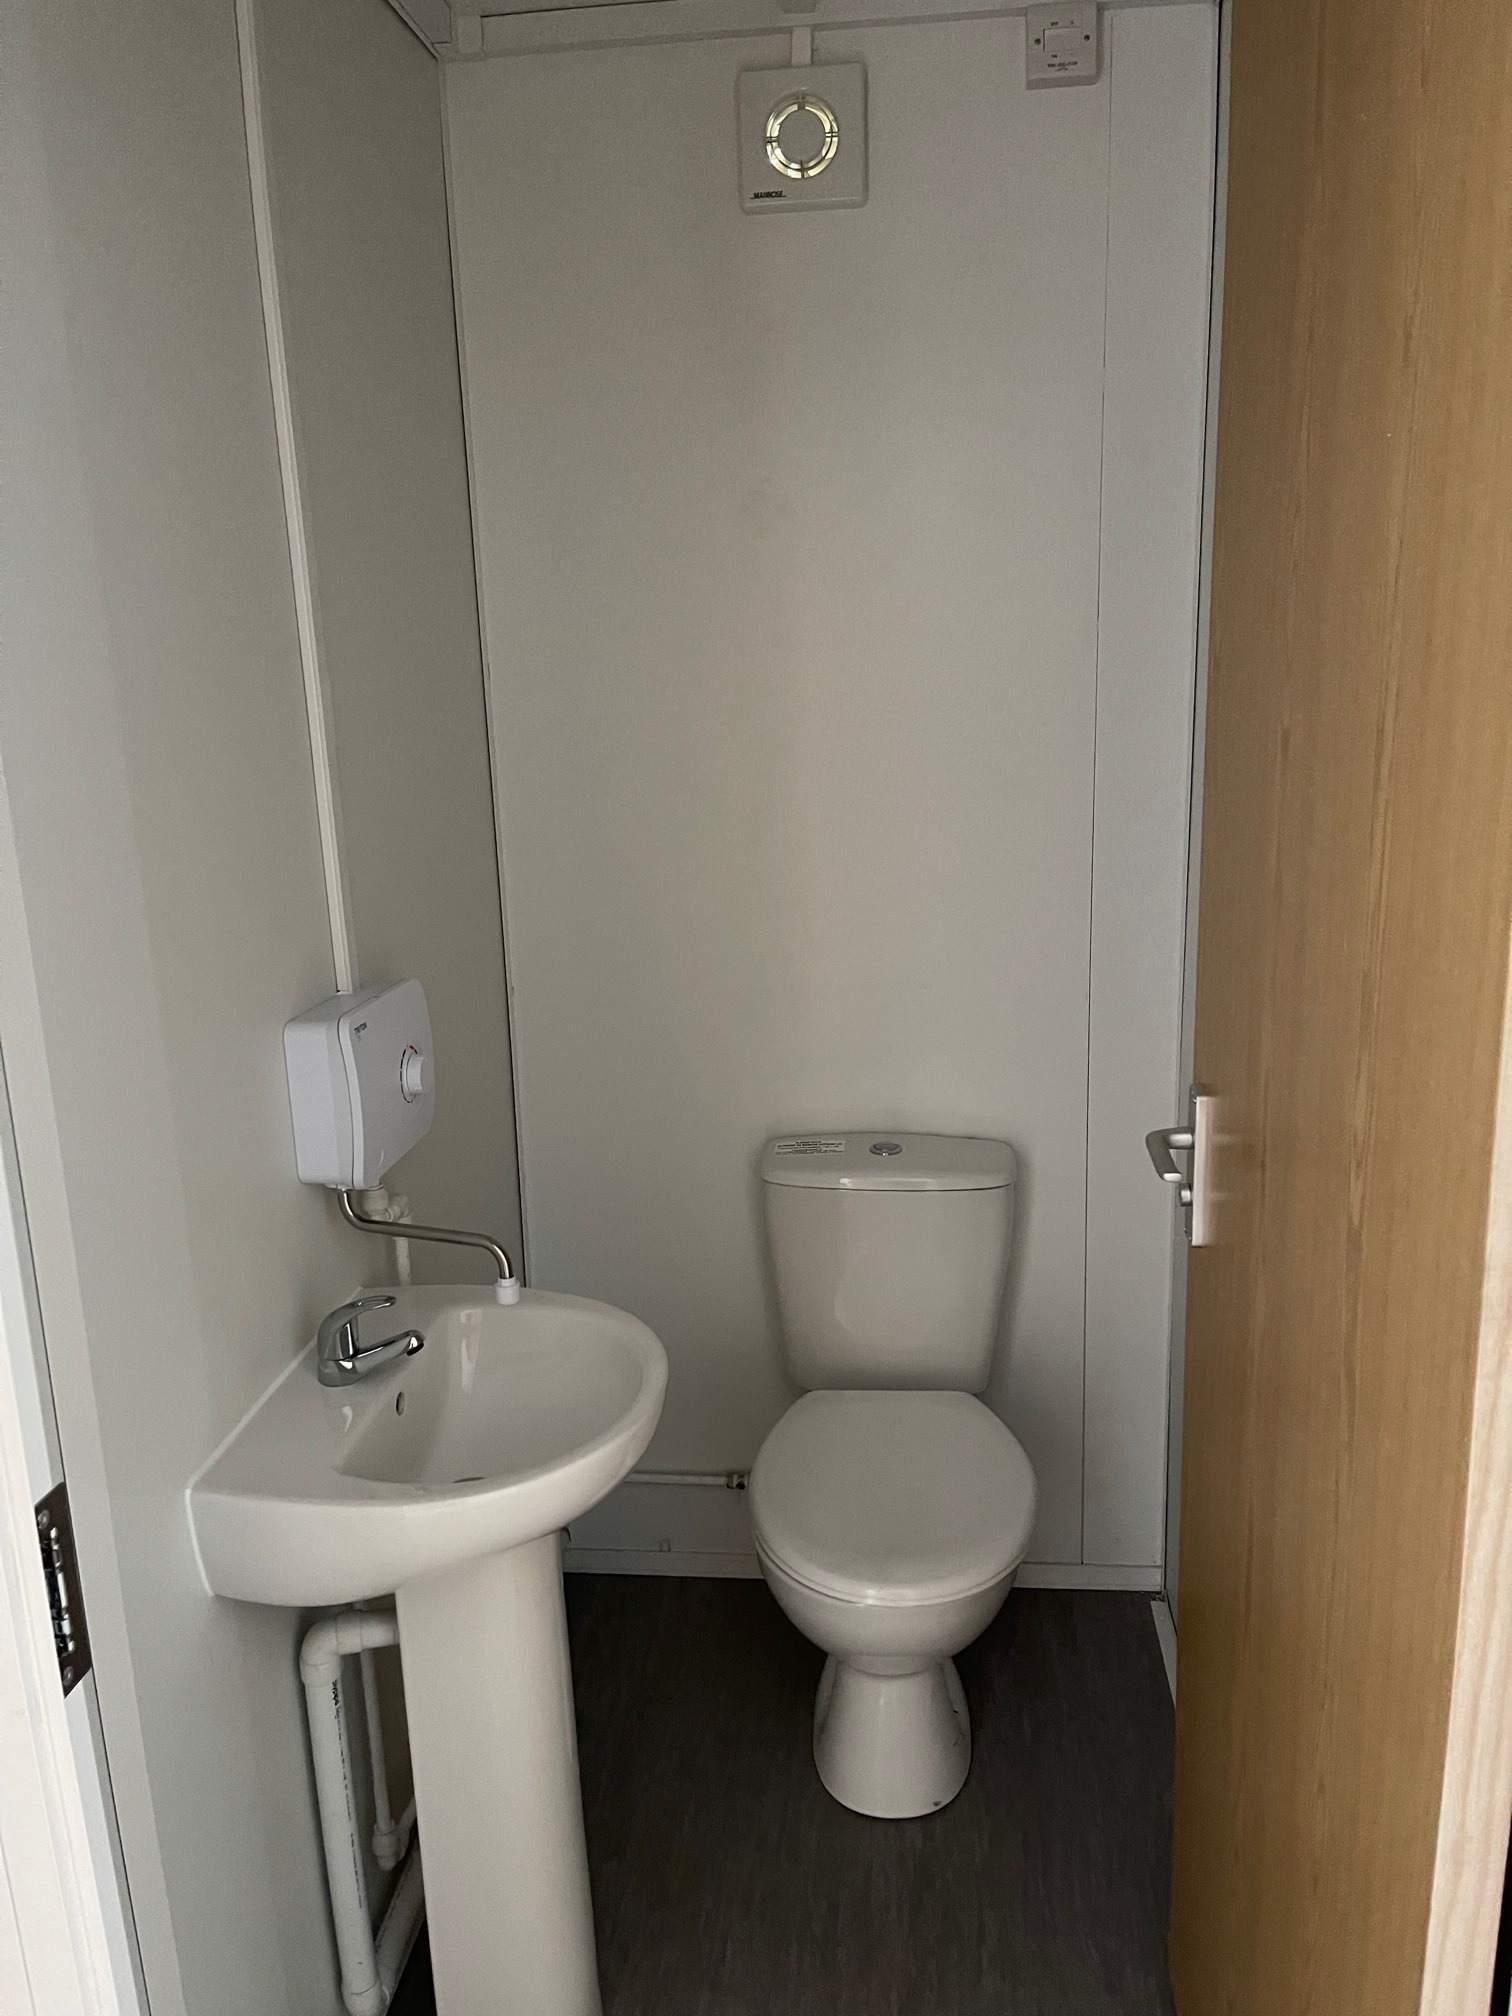
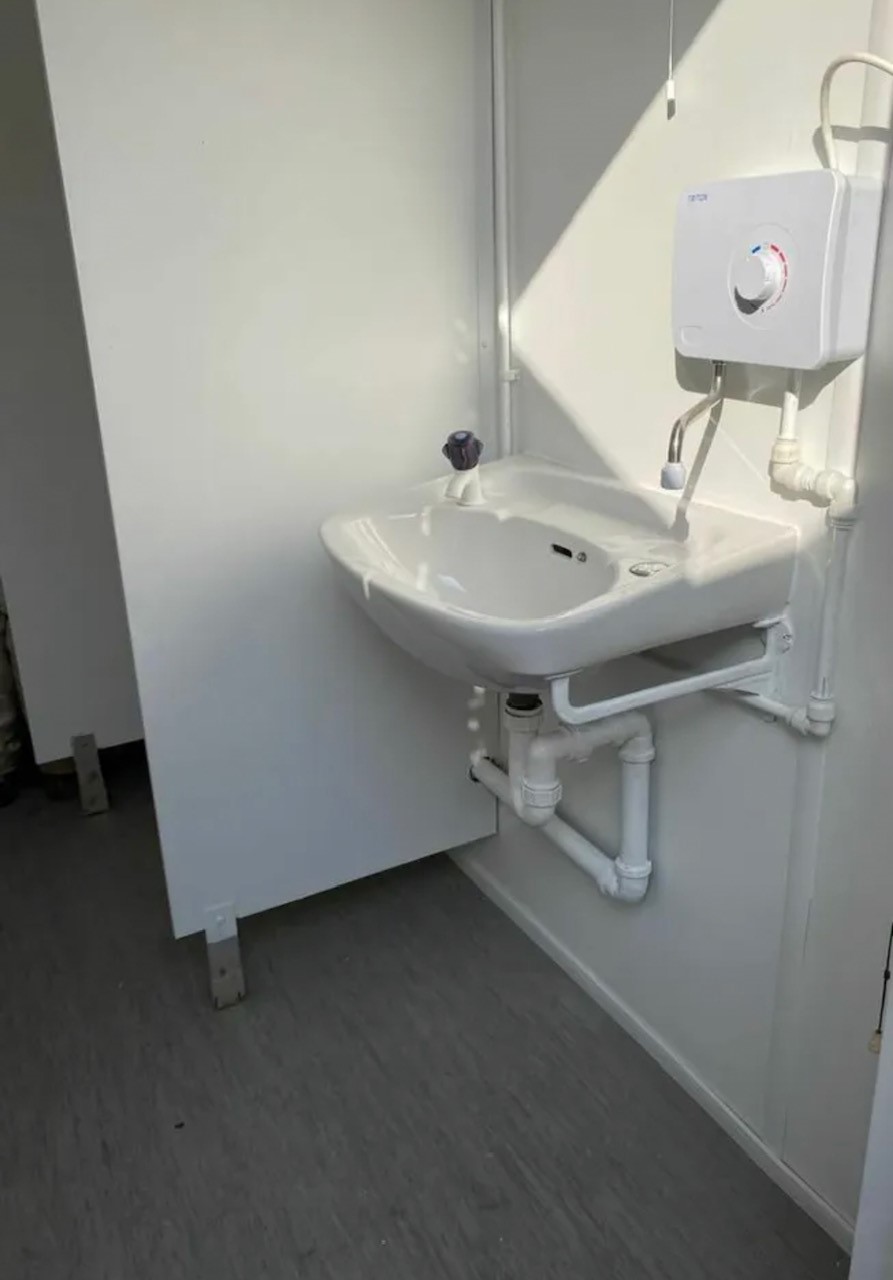
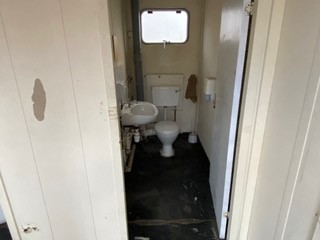
  • New Toilet Room with toilet, Sink, Water Heater and Fan

Location: Nationwide

£18,995

EX VAT

Not Available for Hire

Call for an instant quote!

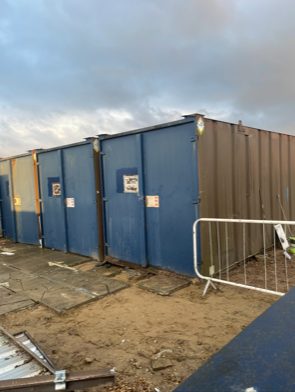
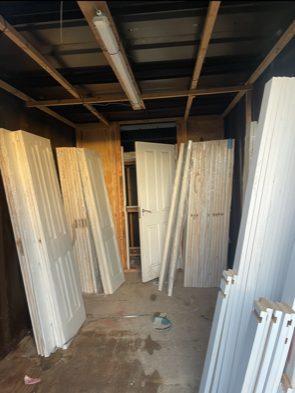
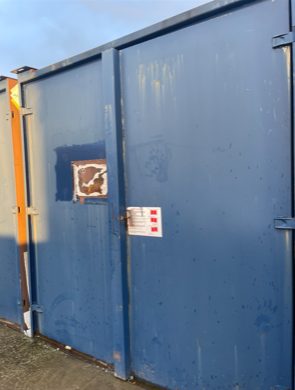
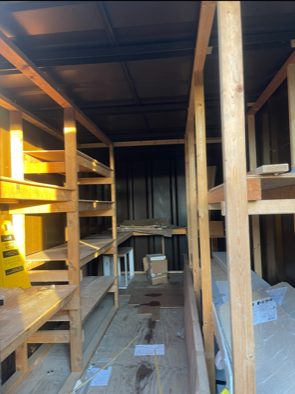
6 x 21ft x 8ft Container Stores

  • Wind and Water Tight
  • Very Good Condition
  • Some have racking inside
  • Floorings all good
  • Contents not included

Location: Nationwide


£1,500

EX VAT

Not Available for Hire

Call for an instant quote!

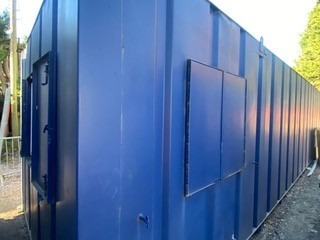
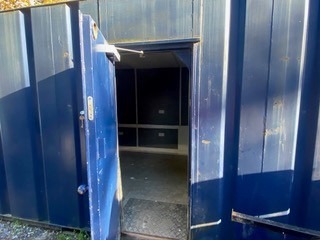
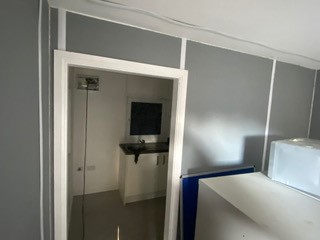
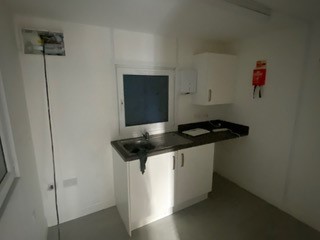
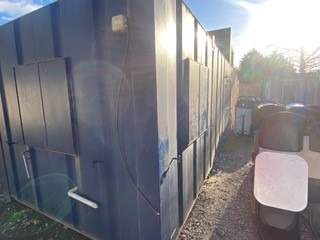
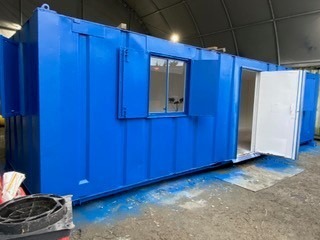
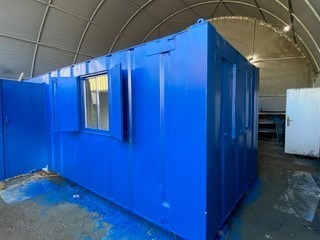
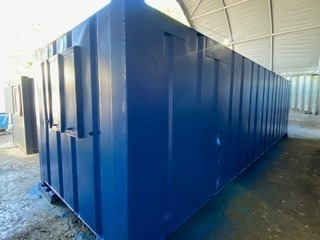
32ft x 10ft Anti Vandal Canteen in Blue

  • Used with electric sockets, lighting and heating
  • UPVC Double Glazed Windows
  • Furniture
  • Kitchenette 

Location: Nationwide


£4,995

EX VAT

Not Available for Hire

Call for an instant quote!

20ft Used Shipping Containers

  • Wind and Water Tight
  • Doors in good working Order
  • Random Selection
  • Lock Box and Lock additional cost.

Location: Nationwide


£1,500

EX VAT

Not Available for Hire

Call for an instant quote!

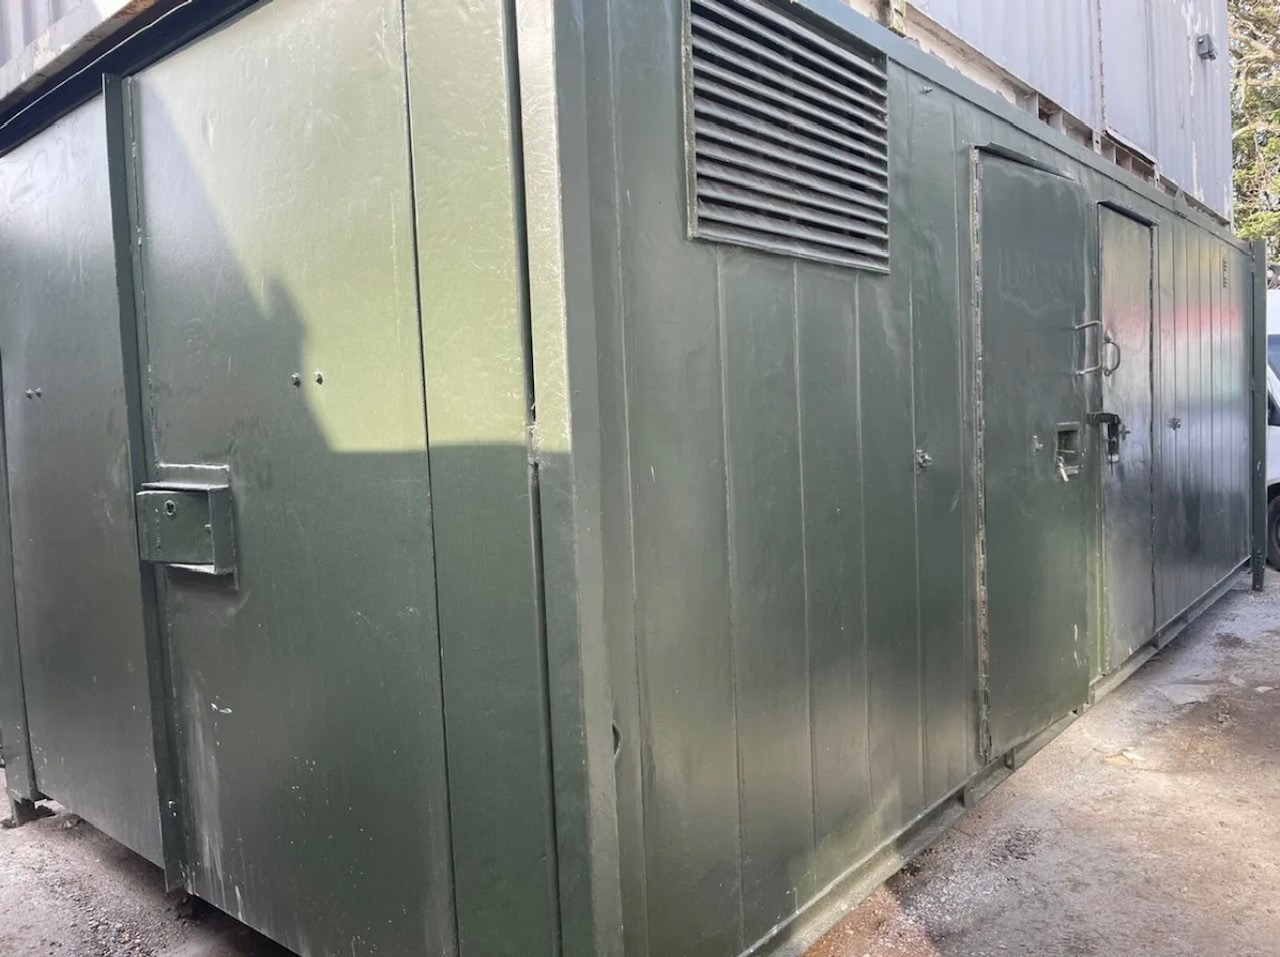
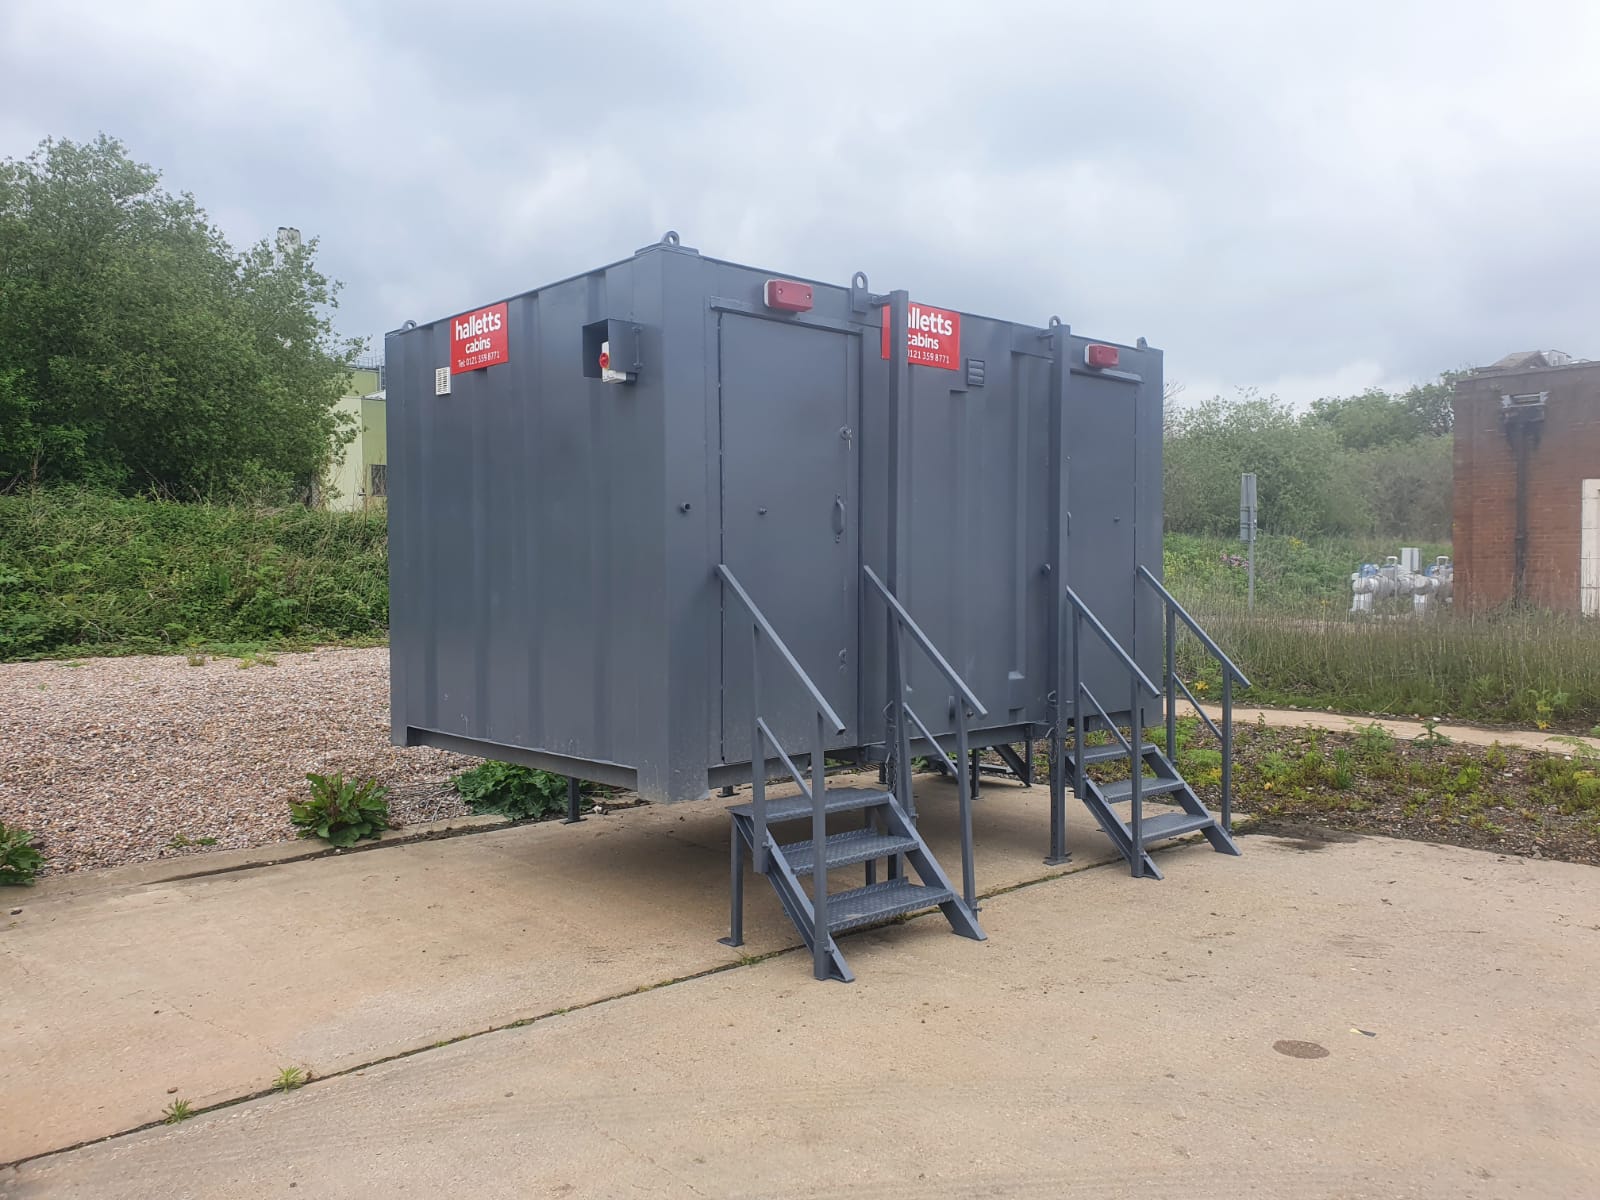
24ft x 10ft Jack Leg Anti Vandal Canteen/Toilet/Storage

  • Split entrance for Canteen room and WC which includes single cubical, urinal and sink.
  • Container door end with storage.
  • Electric Sockets, Lighting and Heating
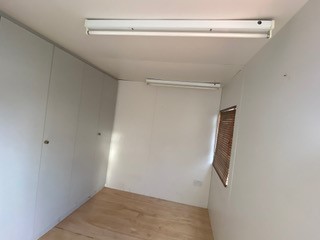
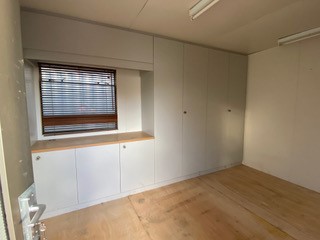
  • Fitted Floor to Ceiling Cupboards
  • Colour: Dark Green

Location: Nationwide


£5,000

EX VAT

Not Available for Hire

Call for an instant quote!

40ft x 12ft Jack Leg Genuine Portakabin Pullman

  • 2 x Offices, Canteen and WC
  • Electric Sockets, Lighting and Heating
  • Colour: Light Grey
  • Full or Part Refurbishment option is available please ask.

Location: Nationwide


£9,500

EX VAT

Not Available for Hire

Call for an instant quote!

32ft x 10ft Anti Vandal Split Canteen/Office

  • Canteen approx 10ft – Office approx 22ft
  • Electric Sockets, Lighting and Heating
  • UPVC Double Glazing
  • Colour: Dark Blue

Location: Nationwide


£5,500

EX VAT

Not Available for Hire

Call for an instant quote!

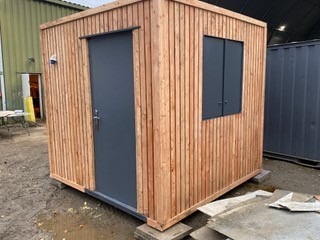
8ft x 8ft Anti Vandal Gate House/Office

  • Open Plan
  • Electric Sockets, Lighting and Heating
  • Colour: Clad in New Larch Timber

Location: Nationwide


£5,500

EX VAT

Not Available for Hire

Call for an instant quote!

20ft x 10ft Anti Vandal Sleeper Unit

  • Split sides with two entrances, each side has its own room and Shower Toilet Facility
  • Electric Sockets, Lighting and Heating
  • Colour: Dark Grey

Location: Nationwide


£6,500

EX VAT

Not Available for Hire

Call for an instant quote!

21ft x 8ft Anti Vandal Canteen

  • Open Plan
  • Electric Sockets, Lighting and Heating, Hot water Unit + kitchen with cupboards and work top.
  • Colour: Dark Grey 

Location: Nationwide


£4,200

EX VAT

Not Available for Hire

Call for an instant quote!

30ft x 9ft Anti Vandal Fire Rated Office

  • Open Plan Refurbished
  • Electric Sockets, Lighting and Heating
  • Colour: Dark Blue

Location: Nationwide


£6,500

EX VAT

Not Available for Hire

Call for an instant quote!

24ft x 9ft Anti Vandal Office

  • Open Plan
  • Electric Sockets, Lighting and Heating
  • Colour: Dark Grey

Location: Nationwide


£4,200

EX VAT

Not Available for Hire

Call for an instant quote!

22ft x 9ft Jack Leg Portable Cabin

  • 22ft x 9ft Jack Leg Portable Cabin
  • Open Plan
  • Electric Sockets, Lighting and Heating
  • Fitted Desk and Floor to Ceiling Cupboards
  • Colour: Light Grey

Location: Nationwide


£4,995

EX VAT

Not Available for Hire

Call for an instant quote!

24ft x 9ft Jack Leg Portable Cabin

  • 24ft x 9ft Jack Leg Portable Cabin
  • Split Offices with two entrances
  • Electric Sockets, Lighting and Heating
  • Fitted Floor to Ceiling Cupboards
  • Colour: Light Grey

Location: Nationwide


£5,500

EX VAT

Not Available for Hire

Call for an instant quote!

10ftx8ft – £5950 + Vat / 16ftx8ft – £7950 + Vat / 20ftx8ft – £9000 + Vat / 24ftx8ft – £12000 + Vat / 30ftx8ft – £13500 + Vat

  • Reinforced doors and windows with secure locking
  • Open plan with electric sockets and lighting
  • Any Extras available: Canteen, Partitions, Toilets.

Location: Nationwide


From £5,950

EX VAT

Not Available for Hire

Call for an instant quote!

  •  Electric Sockets, Lighting and Heating
  •  Wind & watertight
  •  Sprayed Dark Grey

Location: Nationwide


£4,995

EX VAT

Not Available for Hire

Call for an instant quote!

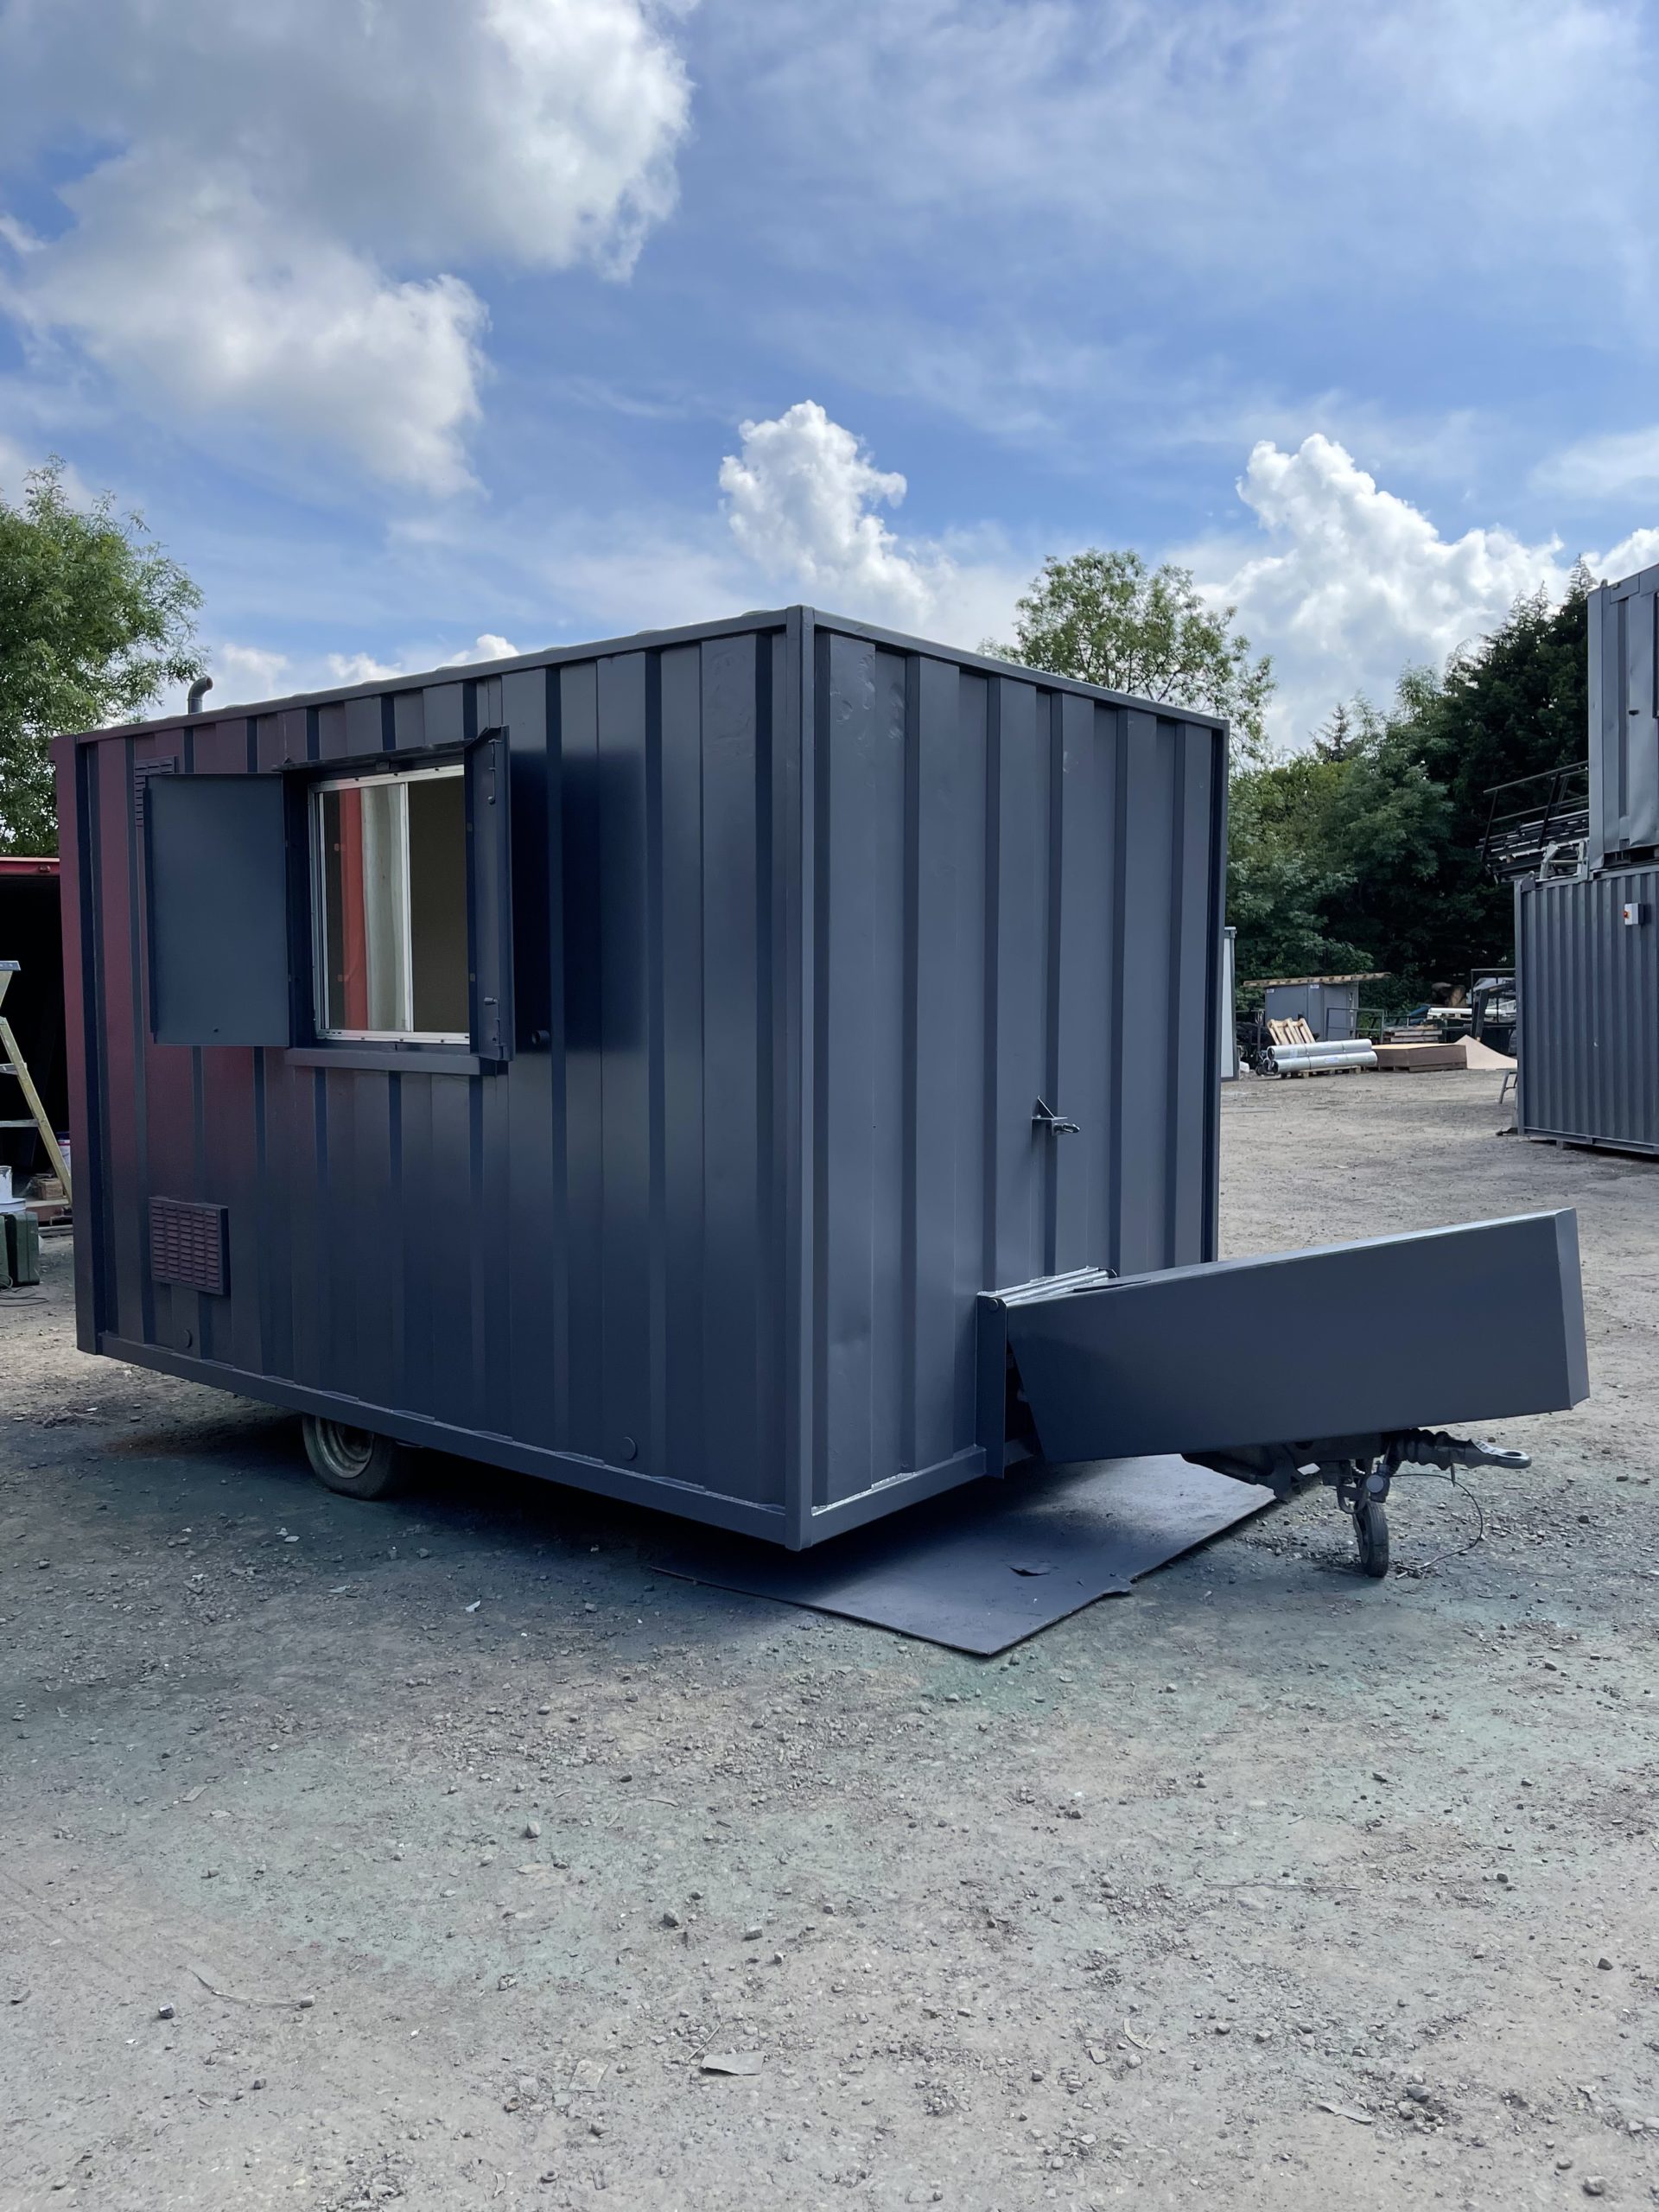
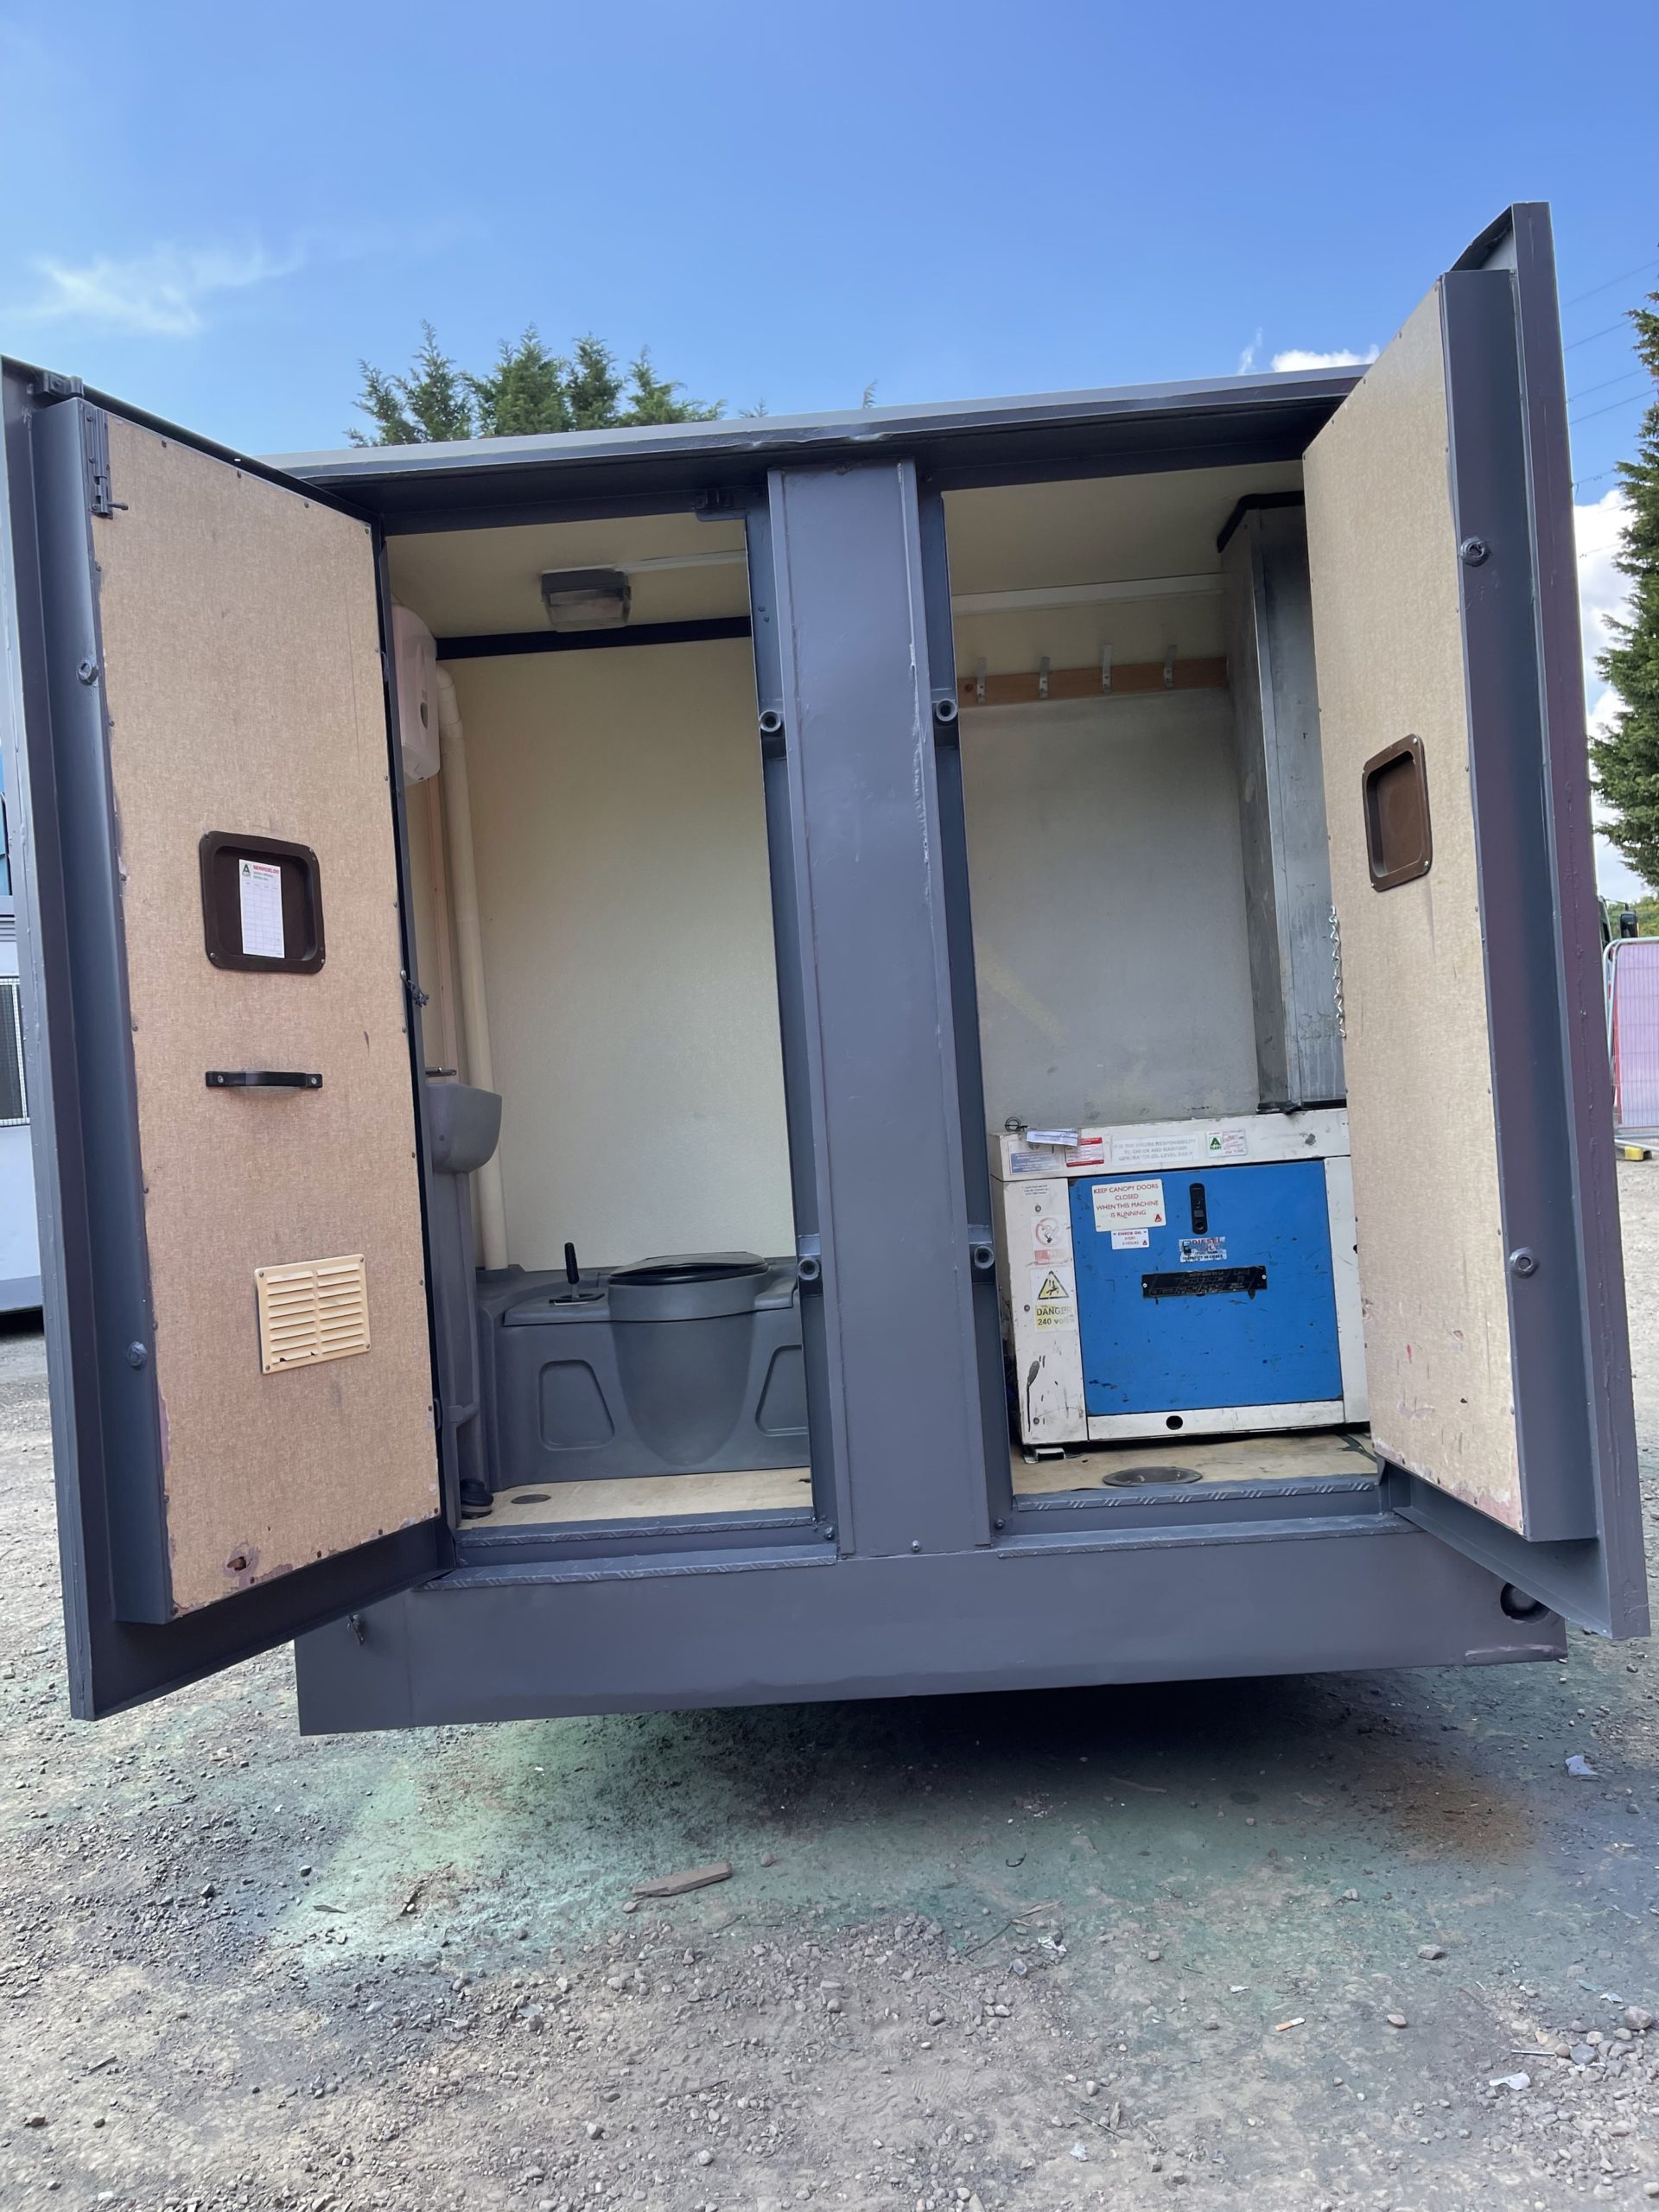
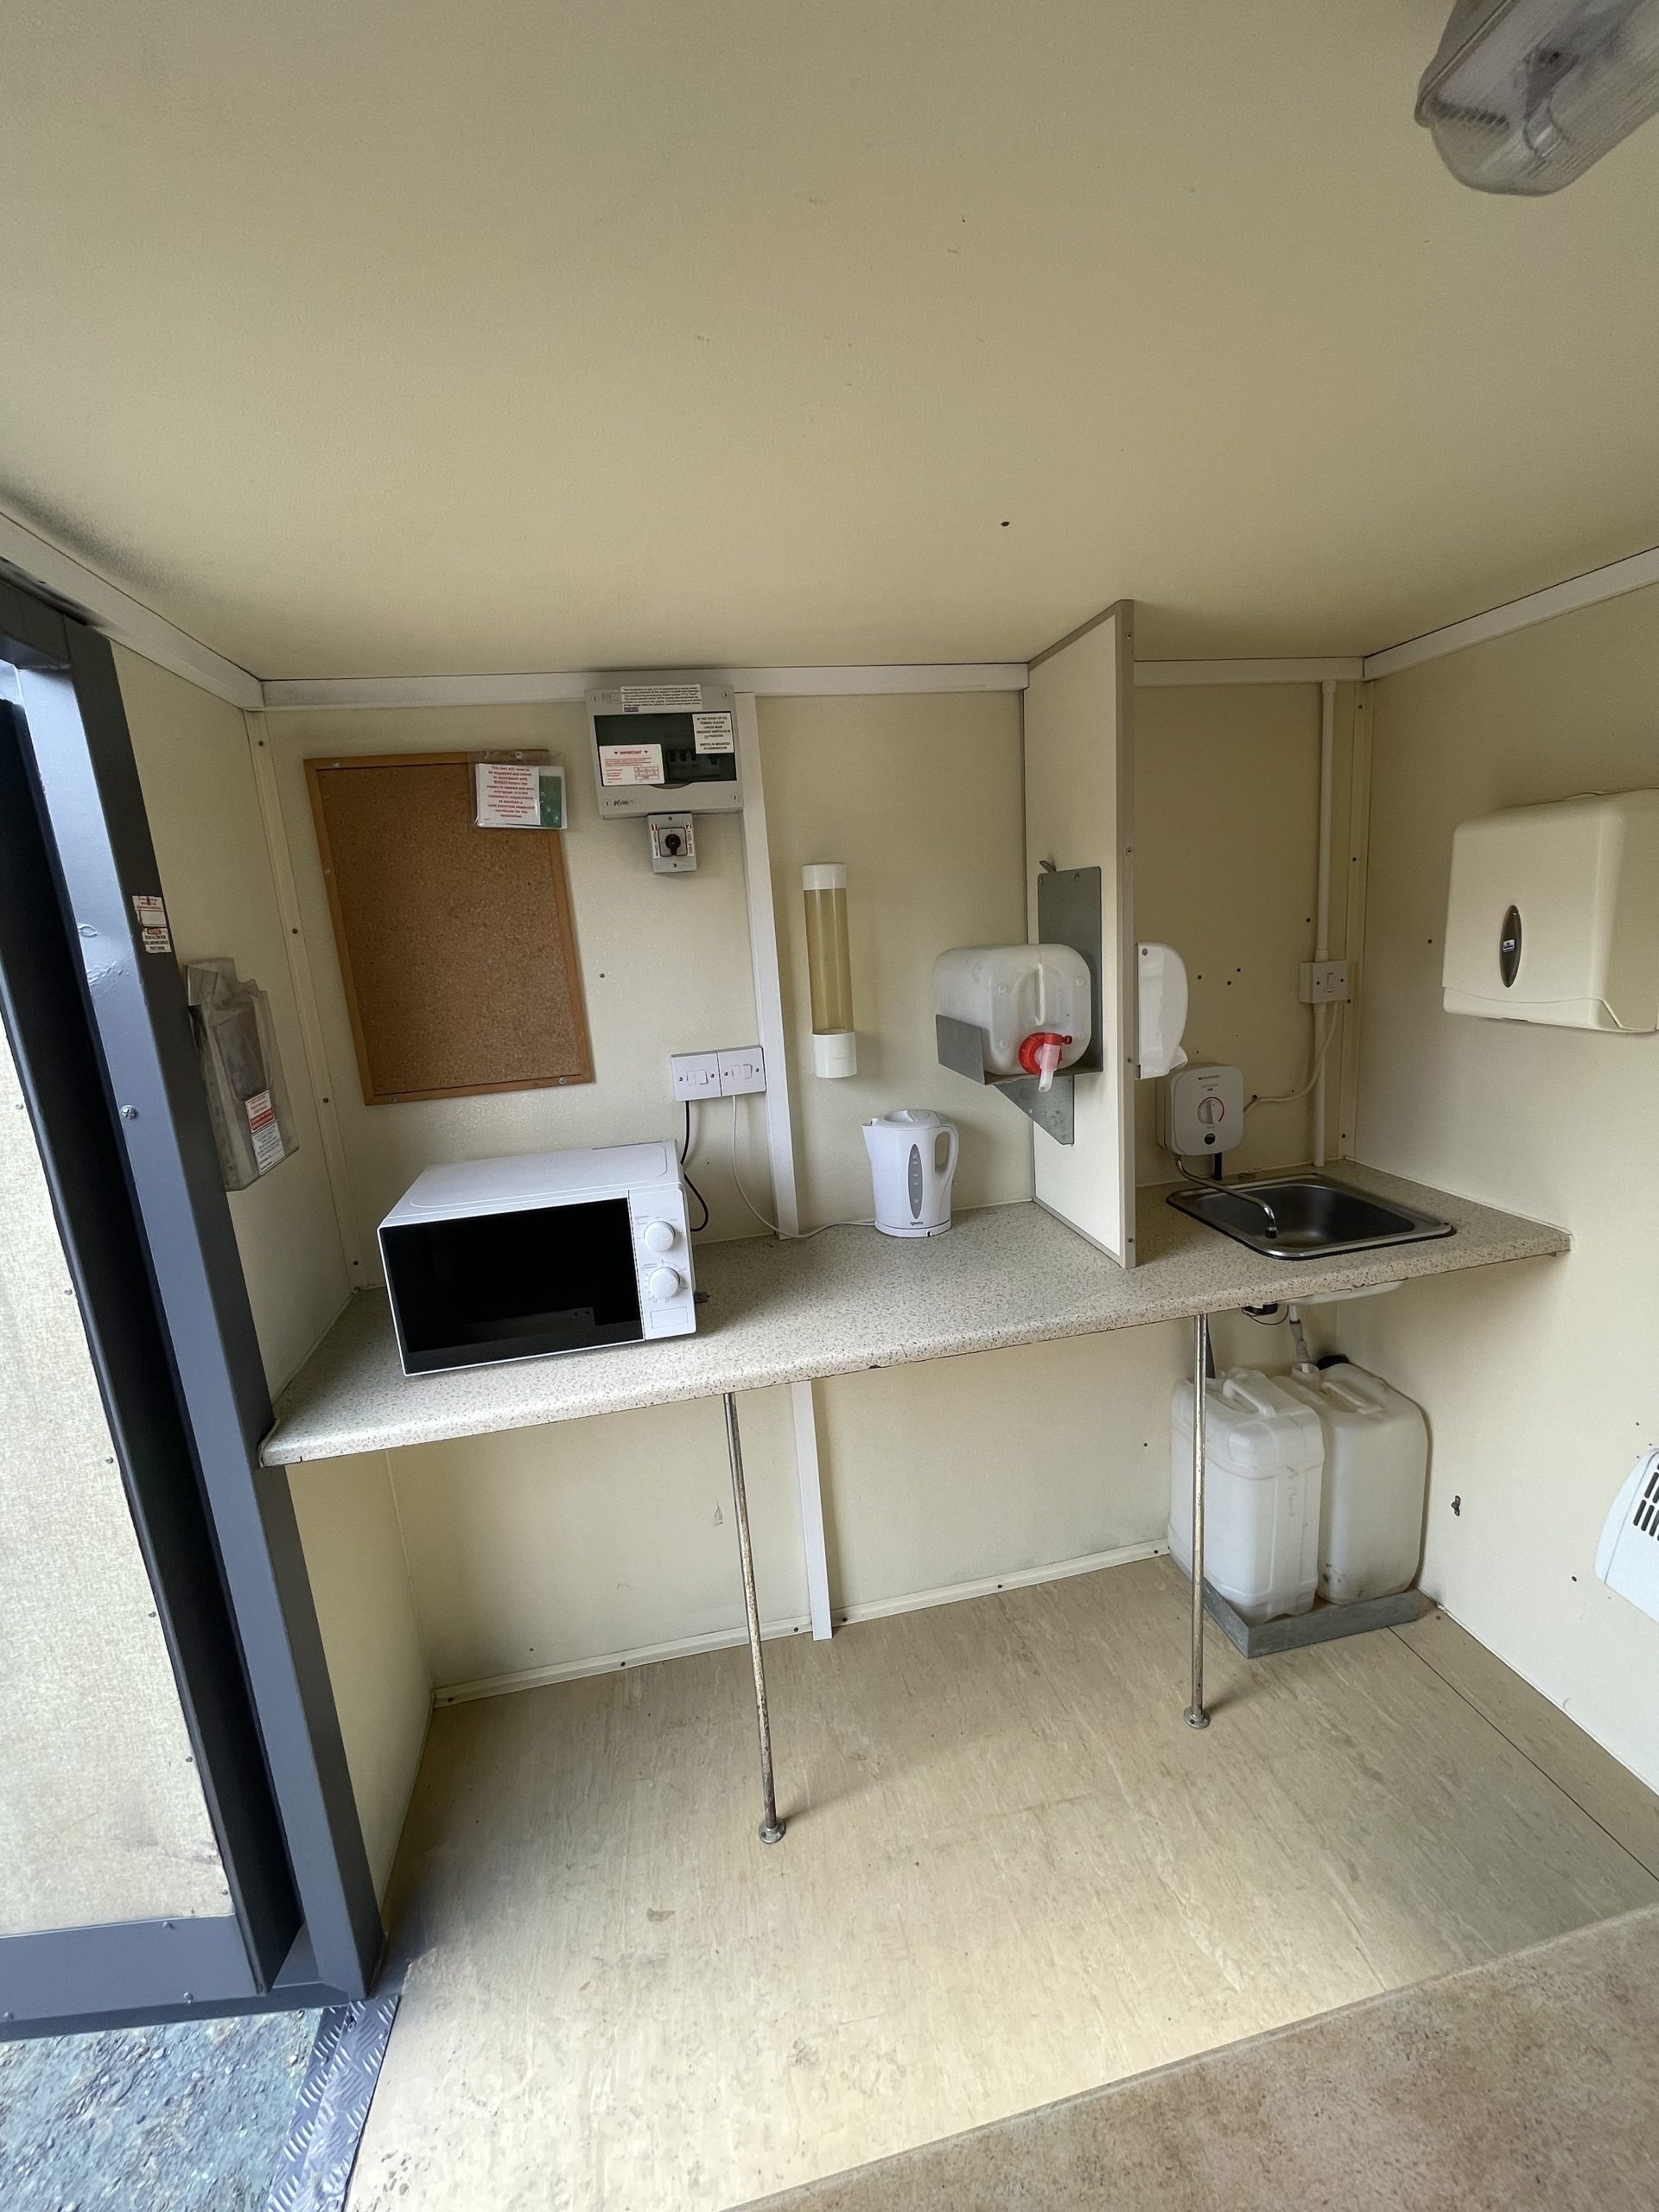
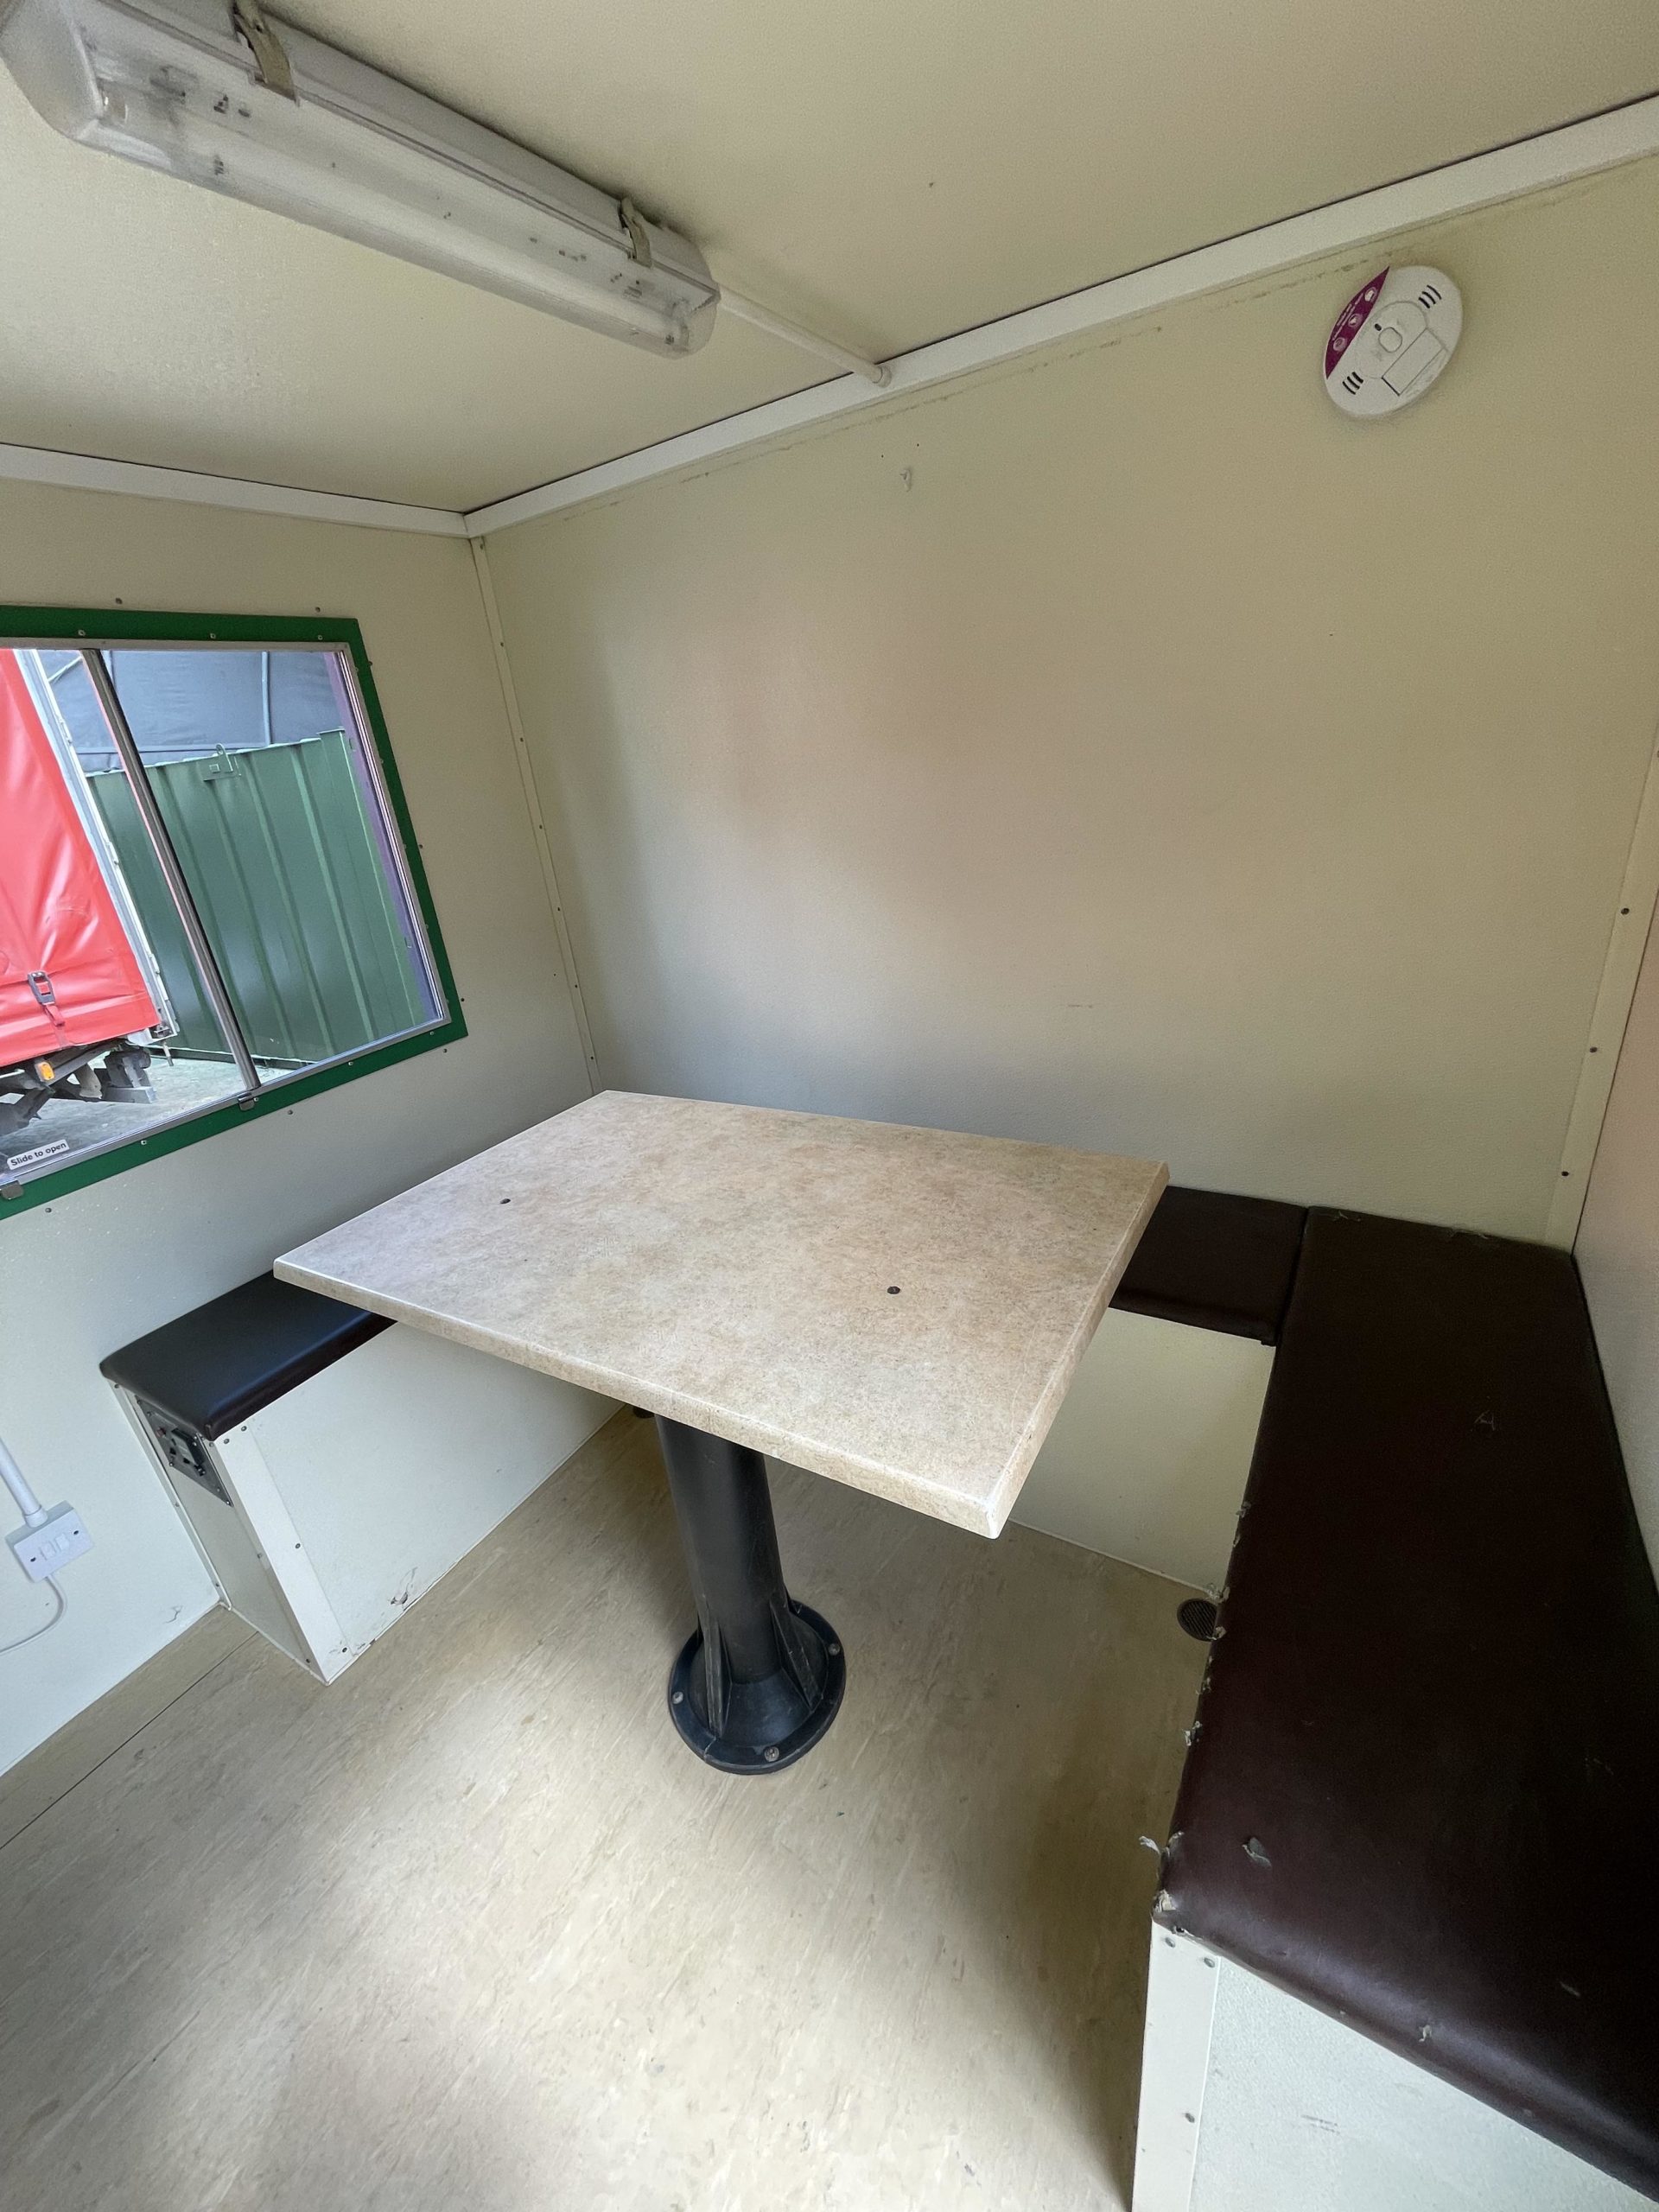
  • 12ft Towable Gound Hog
  • Includes: toilet, canteen and seating area
  • Full working generator, fully serviced and in great condition


Location: Nationwide


£6,500

EX VAT

Not Available for Hire

Call for an instant quote!

  • Reinforced doors with secure locking 
  • Electrics and lights included
  • Sink and water boiler included

Location: Nationwide

Quantity: ∞

£15,000

EX VAT

Not Available for Hire

Call for an instant quote!

• Reinforced doors and windows with secure locking
• Open plan with electric sockets and lighting
• Ral Code Colour of choice

• Any Extras available : Canteen, Partitions, Toilets.

Location: Nationwide


£11,995

EX VAT

Not Available for Hire

Call for an instant quote!

• Reinforced doors and windows with secure locking

• Open plan with electric sockets and lighting

• Ral Code Colour of choice

• Any Extras available : Canteen, Partitions, Toilets.

Location: Nationwide


POA

Not Available for Hire

Call for an instant quote!

test

• Reinforced doors with secure locking
• Sink and water boiler included

Location: Nationwide

Quantity: ∞

£12,495

EX VAT

Not Available for Hire

Call for an instant quote!

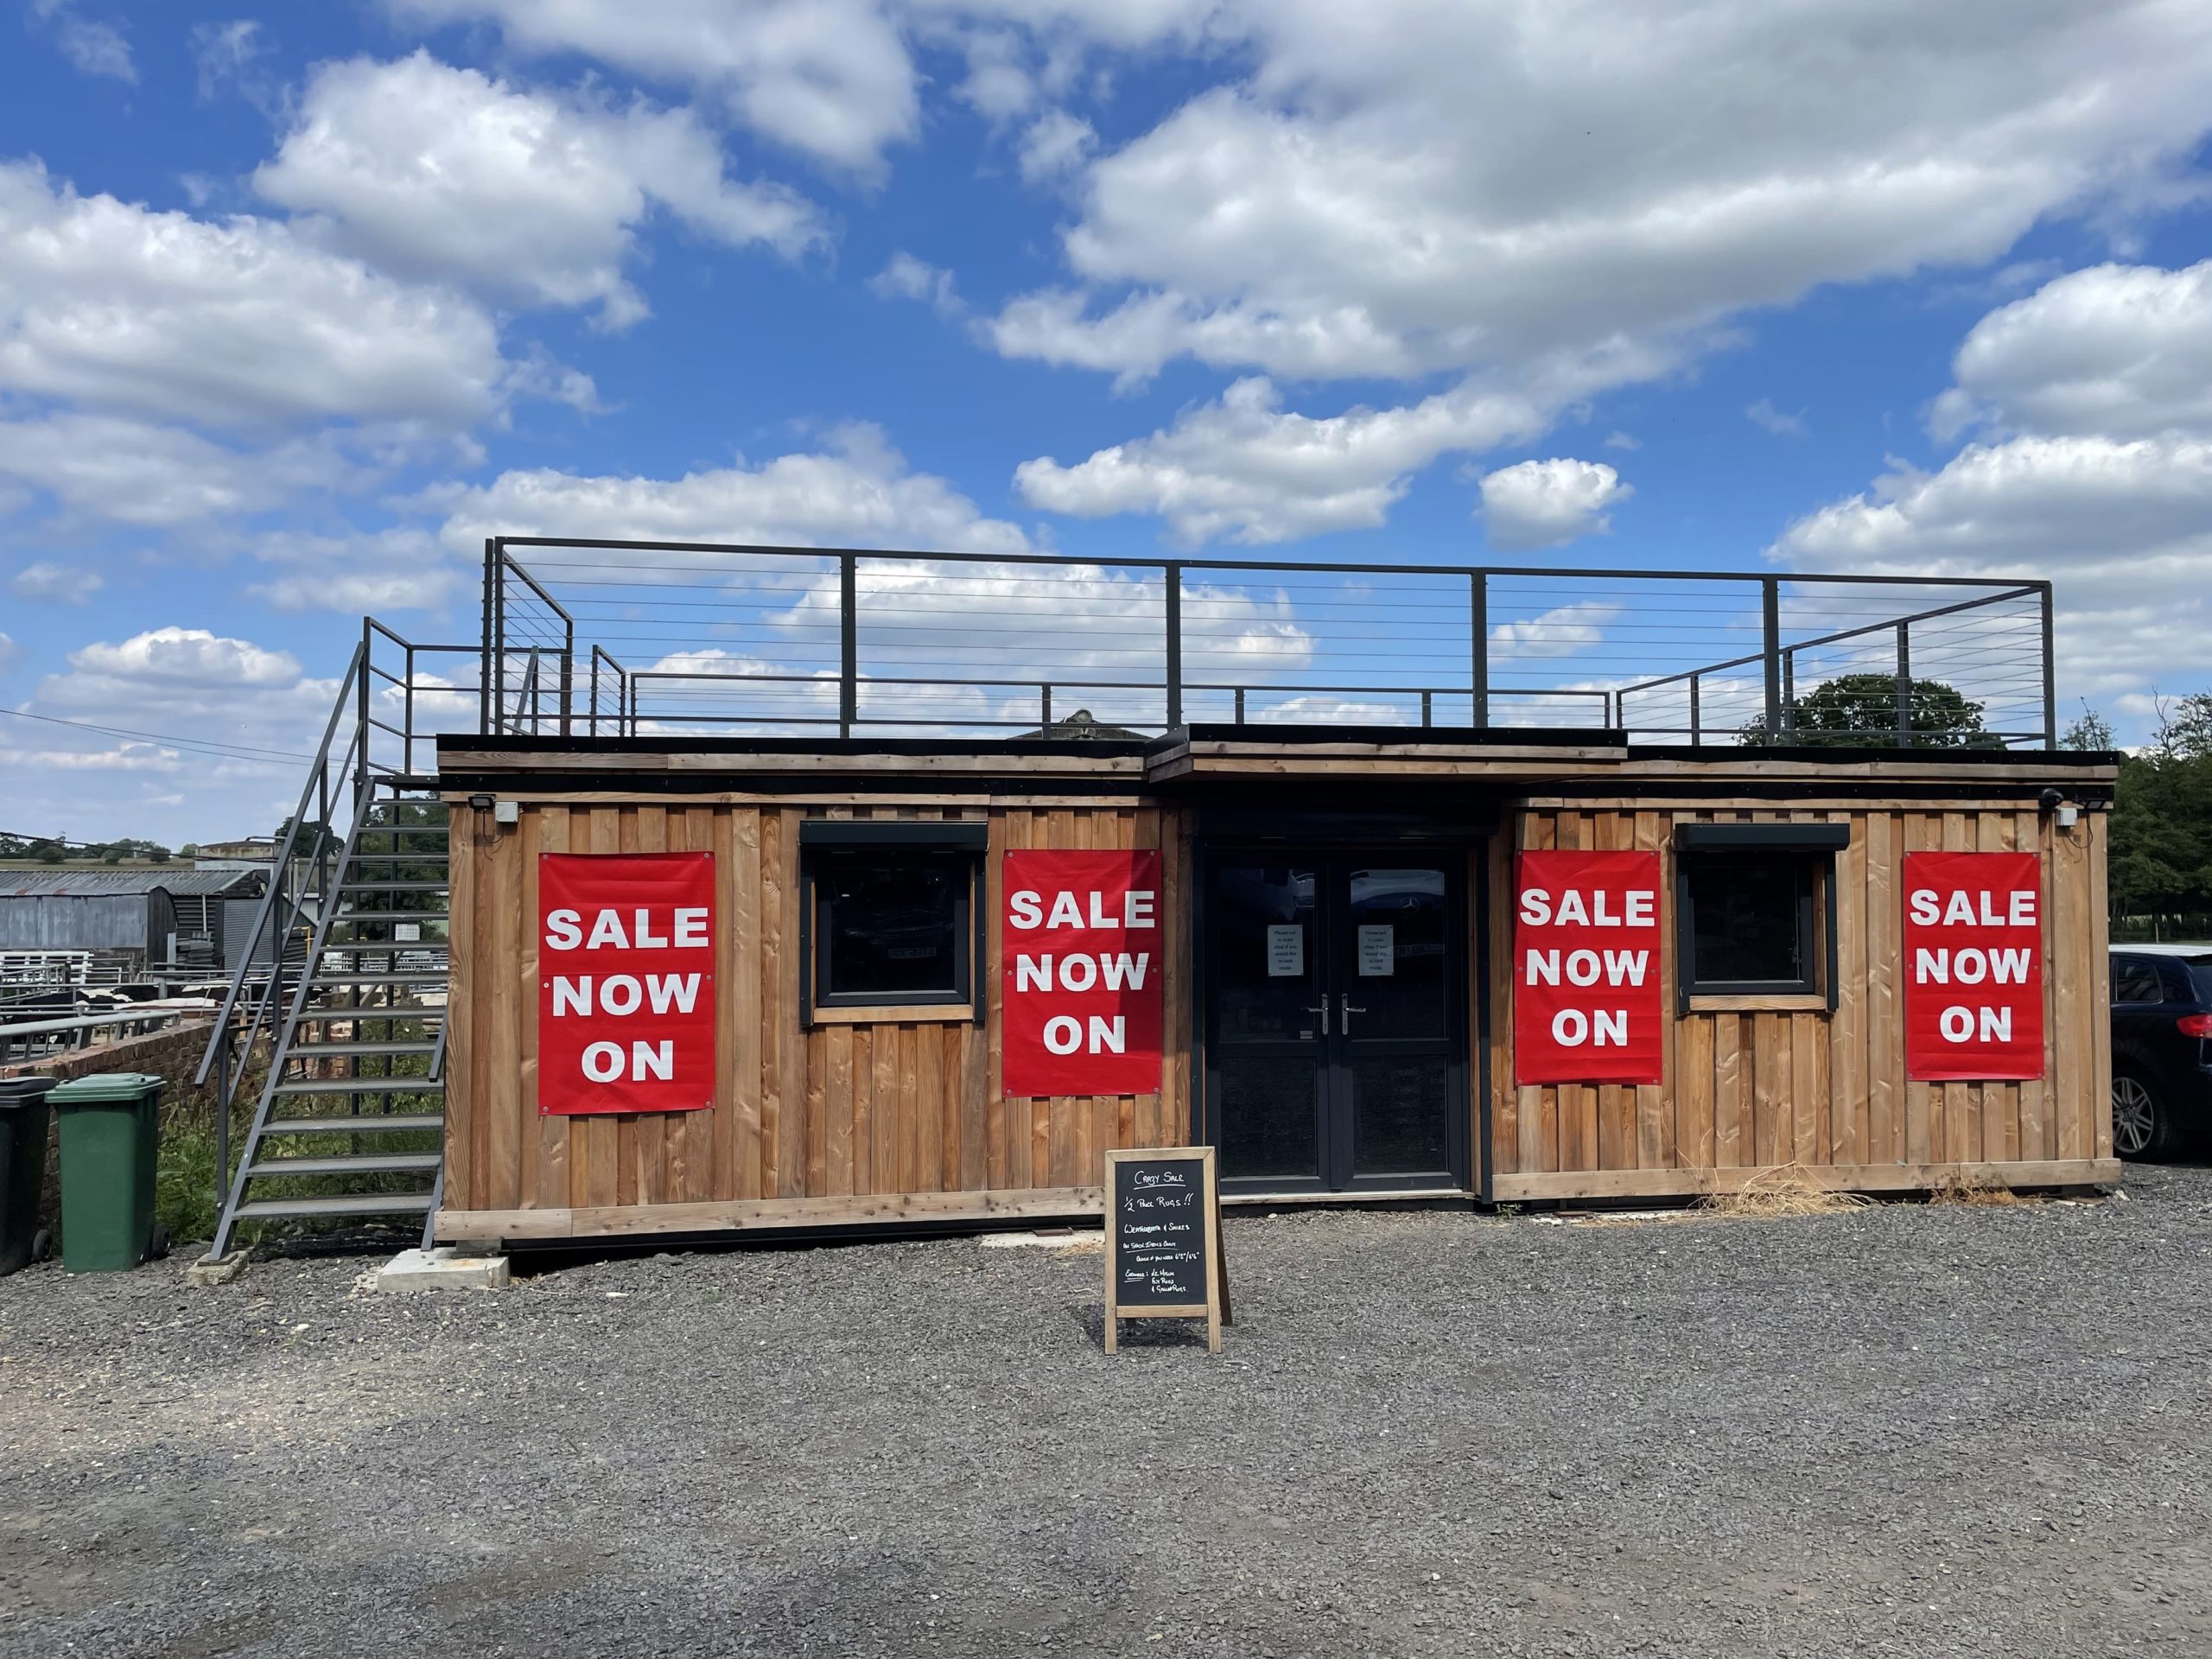
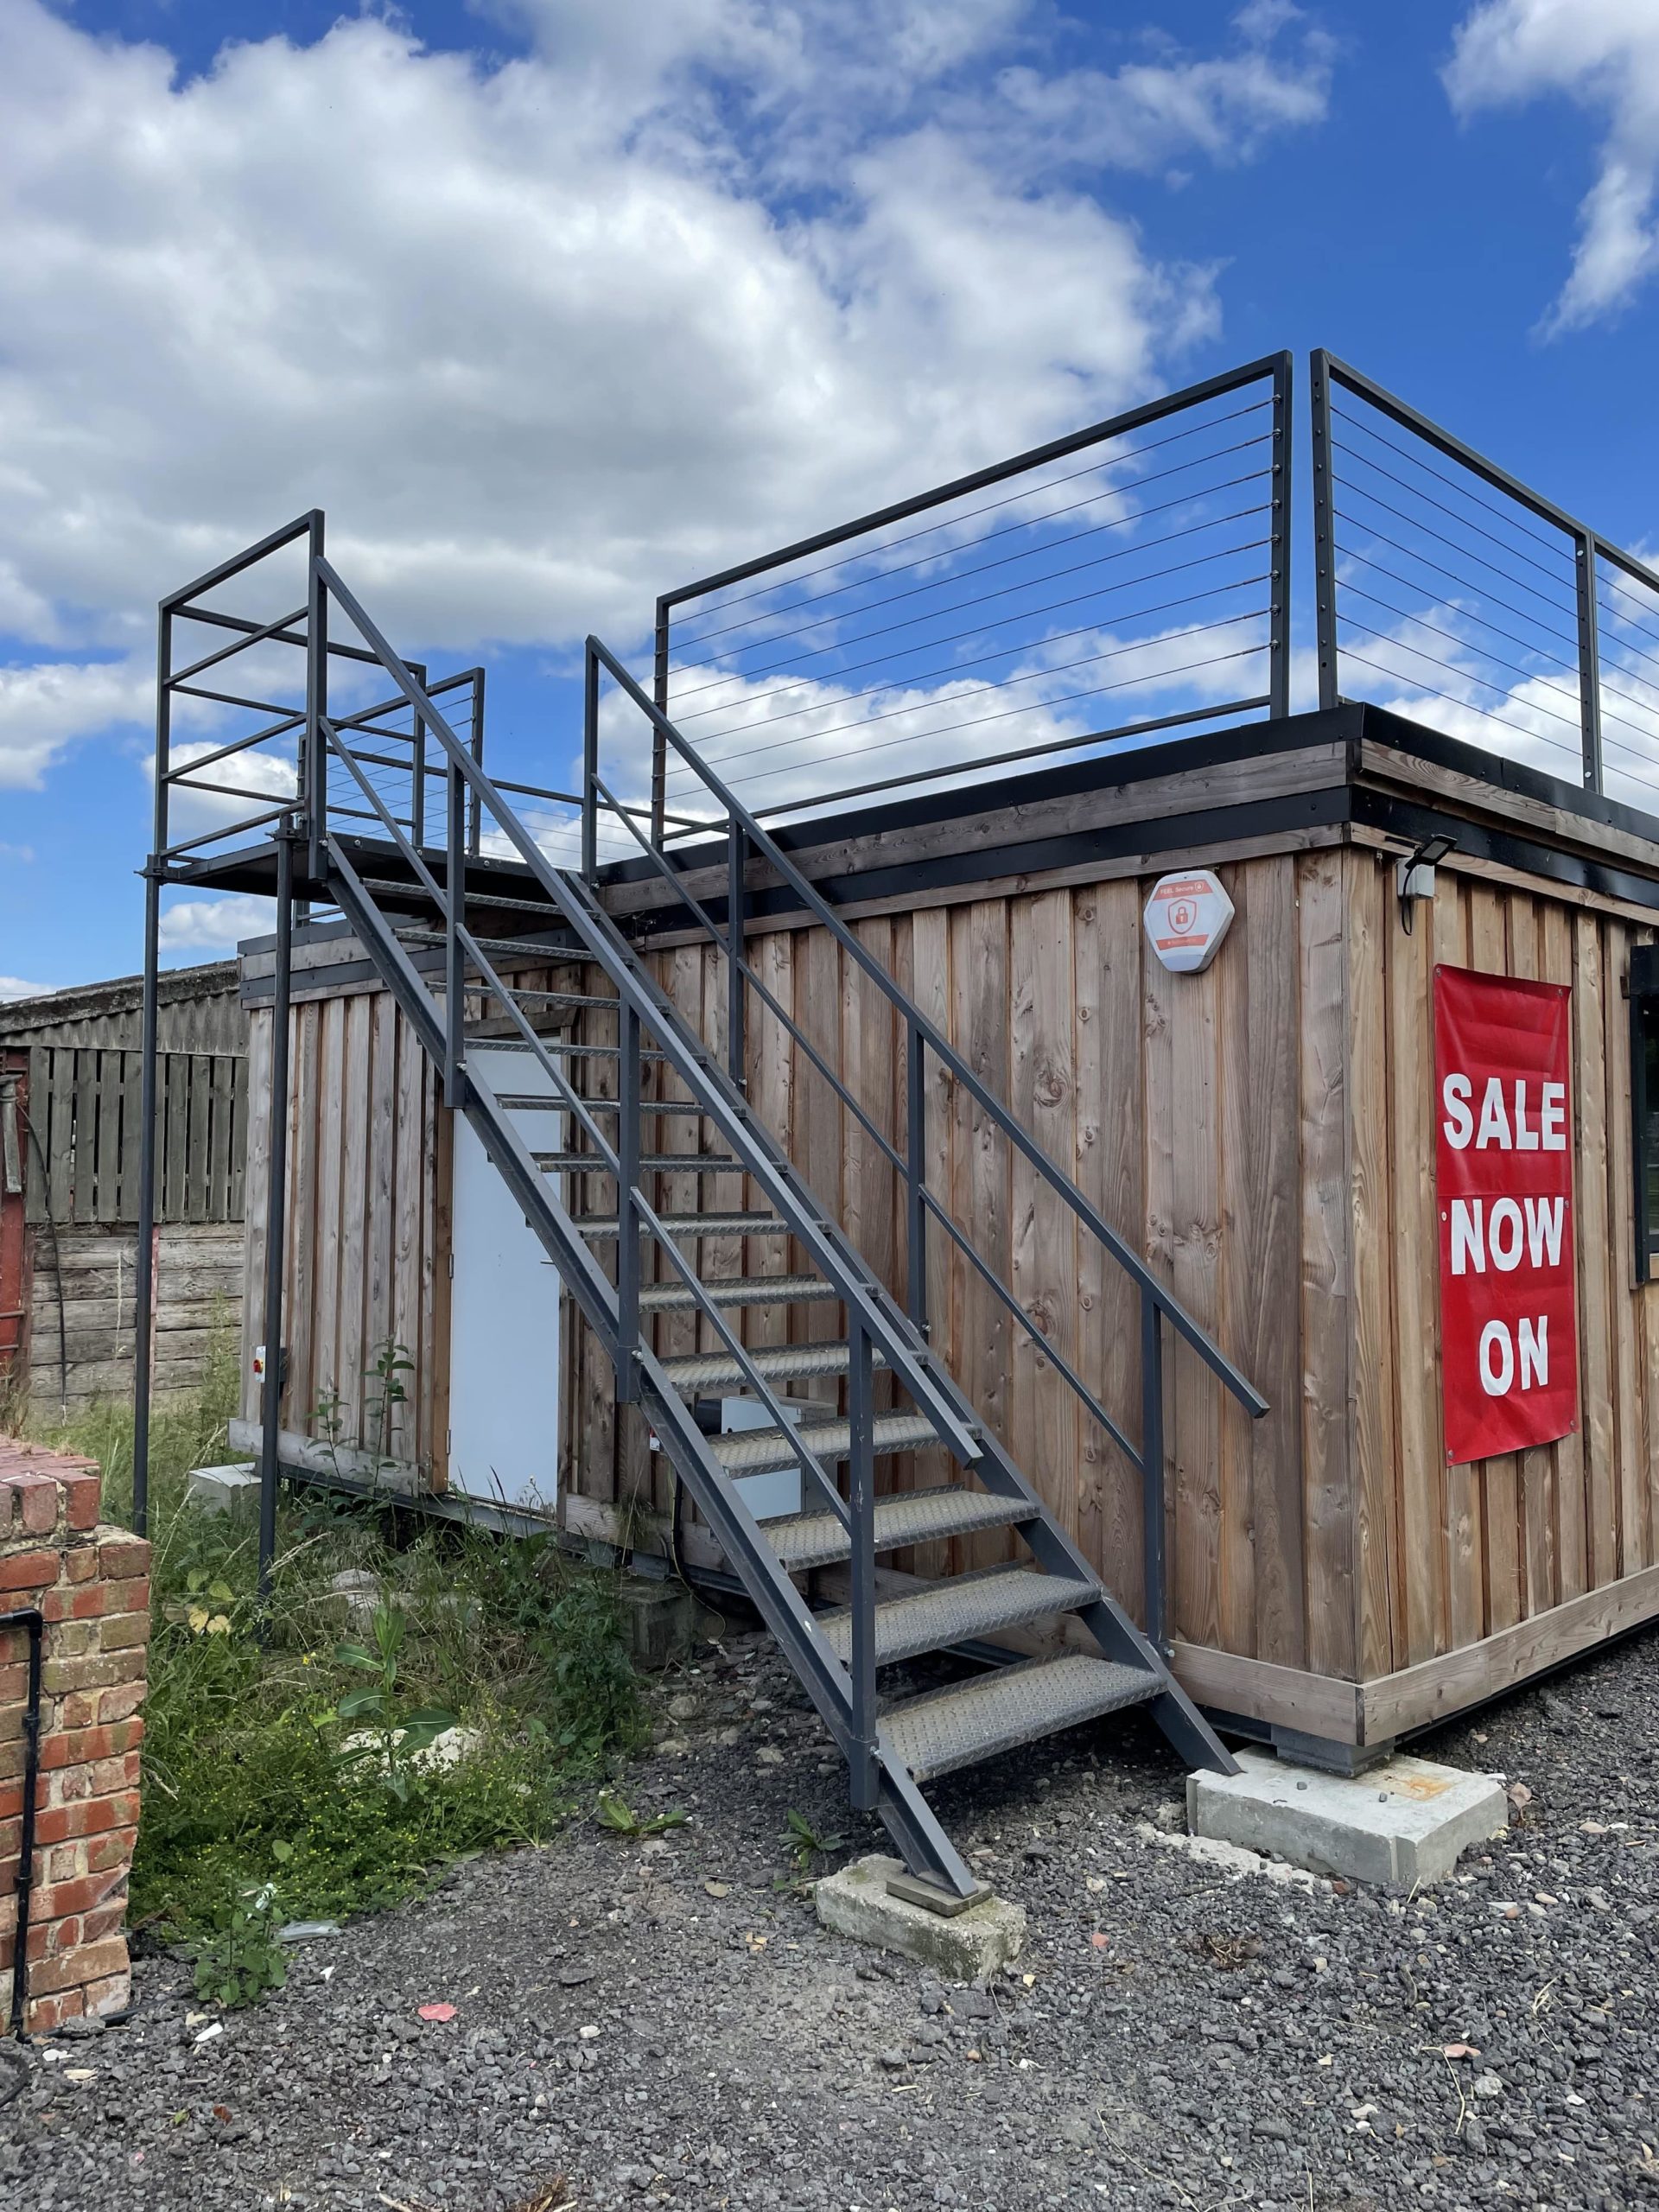
32ft x 20ft Cabin

  • Reinforced doors with secure locking 
  • Electrics and lights included
  • Sink and water boiler included
  • Electric Roller Shutters
  • Roof top terrace 
  • Store Room 
  • Slatwall installation 

Location: Nationwide


£39,000

EX VAT

Not Available for Hire

Call for an instant quote!

Looking to Buy or Hire?

Get a Quick Container Quote Now!

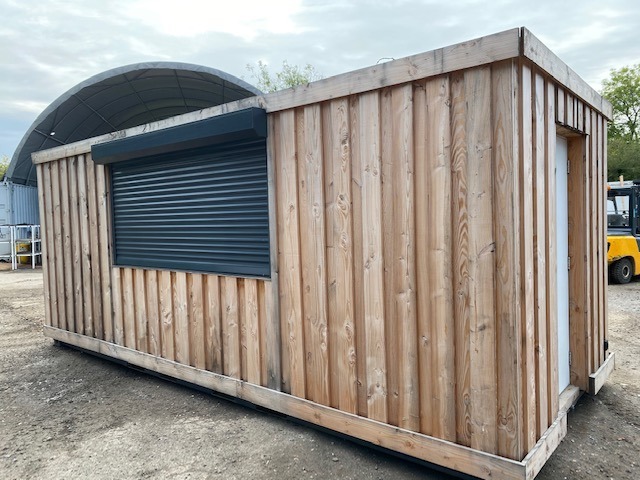
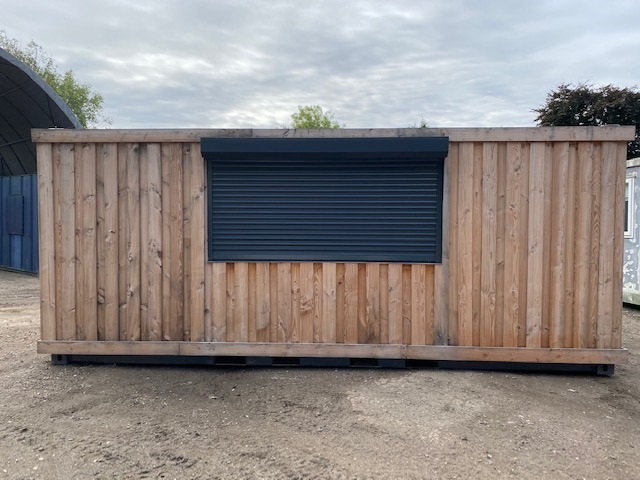
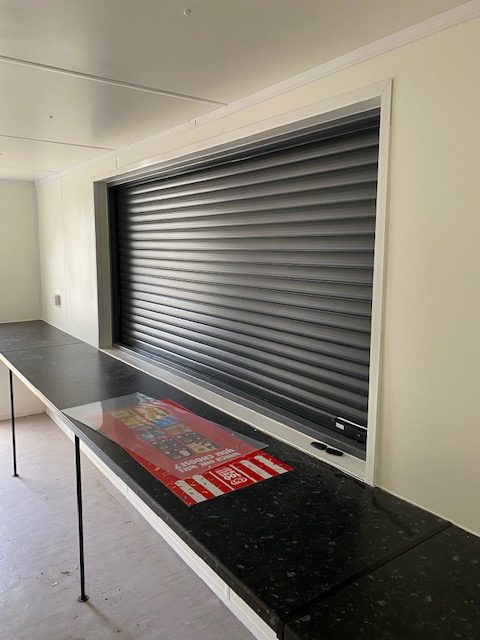
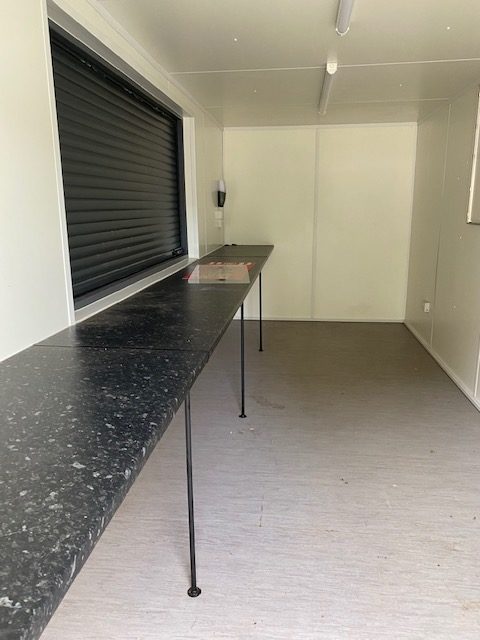
20ft x 8ft Container Kiosk

  • Open plan layout with worktop serving area
  • Electric roller shutter with remote control
  • Electrics and lights included

Location: Nationwide


£15,000

EX VAT

Not Available for Hire

Call for an instant quote!

Looking to Buy?

Get a Quick Container Quote Now!

Newsletter Signup Form

Be the first to discover our exclusive offers and latest company updates by signing up to our email newsletter. Every month we’ll keep you informed of our best prices, industry updates, customer’s container projects, national shows we’ll be exhibiting at, and much more.

Looking to Buy or Hire?

Get a Quick Container Quote Now!